Candy Panning Machine
ProductOverview
A candy panning machine is an industrial batch equipment that applies multiple layers of coating (sugar syrup, chocolate, color, shine dust) onto tumbling candies to create candy centers, dragees, or polish finished hard candies. The machine features a large rotating conical pan (1–1.5 meter diameter) containing 500–1,000 kg of candies that tumble via internal lift flights. A spray nozzle applies syrup atomized by compressed air, and a powder duster follows with starch or sugar coating. Heated or cooled air circulates through the pan to evaporate moisture and set layers. Typical batch time is 30–90 minutes, during which 5–15 coating layers are applied. The panning machine is essential for producing premium coated candies and is the standard choice for chocolates, dragees, and polished hard candies.
Panning is valued for its versatility: the same machine can apply sugar shells, chocolate coatings, or glaze finishes simply by changing the spray liquid and adjusting temperature. Recipe changeover takes minutes.
Pan and tumbling action
The rotating pan is a large stainless steel conical vessel (1.5 m diameter, 1,000 mm height, 2,000 liter capacity typical) with internal spiral or radial lift flights. As the pan rotates at 20–60 rpm via the variable frequency drive, the lift flights continuously elevate candies up the pan wall and cascade them down toward the center. This gentle tumbling action exposes all candy surfaces uniformly to the spray nozzle while preventing breaking or excessive attrition.
The pan inclination (tilt angle) is adjustable via a mechanical frame; a 5–15° tilt enhances cascade action and is often used for smaller candies. Larger candies may require minimal tilt to prevent rolling.
Coating application cycle
A typical panning batch cycle involves multiple repeat steps:
Load: Operator loads 500–1,000 kg of pre-formed candies (e.g., hard candy centers, chocolate truffles) into the pan via a hopper or scoop.
Spray phase (2–5 minutes): Pan rotates at target speed (typically 40 rpm). The spray nozzle atomizes hot syrup (50–80 °C) into the pan, coating all candies. Spray duration is controlled by the PLC timer.
Powder application (1–2 minutes): After syrup spray stops, the powder duster applies starch or powdered sugar, creating a dry outer layer.
Drying (5–10 minutes): The air circulation system circulates heated air (40–60 °C) through the pan, evaporating water and setting the coating.
Cooling (5–10 minutes optional): Air temperature is reduced to ambient to cool candies and harden coating.
Repeat: Steps 2–5 are repeated 5–15 times, building up multiple layers until the desired coating thickness and appearance are achieved.
Total batch time is 30–90 minutes depending on coating complexity. A batch with heavy sugar shell might require 10 cycles (heavy coating); a light glaze might require only 3–5 cycles.
Syrup spray and atomization
The spray system uses a precision nozzle (stainless steel, SAT or Spraying Systems brand) that atomizes syrup into a fine mist. Two methods are common:
Air-assist atomization: Syrup flows at 5–10 bar, and 2–3 bar compressed air is supplied separately through the nozzle, creating very fine droplets (50–100 µm). This is gentler on delicate candies.
Pressure-only atomization: Syrup alone flows at 10–20 bar through a single orifice, creating slightly larger droplets (100–200 µm). This is faster but slightly more aggressive.
The syrup pump (5 cc/rev gear pump, 10 liter/min capacity) maintains consistent flow, and a proportional pressure valve regulates spray pressure to the nozzle, protecting against pressure spikes that can over-saturate candies.
Syrup temperature is maintained via a nozzle RTD sensor; if temperature drifts, the PLC adjusts heater power to maintain setpoint (typically 60 °C for clarity, 70 °C for faster evaporation).
Powder coating and texture
After each syrup spray, a powder duster applies starch, powdered sugar, or talc. The powder serves multiple purposes:
- Dries the sticky syrup-coated surface
- Prevents candies from clumping together
- Adds aesthetic texture (matte vs. gloss finish)
- Reduces surface stickiness during packaging
The powder feed rate is adjustable via the variable-speed auger (20–50 rpm); higher speeds deposit more powder per cycle.
Air circulation and drying
The air circulation system consists of a 1.5 kW blower (5 m³/min) that draws ambient air through an optional 3 kW electric heater before distributing air into the pan via an inlet duct. Moist air exits via an exhaust duct.
Air temperature is critical. At 30–40 °C, drying is slow but gentle. At 50–60 °C, drying is faster and suitable for sugar shells. Above 70 °C, risk of surface crazing or cracking increases, particularly for chocolate-coated candies. The PLC maintains temperature setpoint via a RTD temperature sensor and proportional heater solenoid.
Coating recipes and product types
The panning machine handles diverse candy types:
- Chocolate dragees (chocolate-coated nuts): Core candy tumbled, sprayed with chocolate (melted, ~45 °C), air dried. Multiple passes build a thick shell.
- Polished hard candies: Finished hard candy pieces, sprayed with thin sugar syrup, powdered, air-dried. Creates a shiny finish.
- Cinnamon candies: Hard candy cores, sprayed with hot syrup, dusted with cinnamon-sugar powder, dried. Multiple layers build texture.
- Licorice coatings: Licorice root cores, sprayed with sugar/gum arabic blend, powdered. Creates a chewy outer layer.
- Chocolate-covered fondant: Fondant centers, sprayed with dark chocolate in thin coats, cooled, dusted with cocoa powder. Finished product melts in mouth.
Control and automation
The PLC system manages the entire batch cycle. The operator uses a 7-inch touchscreen HMI to select a pre-programmed recipe or create custom recipes by setting:
- Pan speed (20–60 rpm)
- Spray duration (seconds per cycle)
- Powder application time (seconds)
- Air temperature (°C)
- Drying time (minutes)
- Number of coating cycles (5–15)
The PLC executes the recipe automatically, controlling fan speed (via VFD), spray solenoid timing, powder auger frequency, and heater power. An audible alarm signals when each cycle is complete, prompting the operator to visually inspect candy appearance before triggering the next cycle.
Data logging records all parameters; if coating quality is poor, the operator can adjust and re-run specific cycles.
Production metrics
A mid-size candy panner running a 1-hour batch cycle (load + 10 coating cycles + final cool) produces 500–1,000 kg of finished coated candy per batch. Running two shifts (16 hours) with 80% uptime yields 8–12 batches per day, or 4,000–12,000 kg per day depending on batch size. For a premium candy producer, this represents 15,000–50,000 units daily (assuming 200–300 g average piece weight).
Maintenance and wear
The pan interior is subject to syrup and powder buildup; daily cleaning with hot water and mild caustic (pH 11–12) is standard. The mechanical shaft seal is inspected every 500 hours and replaced every 1,000 hours (cost ~€600–800).
The spray nozzle accumulates sugar crystals and is soaked and cleaned daily. Nozzle replacement cost is ~€200–300 every 2 years.
The blower motor is an EC (electronically commutated) type rated 10+ years. The heating band degrades after 3,000–5,000 operating hours (cost ~€400 to replace).
Stainless steel wetted surfaces (pan, shafts, ducts) last 15+ years with regular cleaning.
Integration in candy lines
Panning is typically a mid-stage operation in candy production lines. A chocolate center line might be: vacuum cooker → cooling → slab cutter → panning machine (multiple passes) → final drying → wrapping. A polished hard candy line might be: candy former → cooling → panner (light glaze) → wrapper → case pack.
Some plants use panning for premium products only (5–10% of output), while bulk candies skip panning and are wrapped directly from cooling.
Candy Panning Machine parts and their functions
8 top-level parts · 41 parts in total · full bill of materials below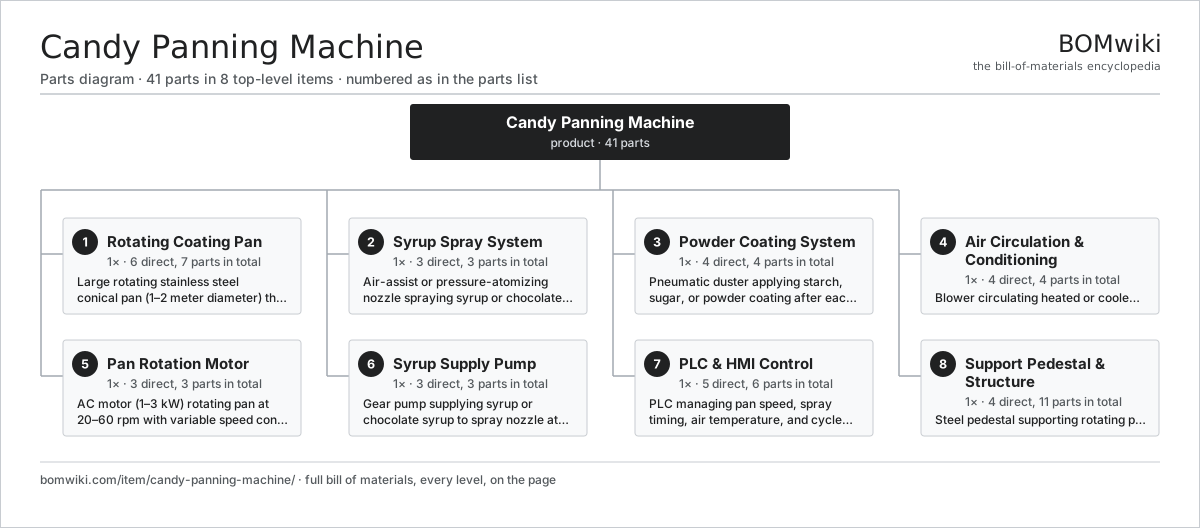
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Rotating Coating Pan 6 parts | 1× | Large rotating stainless steel conical pan (1–2 meter diameter) that tumbles candies during coating |
| 2 | Syrup Spray System 3 parts | 1× | Air-assist or pressure-atomizing nozzle spraying syrup or chocolate into rotating pan |
| 3 | Powder Coating System 4 parts | 1× | Pneumatic duster applying starch, sugar, or powder coating after each syrup spray |
| 4 | Air Circulation & Conditioning 4 parts | 1× | Blower circulating heated or cooled air (30–60 °C) to evaporate moisture and set coating |
| 5 | Pan Rotation Motor 3 parts | 1× | AC motor (1–3 kW) rotating pan at 20–60 rpm with variable speed control |
| 6 | Syrup Supply Pump 3 parts | 1× | Gear pump supplying syrup or chocolate syrup to spray nozzle at controlled flow rate |
| 7 | PLC & HMI Control 5 parts | 1× | PLC managing pan speed, spray timing, air temperature, and cycle duration |
| 8 | Support Pedestal & Structure 4 parts | 1× | Steel pedestal supporting rotating pan, motor, and air circulation ductwork |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Candy Panning Machine
8 top-level lines · 40 rows shown · 41 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Rotating Coating Pan 6 parts | candy-panning-machine-coating-pan | 1× | 1 | 7 | assembly |
| 1.1 | Pan Shell | candy-panning-machine-pan-shell | 1× | 1 | · | part |
| 1.2 | Lift Flights | candy-panning-machine-lift-flights | 1× | 1 | · | part |
| 1.3 | Pan Drive Shaft | candy-panning-machine-pan-shaft | 1× | 1 | · | part |
| 1.4 | Pan Bearing Block | candy-panning-machine-pan-bearing | 2× | 2 | · | part |
| 1.5 | Pan Shaft Seal | candy-panning-machine-pan-seal | 1× | 1 | · | part |
| 1.6 | Adjustable Pan Tilt Frame | candy-panning-machine-tilting-frame | 1× | 1 | · | part |
| 2 | Syrup Spray System 3 parts | candy-panning-machine-syrup-spray | 1× | 1 | 3 | assembly |
| 2.1 | Spray Nozzle | candy-panning-machine-spray-nozzle | 1× | 1 | · | part |
| 2.2 | Nozzle RTD Sensor | candy-panning-machine-nozzle-temperature-probe | 1× | 1 | · | part |
| 2.3 | Inlet Strainer | candy-panning-machine-nozzle-strainer | 1× | 1 | · | part |
| 3 | Powder Coating System 4 parts | candy-panning-machine-powder-duster | 1× | 1 | 4 | assembly |
| 3.1 | Powder Hopper | candy-panning-machine-powder-hopper | 1× | 1 | · | part |
| 3.2 | Powder Dust Nozzle | candy-panning-machine-dust-nozzle | 1× | 1 | · | part |
| 3.3 | Powder Feed Auger | candy-panning-machine-feed-auger | 1× | 1 | · | part |
| 3.4 | Connector | connector | 1× | 1 | · | part |
| 4 | Air Circulation & Conditioning 4 parts | candy-panning-machine-conditioned-air | 1× | 1 | 4 | assembly |
| 4.1 | Blower Motor | candy-panning-machine-blower-motor | 1× | 1 | · | part |
| 4.2 | Heating Band | candy-panning-machine-heating-element | 1× | 1 | · | part |
| 4.3 | Air Inlet Duct | candy-panning-machine-air-inlet-duct | 1× | 1 | · | part |
| 4.4 | Exhaust Duct | candy-panning-machine-exhaust-duct | 1× | 1 | · | part |
| 5 | Pan Rotation Motor 3 parts | candy-panning-machine-drive-motor | 1× | 1 | 3 | assembly |
| 5.1 | Pan Motor | candy-panning-machine-motor-unit | 1× | 1 | · | part |
| 5.2 | Variable Frequency Drive | candy-panning-machine-vfd | 1× | 1 | · | part |
| 5.3 | Motor Coupler | candy-panning-machine-motor-coupler | 1× | 1 | · | part |
| 6 | Syrup Supply Pump 3 parts | candy-panning-machine-syrup-pump | 1× | 1 | 3 | assembly |
| 6.1 | Syrup Pump | candy-panning-machine-gear-pump | 1× | 1 | · | part |
| 6.2 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 6.3 | Pressure Relief Valve | candy-panning-machine-flow-control-valve | 1× | 1 | · | part |
| 7 | PLC & HMI Control 5 parts | candy-panning-machine-control-unit | 1× | 1 | 6 | assembly |
| 7.1 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.2 | Variable Frequency Drive | candy-panning-machine-vfd | 1× | 1 | · | part |
| 7.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.4 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.5 | Connector | connector | 2× | 2 | · | part |
| 8 | Support Pedestal & Structure 4 parts | candy-panning-machine-frame | 1× | 1 | 11 | assembly |
| 8.1 | Sheet Metal Panel | sheet-panel | 2× | 2 | · | part |
| 8.2 | Fastener Set | fastener-set | 3× | 3 | · | part |
| 8.3 | Heavy Pedestal Feet | candy-panning-machine-pedestal-feet | 4× | 4 | · | part |
| 8.4 | Wire Bundle | wire-bundle | 2× | 2 | · | part |
Something wrong in this list? Report a problem with this BOM.
Related products
same domain, ranked by shared parts Candy Cane Machine
258 parts · shares 7 with this page
Candy Twist Wrapper
86 parts · shares 7 with this page
Dough Sheeting Line
456 parts · shares 7 with this page
Egg Breaking and Separating Line
1,126 parts · shares 7 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $1k–$500k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| gea.com ↗ | Düsseldorf, DE | Process technology | 20 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 20 units | 12–20 wks |
| tetrapak.com ↗ | Pully, CH | Food packaging & processing | 20 units | 12–20 wks |
| jbtc.com ↗ | Chicago, US | Food processing equipment | 20 units | 12–20 wks |
| alfalaval.com ↗ | Lund, SE | Heat transfer & separation | 20 units | 12–20 wks |
1,434-word article