Case Erector
ProductOverview
Case erectors are critical machines in bottle-packing lines, automatically building rigid cases from flat cardboard blanks in seconds. The machine receives a flat die-cut cardboard blank from a magazine, uses vacuum and servo mechanics to position it over a lower form, folds up the sides using an upper form, tucks the bottom flaps, applies pressure-sensitive tape to seal the bottom seams, and discharges the completed case onto an infeed conveyor for bottle loading.
Industrial case erectors handle 15–40 cases per minute and adapt to multiple case sizes via changeable forms and adjustable guides. They integrate seamlessly with upstream bottle packers (case fillers) and downstream shipping equipment.
How it works
Blank Magazine Dispensing
Flat cardboard blanks are stacked vertically in a servo-indexed magazine, held vertically under controlled pressure by a spring-loaded separator plate. A stepper motor lowers the magazine continuously as blanks are consumed, maintaining the top blank within reach of the vacuum pickup system. Each blank measures 2–5 mm thick and is dispensed one per cycle.
Vacuum Pickup and Positioning
A pneumatic vacuum pump (0.5–0.8 bar) supplies silicone vacuum cups mounted on a servo-driven head. The head descends, vacuum cups contact the top blank, and the solenoid valve applies vacuum (typically 0.5 bar), lifting the blank from the magazine. The head then raises and positions the blank horizontally above the lower erector form (a fixed mandrel sized to the case interior dimensions).
Erection: Forming Sidewalls
The blank is dropped onto the lower form (a flat platform with edge guides). An upper form, a servo-driven or pneumatic-driven assembly, descends over the lower form, pinching and folding the blank's four sides upward simultaneously. Internal cams on the upper form fold the flaps at precise angles, creating a rigid box shell with open top and bottom. The upper form opens (withdraws upward), and the erected case advances to the next station.
Bottom Flap Folding
Two stationary flap-folder dies (left and right) are positioned at the case bottom. As the partially formed case advances through the folder station, the dies pinch and tuck the bottom flaps inward, creating a "bottomed" case shape. Optional servo motors can apply additional downward force if flap material is heavy or springy.
Tape Sealing
A motorized tape applicator head descends to the bottom seam area. A pneumatic brake-controlled tape reel dispenses 48–72 mm wide pressure-sensitive tape (clear or kraft paper), and the servo-driven applicator head positions the tape roll over the case's bottom center seam. Tape is pressed onto the flap surfaces with force, and a heated roller (50–70 °C) passes over the tape, enhancing adhesive bond strength. A cutter blade (hot-wire or mechanical) severs the tape after application. The process repeats for the side seams if required.
Discharge and Integration
After taping, a solenoid gate opens, releasing the completed case onto a discharge conveyor. The conveyor runs at synchronized speed with the case-packing equipment downstream, ensuring continuous bottle-loading without gaps or collisions.
Servo Control and Synchronization
A PLC orchestrates all motions: magazine motor, vacuum cup pickup, form closure, flap folding, tape application, and discharge. Line-rate encoder feedback from the upstream bottle packer allows the erector to match incoming bottle flow, preventing starvation or overflow.
Typical Applications
Beverage bottles in 4-packs, 6-packs, 12-packs, and 24-packs. Cases range from small 12 oz cans (3 L / 12-case) to 2L bottles (6–8 cases). Craft beverages, juice, sports drinks, and energy drinks commonly use corrugated cardboard cases.
Case Size Changeover
Changing case dimensions requires: (1) replacing the upper form dies (10–15 min), (2) adjusting magazine width guides (5 min), (3) updating PLC recipe with new case footprint and cycle times. Typically 30–45 minutes total, no structural frame changes needed.
Tape Material and Adhesive
Standard pressure-sensitive acrylic tape (48–72 mm wide, 3 mil thick) is preferred for food-safe, moisture-resistant sealing. Kraft paper backing is environmentally friendly; clear polypropylene is used for cosmetics and pharmaceuticals where transparency is desired. Adhesive maintains bond strength at 2–40 °C storage.
Vacuum Cup Maintenance
Silicone cups wear over time (after 100,000+ cycles) and may lose suction if glazed or damaged. Cups are inspected quarterly for wear, cleaned with mild detergent, and replaced annually or per performance metrics. Soft cups prevent blank marking; hard compounds increase durability but risk print damage.
Tape Applicator Troubleshooting
Common issues: (1) Tape wrinkles if reel tension is too loose; tension brake adjustment on reel motor. (2) Poor adhesion if heater roller temperature drops below 50 °C; heating element replacement. (3) Cutter blade dulling; blade sharpening or replacement every 500,000 cuts. (4) Case warping if flap folder pressure is excessive; force reducer valve adjustment.
Integration with Packaging Line
Case erectors are positioned immediately before bottle-loading equipment (case fillers or robotic case packers). Discharge conveyor synchronization is typically managed by a common master PLC or via hardwired encoder handshake, ensuring zero bottle-to-case timing errors.
Case Erector parts and their functions
8 top-level parts · 29 parts in total · full bill of materials below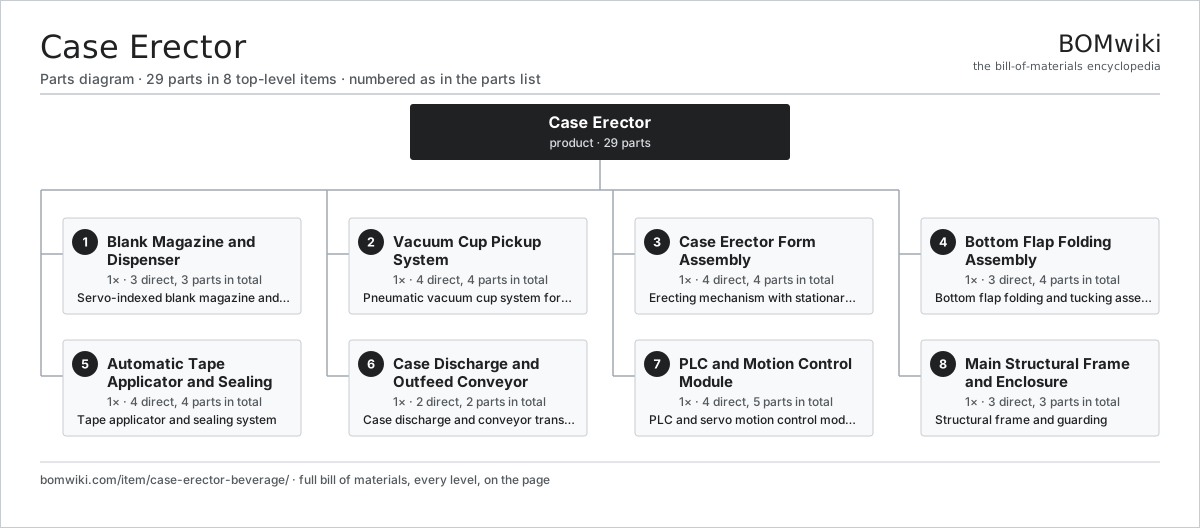
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Blank Magazine and Dispenser 3 parts | 1× | Servo-indexed blank magazine and dispenser |
| 2 | Vacuum Cup Pickup System 4 parts | 1× | Pneumatic vacuum cup system for blank pickup |
| 3 | Case Erector Form Assembly 4 parts | 1× | Erecting mechanism with stationary and moving forms |
| 4 | Bottom Flap Folding Assembly 3 parts | 1× | Bottom flap folding and tucking assembly |
| 5 | Automatic Tape Applicator and Sealing 4 parts | 1× | Tape applicator and sealing system |
| 6 | Case Discharge and Outfeed Conveyor 2 parts | 1× | Case discharge and conveyor transfer |
| 7 | PLC and Motion Control Module 4 parts | 1× | PLC and servo motion control module |
| 8 | Main Structural Frame and Enclosure 3 parts | 1× | Structural frame and guarding |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Case Erector
8 top-level lines · 38 rows shown · 29 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Blank Magazine and Dispenser 3 parts | case-erector-beverage-blank-mag | 1× | 1 | 3 | assembly |
| 1.1 | Magazine Structure | case-erector-beverage-magazine-struct | 1× | 1 | · | part |
| 1.2 | Top Separator Plate | case-erector-beverage-separator-plate | 1× | 1 | · | part |
| 1.3 | Magazine Servo Motor | case-erector-beverage-mag-motor | 1× | 1 | · | part |
| 2 | Vacuum Cup Pickup System 4 parts | case-erector-beverage-vacuum-cup | 1× | 1 | 4 | assembly |
| 2.1 | Vacuum Cup Manifold | case-erector-beverage-vacuum-cup-head | 1× | 1 | · | part |
| 2.2 | Vacuum Pump 1 parts | case-erector-beverage-vacuum-pump | 1× | 1 | 1 | assembly |
| 2.2.1 | Vacuum Pump Motor | case-erector-beverage-vac-pump-motor | 1× | 1 | · | part |
| 2.3 | Pickup Head Servo Motor | case-erector-beverage-pickup-motor | 1× | 1 | · | part |
| 2.4 | Vacuum Release Solenoid Valve | case-erector-beverage-solenoid-valve | 1× | 1 | · | part |
| 3 | Case Erector Form Assembly 4 parts | case-erector-beverage-erector-assy | 1× | 1 | 4 | assembly |
| 3.1 | Lower Case Form and Mandrel | case-erector-beverage-lower-form | 1× | 1 | · | part |
| 3.2 | Upper Servo-Driven Form | case-erector-beverage-upper-form | 1× | 1 | · | part |
| 3.3 | Form Open-Close Motor | case-erector-beverage-erector-motor | 1× | 1 | · | part |
| 3.4 | Form Closure Sensor | case-erector-beverage-form-sensor | 1× | 1 | · | part |
| 4 | Bottom Flap Folding Assembly 3 parts | case-erector-beverage-folder-assy | 1× | 1 | 4 | assembly |
| 4.1 | Flap Folder Die | case-erector-beverage-flap-folder | 2× | 2 | · | part |
| 4.2 | Flap Pusher Motor (optional) | case-erector-beverage-folder-motor | 1× | 1 | · | part |
| 4.3 | Flap Fold Confirmation Sensor | case-erector-beverage-folder-sensor | 1× | 1 | · | part |
| 5 | Automatic Tape Applicator and Sealing 4 parts | case-erector-beverage-taper-assy | 1× | 1 | 4 | assembly |
| 5.1 | Tape Dispenser Reel Assembly 1 parts | case-erector-beverage-tape-reel | 1× | 1 | 1 | assembly |
| 5.1.1 | Tape Reel Motor | case-erector-beverage-tape-motor-drive | 1× | 1 | · | part |
| 5.2 | Tape Applicator Head 1 parts | case-erector-beverage-tape-head | 1× | 1 | 1 | assembly |
| 5.2.1 | Tape Cutter Blade | case-erector-beverage-tape-cutter | 1× | 1 | · | part |
| 5.3 | Tape Adhesion Heater-Roller | case-erector-beverage-tape-heater | 1× | 1 | · | part |
| 5.4 | Applicator Head Servo Motor | case-erector-beverage-tape-motor | 1× | 1 | · | part |
| 6 | Case Discharge and Outfeed Conveyor 2 parts | case-erector-beverage-discharge | 1× | 1 | 2 | assembly |
| 6.1 | Discharge Conveyor Motor | case-erector-beverage-discharge-motor | 1× | 1 | · | part |
| 6.2 | Discharge Gate Solenoid | case-erector-beverage-exit-gate | 1× | 1 | · | part |
| 7 | PLC and Motion Control Module 4 parts | case-erector-beverage-servo-drives | 1× | 1 | 5 | assembly |
| 7.1 | Case Erector Control PLC | case-erector-beverage-plc | 1× | 1 | · | part |
| 7.2 | Motor Servo Amplifier | case-erector-beverage-servo-amp | 2× | 2 | · | part |
| 7.3 | Touch Digitizer | touch-digitizer | 1× | 1 | · | part |
| 7.4 | Encoder | encoder | 1× | 1 | · | part |
| 8 | Main Structural Frame and Enclosure 3 parts | case-erector-beverage-frame | 1× | 1 | 3 | assembly |
| 8.1 | Structural Steel Frame | case-erector-beverage-frame-struct | 1× | 1 | · | part |
| 8.2 | Electrical Enclosure | case-erector-beverage-electrical-box | 1× | 1 | · | part |
| 8.3 | Safety Guard Assembly | case-erector-beverage-guard | 1× | 1 | · | part |
Something wrong in this list? Report a problem with this BOM.
Related products
same domain, ranked by shared parts Aerosol Filling Machine
119 parts · shares 1 with this page
Automatic Labeling Machine
104 parts · shares 1 with this page
Automatic Screen Printing Machine
640 parts · shares 1 with this page
 Automatic Strapping Machine
251 parts · shares 1 with this page
Banner Welder
90 parts · shares 1 with this page
 Blister Packaging Machine
256 parts · shares 1 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$3M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| heidelberg.com ↗ | Heidelberg, DE | Printing presses | 10 units | 12–22 wks |
|
🇨🇭Bobst
bobst.com ↗
|
Lausanne, CH | Packaging machinery | 10 units | 12–22 wks |
| koenig-bauer.com ↗ | Würzburg, DE | Printing presses | 10 units | 12–22 wks |
| wuh-group.com ↗ | Lengerich, DE | Flexible packaging machines | 10 units | 12–22 wks |
| markandy.com ↗ | Chesterfield, US | Label presses | 10 units | 12–22 wks |
843-word article