Concrete Block Machine
ProductOverview
A concrete block machine mass-produces masonry units, hollow blocks, solid blocks, paving stones and kerbs, by compacting zero-slump concrete in a steel mold under simultaneous vibration and top pressure. Because the mix contains barely enough water to hydrate the cement, a freshly molded block holds its shape the instant the mold lifts away. That single property drives the whole machine concept: blocks are formed on flat production pallets, immediately stripped, and carried off still green, so one mold produces a new pallet of products every 15–25 seconds. A mid-size plant makes 1,500–2,500 standard 8-inch blocks per hour around a single machine.
The machine itself is a vertically stacked press built on the Machine Frame. From bottom to top: the Pallet Handling System system slides a pallet onto the Vibration Table, the Mold and Vibration Table clamps the mold over it, the Feed Hopper System doses concrete into the cavities, and the Tamper Head Press presses down from above while the table shakes.
The machine cycle
A cycle begins when the Infeed Conveyor indexes an empty Production Pallet under the mold and the mold lowers onto it, sealing the cavity bottoms. The Feed Drawer then strokes forward from the Main Hopper; its Agitator Grid churns the stiff mix so it rains evenly into the cavities. A short burst of feed vibration during this dwell settles material into corners and webs, uneven filling at this stage is the dominant cause of weight and strength scatter between cavities, so drawer stroke, dwell and agitator speed are all recipe parameters held by the PLC Controller.
The drawer retracts, scraping the mold top flush, and the Tamper Shoe descends into the cavities. Main vibration and press force are applied together: the Vibrator Motor pair spins counter-rotating eccentrics at 50–100 Hz, momentarily fluidizing the mix, while the Press Cylinder pair pushes the shoe down with 30–60 kN. Particles rearrange into a dense packing in two to four seconds, the head landing on the Height Stop blocks that fix block height to about ±1 mm. Density, not time, is the goal, modern machines monitor head displacement and cut vibration the moment the stop is reached, since excess vibration only wears the mold and segregates aggregate.
Stripping follows. The Mold Stripping Cylinder pair lifts the Mold Frame while the tamper head holds the blocks down, so the products release cleanly from the cavity walls. The head then retracts, the Pallet Pusher indexes the loaded pallet onto the Takeoff Conveyor, and a fresh pallet from the Pallet Magazine takes its place.
Vibration system
Compaction quality lives in the vibration table. Two synchronized eccentric shafts run counter-rotating weights so horizontal forces cancel and the table moves purely vertically; phase-shifting the weights relative to each other adjusts the resultant force without changing speed. Older machines used fixed-eccentric hydraulic vibrators switched on and off; current servo-driven tables ramp frequency and amplitude within a single cycle, gentle for filling, hard for compaction, and reach full force in a few table revolutions. The Vibration Isolator mounts decouple this energy from the Base Frame and foundation. The Guide Column set keeps mold and head square through all of it; column wear shows up directly as flash on the block edges.
Tooling and products
The Mold Box and matching tamper shoe define the product, and changing them converts the machine from hollow blocks to pavers or kerbs in under an hour on quick-change designs. Molds are the main consumable: cavity walls are hardened or carbide-faced, yet abrasion from quartz aggregate retires a mold after roughly 80,000–120,000 cycles. For colored or wear-faced pavers, the Face-Mix Unit deposits a 5–10 mm fine-aggregate layer on top of the base mix before a second press, bonding the two layers in the green state.
Hydraulics and control
The Hydraulic Power Unit supplies every linear motion. A pressure-compensated Main Hydraulic Pump driven by the Pump Motor feeds the Valve Stand, whose proportional valves shape each stroke, fast approach, cushioned landing, while the Oil Cooler rejects the heat of continuous cycling. The PLC sequences roughly a dozen interlocked motions per cycle and stores them as recipes in the Recipe Memory, so switching products recalls feed times, vibration profiles and press forces along with the tooling. Downstream, pallets of green blocks travel to curing chambers for 6–24 hours before cubing; the pallet circuit returning empties to the magazine closes the loop, and total plant output is set by whichever of machine cycle, curing capacity or pallet count saturates first.
Concrete Block Machine parts and their functions
7 top-level parts · 118 parts in total · full bill of materials below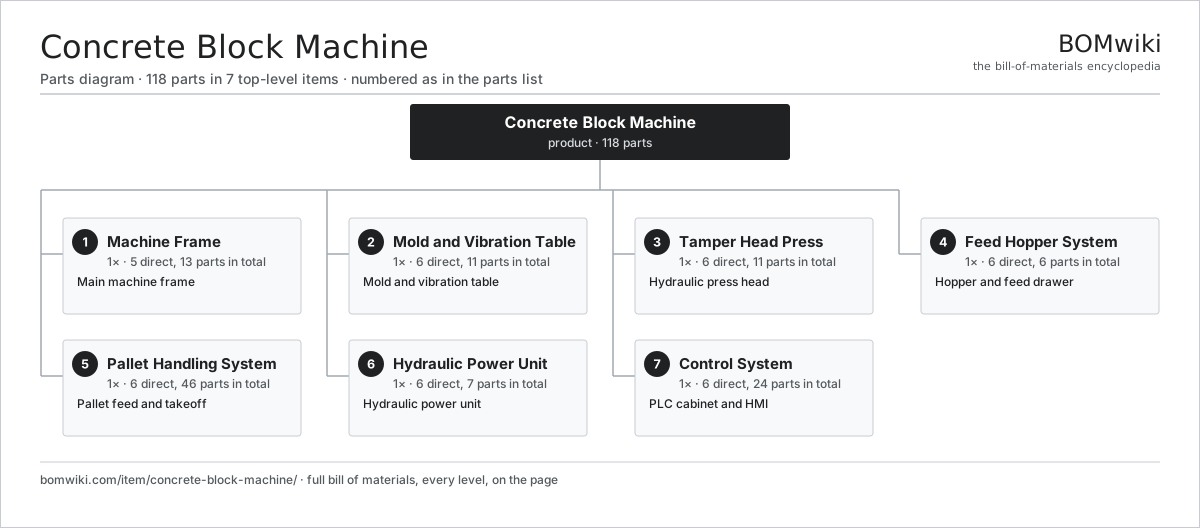
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Machine Frame 5 parts | 1× | Main machine frame |
| 2 | Mold and Vibration Table 6 parts | 1× | Mold and vibration table |
| 3 | Tamper Head Press 6 parts | 1× | Hydraulic press head |
| 4 | Feed Hopper System 6 parts | 1× | Hopper and feed drawer |
| 5 | Pallet Handling System 6 parts | 1× | Pallet feed and takeoff |
| 6 | Hydraulic Power Unit 6 parts | 1× | Hydraulic power unit |
| 7 | Control System 6 parts | 1× | PLC cabinet and HMI |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Concrete Block Machine
7 top-level lines · 48 rows shown · 118 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Machine Frame 5 parts | concrete-block-machine-frame | 1× | 1 | 13 | assembly |
| 1.1 | Base Frame | concrete-block-machine-base-frame | 1× | 1 | · | part |
| 1.2 | Guide Column | concrete-block-machine-guide-column | 4× | 4 | · | part |
| 1.3 | Crosshead Beam | concrete-block-machine-crosshead | 1× | 1 | · | part |
| 1.4 | Vibration Isolator | concrete-block-machine-isolator | 6× | 6 | · | part |
| 1.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Mold and Vibration Table 6 parts | concrete-block-machine-mold-station | 1× | 1 | 11 | assembly |
| 2.1 | Mold Box | concrete-block-machine-mold-box | 1× | 1 | · | part |
| 2.2 | Mold Frame | concrete-block-machine-mold-frame | 1× | 1 | · | part |
| 2.3 | Vibration Table | concrete-block-machine-vibration-table | 1× | 1 | · | part |
| 2.4 | Vibrator Motor | concrete-block-machine-vibrator-motor | 2× | 2 | · | part |
| 2.5 | Mold Stripping Cylinder | concrete-block-machine-mold-cylinder | 2× | 2 | · | part |
| 2.6 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 3 | Tamper Head Press 6 parts | concrete-block-machine-tamper-head | 1× | 1 | 11 | assembly |
| 3.1 | Press Cylinder | concrete-block-machine-press-cylinder | 2× | 2 | · | part |
| 3.2 | Tamper Shoe | concrete-block-machine-tamper-shoe | 1× | 1 | · | part |
| 3.3 | Tamper Head Frame | concrete-block-machine-head-frame | 1× | 1 | · | part |
| 3.4 | Height Stop | concrete-block-machine-height-stop | 2× | 2 | · | part |
| 3.5 | Oil Seal | oil-seal | 4× | 4 | · | part |
| 3.6 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 4 | Feed Hopper System 6 parts | concrete-block-machine-feed-system | 1× | 1 | 6 | assembly |
| 4.1 | Main Hopper | concrete-block-machine-main-hopper | 1× | 1 | · | part |
| 4.2 | Feed Drawer | concrete-block-machine-feed-drawer | 1× | 1 | · | part |
| 4.3 | Agitator Grid | concrete-block-machine-agitator-grid | 1× | 1 | · | part |
| 4.4 | Drawer Drive | concrete-block-machine-drawer-drive | 1× | 1 | · | part |
| 4.5 | Face-Mix Unit | concrete-block-machine-face-mix-unit | 1× | 1 | · | part |
| 4.6 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 5 | Pallet Handling System 6 parts | concrete-block-machine-pallet-handling | 1× | 1 | 46 | assembly |
| 5.1 | Pallet Magazine | concrete-block-machine-pallet-magazine | 1× | 1 | · | part |
| 5.2 | Production Pallet | concrete-block-machine-pallet | 40× | 40 | · | part |
| 5.3 | Infeed Conveyor | concrete-block-machine-infeed-conveyor | 1× | 1 | · | part |
| 5.4 | Takeoff Conveyor | concrete-block-machine-takeoff-conveyor | 1× | 1 | · | part |
| 5.5 | Pallet Pusher | concrete-block-machine-pallet-pusher | 1× | 1 | · | part |
| 5.6 | Encoder | encoder | 2× | 2 | · | part |
| 6 | Hydraulic Power Unit 6 parts | concrete-block-machine-hydraulic-pack | 1× | 1 | 7 | assembly |
| 6.1 | Pump Motor | concrete-block-machine-hpu-motor | 1× | 1 | · | part |
| 6.2 | Main Hydraulic Pump | concrete-block-machine-hpu-pump | 1× | 1 | · | part |
| 6.3 | Valve Stand | concrete-block-machine-valve-stand | 1× | 1 | · | part |
| 6.4 | Oil Cooler | concrete-block-machine-oil-cooler | 1× | 1 | · | part |
| 6.5 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 6.6 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 7 | Control System 6 parts | concrete-block-machine-control-system | 1× | 1 | 24 | assembly |
| 7.1 | PLC Controller | concrete-block-machine-plc | 1× | 1 | · | part |
| 7.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.3 | Recipe Memory | concrete-block-machine-recipe-store | 1× | 1 | · | part |
| 7.4 | Relay | relay | 8× | 8 | · | part |
| 7.5 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 7.6 | Connector | connector | 12× | 12 | · | part |
Something wrong in this list? Report a problem with this BOM.
Related products
same domain, ranked by shared parts Asphalt Recycler
226 parts · shares 6 with this page
 Bridge Girder Launching Gantry
1,542 parts · shares 6 with this page
 Flat-Top Tower Crane
358 parts · shares 6 with this page
 Ground Anchor Drill Rig
142 parts · shares 6 with this page
 Guardrail Installation Rig
320 parts · shares 6 with this page
 Jet Grouting Rig
154 parts · shares 6 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $15k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| caterpillar.com ↗ | Irving, US | Construction & mining equipment | made to order | 16–28 wks |
|
🇯🇵Komatsu
komatsu.com ↗
|
Tokyo, JP | Construction & mining equipment | made to order | 16–28 wks |
|
🇸🇪Volvo CE
volvoce.com ↗
|
Gothenburg, SE | Construction equipment | made to order | 16–28 wks |
|
🇨🇭Liebherr
liebherr.com ↗
|
Bulle, CH | Cranes & heavy equipment | made to order | 16–28 wks |
|
🇨🇳XCMG
xcmg.com ↗
|
Xuzhou, CN | Construction machinery | made to order | 16–28 wks |
856-word article