Mattress Roll-Pack Machine
ProductOverview
The mattress roll-packing machine is specialized equipment for shipping optimization and logistics. It compresses finished mattresses (after all surface treatments, tufting, and binding are complete) to approximately 50–70% of their original thickness, then encases the compressed mattress in plastic film and applies a heat-sealed closure. This packaging reduces shipping volume dramatically, lowering freight costs for mattress retailers and online sellers who ship directly to consumers. A queen-size mattress (typically 1600×2000×250 mm) compresses to approximately 1600×2000×100 mm, reducing volume by ~60%.
The machine integrates an motorized infeed system to deliver finished mattresses, twin heated compression rollers that progressively squeeze the mattress as it passes through, a polyethylene film feeding system that wraps the compressed roll, and a thermal sealing head that heat-seals the film overlap. An outfeed conveyor discharges the finished wrapped roll for palletizing and shipment.
How it works
Finished mattresses (post-tufting and edge-binding) arrive on the infeed conveyor at approximately 1.5 m/min. The conveyor drive rollers transport the mattress toward the compression roller nip. The machine operator (or upstream PLC) signals the control system with mattress dimensions (length, width, thickness) so the system can calculate required compression ratio and film length.
The twin compression rollers (typically 300–400 mm diameter, 1500 mm face width) rotate toward each other, creating a converging nip. The upper roller is heated internally via steam or electric cartridge heaters, maintaining 60–80°C surface temperature to soften the foam and improve compressibility. The lower roller remains unheated and provides the backing force. A hydraulic ram (80 mm bore, 10–20 tons force) applies the nip pressure, which is adjustable via a fine-tuning screw to accommodate different mattress densities and target compression ratios.
The main compression motor (2 kW, 1800 rpm) drives the rollers via a 10:1 reducer and flexible coupling, outputting approximately 180 rpm to the roller shafts. A variable frequency drive (VFD) allows the operator to adjust roller speed from 50–100% of nominal (90–180 rpm), enabling slower speeds for dense foams and faster speeds for soft foams. As the mattress passes through the compression nip, the foam cell structure compresses. The mattress emerges as a compact roll, approximately 50–70% of its original thickness.
Simultaneously, the plastic film unwinding system feeds polyethylene or polypropylene film (1000–1500 mm width) from a large supply roll. The quick-change spindle holds rolls up to 1500 mm width and allows rapid changeover (typically <5 minutes). A magnetic particle brake maintains constant film tension as it unwinds, preventing slack or wrinkles. The film is guided via PTFE-coated guide rollers preventing snags. An film advance encoder on the unwinding shaft provides feedback to the PLC, synchronizing film feed speed to the roller discharge speed.
As the compressed mattress exits the roller nip, the film wraps around it in a spiral pattern. The film overlap (typically 50–100 mm) is positioned to be sealed by the thermal sealing head. The electric heating element (2 kW, embedded in the blade block) maintains a hardened steel blade at 150–200°C (regulated via a PID thermostat and {{pcb-bare}}-based solid-state relay). The pneumatic seal ram (bore 50 mm, 1000–2000 N force) is triggered by a 24 VDC solenoid valve, pressing the heated blade and a backing plate against the film overlap for 2–4 seconds. The blade heat melts the polyethylene, and the pressure creates a hermetic seal. The Teflon-coated blade prevents film sticking during retraction.
The sealed roll then transfers to the outfeed discharge conveyor, moving at approximately 1 m/min. A centrifugal cooling fan (1.5 kW EC motor) blows air across the wrapped roll, accelerating film cooling and hardening before the roll reaches the end of the conveyor. Once fully cooled (typically 1–2 minutes), the roll is manually or automatically removed for palletizing and shipping.
Control and sequencing
The PLC control system orchestrates the entire process:
- Load detection: Infeed conveyor motion triggered by operator button or upstream sensor.
- Compression start: Compression rollers accelerate to programmed speed; hydraulic ram applies preset nip force.
- Film unwinding: Film unwinding synchronized to roller discharge rate via encoder feedback.
- Seal trigger: Once film wrap is complete (detected by film advance count), seal cycle initiates: heating element is already at setpoint temperature, seal ram descends, dwell timer counts 2–4 seconds, then ram retracts.
- Cooling and discharge: Outfeed conveyor acceleration; cooling fan runs for 60–120 seconds; roll discharged at end.
- Cycle repeat: After operator clears previous roll, infeed conveyor restarts for next mattress.
Cycle time typically ranges from 6–15 minutes depending on mattress size and compression ratio.
Thermal and mechanical considerations
The upper compression roller must maintain consistent surface temperature to ensure uniform foam compression. Too cold and compression is incomplete (causing springback); too hot and the foam surface may scorch or char. Internal steam or electric heating passages provide uniform heat distribution. Regular descaling (if steam-heated) or cartridge element inspection (if electric) maintains heat transfer efficiency.
The thermal sealing blade must be kept clean of accumulated polyethylene residue. Weekly cleaning (using a soft brush and light solvent) prevents buildup, which degrades seal quality. Over-temperature (>220°C) causes yellowing of clear film and weakens the plastic; under-temperature (<140°C) creates weak seals that may split during handling.
The hydraulic pressure cylinder requires monthly fluid level checks and annual filter changes. Leakage in the cylinder rod seals reduces nip force and is detected by slow or incomplete compression.
Quality parameters
Successful roll packing requires careful control of:
- Nip force: Too low (< 10 tons) results in incomplete compression and springback; too high (> 25 tons) crushes foam permanently and creates hard spots.
- Roller temperature: Mismatched temperature between left and right roller ends causes uneven compression and roll curvature.
- Film tension: Loose film creates wrinkles and poor seal overlap; over-tension causes film tearing during wrap.
- Seal dwell time: Too short (<2 seconds) produces a partial, weak seal; too long (>6 seconds) can overheat and perforate the film.
- Blade temperature stability: Fluctuations ±10°C degrade seal consistency; PLC trending of temperature logs identifies heating element degradation early.
Modern machines log all process parameters (nip force, roller speed, film feed rate, blade temperature, seal dwell time) to memory or cloud database, enabling root-cause analysis and predictive maintenance.
Mattress Roll-Pack Machine parts and their functions
8 top-level parts · 53 parts in total · full bill of materials below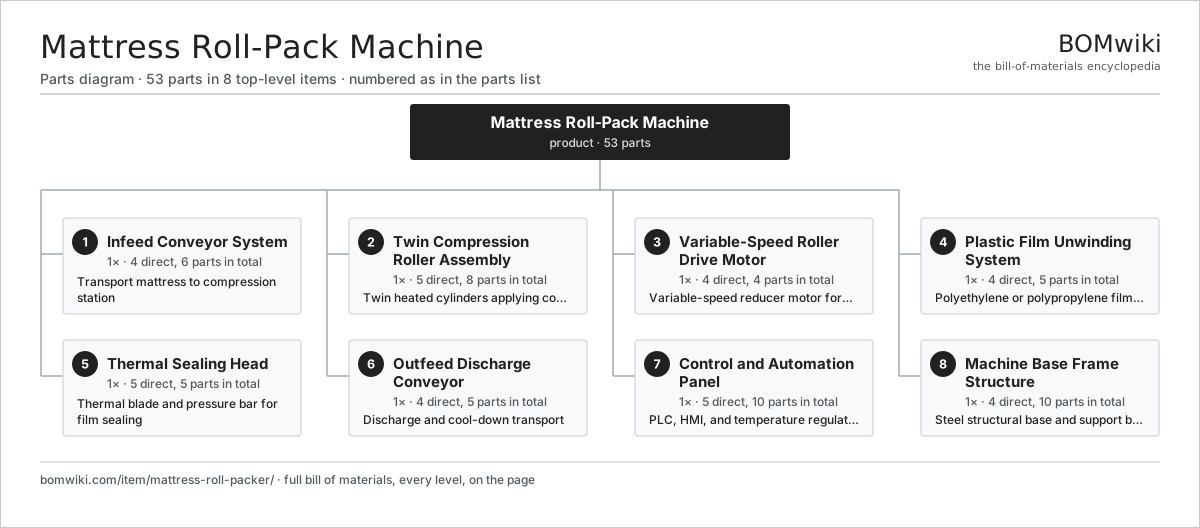
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Infeed Conveyor System 4 parts | 1× | Transport mattress to compression station |
| 2 | Twin Compression Roller Assembly 5 parts | 1× | Twin heated cylinders applying compressive force |
| 3 | Variable-Speed Roller Drive Motor 4 parts | 1× | Variable-speed reducer motor for roller rotation |
| 4 | Plastic Film Unwinding System 4 parts | 1× | Polyethylene or polypropylene film feed system |
| 5 | Thermal Sealing Head 5 parts | 1× | Thermal blade and pressure bar for film sealing |
| 6 | Outfeed Discharge Conveyor 4 parts | 1× | Discharge and cool-down transport |
| 7 | Control and Automation Panel 5 parts | 1× | PLC, HMI, and temperature regulation |
| 8 | Machine Base Frame Structure 4 parts | 1× | Steel structural base and support beams |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Mattress Roll-Pack Machine
8 top-level lines · 43 rows shown · 53 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Infeed Conveyor System 4 parts | mattress-roll-packer-infeed-conveyor | 1× | 1 | 6 | assembly |
| 1.1 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 1.2 | Infeed Conveyor Drive Motor | mattress-roll-packer-infeed-motor | 1× | 1 | · | part |
| 1.3 | Drive Roller Cylinder | mattress-roll-packer-drive-roller | 2× | 2 | · | part |
| 1.4 | Conveyor Side Guide Rail | mattress-roll-packer-guide-rail | 2× | 2 | · | part |
| 2 | Twin Compression Roller Assembly 5 parts | mattress-roll-packer-compression-rollers | 1× | 1 | 8 | assembly |
| 2.1 | Upper Compression Roller | mattress-roll-packer-upper-roller | 1× | 1 | · | part |
| 2.2 | Lower Compression Roller | mattress-roll-packer-lower-roller | 1× | 1 | · | part |
| 2.3 | Large-Bore Deep-Groove Ball Bearing | mattress-roll-packer-roller-bearing-set | 4× | 4 | · | part |
| 2.4 | Compression Pressure Hydraulic Ram | mattress-roll-packer-pressure-cylinder | 1× | 1 | · | part |
| 2.5 | Fine Compression Adjustment Screw | mattress-roll-packer-nip-adjustment | 1× | 1 | · | part |
| 3 | Variable-Speed Roller Drive Motor 4 parts | mattress-roll-packer-roller-motor | 1× | 1 | 4 | assembly |
| 3.1 | Main Compression Motor | mattress-roll-packer-ac-motor | 1× | 1 | · | part |
| 3.2 | Variable Frequency Drive | mattress-roll-packer-vfd-drive | 1× | 1 | · | part |
| 3.3 | Gearbox Speed Reducer | mattress-roll-packer-gear-reducer | 1× | 1 | · | part |
| 3.4 | Flexible Shaft Coupling | mattress-roll-packer-shaft-coupling | 1× | 1 | · | part |
| 4 | Plastic Film Unwinding System 4 parts | mattress-roll-packer-film-unwinder | 1× | 1 | 5 | assembly |
| 4.1 | Film Roll Quick-Change Spindle | mattress-roll-packer-film-spool-holder | 1× | 1 | · | part |
| 4.2 | Film Tension Magnetic Brake | mattress-roll-packer-film-tension-brake | 1× | 1 | · | part |
| 4.3 | PTFE-Coated Guide Roller | mattress-roll-packer-film-guide-roller | 2× | 2 | · | part |
| 4.4 | Encoder | encoder | 1× | 1 | · | part |
| 5 | Thermal Sealing Head 5 parts | mattress-roll-packer-sealing-head | 1× | 1 | 5 | assembly |
| 5.1 | Electric Heating Cartridge Element | mattress-roll-packer-heating-element | 1× | 1 | · | part |
| 5.2 | Hardened Thermal Sealing Blade | mattress-roll-packer-thermal-blade | 1× | 1 | · | part |
| 5.3 | RTD Temperature Probe | mattress-roll-packer-temperature-sensor | 1× | 1 | · | part |
| 5.4 | Pneumatic Seal Pressure Ram | mattress-roll-packer-pressure-bar | 1× | 1 | · | part |
| 5.5 | Sealing Cycle Solenoid Valve | mattress-roll-packer-seal-solenoid | 1× | 1 | · | part |
| 6 | Outfeed Discharge Conveyor 4 parts | mattress-roll-packer-outfeed-conveyor | 1× | 1 | 5 | assembly |
| 6.1 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 6.2 | Outfeed Conveyor Drive Motor | mattress-roll-packer-outfeed-motor | 1× | 1 | · | part |
| 6.3 | Outfeed Support Roller | mattress-roll-packer-outfeed-roller | 2× | 2 | · | part |
| 6.4 | Axial Cooling Blower Fan | mattress-roll-packer-cooling-fan | 1× | 1 | · | part |
| 7 | Control and Automation Panel 5 parts | mattress-roll-packer-control-panel | 1× | 1 | 10 | assembly |
| 7.1 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.3 | Power Supply | power-supply | 2× | 2 | · | part |
| 7.4 | Relay | relay | 5× | 5 | · | part |
| 7.5 | PID Temperature Controller | mattress-roll-packer-temp-controller | 1× | 1 | · | part |
| 8 | Machine Base Frame Structure 4 parts | mattress-roll-packer-frame | 1× | 1 | 10 | assembly |
| 8.1 | Steel I-Beam Structural Member | mattress-roll-packer-structural-beam | 4× | 4 | · | part |
| 8.2 | Full-Penetration Fillet Weld | mattress-roll-packer-weld-connection | 1× | 1 | · | part |
| 8.3 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 8.4 | Elastomer Vibration Isolation Foot | mattress-roll-packer-vibration-feet | 4× | 4 | · | part |
Something wrong in this list? Report a problem with this BOM.
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇨🇭Rieter
rieter.com ↗
|
Winterthur, CH | Spinning machinery | 10 units | 14–24 wks |
| truetzschler.com ↗ | Mönchengladbach, DE | Textile machinery | 10 units | 14–24 wks |
|
🇧🇪Picanol
picanol.be ↗
|
Ypres, BE | Weaving machines | 10 units | 14–24 wks |
| karlmayer.com ↗ | Obertshausen, DE | Warp knitting machines | 10 units | 14–24 wks |
|
🇨🇭Saurer
saurer.com ↗
|
Arbon, CH | Spinning & embroidery | 10 units | 14–24 wks |
1,248-word article