Hydraulic Pipe Bender
ProductOverview
The hydraulic pipe bender is a shop-floor tool designed to bend carbon steel, stainless, and aluminum pipes to precise radii without kinking, cracking, or over-thinning the wall. The machine uses a replaceable Male Bending Die and Female Bending Shoe forming a curved path, a Bending Hydraulic Cylinder applying bending force (10–20 tons), an internal Internal Mandrel Support preventing wall collapse, and a Pipe Clamp and Rotation Unit holding the pipe in alignment. The process conforms to ASME B4.19 (Precision Gage Blocks and Accessories) and API 5L (Line Pipe Specifications) for pipeline construction and pressure-vessel fabrication.
Pipes are bent to four common standards: 1D (one-diameter radius, tightest), 2D, 3D, and 5D (six-times-diameter radius, gentlest), with special dies available for 7D or 10D for long-sweep applications. The machine is portable (2,000 lbs) with a hydraulic pipe-bending-machine-pump-unit driven by a 5–10 hp electric motor, a SAE NG10 Directional Control Valve for proportional or manual actuation, and a Machine Frame and Base bolted to the shop floor.
How It Works
The operator loads a straight pipe into the Pipe Clamp and Rotation Unit, where fixed and moving jaws grip the pipe with a known clamping force (typically 500–1,000 psi) to prevent slipping. The Mandrel Rod is inserted into the pipe bore through the clamp end, with a Mandrel Ball Joint allowing the mandrel to swivel and follow the bend without binding.
The pump unit engages: the Hydraulic Motor Drive (5–10 hp AC induction) drives the Gear Pump Assembly (10–20 cc/rev displacement) at 1,800 rpm, delivering oil at 2,500–3,000 psi to the Directional Control Valve. When the operator actuates the control lever (or electrical solenoid), the Control Spool Valve opens a passage from pump (P) to the cap end of the Bending Hydraulic Cylinder, while simultaneously opening the rod end to tank (T).
The double-acting Bending Hydraulic Cylinder (2–4 inch bore, 12–24 inch stroke) extends, pushing the bending die against the pipe clamped between the die and the fixed shoe. As the die advances, the pipe radius decreases from infinity (straight) to the target radius (e.g., 2D = two-times-diameter). The Mandrel Rod inside the pipe expands with the bend, supporting the inner wall and preventing buckling and ovality. The pipe wall thins slightly (typical 5–15% reduction) but remains uniform.
The operator monitors the bend angle (manually via reference marks or digitally via laser/laser indicator), and when the target angle is reached, pulls the control lever to the center (neutral) position. The Control Spool Valve centers, closing both A and B ports, and the cylinder pressure holds steady, maintaining the bend. A light pull on the reverse lever (or solenoid reversal) retracts the cylinder, backing the die away and releasing the pipe.
The operator extracts the bent pipe, resets the clamp, and loads the next section. Modern machines include a Pressure Compensator that maintains a constant differential pressure across the spool, improving repeatability and reducing cycle time variation with pipe size.
Die and Mandrel Selection
Different pipe sizes and radii require different dies and mandrels. A typical machine kit includes dies for four radii (1D, 2D, 3D, 5D) across five pipe sizes (1", 1.5", 2", 3", 4"), totaling 20 Male Bending Die and Female Bending Shoe pairs, and matching Mandrel Rod sections. Changing a die requires unbolting the Main Frame Structure, aligning the new die and shoe on the Cylinder Barrel, and securing with Die Retaining Pin (spring-loaded dowels that lock the die position).
The mandrel is hand-fed into the pipe clamp; for best results, the mandrel tip is coated with a thin soap or PTFE grease to reduce friction as the pipe radius tightens. For very tight 1D bends, some operators insert a small ball-bearing mandrel follower at the exit of the clamp to further support the inner radius.
Wall Thickness and Material Limits
The bending capacity of a pipe depends on material, wall thickness, and diameter. A rule of thumb: minimum radius = 2–3 times the bend stiffness (EI / applied load). Thin-walled tubing (0.035–0.065 inch wall) can achieve 1D bends at small diameters (under 2 inches) without mandrel, but requires one for larger or thicker pipe. Stainless steel (higher yield strength) is more prone to cracking in tight radii than mild steel; copper and aluminum are gentler. The machine relief valve is set to prevent overpressure: at 3,000 psi, it stops the bend and vents excess flow, protecting the Bending Hydraulic Cylinder and Hydraulic Hose Assemblies.
Maintenance
The Return Filter Assembly spin-on element is replaced every 500–1,000 operating hours to maintain cleanliness and protect the Proportional Solenoid Coil and spool clearances. The hydraulic oil (ISO VG 46) is sampled annually for moisture and particulate; the Hydraulic Reservoir Tank is drained and refilled every 2,000 hours. The Cylinder Seal Kit are replaced if the cylinder develops internal leakage (slow drift of the pipe during a bend hold). The Clamp Piston Seals and Clamp Block Assembly are inspected for erosion from repeated jaw cycling; clamp jaws are re-hardened or replaced every 10,000 bends. The Cylinder Guide Rails are wiped clean of hydraulic mist and checked for alignment annually.
Hydraulic Pipe Bender parts and their functions
8 top-level parts · 49 parts in total · full bill of materials below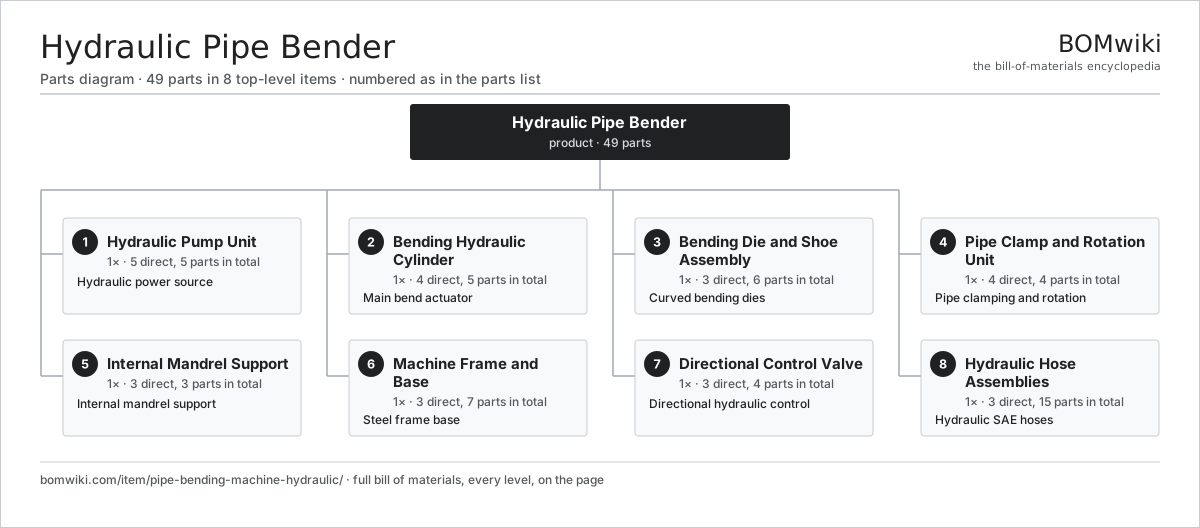
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Hydraulic Pump Unit 5 parts | 1× | Hydraulic power source |
| 2 | Bending Hydraulic Cylinder 4 parts | 1× | Main bend actuator |
| 3 | Bending Die and Shoe Assembly 3 parts | 1× | Curved bending dies |
| 4 | Pipe Clamp and Rotation Unit 4 parts | 1× | Pipe clamping and rotation |
| 5 | Internal Mandrel Support 3 parts | 1× | Internal mandrel support |
| 6 | Machine Frame and Base 3 parts | 1× | Steel frame base |
| 7 | Directional Control Valve 3 parts | 1× | Directional hydraulic control |
| 8 | Hydraulic Hose Assemblies 3 parts | 1× | Hydraulic SAE hoses |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Hydraulic Pipe Bender
8 top-level lines · 36 rows shown · 49 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Hydraulic Pump Unit 5 parts | pipe-bending-machine-hydraulic-pump-unit | 1× | 1 | 5 | assembly |
| 1.1 | Hydraulic Motor Drive | pipe-bending-machine-hydraulic-motor | 1× | 1 | · | part |
| 1.2 | Gear Pump Assembly | pipe-bending-machine-hydraulic-pump | 1× | 1 | · | part |
| 1.3 | Main Relief Valve | pipe-bending-machine-pump-relief-valve | 1× | 1 | · | part |
| 1.4 | Return Filter Assembly | pipe-bending-machine-pump-filter | 1× | 1 | · | part |
| 1.5 | Hydraulic Reservoir Tank | pipe-bending-machine-pump-reservoir | 1× | 1 | · | part |
| 2 | Bending Hydraulic Cylinder 4 parts | pipe-bending-machine-hydraulic-cylinder | 1× | 1 | 5 | assembly |
| 2.1 | Cylinder Tie Rod | pipe-bending-machine-cylinder-rod | 1× | 1 | · | part |
| 2.2 | Cylinder Barrel | pipe-bending-machine-cylinder-barrel | 1× | 1 | · | part |
| 2.3 | Cylinder Seal Kit | pipe-bending-machine-cylinder-seals | 1× | 1 | · | part |
| 2.4 | SAE Cylinder End Caps | pipe-bending-machine-cylinder-ports | 2× | 2 | · | part |
| 3 | Bending Die and Shoe Assembly 3 parts | pipe-bending-machine-bending-die-set | 1× | 1 | 6 | assembly |
| 3.1 | Male Bending Die | pipe-bending-machine-bending-die | 1× | 1 | · | part |
| 3.2 | Female Bending Shoe | pipe-bending-machine-bending-shoe | 1× | 1 | · | part |
| 3.3 | Die Retaining Pin | pipe-bending-machine-die-clamp-pins | 4× | 4 | · | part |
| 4 | Pipe Clamp and Rotation Unit 4 parts | pipe-bending-machine-clamp-assembly | 1× | 1 | 4 | assembly |
| 4.1 | Fixed Clamp Jaw | pipe-bending-machine-clamp-jaw-fixed | 1× | 1 | · | part |
| 4.2 | Moving Clamp Jaw | pipe-bending-machine-clamp-jaw-moving | 1× | 1 | · | part |
| 4.3 | Clamp Block Assembly | pipe-bending-machine-clamp-block | 1× | 1 | · | part |
| 4.4 | Clamp Piston Seals | pipe-bending-machine-clamp-seal-kit | 1× | 1 | · | part |
| 5 | Internal Mandrel Support 3 parts | pipe-bending-machine-mandrel-assembly | 1× | 1 | 3 | assembly |
| 5.1 | Mandrel Rod | pipe-bending-machine-mandrel-rod | 1× | 1 | · | part |
| 5.2 | Mandrel Ball Joint | pipe-bending-machine-mandrel-ball-joint | 1× | 1 | · | part |
| 5.3 | Mandrel Retaining Collar | pipe-bending-machine-mandrel-keeper | 1× | 1 | · | part |
| 6 | Machine Frame and Base 3 parts | pipe-bending-machine-frame | 1× | 1 | 7 | assembly |
| 6.1 | Main Frame Structure | pipe-bending-machine-frame-main | 1× | 1 | · | part |
| 6.2 | Leveling Feet | pipe-bending-machine-frame-base-feet | 4× | 4 | · | part |
| 6.3 | Cylinder Guide Rails | pipe-bending-machine-frame-guide-rails | 2× | 2 | · | part |
| 7 | Directional Control Valve 3 parts | pipe-bending-machine-control-valve | 1× | 1 | 4 | assembly |
| 7.1 | Control Spool Valve | pipe-bending-machine-control-spool | 1× | 1 | · | part |
| 7.2 | Proportional Solenoid Coil | pipe-bending-machine-control-solenoids | 2× | 2 | · | part |
| 7.3 | Pressure Compensator | pipe-bending-machine-control-pressure-compensator | 1× | 1 | · | part |
| 8 | Hydraulic Hose Assemblies 3 parts | pipe-bending-machine-hose-bundle | 1× | 1 | 15 | assembly |
| 8.1 | High-Pressure Hose | pipe-bending-machine-hose-pressure | 2× | 2 | · | part |
| 8.2 | Return Hose | pipe-bending-machine-hose-return | 1× | 1 | · | part |
| 8.3 | Hose Clamp and Support | pipe-bending-machine-hose-clamps | 12× | 12 | · | part |
Something wrong in this list? Report a problem with this BOM.
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $15k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| caterpillar.com ↗ | Irving, US | Construction & mining equipment | made to order | 16–28 wks |
|
🇯🇵Komatsu
komatsu.com ↗
|
Tokyo, JP | Construction & mining equipment | made to order | 16–28 wks |
|
🇸🇪Volvo CE
volvoce.com ↗
|
Gothenburg, SE | Construction equipment | made to order | 16–28 wks |
|
🇨🇭Liebherr
liebherr.com ↗
|
Bulle, CH | Cranes & heavy equipment | made to order | 16–28 wks |
|
🇨🇳XCMG
xcmg.com ↗
|
Xuzhou, CN | Construction machinery | made to order | 16–28 wks |
961-word article