Pocket Spring Assembler
ProductOverview
The pocket spring assembler is a specialized production line for mattress and upholstered furniture manufacturing, encapsulating individual steel coil springs in individual fabric pockets and bonding rows together via ultrasonic welding and hot-melt adhesive. This process creates the "pocketed spring core" found in premium mattresses, offering superior motion isolation compared to open-coil construction. Each spring is independently supported, reducing vibration transfer across the mattress surface.
The line integrates multiple sub-systems: a spring infeed hopper, a pneumatic singulator arm that picks individual springs, a nonwoven unwinding system, a heat-sealing station that envelops each spring, an ultrasonic welder bonding pocket seams, a hot-melt adhesive dispenser, a heated lamination press for row bonding, and a accumulation conveyor for cooling and outfeed. A central PLC control system orchestrates timing, temperature, and motion across all stations.
Production volumes typically reach 50–100 spring rows per minute, depending on spring size and pocket pitch. Rolls of nonwoven PET (polyethylene terephthalate) fabric are unwound continuously as the picker arm places each spring onto the advancing fabric web.
How it works
The process begins with springs pre-sorted into a gravity hopper. An electromagnetic vibrator on the hopper base agitates and advances springs into a linear chute. A pneumatic slide gate meters the flow to prevent jams.
The pneumatic picker arm (typically 5–6 axes) detects individual springs via an inductive proximity sensor and vacuum-picks them using a suction cup gripper. The arm accelerates under proportional valve control to avoid spring deformation, then precisely places each spring onto the advancing nonwoven web.
The nonwoven feed system consists of a large roll holder unwinding polyester or polyethylene nonwoven (typically 150–300 g/m² weight) under constant tension maintained by a magnetic particle brake. An advance sensor triggers the heated forming press whenever a spring reaches the sealing station, synchronizing fabric advance with spring placement.
The heat-sealing jaw consists of an aluminum or ductile iron block containing two cartridge heaters (1 kW total) maintaining 130–160°C. The jaw descends via a pneumatic cylinder (1500–2000 N load), folding the fabric around the spring and thermally bonding the edges together. The bond strength depends on time (2–5 seconds dwell), temperature precision (PID-controlled ±5°C via a thermostat), and fabric properties. After the first pocket is sealed, the singulator picks the next spring while fabric advances; this overlapping operation maintains line throughput.
Once a row of 50–100 pockets is complete, the fabricated web transfers to the ultrasonic sealing station. Here, a high-frequency 40 kHz generator (3 kW) drives a titanium horn vibrating at 10–50 micrometers amplitude. The horn presses down onto the pocket seams via a pneumatic clamping cylinder (3000–5000 N). The ultrasonic energy melts and fuses the polyester fibers at the interface without adhesive, creating a waterproof molecular bond between adjacent pockets. The backing anvil provides counter-pressure, improving weld uniformity.
For rows destined to be stacked into a multi-layer core, the hot-melt adhesive system applies edge beads between rows. A heated tank maintains hot-melt polyurethane or EVA adhesive at 160–180°C with an agitator paddle. A peristaltic pump meters adhesive to multiple servo-controlled solenoid nozzles positioned along the row edges. Each nozzle opens only during a programmed dwell, depositing adhesive bead at precise locations. Insulated hose assemblies with integrated thermostats maintain adhesive temperature throughout the feed path, preventing solidification.
After adhesive application, completed rows enter the lamination press station. Twin heated cartridge heater arrays in the upper and lower aluminum and steel platens reach 180°C. A large air cylinder (80 mm bore, ~4 tons force) clamps the assembly for 15–30 seconds while adhesive cures. Temperature is precisely regulated via PLC feedback from RTD probes embedded in both platens, ensuring uniform cure across the laminate and preventing thermal runaway or undercure.
Post-press, the completed rows transfer to an accumulation conveyor powered by a 2 kW variable-frequency motor. Rows move at 2–10 m/min, allowing residual heat to dissipate and adhesive to fully cure. Pneumatic accumulation gates create intermediate buffer zones to smooth production rhythm and decouple the assembler from downstream mattress-assembly equipment like the tape edge unit or tufting frame.
Integration and control
The entire line is orchestrated by a centralized PLC running a state-machine algorithm. Operators program row length (number of pockets), spring type (diameter, height, material), nonwoven weight, and adhesive brand via an HMI touchscreen. The PLC calculates fabric advance distance per spring, heating ramp profiles, ultrasonic weld dwell time, and press cycle duration, then automatically controls all solenoid and heating relays. Production counters, temperature logs, and fault diagnostics are displayed real-time.
Changeovers between spring sizes or pocket densities typically require only parameter updates and possibly a new fabric roll. If spring diameter shifts significantly, the picker arm vacuum cup may need adjustment, but in most modern systems this is automated via proportional solenoid calibration.
Quality and maintenance
Pocket spring quality hinges on consistent spring placement, precise pocket seal temperature, and adequate ultrasonic weld energy. Poor vacuum cup condition leads to spring misalignment, visible as off-center bulges in the finished row. Under-temperature in the heat-sealing jaw results in weak fabric bonds and potential pocket rupture during subsequent pressing. Over-temperature causes fabric yellowing and brittleness. Ultrasonic horn face wear (>0.5 mm deformation) produces inconsistent welds and is detected by progressive decline in weld strength; horn replacement is a field service task.
Hot-melt adhesive batches must match the specified cure profile and viscosity; incompatible adhesive brands risk poor layer adhesion or delamination during mattress shipping and use. Regular tank cleaning (typically weekly on continuous runs) prevents charred residue buildup, which reduces heat transfer and increases cycle time.
Pocket Spring Assembler parts and their functions
9 top-level parts · 53 parts in total · full bill of materials below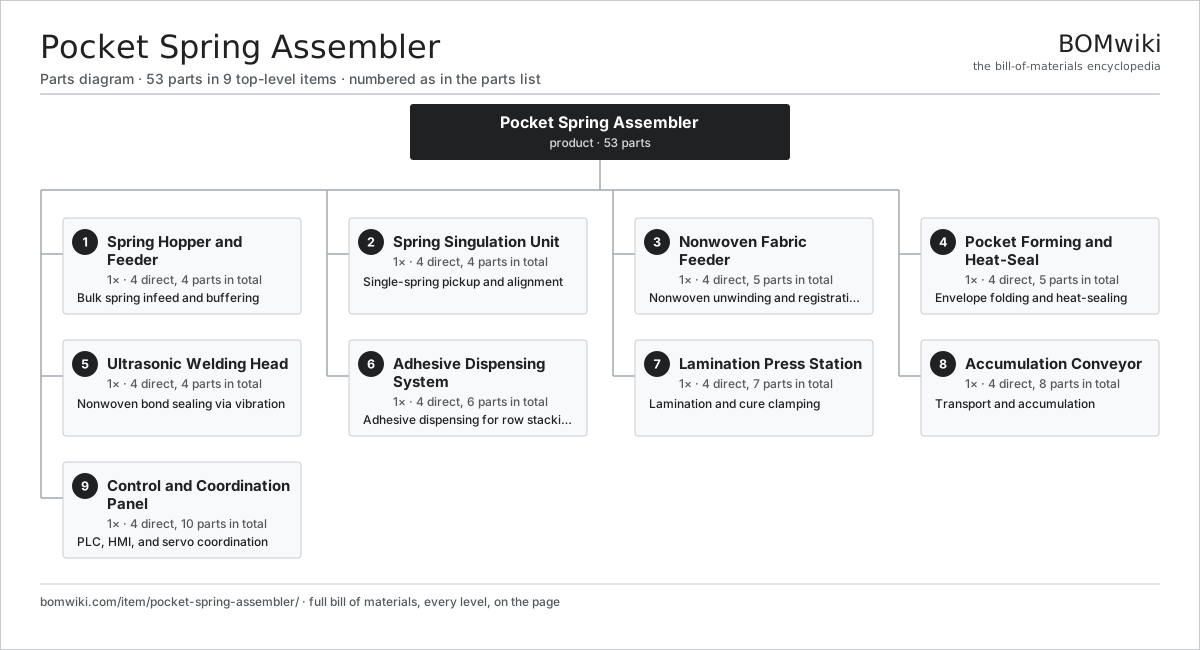
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Spring Hopper and Feeder 4 parts | 1× | Bulk spring infeed and buffering |
| 2 | Spring Singulation Unit 4 parts | 1× | Single-spring pickup and alignment |
| 3 | Nonwoven Fabric Feeder 4 parts | 1× | Nonwoven unwinding and registration |
| 4 | Pocket Forming and Heat-Seal 4 parts | 1× | Envelope folding and heat-sealing |
| 5 | Ultrasonic Welding Head 4 parts | 1× | Nonwoven bond sealing via vibration |
| 6 | Adhesive Dispensing System 4 parts | 1× | Adhesive dispensing for row stacking |
| 7 | Lamination Press Station 4 parts | 1× | Lamination and cure clamping |
| 8 | Accumulation Conveyor 4 parts | 1× | Transport and accumulation |
| 9 | Control and Coordination Panel 4 parts | 1× | PLC, HMI, and servo coordination |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Pocket Spring Assembler
9 top-level lines · 45 rows shown · 53 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Spring Hopper and Feeder 4 parts | pocket-spring-assembler-hopper | 1× | 1 | 4 | assembly |
| 1.1 | Steel Hopper Bin | pocket-spring-assembler-hopper-bin | 1× | 1 | · | part |
| 1.2 | Electromagnetic Vibrator | pocket-spring-assembler-vibration-motor | 1× | 1 | · | part |
| 1.3 | Pneumatic Slide Gate | pocket-spring-assembler-diverter-gate | 1× | 1 | · | part |
| 1.4 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Spring Singulation Unit 4 parts | pocket-spring-assembler-singulator | 1× | 1 | 4 | assembly |
| 2.1 | Multi-Axis Pneumatic Robot | pocket-spring-assembler-picker-arm | 1× | 1 | · | part |
| 2.2 | Suction Cup Gripper | pocket-spring-assembler-vacuum-cup | 1× | 1 | · | part |
| 2.3 | Inductive Proximity Sensor | pocket-spring-assembler-proximity-sensor | 1× | 1 | · | part |
| 2.4 | Proportional Directional Solenoid Valve | pocket-spring-assembler-pilot-valve | 1× | 1 | · | part |
| 3 | Nonwoven Fabric Feeder 4 parts | pocket-spring-assembler-fabric-feed | 1× | 1 | 5 | assembly |
| 3.1 | Large Fabric Roll Holder | pocket-spring-assembler-fabric-spool | 1× | 1 | · | part |
| 3.2 | Magnetic Particle Brake | pocket-spring-assembler-tension-brake | 1× | 1 | · | part |
| 3.3 | PTFE-Faced Guide Cylinder | pocket-spring-assembler-guide-rollers | 2× | 2 | · | part |
| 3.4 | Encoder | encoder | 1× | 1 | · | part |
| 4 | Pocket Forming and Heat-Seal 4 parts | pocket-spring-assembler-pocket-forming | 1× | 1 | 5 | assembly |
| 4.1 | Heating Element | heating-element | 2× | 2 | · | part |
| 4.2 | Heated Forming Press Jaw | pocket-spring-assembler-press-jaw | 1× | 1 | · | part |
| 4.3 | PID Thermostatic Controller | pocket-spring-assembler-temperature-control | 1× | 1 | · | part |
| 4.4 | Pneumatic Forming Clamp Cylinder | pocket-spring-assembler-pneumatic-clamp | 1× | 1 | · | part |
| 5 | Ultrasonic Welding Head 4 parts | pocket-spring-assembler-ultrasonic-sealer | 1× | 1 | 4 | assembly |
| 5.1 | 40 kHz Ultrasonic Power Unit | pocket-spring-assembler-ultrasonic-generator | 1× | 1 | · | part |
| 5.2 | Titanium Ultrasonic Horn | pocket-spring-assembler-horn | 1× | 1 | · | part |
| 5.3 | Ultrasonic Anvil Backing Plate | pocket-spring-assembler-anvil | 1× | 1 | · | part |
| 5.4 | Pneumatic Boost Clamping Ram | pocket-spring-assembler-boost-ram | 1× | 1 | · | part |
| 6 | Adhesive Dispensing System 4 parts | pocket-spring-assembler-glue-system | 1× | 1 | 6 | assembly |
| 6.1 | Hot-Melt Adhesive Melter | pocket-spring-assembler-melter-tank | 1× | 1 | · | part |
| 6.2 | Peristaltic Adhesive Pump | pocket-spring-assembler-glue-pump | 1× | 1 | · | part |
| 6.3 | Servo-Controlled Hot-Melt Nozzle | pocket-spring-assembler-spray-nozzle | 3× | 3 | · | part |
| 6.4 | Insulated Adhesive Hose Assy | pocket-spring-assembler-hose-assembly | 1× | 1 | · | part |
| 7 | Lamination Press Station 4 parts | pocket-spring-assembler-press-station | 1× | 1 | 7 | assembly |
| 7.1 | Heating Element | heating-element | 4× | 4 | · | part |
| 7.2 | Upper Press Heating Platen | pocket-spring-assembler-press-top-platen | 1× | 1 | · | part |
| 7.3 | Lower Press Steel Platen | pocket-spring-assembler-press-bottom-platen | 1× | 1 | · | part |
| 7.4 | Vertical Lamination Clamp Cylinder | pocket-spring-assembler-press-clamping-cylinder | 1× | 1 | · | part |
| 8 | Accumulation Conveyor 4 parts | pocket-spring-assembler-conveyor | 1× | 1 | 8 | assembly |
| 8.1 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 8.2 | Conveyor Drive Motor | pocket-spring-assembler-conveyor-motor | 1× | 1 | · | part |
| 8.3 | Sealed Bearing Drive Roller | pocket-spring-assembler-roller | 4× | 4 | · | part |
| 8.4 | Pneumatic Accumulation Gate | pocket-spring-assembler-buffer-gates | 2× | 2 | · | part |
| 9 | Control and Coordination Panel 4 parts | pocket-spring-assembler-control-panel | 1× | 1 | 10 | assembly |
| 9.1 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 9.3 | Relay | relay | 6× | 6 | · | part |
| 9.4 | Power Supply | power-supply | 2× | 2 | · | part |
Something wrong in this list? Report a problem with this BOM.
Related products
same domain, ranked by shared parts Automatic Fabric Cutting Machine
1,695 parts · shares 1 with this page
 Digital Textile Printer
1,093 parts · shares 1 with this page
DTY Texturing Machine
118 parts · shares 1 with this page
Fabric Coating Machine
316 parts · shares 1 with this page
FDY Filament Spinning Line
679 parts · shares 1 with this page
Garment Fusing Press
93 parts · shares 1 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇨🇭Rieter
rieter.com ↗
|
Winterthur, CH | Spinning machinery | 10 units | 14–24 wks |
| truetzschler.com ↗ | Mönchengladbach, DE | Textile machinery | 10 units | 14–24 wks |
|
🇧🇪Picanol
picanol.be ↗
|
Ypres, BE | Weaving machines | 10 units | 14–24 wks |
| karlmayer.com ↗ | Obertshausen, DE | Warp knitting machines | 10 units | 14–24 wks |
|
🇨🇭Saurer
saurer.com ↗
|
Arbon, CH | Spinning & embroidery | 10 units | 14–24 wks |
1,198-word article