Retarder Proofer
ProductOverview
A retarder-proofer is a climate-controlled cabinet that manages fermentation in bakery production. It combines refrigeration (for slow fermentation/retarding) and heating (for final proofing) with precise humidity control, allowing bakers to store shaped doughs overnight and accelerate fermentation at will.
The core advantage is production flexibility. A baker can prepare shaped doughs in the evening, load them into the retarder at 3–8°C overnight (slowing fermentation to a crawl), and bake them fresh the next morning. Alternatively, the same cabinet can rapidly proof doughs at 28–32°C with 80%+ RH before oven loading. This decouples the baker's production schedule from fermentation kinetics.
Retarder-proofers are standard in artisan and commercial bakeries, with capacities ranging from 200 L (small shop, 2–3 racks) to 600 L (high-volume, 10–16 racks). Large operations may have multiple units dedicated to different product lines.
Retarding (Cold Fermentation)
The Refrigeration Unit system cools the cabinet to 2–10°C by circulating refrigerant through the Evaporator Coil inside the chamber. At this temperature, yeast and bacterial metabolism slow dramatically: fermentation that would take 2 hours at 27°C stretches to 12–18 hours at 4°C.
The Refrigeration Compressor is a semi-hermetic reciprocating unit running at 1200–1500 rpm, delivering ~1–2 tons of refrigeration. The Condenser Coil rejects heat to ambient air. The Expansion Valve meters refrigerant, maintaining evaporator temperatures at -2 to +4°C while the Temperature Sensor feeds feedback to the Control System.
Proofing (Warm, Humid Fermentation)
For final proof, the retarder switches to heating mode. The Heating System activates electric Heating Elements (1–2 kW each), warming the chamber to 28–32°C. Simultaneously, the Humidity Control system raises humidity via the Steam Generator, aiming for 75–85% RH. The Humidity Sensor provides closed-loop control.
A typical proof cycle runs 45–90 minutes at 28–32°C with 80%+ RH. The dough rises visibly (20–40% volume increase), and the baker can observe through the door window to judge readiness for oven loading.
Control & Programmability
The PLC Controller is the operational heart. It manages:
- Temperature setpoint (stored program or real-time dial input).
- Humidity setpoint (triggered when humidity falls below target; steam injection maintains level).
- Cycle timing (for automated transitions, e.g., retard at 8°C for 14 hours, then proof at 28°C for 60 minutes).
- Alarms (temperature overshoot, sensor failure, door open too long).
The Touchscreen Interface displays real-time temp/humidity, allows program selection, and logs cycle history. Most commercial units support 10–20 stored recipes, each with custom ramps and holds.
Uniform Environment
The Circulation Fan runs continuously at low speed (500–1500 rpm), ensuring temperature and humidity do not stratify. Without circulation, the top shelves could be 2–3°C warmer than the bottom, causing uneven proofing. The fan homogenizes the chamber, keeping all Removable Racks within ±1°C.
Condensation & Drain Management
Cold retarding causes condensation: when warm dough is introduced into a cold cabinet, or when the door opens and warm air enters, moisture condenses on the Evaporator Coil. The Drain Pan collects this liquid, which is drained periodically via a solenoid valve. Excessive condensation pooling can cause dripping onto dough, so regular drain checks are essential.
Racks & Load Path
The Rack System uses ball-bearing Rack Rails (heavy-duty linear slides) allowing full pull-out of loaded racks (8–16 Removable Racks per cabinet). Each rack typically holds 8–16 standard baking trays (60×40 cm) with a total load of 50–100 kg. The rails can sustain 50 kg per corner, providing safety margin.
Insulation & Efficiency
The Insulation Assembly comprises 50–100 mm polyurethane foam core sandwiched between inner (stainless-steel) and outer (epoxy-painted steel) skins. The Door Gasket (magnetic or compression style) and Thermal Break minimize air and thermal leakage. Well-insulated cabinets can hold ±1°C setpoint indefinitely without energy loss.
Energy consumption is typically 2–4 kW·h per 8-hour retarding cycle, and 1–2 kW·h per 60-minute proof cycle (because heating and small fan loads are minimal compared to refrigeration).
Maintenance
The Refrigeration Compressor should be serviced annually (oil level, vibration check). The Door Gasket should be inspected quarterly; a degraded gasket causes temperature creep and energy waste. The Evaporator Coil accumulates ice during retarding; a defrost cycle (heating the coil while the compressor is off) runs automatically every 4–6 hours to shed ice buildup.
Most cabinets require annual EPA-licensed HVAC service for refrigerant charge verification and system leak check.
Workflow Integration
A typical overnight retarding workflow:
- 7 PM: Shape doughs; load into racks; insert into retarder at 8°C.
- 8 PM – 6 AM: Cabinet holds at cold temperature; fermentation slows to near-stop.
- 5:30 AM: Baker switches controller to proofing program (28°C, 80% RH, 60 min).
- 6:30 AM: Doughs have proofed at warm temperature; ready to load into deck oven.
- 7:00 AM – noon: Bake and cool.
This schedule is impossible without a retarder-proofer, because hand-shaping at 5 PM and baking by 7 AM leaves no time for fermentation unless doughs are pre-fermented or bulk fermented overnight (less flavor, less flexibility).
Retarder Proofer parts and their functions
8 top-level parts · 35 parts in total · full bill of materials below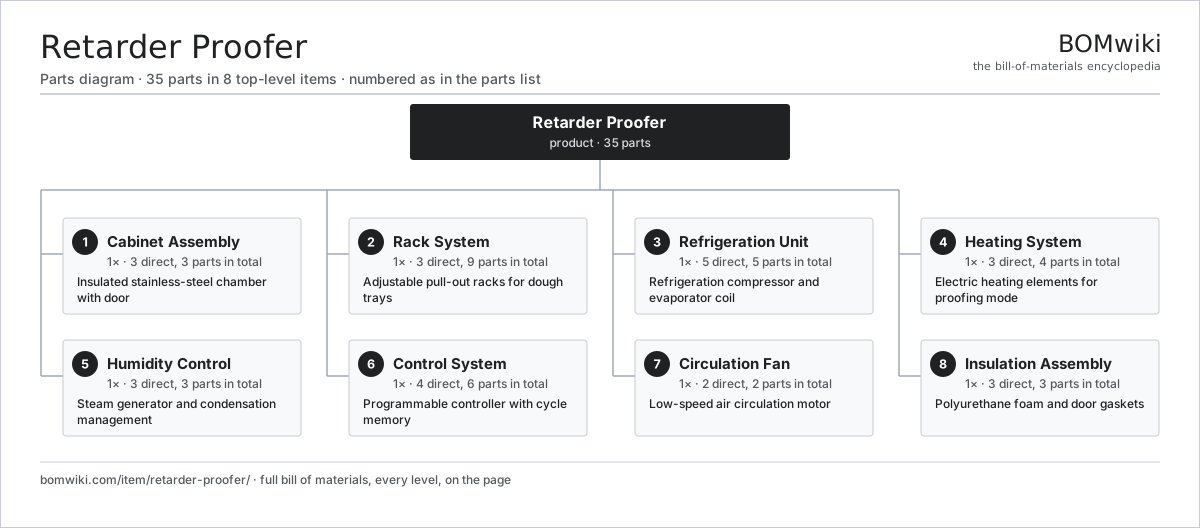
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Cabinet Assembly 3 parts | 1× | Insulated stainless-steel chamber with door |
| 2 | Rack System 3 parts | 1× | Adjustable pull-out racks for dough trays |
| 3 | Refrigeration Unit 5 parts | 1× | Refrigeration compressor and evaporator coil |
| 4 | Heating System 3 parts | 1× | Electric heating elements for proofing mode |
| 5 | Humidity Control 3 parts | 1× | Steam generator and condensation management |
| 6 | Control System 4 parts | 1× | Programmable controller with cycle memory |
| 7 | Circulation Fan 2 parts | 1× | Low-speed air circulation motor |
| 8 | Insulation Assembly 3 parts | 1× | Polyurethane foam and door gaskets |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Retarder Proofer
8 top-level lines · 34 rows shown · 35 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Cabinet Assembly 3 parts | retarder-proofer-cabinet | 1× | 1 | 3 | assembly |
| 1.1 | Cabinet Shell | retarder-proofer-cabinet-shell | 1× | 1 | · | part |
| 1.2 | Door Assembly | retarder-proofer-door-assembly | 1× | 1 | · | part |
| 1.3 | Interior Shelves | retarder-proofer-interior-shelves | 1× | 1 | · | part |
| 2 | Rack System 3 parts | retarder-proofer-rack-system | 1× | 1 | 9 | assembly |
| 2.1 | Rack Rails | retarder-proofer-rack-rails | 4× | 4 | · | part |
| 2.2 | Removable Racks | retarder-proofer-racks | 1× | 1 | · | part |
| 2.3 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 3 | Refrigeration Unit 5 parts | retarder-proofer-refrigeration | 1× | 1 | 5 | assembly |
| 3.1 | Refrigeration Compressor | retarder-proofer-compressor | 1× | 1 | · | part |
| 3.2 | Condenser Coil | retarder-proofer-condenser-coil | 1× | 1 | · | part |
| 3.3 | Evaporator Coil | retarder-proofer-evaporator-coil | 1× | 1 | · | part |
| 3.4 | Expansion Valve | retarder-proofer-expansion-valve | 1× | 1 | · | part |
| 3.5 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 4 | Heating System 3 parts | retarder-proofer-heating-system | 1× | 1 | 4 | assembly |
| 4.1 | Heating Element | retarder-proofer-heating-element | 2× | 2 | · | part |
| 4.2 | Heating Thermostat | retarder-proofer-heating-thermostat | 1× | 1 | · | part |
| 4.3 | Relay | relay | 1× | 1 | · | part |
| 5 | Humidity Control 3 parts | retarder-proofer-humidity-control | 1× | 1 | 3 | assembly |
| 5.1 | Steam Generator | retarder-proofer-steam-generator | 1× | 1 | · | part |
| 5.2 | Humidity Sensor | retarder-proofer-humidity-sensor | 1× | 1 | · | part |
| 5.3 | Drain Pan | retarder-proofer-drain-pan | 1× | 1 | · | part |
| 6 | Control System 4 parts | retarder-proofer-control-system | 1× | 1 | 6 | assembly |
| 6.1 | PLC Controller | retarder-proofer-plc-controller | 1× | 1 | · | part |
| 6.2 | Touchscreen Interface | retarder-proofer-touchscreen | 1× | 1 | · | part |
| 6.3 | Temperature Sensor | retarder-proofer-temperature-sensor | 1× | 1 | · | part |
| 6.4 | Relay | relay | 3× | 3 | · | part |
| 7 | Circulation Fan 2 parts | retarder-proofer-circulation-fan | 1× | 1 | 2 | assembly |
| 7.1 | Fan Motor | retarder-proofer-fan-motor | 1× | 1 | · | part |
| 7.2 | Fan Blade | retarder-proofer-fan-blade | 1× | 1 | · | part |
| 8 | Insulation Assembly 3 parts | retarder-proofer-insulation | 1× | 1 | 3 | assembly |
| 8.1 | Insulation Foam | retarder-proofer-insulation-foam | 1× | 1 | · | part |
| 8.2 | Door Gasket | retarder-proofer-door-gasket | 1× | 1 | · | part |
| 8.3 | Thermal Break | retarder-proofer-thermal-break | 1× | 1 | · | part |
Something wrong in this list? Report a problem with this BOM.
Related products
same domain, ranked by shared parts Automatic Espresso Tamper
45 parts · shares 1 with this page
Automatic Filleting Machine
73 parts · shares 1 with this page
 Bakery Deck Oven
44 parts · shares 1 with this page
Batter and Breading Line
127 parts · shares 1 with this page
Beverage Carbonator
95 parts · shares 1 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $1k–$500k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| gea.com ↗ | Düsseldorf, DE | Process technology | 20 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 20 units | 12–20 wks |
| tetrapak.com ↗ | Pully, CH | Food packaging & processing | 20 units | 12–20 wks |
| jbtc.com ↗ | Chicago, US | Food processing equipment | 20 units | 12–20 wks |
| alfalaval.com ↗ | Lund, SE | Heat transfer & separation | 20 units | 12–20 wks |
920-word article