Underfloor Wheel Lathe
ProductOverview
An underfloor wheel lathe is a specialized machine tool installed in a maintenance pit beneath freight or passenger cars for in-place wheel restoration. When a railway wheel develops a flat (spot), lost roundness, or rim damage from sliding, the wheel can no longer ride smoothly and creates a harsh shock at each rotation, accelerating bearing wear and creating noise. Rather than removing the wheel (a labor-intensive process requiring axle extraction), a wheel lathe restores roundness by spinning the wheel in place using friction rollers and cutting away the damaged outer rim with a carbide tool, shaving up to 3–5 mm per pass. Within 15–30 minutes, a flat wheel becomes round again and fit for continued service.
The Cutting Spindle Motor is the cutting head, a high-speed rotating Spindle Motor (15–30 kW) fitted with a precision Carbide/Diamond Bit (tungsten carbide or polycrystalline diamond) that removes damaged material. The Friction Drive Roller units, two independent motor-driven rubber rollers, grip the wheel periphery and rotate it at a steady 50–100 RPM during cutting. The Vertical Lifting Carriage is a motorized vertical drive positioning the spindle at precisely the wheel center-line height; an Wheel Profile Measuring System with a laser sensor continuously measures wheel diameter during rotation, feeding back data to the Operator Control Console so the operator can dial in the exact cutting depth needed to remove all damage.
The entire machine is anchored to the pit floor via a Pit-Mounted Base Frame heavy enough to resist the 5–10 kW cutting forces; pit-mounted machines are chosen over portable ones because cars remain stationary during maintenance, eliminating the need to reposition equipment. All safety interlocks ensure that spindle rotation is inhibited unless both friction rollers are engaged and pit gates are closed.
How it works
A worn or flat-spotted wheel car is driven into a maintenance pit on a shallow-drop or lift. The mechanic manually positions the wheel over the machine center-line, then lowers the pit gates (which trigger the Pit Gate Interlock allowing spindle start). At the Operator Control Console, the operator inputs wheel diameter (e.g., 860 mm) and the laser Wheel Profile Measuring System is zeroed by placing the laser probe at the wheel rim and jogging the Vertical Lifting Carriage until the laser distance reading stabilizes, this is the wheel's current diameter.
The operator then presses START. The Friction Drive Roller motors energize, pressing the rubber tires against the wheel rim with Hydraulic Power System pressure (typically 2–3 tonnes per roller). Friction spins the wheel at approximately 100 RPM. Simultaneously, the Spindle Motor ramps to cutting speed (1,500–2,500 RPM depending on wheel diameter and material hardness). The PLC Controller then slowly feeds the Carriage Motor downward at 20–50 mm/min, bringing the Carbide/Diamond Bit into the wheel rim.
As the cutting tool engages, sparks fly and metal chips ejected. The laser probe continuously reports wheel diameter to the PLC. Once the PLC detects that the wheel diameter has reduced by the target amount (say, 4 mm, removing all flat), the controller automatically retracts the carriage, stopping the cut. The friction rollers disengage, the wheel coasts to a stop, and the operator retrieves the car. Total time: 20–25 minutes. The restored wheel is now round and rolls smoothly.
If only one side of the wheel is damaged (a common flat-spot), the car is flipped on a Y-junction or turntable and the process repeated on the opposite side. Modern facilities have two lathes operating in parallel: one restores the leading axle while crew repositions another car at the second lathe, doubling throughput.
Design considerations
The Friction Drive Roller system is the heart of the design: rubber tire provides sufficient grip on steel rim (coefficient of friction ~0.5) to spin even a 25-tonne carriage axle at 100 RPM without slipping. The Hydraulic Power System pressure is kept at 2–4 MPa (20–40 bar) to avoid crushing wheel rim or deforming the rim web, which would require subsequent heat treatment. Roller speed and spindle speed are coupled via PLC Controller logic: as the Wheel Profile Measuring System laser detects diameter loss, the Carriage Motor automatically reduces carriage descent rate, preventing runaway cutting that would remove too much material.
The Cutting Tool Bit Assembly is a consumable: a single carbide bit cuts 5–10 wheels before flank wear (wear on the rear edge of the cutting face) exceeds tolerance and requires re-sharpening. Polycrystalline diamond (PCD) bits last 3× longer but cost 5–10× more and are reserved for high-volume facilities. The Vertical Lifting Carriage uses a ball-screw and position encoder so that multiple identical wheels are cut to within ±0.1 mm diameter, ensuring uniform rolling and minimal vibration on the track.
The Pit-Mounted Base Frame is always reinforced, sometimes with a welded base and anchor bolts into pit concrete, because the cutting load is equivalent to a 1–2 kg radial force applied 400 mm away from the machine centerline, leverage that would deflect a lighter structure unacceptably. Stiffness ensures the Wheel Profile Measuring System laser readings are accurate and repeatability is ±0.2 mm between consecutive wheels.
Underfloor Wheel Lathe parts and their functions
8 top-level parts · 62 parts in total · full bill of materials below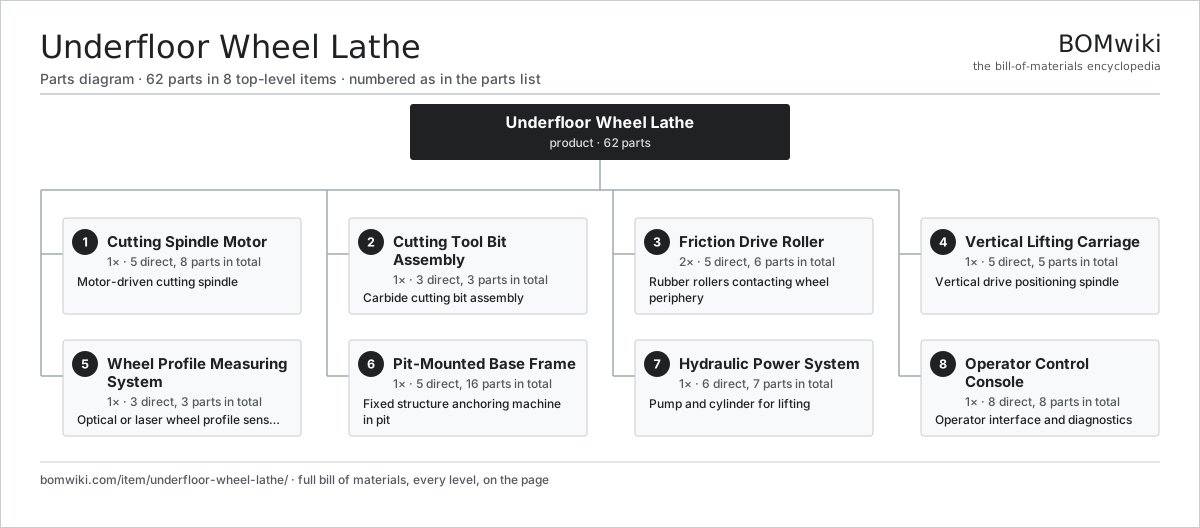
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Cutting Spindle Motor 5 parts | 1× | Motor-driven cutting spindle |
| 2 | Cutting Tool Bit Assembly 3 parts | 1× | Carbide cutting bit assembly |
| 3 | Friction Drive Roller 5 parts | 2× | Rubber rollers contacting wheel periphery |
| 4 | Vertical Lifting Carriage 5 parts | 1× | Vertical drive positioning spindle |
| 5 | Wheel Profile Measuring System 3 parts | 1× | Optical or laser wheel profile sensor |
| 6 | Pit-Mounted Base Frame 5 parts | 1× | Fixed structure anchoring machine in pit |
| 7 | Hydraulic Power System 6 parts | 1× | Pump and cylinder for lifting |
| 8 | Operator Control Console 8 parts | 1× | Operator interface and diagnostics |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Underfloor Wheel Lathe
8 top-level lines · 48 rows shown · 62 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Cutting Spindle Motor 5 parts | underfloor-wheel-lathe-spindle-unit | 1× | 1 | 8 | assembly |
| 1.1 | Spindle Motor | underfloor-wheel-lathe-spindle-motor | 1× | 1 | · | part |
| 1.2 | Spindle Shaft | underfloor-wheel-lathe-spindle-shaft | 1× | 1 | · | part |
| 1.3 | Spindle Bearing | underfloor-wheel-lathe-spindle-bearing | 4× | 4 | · | part |
| 1.4 | Drive Belt | underfloor-wheel-lathe-spindle-belt | 1× | 1 | · | part |
| 1.5 | Tool Taper Interface | underfloor-wheel-lathe-spindle-taper | 1× | 1 | · | part |
| 2 | Cutting Tool Bit Assembly 3 parts | underfloor-wheel-lathe-cutting-tool | 1× | 1 | 3 | assembly |
| 2.1 | Carbide/Diamond Bit | underfloor-wheel-lathe-tool-bit | 1× | 1 | · | part |
| 2.2 | Tool Holder | underfloor-wheel-lathe-tool-holder | 1× | 1 | · | part |
| 2.3 | Bit Clamp | underfloor-wheel-lathe-tool-clamp | 1× | 1 | · | part |
| 3 | Friction Drive Roller 5 parts | underfloor-wheel-lathe-friction-roller | 2× | 2 | 6 | assembly |
| 3.1 | Roller Motor | underfloor-wheel-lathe-roller-motor | 1× | 2 | · | part |
| 3.2 | Roller Shaft | underfloor-wheel-lathe-roller-shaft | 1× | 2 | · | part |
| 3.3 | Roller Bearing | underfloor-wheel-lathe-roller-bearing | 2× | 4 | · | part |
| 3.4 | Rubber Roller Tire | underfloor-wheel-lathe-rubber-tire | 1× | 2 | · | part |
| 3.5 | Roller Mounting Arm | underfloor-wheel-lathe-roller-arm | 1× | 2 | · | part |
| 4 | Vertical Lifting Carriage 5 parts | underfloor-wheel-lathe-lifting-carriage | 1× | 1 | 5 | assembly |
| 4.1 | Carriage Frame | underfloor-wheel-lathe-carriage-frame | 1× | 1 | · | part |
| 4.2 | Ball-Screw Drive | underfloor-wheel-lathe-ballscrew-drive | 1× | 1 | · | part |
| 4.3 | Carriage Motor | underfloor-wheel-lathe-carriage-motor | 1× | 1 | · | part |
| 4.4 | Position Encoder | underfloor-wheel-lathe-carriage-encoder | 1× | 1 | · | part |
| 4.5 | Holding Brake | underfloor-wheel-lathe-carriage-brake | 1× | 1 | · | part |
| 5 | Wheel Profile Measuring System 3 parts | underfloor-wheel-lathe-measuring-system | 1× | 1 | 3 | assembly |
| 5.1 | Laser Distance Sensor | underfloor-wheel-lathe-laser-sensor | 1× | 1 | · | part |
| 5.2 | Probe Holder | underfloor-wheel-lathe-measurement-probe | 1× | 1 | · | part |
| 5.3 | Measurement Processor | underfloor-wheel-lathe-signal-processor | 1× | 1 | · | part |
| 6 | Pit-Mounted Base Frame 5 parts | underfloor-wheel-lathe-pit-frame | 1× | 1 | 16 | assembly |
| 6.1 | Base Plate | underfloor-wheel-lathe-base-plate | 1× | 1 | · | part |
| 6.2 | Frame Column | underfloor-wheel-lathe-frame-column | 2× | 2 | · | part |
| 6.3 | Cross Brace | underfloor-wheel-lathe-frame-brace | 4× | 4 | · | part |
| 6.4 | Anchor Bolt | underfloor-wheel-lathe-anchor-bolt | 8× | 8 | · | part |
| 6.5 | Leveling Shims | underfloor-wheel-lathe-shims | 1× | 1 | · | part |
| 7 | Hydraulic Power System 6 parts | underfloor-wheel-lathe-hydraulic-power | 1× | 1 | 7 | assembly |
| 7.1 | Hydraulic Pump | underfloor-wheel-lathe-hydraulic-pump | 1× | 1 | · | part |
| 7.2 | Pump Motor | underfloor-wheel-lathe-hydraulic-motor | 1× | 1 | · | part |
| 7.3 | Pressure Control Valve | underfloor-wheel-lathe-pressure-valve | 1× | 1 | · | part |
| 7.4 | Accumulator | underfloor-wheel-lathe-accumulator | 1× | 1 | · | part |
| 7.5 | Hydraulic Cylinder | underfloor-wheel-lathe-cylinder | 2× | 2 | · | part |
| 7.6 | Hydraulic Hose | underfloor-wheel-lathe-hydraulic-hose | 1× | 1 | · | part |
| 8 | Operator Control Console 8 parts | underfloor-wheel-lathe-control-console | 1× | 1 | 8 | assembly |
| 8.1 | Console Pedestal | underfloor-wheel-lathe-control-pedestal | 1× | 1 | · | part |
| 8.2 | PLC Controller | underfloor-wheel-lathe-plc-controller | 1× | 1 | · | part |
| 8.3 | Speed Potentiometer | underfloor-wheel-lathe-speed-potentiometer | 1× | 1 | · | part |
| 8.4 | Height Control Joystick | underfloor-wheel-lathe-height-joystick | 1× | 1 | · | part |
| 8.5 | Start/Stop Buttons | underfloor-wheel-lathe-start-stop-buttons | 1× | 1 | · | part |
| 8.6 | Emergency Stop | underfloor-wheel-lathe-emergency-stop | 1× | 1 | · | part |
| 8.7 | Digital Display | underfloor-wheel-lathe-status-display | 1× | 1 | · | part |
| 8.8 | Pit Gate Interlock | underfloor-wheel-lathe-safety-interlock-switch | 1× | 1 | · | part |
Something wrong in this list? Report a problem with this BOM.
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $500k–$60M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇨🇳CRRC
crrcgc.cc ↗
|
Beijing, CN | Rolling stock & rail systems | made to order | 40–72 wks |
|
🇫🇷Alstom
alstom.com ↗
|
Saint-Ouen, FR | Rail rolling stock | made to order | 40–72 wks |
| mobility.siemens.com ↗ | Munich, DE | Rail systems | made to order | 40–72 wks |
| stadlerrail.com ↗ | Bussnang, CH | Rail rolling stock | made to order | 40–72 wks |
|
🇺🇸Wabtec
wabteccorp.com ↗
|
Pittsburgh, US | Rail equipment | made to order | 40–72 wks |
932-word article