Centrifugal Casting Machine
ProductOverview
Centrifugal casting is a specialized process where molten metal is poured into a rotating mold, and centrifugal force, rather than gravity, pushes the metal outward against the mold wall. This technique produces extremely dense, sound castings with minimal gas porosity and shrinkage cavities. It is particularly suited to cylindrical or tubular shapes (pipes, sleeves, bearings) but can also produce complex geometries using properly designed mold cavities.
The principal advantage of centrifugal casting is porosity elimination: a metal "plug" naturally forms at the mold center (the low-g zone), containing most shrinkage and gases; the outer wall (highest centrifugal force) is pristine and compact. After solidification, this porous plug is removed, leaving a sound casting.
How it works
The process begins with an empty, refractory-lined steel rotating mold mounted on a horizontal spindle drive. The operator places the mold on the spindle, securing it with the precision flange. Water cooling lines are connected to the rotary union, enabling cooling flow to the rotating mold jacket.
Next, molten metal is poured into the stationary pouring ladle, which is positioned above the spindle centerline. The metal temperature is held at 1400–1500 °C (verified by thermocouple).
When the PLC start signal is given, the spindle motor and VFD begin ramping the spindle speed upward smoothly (acceleration ramp: 0 to final speed over 5–10 seconds). Simultaneously, the operator opens a gate valve on the pouring ladle, releasing molten metal into a feed tube that drops into the mold center.
As the spindle accelerates, centrifugal force increases (linear with radius and quadratic with angular velocity). By the time the spindle reaches target speed (typically 500–1500 rpm for large castings, 1500–2000 rpm for small), the metal is being pressed hard against the mold wall at 50–200 g acceleration. The liquid metal fills the mold from inside outward, with the rotating mold surface acting as the "outside" boundary and the mold centerline (lowest g-force) as the inside boundary.
During pouring (30–90 seconds), the mold cooling system is actively rejecting heat: water at 5 bar flows through the rotating union into the cooling jacket, removing sensible heat from the solidifying metal. The outer wall (against the hot mold copper) solidifies first; inner layers solidify gradually as heat conducts inward.
Once the predetermined pour volume is reached, the operator closes the feed valve, stopping metal flow. The spindle continues rotating briefly (20–60 seconds) to maintain pressure during final solidification. Then the spindle decelerates and stops.
After cooling (typically 2–10 minutes at rest, depending on wall thickness), the ejection system is activated: a hydraulic stripper cylinder pushes a stripper plate, removing the casting from the mold. The casting falls onto a conveyor for removal; the mold is cleaned and a new cycle begins.
Porosity control and metallurgy
The key benefit of centrifugal casting is porosity distribution. Gravity casting produces a casting with gas bubbles scattered throughout, reducing density and strength. Centrifugal casting concentrates shrinkage and gas bubbles at the mold center (the low-g zone), leaving the outer wall (high stress zone) porosity-free.
After ejection, the casting's central "plug" (typically 10–20 % of diameter) is removed by boring or cutting, discarding the porous material. The remaining outer wall is a dense, sound casting with >99 % density vs. gravity-cast baseline of ~95–98 %.
This density improvement is critical for applications like pump casings, bearing sleeves, or hydraulic cylinders, where internal porosity would propagate fatigue cracks and cause premature failure.
Mold design and materials
The mold must be dynamically balanced (typically <2.5 g·mm runout) to avoid vibration and poor surface finish. Molds are precision-ground and often paired with counterweights to achieve balance.
The refractory lining (high-alumina brick or castable) must resist the pressure and impact of molten metal. A typical lining lasts 50–200 castings before erosion or cracking requires replacement.
The cooling jacket is critical: inadequate cooling results in slow solidification, allowing segregation and bubble formation. Over-cooling can cause thermal shock and mold cracking. Water flow is typically 100–200 LPM at 5 bar, controlled by the operator or PLC based on cooling-tower setpoint.
Process parameters and adjustability
Spindle speed is the primary control variable: lower speeds (500–800 rpm) are used for large-diameter, thin-wall castings where high centrifugal force is necessary for density; higher speeds (1500–2000 rpm) are used for small-diameter or thick-wall castings where the metal naturally fills the mold even with modest acceleration.
Pour rate (metal flow into the mold) is controlled by the feed valve: faster pour (larger valve opening) fills the mold quickly but risks segregation; slower pour allows steady-state filling and better density.
Cooling-water temperature is adjustable via a thermostatic mixing valve: hotter water (30–40 °C) slows cooling, improving flow before solidification sets; cooler water (15–20 °C) accelerates solidification, useful for thick-wall castings.
Comparison with other casting methods
Centrifugal casting is superior to sand-mold gravity casting for producing sound parts with high strength. It is inferior to continuous casting in terms of speed and automation but produces superior castings for complex geometries.
For specialty applications (large bearing sleeves, pump housings), foundries often justify the capital investment in centrifugal equipment.
Maintenance and safety
The spindle bearing must be well-lubricated (automated grease system) and inspected regularly; bearing failures are catastrophic (mold can come loose at speed, creating a safety hazard).
The safety enclosure with interlocked doors is mandatory: no operator should access the rotating spindle. The emergency-stop button must be prominently located and easily accessible.
The hydraulic system requires weekly filter changes; contamination causes cylinder seal failure and slow ejection, risking casting damage or operator injury.
Centrifugal Casting Machine parts and their functions
8 top-level parts · 43 parts in total · full bill of materials below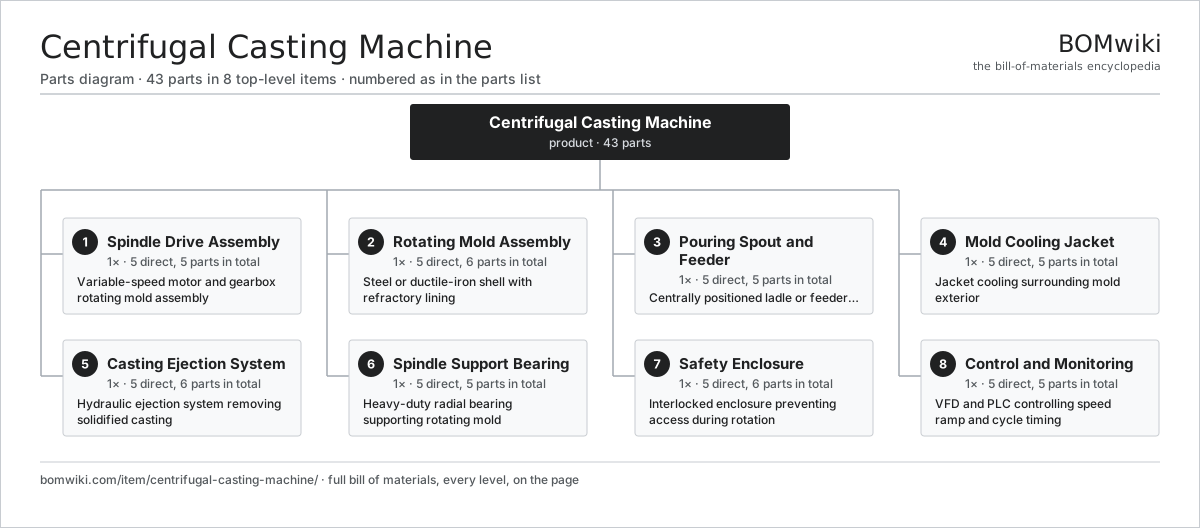
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Spindle Drive Assembly 5 parts | 1× | Variable-speed motor and gearbox rotating mold assembly |
| 2 | Rotating Mold Assembly 5 parts | 1× | Steel or ductile-iron shell with refractory lining |
| 3 | Pouring Spout and Feeder 5 parts | 1× | Centrally positioned ladle or feeder directing metal into mold |
| 4 | Mold Cooling Jacket 5 parts | 1× | Jacket cooling surrounding mold exterior |
| 5 | Casting Ejection System 5 parts | 1× | Hydraulic ejection system removing solidified casting |
| 6 | Spindle Support Bearing 5 parts | 1× | Heavy-duty radial bearing supporting rotating mold |
| 7 | Safety Enclosure 5 parts | 1× | Interlocked enclosure preventing access during rotation |
| 8 | Control and Monitoring 5 parts | 1× | VFD and PLC controlling speed ramp and cycle timing |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Centrifugal Casting Machine
8 top-level lines · 48 rows shown · 43 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Spindle Drive Assembly 5 parts | centrifugal-casting-machine-spindle-drive | 1× | 1 | 5 | assembly |
| 1.1 | Spindle Drive Motor | centrifugal-casting-machine-spindle-motor | 1× | 1 | · | part |
| 1.2 | Spindle VFD | centrifugal-casting-machine-vfd-drive | 1× | 1 | · | part |
| 1.3 | Spindle Gearbox | centrifugal-casting-machine-spindle-gearbox | 1× | 1 | · | part |
| 1.4 | Main Spindle Shaft | centrifugal-casting-machine-spindle-shaft | 1× | 1 | · | part |
| 1.5 | Spindle Brake | centrifugal-casting-machine-shaft-brake | 1× | 1 | · | part |
| 2 | Rotating Mold Assembly 5 parts | centrifugal-casting-machine-rotating-mold | 1× | 1 | 6 | assembly |
| 2.1 | Mold Steel Shell | centrifugal-casting-machine-mold-shell | 1× | 1 | · | part |
| 2.2 | Mold Refractory Lining | centrifugal-casting-machine-mold-refractory | 1× | 1 | · | part |
| 2.3 | Mold Mounting Flange | centrifugal-casting-machine-mold-flange | 1× | 1 | · | part |
| 2.4 | Mold Seal Ring | centrifugal-casting-machine-mold-seal-ring | 1× | 1 | · | part |
| 2.5 | Mold End Caps | centrifugal-casting-machine-end-caps | 2× | 2 | · | part |
| 3 | Pouring Spout and Feeder 5 parts | centrifugal-casting-machine-pouring-spout | 1× | 1 | 5 | assembly |
| 3.1 | Pouring Ladle | centrifugal-casting-machine-pouring-ladle | 1× | 1 | · | part |
| 3.2 | Ladle Support Arm | centrifugal-casting-machine-ladle-support-arm | 1× | 1 | · | part |
| 3.3 | Feed Tube | centrifugal-casting-machine-feed-tube | 1× | 1 | · | part |
| 3.4 | Feed Control Valve | centrifugal-casting-machine-feed-valve | 1× | 1 | · | part |
| 3.5 | Ladle Immersion Heater | centrifugal-casting-machine-spout-heater | 1× | 1 | · | part |
| 4 | Mold Cooling Jacket 5 parts | centrifugal-casting-machine-water-cooling | 1× | 1 | 5 | assembly |
| 4.1 | Cooling Jacket Tubing | centrifugal-casting-machine-cooling-jacket | 1× | 1 | · | part |
| 4.2 | Rotating Water Union | centrifugal-casting-machine-rotary-coupling | 1× | 1 | · | part |
| 4.3 | Cooling Pump | centrifugal-casting-machine-cooling-pump | 1× | 1 | · | part |
| 4.4 | Cooling Tower | centrifugal-casting-machine-cooling-tower | 1× | 1 | · | part |
| 4.5 | Coolant Filter | centrifugal-casting-machine-coolant-filter | 1× | 1 | · | part |
| 5 | Casting Ejection System 5 parts | centrifugal-casting-machine-mold-extraction | 1× | 1 | 6 | assembly |
| 5.1 | Ejection Stripper Plate | centrifugal-casting-machine-stripper-plate | 1× | 1 | · | part |
| 5.2 | Stripper Hydraulic Cylinder | centrifugal-casting-machine-stripper-cylinder | 1× | 1 | · | part |
| 5.3 | Stripper Guide Post | centrifugal-casting-machine-stripper-guide | 2× | 2 | · | part |
| 5.4 | Return Spring | centrifugal-casting-machine-ejection-spring | 1× | 1 | · | part |
| 5.5 | Hydraulic Pump | centrifugal-casting-machine-hydraulic-pump | 1× | 1 | · | part |
| 6 | Spindle Support Bearing 5 parts | centrifugal-casting-machine-spindle-bearing | 1× | 1 | 5 | assembly |
| 6.1 | Bearing Pillow Block | centrifugal-casting-machine-bearing-block | 1× | 1 | · | part |
| 6.2 | Roller Bearing | centrifugal-casting-machine-bearing-unit | 1× | 1 | · | part |
| 6.3 | Bearing Lubrication System | centrifugal-casting-machine-bearing-lubrication | 1× | 1 | · | part |
| 6.4 | Thrust Collar | centrifugal-casting-machine-thrust-collar | 1× | 1 | · | part |
| 6.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 7 | Safety Enclosure 5 parts | centrifugal-casting-machine-safety-guards | 1× | 1 | 6 | assembly |
| 7.1 | Guard Frame Structure | centrifugal-casting-machine-guard-frame | 1× | 1 | · | part |
| 7.2 | Door Interlock Switch | centrifugal-casting-machine-interlock-switch | 2× | 2 | · | part |
| 7.3 | Safety Relay Module | centrifugal-casting-machine-safety-relay | 1× | 1 | · | part |
| 7.4 | E-Stop Button | centrifugal-casting-machine-emergency-stop | 1× | 1 | · | part |
| 7.5 | Beacon Light | centrifugal-casting-machine-warning-light | 1× | 1 | · | part |
| 8 | Control and Monitoring 5 parts | centrifugal-casting-machine-control-system | 1× | 1 | 5 | assembly |
| 8.1 | Control PLC | centrifugal-casting-machine-main-plc | 1× | 1 | · | part |
| 8.2 | Spindle Motor VFD | centrifugal-casting-machine-vfd-spindle | 1× | 1 | · | part |
| 8.3 | Speed Feedback Encoder | centrifugal-casting-machine-speed-sensor | 1× | 1 | · | part |
| 8.4 | Mold Temperature Sensor | centrifugal-casting-machine-temperature-sensor | 1× | 1 | · | part |
| 8.5 | Control Panel | centrifugal-casting-machine-hmi-panel | 1× | 1 | · | part |
Something wrong in this list? Report a problem with this BOM.
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
1,072-word article