Column Still
ProductAlso known as: Column Distillation Still
Overview
The continuous column still represents the opposite approach from the copper pot still: instead of batch heating and manual cuts (heads/hearts/tails), the column still operates continuously, automatically separating ethanol vapors from heavier congeners via 12 stacked distillation stages. Input is fermented wash (10–12 % ABV); output is near-neutral grain spirits (92–96 % ABV) 24/7 without operator intervention beyond initial startup and feed replenishment. This technology dominates industrial spirit production globally, vodka, gin, rectified spirits, fuel ethanol, because yield is maximized (98–99 % of theoretical maximum) and operating costs (labor, energy) are minimized.
For craft and small commercial distilleries seeking high-proof spirits without batch interruptions, a column still is the automation step between artisanal pot stills and massive industrial towers. A 0.5 m diameter column still (described here) produces 50–100 L/day of product spirits, suitable for a small gin house, premium vodka producer, or grain neutral spirit manufacturer.
Thermodynamic Separation: The Bubble-Cap Tray
The column's heart is its 12 stacked bubble-cap trays, each creating a stage of equilibrium separation. Ascending hot vapor from the reboiler bubbles upward through each tray's liquid, while heavier liquid (reflux condensate) flows downward via the downpipes. In each stage, lighter volatiles (ethanol, aldehydes) preferentially evaporate into rising vapor; heavier congeners (fusel alcohols, esters) remain in liquid phase.
This counter-current flow is the secret to high separation efficiency. After just 12 stages (HETP ~0.3–0.4 m, Height Equivalent to Theoretical Plate), the still achieves what a single-pot distillation cannot do in 20 boilings. The thermodynamic principle is Raoult's law: each component has a unique vapor pressure; continuous contact allows vapor and liquid to approach equilibrium at each stage.
Consider fermented wash entering at the column mid-point (tray 6):
- Tray 1 (top): ~98 % ethanol, near-trace congeners
- Tray 6 (feed inlet): 40–50 % ethanol, mixed congeners
- Tray 12 (bottom): ~5 % ethanol, water, heavy stillage
Rising vapor from tray 12 carries perhaps 50 % ethanol. By tray 11, it has concentrated to 60 %. By tray 1, it reaches 98 %. The dephlegmator (partial condenser at top) captures only vapors >96 % ABV, returning the 90–96 % fraction as reflux; this reflux re-boils, driving further separation.
Operational Sequence: Startup to Steady State
Pre-startup (Cold Still): All trays are empty; no vapor rises. The operator fills the reboiler kettle with 50 L of fermented wash. The feed pump is off. The steam valve is closed.
Phase 1: Reboiler Heating (0–30 min) Steam opens slowly via the control valve. The RTD sensor monitors kettle temperature. At 80°C, light vapors rise into the column but condense at the cold tray surfaces (condensation heat warms trays, inefficient). By 100°C, steady vapor generation begins. Light vapors ascend, condense on upper trays, create a reflux cascade. Temperature gradually rises through the column.
Phase 2: Column Temperature Rise (30–90 min) Vapor reaches the top tray; a small amount escapes to the dephlegmator, which condenses it and returns reflux. As tray temperatures rise above condensation point, the column stabilizes. The dephlegmator cooling valve is cracked open slightly; reflux begins. The product condenser starts receiving high-proof vapors and producing first drops of spirits (~88 % ABV).
Phase 3: Steady State (90+ min) The entire column reaches equilibrium. The reboiler temperature stabilizes at 100°C. The dephlegmator maintains reflux return at ~3:1 ratio (3 L reflux per 1 L product takeoff). The feed pump opens to deliver 40 L/hour fermented wash. This wash enters at mid-column (tray 6) at 65°C (pre-heated via the feed HX). As fresh feed enters, an equal mass of exhausted stillage is withdrawn from the reboiler bottom and pumped back to tray 12.
Steady-state product is now 92–96 % ABV, emerging from the product condenser at 20–25°C and flowing into collection via glass rotameter for visual flowrate confirmation.
The Dephlegmator's Critical Role
The dephlegmator is not a full condenser, it is a partial one, selectively condensing only the lowest-boiling fractions (>96 % ethanol equivalent). This is counterintuitive but essential. If the dephlegmator were a full condenser, 100 % of top vapors would condense to liquid reflux, returning nothing to the product condenser. The column would produce nothing, all liquid refluxes indefinitely.
The solution: run cooling water at 15–20°C through the dephlegmator tubes at modest flowrate (5–10 GPM). At this rate, only vapors boiling above 78°C (pure ethanol equivalent) fully condense. Vapors boiling 70–78°C (94–96 % ABV ethanol-fusel alcohol mixtures) partially condense, creating a two-phase mixture that is drawn off as product.
The dephlegmator cooling valve modulates water flow to control reflux ratio:
- Higher water flow → more condensation → higher reflux ratio → higher column separation → product approaches 96 % ABV but yield drops
- Lower water flow → less condensation → lower reflux ratio → faster throughput → product 92–94 % ABV but composition varies
A skilled operator balances yield vs. purity. Most commercial operations run 92–94 % ABV neutral spirits to maximize hourly throughput; premium gin producers might back-off to 90 % ABV to allow slightly more congener carry-over (esters, aldehydes) for flavor contribution.
Feed Preheating & Heat Integration
The feed preheating system serves dual purpose: thermodynamic and economic.
Thermodynamic: Cold fermented wash entering at room temperature (20°C) into a 100°C column would vaporize immediately, creating violent flooding and foaming. Pre-heating to 65°C allows controlled evaporation. The feed enters at tray 6 as liquid, partially evaporates due to sensible heat of the surrounding hot liquid/vapor.
Economic: The column overhead constantly vaporizes ethanol-rich mixtures. This vapor carries latent heat ~900 kJ/kg ethanol. The feed HX captures this heat, condensing a small portion of overhead vapors (reducing product yield by ~2 %) but raising incoming wash to 65°C. This provides a net energy savings of 30–40 % compared to preheating via external boiler.
The outlet thermometer confirms 65°C feedstock. If wash is too cold (<55°C), flooding risk increases; too hot (>75°C) causes uncontrolled boiling at the feed zone.
Continuous Operation & Automation
Unlike batch pot stills (requiring operator attention for heads/hearts/tails cuts), the column still runs fully automated once steady-state is reached. The PLC controller manages:
- Reboiler steam valve: Maintains kettle temperature at 100°C via RTD feedback
- Dephlegmator cooling water valve: Adjusts reflux return rate based on top column temperature
- Feed pump speed: Delivers constant 40–80 L/hour wash to maintain column pressure
- Condensate drain rate: Balances stillage discharge to prevent kettle overfill
An operator simply:
- Tops up fermented wash feed tank daily
- Monitors product ABV hourly via sampling to spirit safe-equivalent hydrometer
- Periodically opens bottom drain to discharge exhausted stillage
Typical daily routine: load 500 L fermented wash; produce 50–80 L spirits at 92 % ABV; drain 420 L spent stillage. Single shift operation.
The Neutral Spirits Flavor Profile
A column still producing 92–96 % ABV grain spirits is intentionally high-reflux (heavy continuous distillation), stripping away nearly all congeners, esters, aldehydes, fusel alcohols. The output tastes neutral, suitable for:
- Vodka: Filtered and diluted to 40 % ABV, marketed on purity and smoothness
- Gin: Product taken at 92 % ABV, then diluted and blended with juniper/botanicals (congeners from botanicals provide flavor)
- Neutral grain spirit: Base ingredient for liqueurs, creams, extracts
- Fuel ethanol: Industrial solvent
For contrast, a pot still produces 70 % ABV spirits with full congener carry-over, giving whiskey its fruity character, brandy its wine-like richness. The choice is deliberate: column still = neutral base for blending; pot still = flavorful product ready to drink (after barrel aging).
Maintenance & Tray Fouling
Over weeks of continuous operation, a column still's bubble-cap trays accumulate organic residue, yeast cell walls, proteins, minerals, reducing efficiency. Signs include rising temperature differential across trays (inefficient heat/mass transfer) or falling product ABV at constant feed rate (fractionation degrading).
Remedy: In-place chemical cleaning (CIP):
- Stop feed pump; close reboiler steam
- Inject hot water + 2 % NaOH (caustic) into feed inlet for 1 hour
- Circulate through reboiler, condenser, drain system
- Rinse with 1 % H₂SO₄ acid for 30 min
- Final hot water rinse
- Restart after 12-hour dry-out
For severe fouling (tray valve sticking), manual disassembly is required, a specialized skill job taking 2–4 days. Most commercial plants budget one deep clean per year.
Regulatory & Excise Tax Context
Column stills used for spirit production operate under government excise supervision. In the USA, TTB regulates:
- Spirits must be produced under permit in bonded facility
- All product is taxed at $13.50/proof gallon (federal)
- Accurate production records (daily logs of feed, steam, yield)
A 92 % ABV column still producing 100 L/day (92 proof-liters/day = 1,196 proof-liters/month) incurs ~$16,000 monthly federal excise tax. This is pre-paid or deferred via bonded warehouse system. The economics favor large-volume producers; small batch distilleries often accept the tax burden as cost of doing business.
This equipment represents a $40K–80K capital investment (custom-built column, controls, utilities integration), suitable for established production facilities with consistent demand for neutral spirits or gin.
Column Still parts and their functions
7 top-level parts · 137 parts in total · full bill of materials below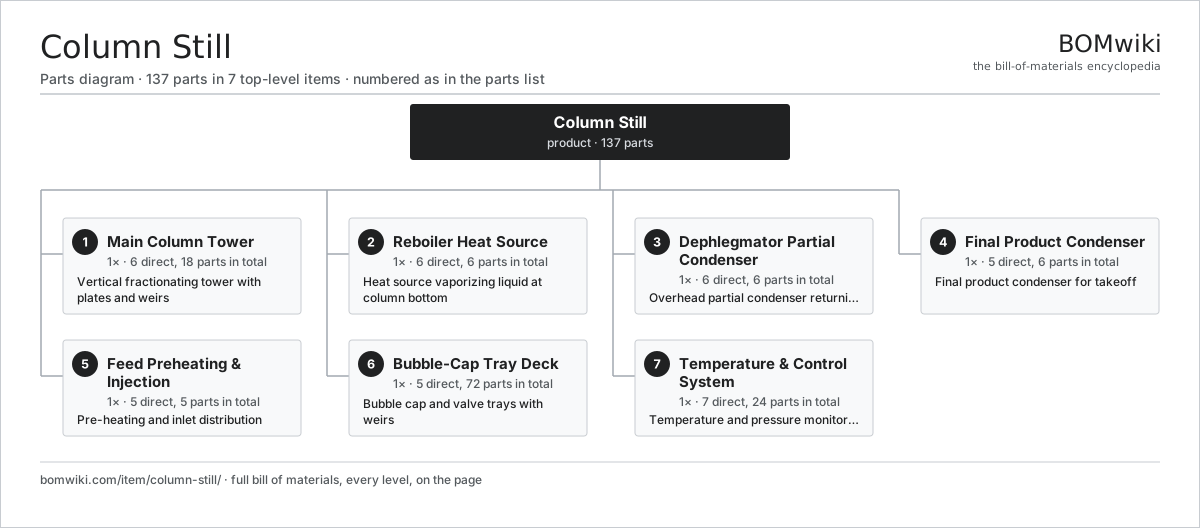
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Main Column Tower 6 parts | 1× | Vertical fractionating tower with plates and weirs |
| 2 | Reboiler Heat Source 6 parts | 1× | Heat source vaporizing liquid at column bottom |
| 3 | Dephlegmator Partial Condenser 6 parts | 1× | Overhead partial condenser returning reflux liquid |
| 4 | Final Product Condenser 5 parts | 1× | Final product condenser for takeoff |
| 5 | Feed Preheating & Injection 5 parts | 1× | Pre-heating and inlet distribution |
| 6 | Bubble-Cap Tray Deck 5 parts | 1× | Bubble cap and valve trays with weirs |
| 7 | Temperature & Control System 7 parts | 1× | Temperature and pressure monitoring |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Column Still
7 top-level lines · 47 rows shown · 137 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Main Column Tower 6 parts | column-still-main-column | 1× | 1 | 18 | assembly |
| 1.1 | Column Tube | column-still-column-shell | 1× | 1 | · | part |
| 1.2 | Tray Support Ring | column-still-tray-support-rings | 12× | 12 | · | part |
| 1.3 | Manway Access Port | column-still-manway-port | 2× | 2 | · | part |
| 1.4 | Wash Feed Inlet | column-still-wash-lines-inlet | 1× | 1 | · | part |
| 1.5 | Bottom Stillage Outlet | column-still-column-bottom-outlet | 1× | 1 | · | part |
| 1.6 | Overhead Product Line | column-still-top-product-outlet | 1× | 1 | · | part |
| 2 | Reboiler Heat Source 6 parts | column-still-reboiler-base | 1× | 1 | 6 | assembly |
| 2.1 | Reboiler Kettle | column-still-reboiler-pot | 1× | 1 | · | part |
| 2.2 | Reboiler Steam Coil | column-still-steam-coil | 1× | 1 | · | part |
| 2.3 | Reboiler Circulation Pump | column-still-reboiler-pump | 1× | 1 | · | part |
| 2.4 | Reboiler Steam Control Valve | column-still-steam-control-valve | 1× | 1 | · | part |
| 2.5 | Reboiler RTD Sensor | column-still-reboiler-temperature-probe | 1× | 1 | · | part |
| 2.6 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 3 | Dephlegmator Partial Condenser 6 parts | column-still-dephlegmator | 1× | 1 | 6 | assembly |
| 3.1 | Dephlegmator Shell | column-still-dephlegmator-shell | 1× | 1 | · | part |
| 3.2 | Dephlegmator Tube Bundle | column-still-dephlegmator-tubes | 1× | 1 | · | part |
| 3.3 | Dephlegmator Cooling Valve | column-still-dephlegmator-cooling-valve | 1× | 1 | · | part |
| 3.4 | Reflux Return Line | column-still-reflux-return-line | 1× | 1 | · | part |
| 3.5 | Spirits Vapor Outlet | column-still-spirits-vapor-outlet | 1× | 1 | · | part |
| 3.6 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 4 | Final Product Condenser 5 parts | column-still-total-condenser | 1× | 1 | 6 | assembly |
| 4.1 | Product Condenser Shell | column-still-condenser-shell | 1× | 1 | · | part |
| 4.2 | Product Condenser Tubes | column-still-condenser-tubes | 1× | 1 | · | part |
| 4.3 | Product Outlet Thermometer | column-still-condenser-outlet-thermometer | 1× | 1 | · | part |
| 4.4 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 4.5 | Connector | connector | 2× | 2 | · | part |
| 5 | Feed Preheating & Injection 5 parts | column-still-feed-system | 1× | 1 | 5 | assembly |
| 5.1 | Feed Preheater HX | column-still-feed-hx | 1× | 1 | · | part |
| 5.2 | Feed Metering Pump | column-still-feed-pump | 1× | 1 | · | part |
| 5.3 | Feed Flow Meter | column-still-feed-flowmeter | 1× | 1 | · | part |
| 5.4 | Feed Distribution Ring | column-still-feed-distributor | 1× | 1 | · | part |
| 5.5 | Feed Temperature Gauge | column-still-feed-thermometer | 1× | 1 | · | part |
| 6 | Bubble-Cap Tray Deck 5 parts | column-still-plate-assembly | 1× | 1 | 72 | assembly |
| 6.1 | Bubble-Cap Riser | column-still-bubble-cap | 24× | 24 | · | part |
| 6.2 | Tray Plate | column-still-tray-frame | 12× | 12 | · | part |
| 6.3 | Tray Overflow Weir | column-still-tray-weir | 12× | 12 | · | part |
| 6.4 | Tray Liquid Downpipe | column-still-tray-downpipe | 12× | 12 | · | part |
| 6.5 | Fastener Set | fastener-set | 12× | 12 | · | part |
| 7 | Temperature & Control System 7 parts | column-still-instrumentation | 1× | 1 | 24 | assembly |
| 7.1 | Column Control PLC | column-still-plc | 1× | 1 | · | part |
| 7.2 | Temperature Probe | column-still-temp-probes | 5× | 5 | · | part |
| 7.3 | Pressure Transducer | column-still-pressure-transducers | 3× | 3 | · | part |
| 7.4 | Valve Control Motor | column-still-control-valve-motor | 2× | 2 | · | part |
| 7.5 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.6 | Relay | relay | 4× | 4 | · | part |
| 7.7 | Connector | connector | 8× | 8 | · | part |
Something wrong in this list? Report a problem with this BOM.
Related products
same domain, ranked by shared parts Automatic Espresso Tamper
45 parts · shares 3 with this page
Automatic Filleting Machine
73 parts · shares 3 with this page
 Bakery Deck Oven
44 parts · shares 3 with this page
Beverage Carbonator
95 parts · shares 3 with this page
Bottle Rinser
36 parts · shares 3 with this page
 Bottle Washing Machine
2,388 parts · shares 3 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $1k–$500k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| gea.com ↗ | Düsseldorf, DE | Process technology | 20 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 20 units | 12–20 wks |
| tetrapak.com ↗ | Pully, CH | Food packaging & processing | 20 units | 12–20 wks |
| jbtc.com ↗ | Chicago, US | Food processing equipment | 20 units | 12–20 wks |
| alfalaval.com ↗ | Lund, SE | Heat transfer & separation | 20 units | 12–20 wks |
1,653-word article