Digital Textile Printer
ProductOverview
A digital textile printer deposits colored liquid ink directly onto fabric using computer-controlled inkjet nozzles, eliminating the need for screen preparation and enabling high-resolution, full-color prints. The machine accepts design files (bitmap or vector) from design software, uses a Rasterimage Processor (RIP) to separate colors and generate head firing sequences, and prints by depositing ink droplets 5–10 picoliters each at 1–10 kHz frequency.
Digital printing has revolutionized textile production for short-run and custom applications. It eliminates traditional screen setup costs and time, enabling economical production of one-of-a-kind designs, prototypes, and small batches. Quality textile digital printers produce photo-realistic images rivaling traditional printing methods at similar quality levels.
How It Works
The process begins with a design file (TIFF, PNG, PDF, or vector format) loaded into the RIP software on the control computer. The RIP separates the image into cyan, magenta, yellow, and black (CMYK) separations and generates a binary firing pattern for each print head's 300–1200 nozzles.
Fabric is positioned on a motorized transport belt and optionally pre-warmed by a preheating zone to 40–60°C. Pre-warming improves ink absorption and color intensity on cotton and silk. The fabric advances one print pass at a time, typically 0.1–0.5 mm per pass.
Four piezo or thermal print heads (one per color: cyan, magenta, yellow, black) are mounted in a fixed position above the fabric. At each print pass, the RIP-generated firing sequence triggers nozzles to eject ink droplets. Each nozzle fires 1–10 times per millisecond, depositing cumulative ink onto the same fabric location. Overlapping passes with different colors create the full-color image through color overlap and dithering.
After printing, the fabric passes through a dryer where heated air (80–120°C) and infrared heat evaporate water and fix dyes into fibers. The drying duration depends on fabric type: cotton reactive dyes need 5–10 seconds; silk direct dyes need 10–20 seconds.
The finished printed fabric unwinds from the take-up roll. Some applications require post-printing processing (steaming, chemical fixation) depending on ink type.
Print Head Technology
Modern textile printers use two print head types:
Piezo inkjet: An electric signal deforms a piezo ceramic element, reducing chamber volume and forcing ink through a nozzle orifice 70–100 µm diameter. Piezo heads are robust and tolerant of varying ink viscosity. Firing frequency is 1–10 kHz.
Thermal inkjet: An electric heater boils ink, creating a vapor bubble that forces liquid through the nozzle. Thermal heads are lower cost but more sensitive to ink chemistry and temperature.
Each head contains 300–1200 nozzles arranged in a line across the fabric width. For a 3.2 m printer at 300 dpi, the cyan head has 3800 nozzles spaced 85 µm (1/300 inch). All nozzles in a head fire simultaneously to create one pass across the fabric.
Nozzles must remain clean and primed. A damper on the ink line prevents pressure spikes that could cause cavitation or nozzle flooding. Regular maintenance includes purging (forcing fresh ink through nozzles) and head cleaning (backflushing or ultrasonic vibration).
Ink System
The ink system includes separate reservoirs (5–50 liters each) for cyan, magenta, yellow, and black. An ink pump circulates ink continuously through the print heads at 0.5–2 liters/minute and 1.5–3 bar pressure. A regulator maintains constant pressure despite variations in nozzle backpressure.
An ink filter removes particles larger than the nozzle orifice (typically >10 µm). Ink viscosity must be controlled: too thick and nozzles clog; too thin and satellite drops form. Most systems maintain ink at 20–25°C for consistent viscosity.
Ink types depend on fabric and final use:
- Reactive dyes: Form covalent bonds with fiber, offering brightness and wash-fastness (cotton, silk).
- Direct dyes: Absorb into fibers via hydrogen bonding (less durable but cheaper).
- Pigment suspensions: Particles coating fiber surface (suitable for synthetics).
- Specialty inks: Fluorescent, metallic, opaque white, or discharge (bleach-based).
Fabric Transport and Registration
The transport belt must move with sub-0.1 mm accuracy. An encoder on the belt drive provides feedback, allowing the RIP to synchronize head firing with fabric position. If the fabric advances 0.2 mm per pass and the printer runs 600 dpi (42.3 µm per dot), roughly 5 passes are needed to cover the print width fully.
Registration marks printed in each color allow optical feedback correction. If magenta is 0.5 mm off-register relative to cyan, the camera detects the misalignment and the control system adjusts the print head position micrometers at a time until colors overlap perfectly.
Preheating and Drying
The preheating zone warms fabric to 40–60°C, expanding fiber and opening fiber structure for better dye absorption. This is optional but improves color intensity and wash-fastness. Heated water or infrared elements provide heat.
The dryer is critical for final quality. Insufficient drying leaves ink wet and prone to bleeding; over-drying can cause dye migration or fiber damage. Temperature and duration are adjusted per fabric type using the timer controller. Exhaust air, if uncontrolled, can smell of ink solvents (acetic acid, propylene glycol); many industrial installations include solvent scrubbers or condensers.
Design to Print Workflow
A designer creates artwork in Adobe Illustrator, Photoshop, or CAD software. The file is imported into the RIP software, which displays a preview and allows color correction (saturation, brightness), halftoning settings (dot shape, size), and width/repeat adjustments.
The RIP separates the design into CMYK and generates binary firing maps: for each nozzle in each head, when should it fire during each pass. This firing map is typically 1–2 MB for a single garment. The map is uploaded to the printer's control computer, which streams it to the print engine during production.
Modern RIP software includes color management profiles (device profiles) calibrating printer output to industry standards (PANTONE, Fogra). Many printers include onboard color correction to match reference prints or digital proofs.
Production Capacity and Economics
Print speed varies with resolution:
- 300 dpi: 100–150 m²/hour
- 600 dpi: 50–100 m²/hour
- 1200 dpi: 20–50 m²/hour
A T-shirt front (0.3 m²) at 600 dpi takes 11–18 seconds print time. Reload and preheating add another 20–40 seconds. Economics favor runs of 50–500 pieces for custom prints; above 500, traditional screen printing becomes cheaper per unit.
Ink consumption is 0.5–1.5 ml per m² depending on color intensity. A typical fabric at full saturation uses 1 ml/m²; pale pastels use 0.3 ml/m².
Variants
- Flatbed digital printers: Print heads move across stationary fabric; used for pre-cut garments, leather, rigid substrates.
- Belt-fed machines: Like roll-fed but with fabric secured to a moving belt.
- Continuous printing: Fabric moves continuously; heads fire with no start-stop acceleration, maximizing throughput.
- Hybrid systems: Digital print head on traditional rotary screen machine, combining speed with design flexibility.
Digital Textile Printer parts and their functions
8 top-level parts · 1,093 parts in total · full bill of materials below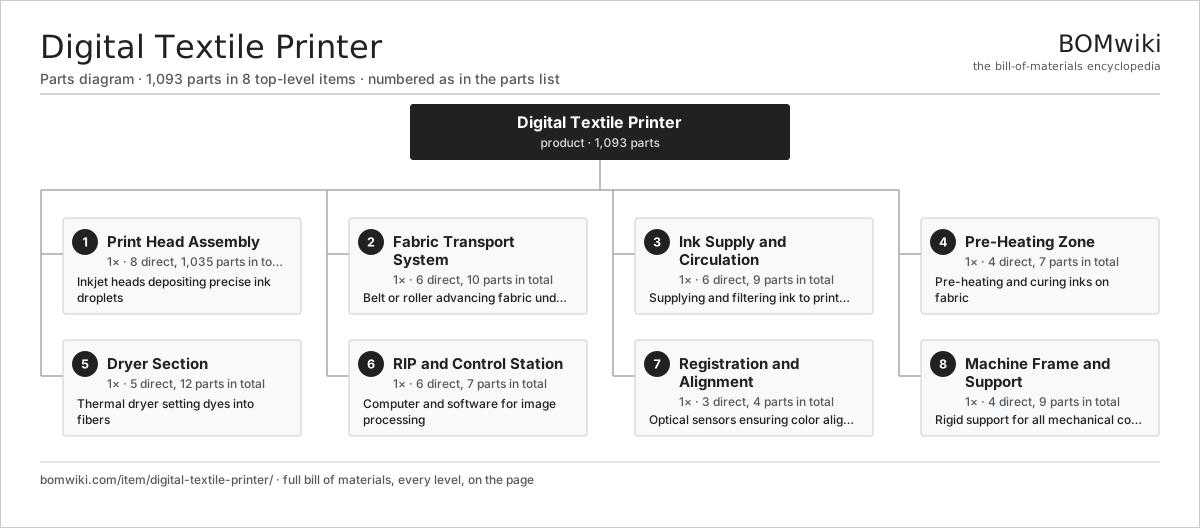
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Print Head Assembly 8 parts | 1× | Inkjet heads depositing precise ink droplets |
| 2 | Fabric Transport System 6 parts | 1× | Belt or roller advancing fabric under print heads |
| 3 | Ink Supply and Circulation 6 parts | 1× | Supplying and filtering ink to print heads |
| 4 | Pre-Heating Zone 4 parts | 1× | Pre-heating and curing inks on fabric |
| 5 | Dryer Section 5 parts | 1× | Thermal dryer setting dyes into fibers |
| 6 | RIP and Control Station 6 parts | 1× | Computer and software for image processing |
| 7 | Registration and Alignment 3 parts | 1× | Optical sensors ensuring color alignment |
| 8 | Machine Frame and Support 4 parts | 1× | Rigid support for all mechanical components |
Diagrams & photos


3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Digital Textile Printer
8 top-level lines · 50 rows shown · 1,093 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Print Head Assembly 8 parts | digital-textile-printer-print-head-assembly | 1× | 1 | 1,035 | assembly |
| 1.1 | Cyan Print Head | digital-textile-printer-cyan-head | 1× | 1 | · | part |
| 1.2 | Magenta Print Head | digital-textile-printer-magenta-head | 1× | 1 | · | part |
| 1.3 | Yellow Print Head | digital-textile-printer-yellow-head | 1× | 1 | · | part |
| 1.4 | Black Print Head | digital-textile-printer-black-head | 1× | 1 | · | part |
| 1.5 | White Print Head | digital-textile-printer-white-head | 1× | 1 | · | part |
| 1.6 | Print Head Carriage | digital-textile-printer-head-carriage | 1× | 1 | · | part |
| 1.7 | Printhead Nozzle Orifice | digital-textile-printer-head-nozzles | 1024× | 1,024 | · | part |
| 1.8 | Ink Damper | digital-textile-printer-head-dampers | 5× | 5 | · | part |
| 2 | Fabric Transport System 6 parts | digital-textile-printer-fabric-transport-system | 1× | 1 | 10 | assembly |
| 2.1 | Transport Belt | digital-textile-printer-transport-belt | 1× | 1 | · | part |
| 2.2 | Transport Drive Motor | digital-textile-printer-belt-drive-motor | 1× | 1 | · | part |
| 2.3 | Belt Tensioner | digital-textile-printer-belt-tensioner | 2× | 2 | · | part |
| 2.4 | Pinch Roller | digital-textile-printer-pinch-roller | 1× | 1 | · | part |
| 2.5 | Transport Encoder | digital-textile-printer-encoder | 1× | 1 | · | part |
| 2.6 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 3 | Ink Supply and Circulation 6 parts | digital-textile-printer-ink-circulation-system | 1× | 1 | 9 | assembly |
| 3.1 | Ink Reservoir Tank | digital-textile-printer-ink-reservoir | 4× | 4 | · | part |
| 3.2 | Ink Circulation Pump | digital-textile-printer-ink-pump | 1× | 1 | · | part |
| 3.3 | Ink Pressure Regulator | digital-textile-printer-pressure-regulator | 1× | 1 | · | part |
| 3.4 | Ink Filter | digital-textile-printer-ink-filter | 1× | 1 | · | part |
| 3.5 | Ink Supply Tubing | digital-textile-printer-ink-lines | 1× | 1 | · | part |
| 3.6 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 4 | Pre-Heating Zone 4 parts | digital-textile-printer-heating-system | 1× | 1 | 7 | assembly |
| 4.1 | Heating Element | heating-element | 4× | 4 | · | part |
| 4.2 | Heated Pretreatment Roller | digital-textile-printer-heating-roller | 1× | 1 | · | part |
| 4.3 | Temperature Controller | digital-textile-printer-temperature-controller | 1× | 1 | · | part |
| 4.4 | Heat Sensor | digital-textile-printer-heat-sensor | 1× | 1 | · | part |
| 5 | Dryer Section 5 parts | digital-textile-printer-dryer-section | 1× | 1 | 12 | assembly |
| 5.1 | Infrared Heater Element | digital-textile-printer-ir-heating-element | 8× | 8 | · | part |
| 5.2 | Drying Blower Motor | digital-textile-printer-hot-air-blower | 1× | 1 | · | part |
| 5.3 | Drying Chamber | digital-textile-printer-drying-chamber | 1× | 1 | · | part |
| 5.4 | Dryer Temperature Sensor | digital-textile-printer-dryer-temperature-sensor | 1× | 1 | · | part |
| 5.5 | Drying Time Controller | digital-textile-printer-dryer-timer | 1× | 1 | · | part |
| 6 | RIP and Control Station 6 parts | digital-textile-printer-rip-station | 1× | 1 | 7 | assembly |
| 6.1 | Microcontroller | mcu | 1× | 1 | · | part |
| 6.2 | RIP Computer | digital-textile-printer-pc-workstation | 1× | 1 | · | part |
| 6.3 | Touch Screen Interface | digital-textile-printer-touch-screen-hmi | 1× | 1 | · | part |
| 6.4 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 6.5 | Bare PCB | pcb-bare | 2× | 2 | · | part |
| 6.6 | USB Data Interface | digital-textile-printer-usb-interface | 1× | 1 | · | part |
| 7 | Registration and Alignment 3 parts | digital-textile-printer-registration-system | 1× | 1 | 4 | assembly |
| 7.1 | CMOS Image Sensor | image-sensor | 2× | 2 | · | part |
| 7.2 | Registration Micro-Stepper | digital-textile-printer-alignment-motor | 1× | 1 | · | part |
| 7.3 | Alignment LED Light | digital-textile-printer-led-illuminator | 1× | 1 | · | part |
| 8 | Machine Frame and Support 4 parts | digital-textile-printer-frame-structure | 1× | 1 | 9 | assembly |
| 8.1 | Main Frame | digital-textile-printer-main-frame | 1× | 1 | · | part |
| 8.2 | Gantry Rail System | digital-textile-printer-gantry-rails | 1× | 1 | · | part |
| 8.3 | Sheet Metal Panel | sheet-panel | 6× | 6 | · | part |
| 8.4 | Fastener Set | fastener-set | 1× | 1 | · | part |
Something wrong in this list? Report a problem with this BOM.
Related products
same domain, ranked by shared parts Automatic Fabric Cutting Machine
1,695 parts · shares 3 with this page
Fabric Coating Machine
316 parts · shares 3 with this page
FDY Filament Spinning Line
679 parts · shares 3 with this page
 Meltblown Nonwoven Line
933 parts · shares 3 with this page
Mercerizing Range
585 parts · shares 3 with this page
POY Spinning Machine
2,277 parts · shares 3 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇨🇭Rieter
rieter.com ↗
|
Winterthur, CH | Spinning machinery | 10 units | 14–24 wks |
| truetzschler.com ↗ | Mönchengladbach, DE | Textile machinery | 10 units | 14–24 wks |
|
🇧🇪Picanol
picanol.be ↗
|
Ypres, BE | Weaving machines | 10 units | 14–24 wks |
| karlmayer.com ↗ | Obertshausen, DE | Warp knitting machines | 10 units | 14–24 wks |
|
🇨🇭Saurer
saurer.com ↗
|
Arbon, CH | Spinning & embroidery | 10 units | 14–24 wks |
1,248-word article