Stud Welding System
ProductAlso known as: Stud Welding Machine
Overview
Drawn arc stud welding fastens mechanical anchors to structural steel, boilers, shipbuilding, and automotive assemblies. Unlike threaded fasteners, studs are arc-welded in seconds, creating a full-strength metallurgical bond with zero thread stripping or vibration loosening. The arc melts a small pool on the base metal and the stud tip simultaneously; the electromagnet lifts the stud 3–6 mm, drawing a bridge of molten metal. When the timer expires, a heavy spring plunges the stud downward, forging the weld nugget. The ceramic ferrule contains spatter and cooling flux.
One operator with a handheld gun can weld 20–40 studs per hour on flat plate. No skill required, trigger, wait for the beep, remove gun.
How it works
Stud Preparation: The operator selects a ferrule (1/2", 5/8", 3/4") matching stud diameter, and inserts it into the holder on the gun tip. A stud is inserted into the collet chuck, which springs tight. The gun is positioned over the weld location on the base metal, with the ferrule sitting flush.
Arc Initiation: The magnetic clamp is placed nearby on the workpiece, bonding it to the power supply return. The operator pulls the trigger. The timer circuit signals the SCR phase controller to apply full AC voltage to the secondary, and simultaneously energizes the lift solenoid.
The solenoid pulls the stud upward at ~1 m/s. As the gap widens, the voltage across the gap increases, ionizing the air gap into an arc. The arc strikes at 3–6 mm standoff. Current jumps to 100–300 A (limited by the output inductor). The arc heats both the stud tip and the base metal pool to 1500+ °C.
Arc Duration: The timer circuit (set for 200–800 ms, depending on stud size) maintains the arc at constant voltage while current rises at a slow, controlled rate. Large studs (5/8", 3/4") use longer arcs (600–800 ms) to ensure deep fusion; small studs (1/4") use 200–400 ms to avoid overheating.
Plunge and Forge: When the timer expires, the controller de-energizes the solenoid, and the heavy compression spring (k = 15 N/mm) slams the stud downward at ~2 m/s. The stud plunges into the molten pool created by the arc, simultaneously:
- Displacing liquid metal outward (creating the fused nugget)
- Forging (compressing and consolidating) the weld metal
- Extinguishing the arc (metallic contact replaces the arc column)
The ferrule contains the expelled molten spatter, which cools and hardens, leaving a clean weld with minimal smoke.
Cool and Repeat: The operator waits 3–5 seconds for the weld to cool (metallurgical time constant for the nugget), then removes the gun and repeats at the next location.
Ferrule Function
The ceramic ferrule is essential: it surrounds the stud during the arc phase, containing molten spatter and allowing flux (typically rosin from the stud flux coating) to boil off and shield the weld pool. Without a ferrule, spatter scatters across the workpiece and surrounding area.
Ferrules are consumable, typically lasting 10–20 welds before cracking or spalling. Changing ferrules is quick (bayonet or spring clip), but requires the operator to match ferrule diameter to stud diameter. Cross-sized ferrules result in poor containment and excessive spatter.
Arc Voltage and Current Profiles
Typical weld sequence:
- Lift phase (0–50 ms): Stud moving upward, gap widening. Current low (10–50 A), voltage rising.
- Arc burn (100–800 ms): Full arc at 20–30 VAC, current rising from 100 A to peak 300–600 A. Pool heating up.
- Plunge (0–200 ms): Stud accelerating downward. Current peaks as molten metal offers low resistance. Forging occurs.
- Weld solidification (1–5 s): Metallurgical time for fusion to consolidate. Operator holds gun steady, awaiting cool signal.
Longer arc times deposit more heat and produce deeper, broader nuggets. This is necessary for large studs in thin plate (avoid burn-through) and thick sections (ensure adequate fusion). Shorter arcs work for small studs and lightweight fastening.
Stud Materials and Strength
Common stud grades:
- Mild steel (SAE 1020): Low cost, adequate for structural bolting. Tensile ~450 MPa.
- Medium carbon (SAE 1045): Higher strength (~600 MPa). Used in automotive and machinery.
- Stainless 304 or 316: Corrosion-resistant, used in marine and chemical tanks. Slightly higher arc time needed.
- Coated studs (zinc plated, Dacromet): Coating burns off during arc, leaving bare steel stud at the weld. Coating provides corrosion protection on threads.
All grades are compatible with the same gun and power source; only the timer (arc duration) and current setpoint vary.
Penetration and Strength
The weld is a fusion nugget, not a mechanical joint. Full penetration requires sufficient arc energy to melt both the stud tip and a small crater in the base metal. Proper procedure ensures:
- Root fusion: Entire stud tip melted and bonded to base metal crater.
- Nugget size: Diameter 1.5–2× stud diameter (strength proportional to nugget area).
- No cracks: Forging action closes any micro-voids, producing ductile metal.
A properly welded stud is stronger than the stud itself: failure occurs in the stud shank, not at the weld. Tensile strength of the weld often exceeds 90% of base metal.
Power Supply Types
Phase-controlled AC: Most common. An SCR phase-shift circuit (similar to light dimmers) adjusts AC voltage from 0–100%, controlling arc current and weld energy. Simple, reliable, inexpensive. No harmonic distortion.
Capacitor discharge (CD): Stores energy in a large capacitor bank, releasing it as a very fast transient pulse (10–50 µs). Produces shallow, narrow welds with minimal base metal heating. Used for fastening light alloys and thin foil. Requires more sophisticated power supply ($$$).
Modern systems mostly use phase-controlled AC because it's simple and produces consistent welds across stud sizes with a single timer adjustment.
Maintenance and Consumables
Ferrule replacement: Inspect visually before each weld. Spalled or cracked ferrules must be replaced (quick-change clip). Keep a stock of common sizes (1/2", 5/8", 3/4") in the shop.
Collet chuck inspection: The split collet grips the stud. After ~1000 welds, it hardens slightly and grip force drops. If studs slip during lift, replace the collet cartridge (10 USD, 5-minute swap).
Solenoid maintenance: The lifting solenoid is sealed and lubricated for life. If the lift feels sluggish or incomplete, measure solenoid voltage with a multimeter (should read nominal 24 VDC). If voltage is low, the contactor or control circuit needs service.
Transformer thermal: The secondary transformer handles high current pulses. Keep the 60% duty cycle. Continuous use will trip thermal overload (wait 30 min for cooldown). Annual inspection of cooling fins and blower motor ensures adequate heat rejection.
Cable and clamp resistance: Electrical resistance in the cable and clamp circuit affects weld quality. Every 6 months, check:
- Cable insulation for cracks (replace if damaged)
- Clamp jaw for corrosion (polish with emery cloth)
- Stud collet for deformation (replace if loose)
High-resistance circuits reduce arc voltage, making the arc harder to strike and weld quality marginal.
Troubleshooting
Arc won't strike: Dirty base metal or clamp jaw (wire-brush both), low input voltage (check 3-phase supply at 380V), or ferrule bridging the gap (reposition gun or select taller ferrule).
Incomplete fusion (cold weld): Arc duration too short (increase timer setting), low input voltage, or base metal contaminated (grind clean). Test by bending the stud; a good weld bends without fracture.
Excessive spatter: Ferrule worn or spalled (replace), arc current too high (reduce phase-shift), or stud dirty (wipe with cloth).
Stud slips during lift: Collet chuck worn (replace), or stud too small for collet (check size match). Reposition collet on stud (ensure seated fully in chuck).
No lift (solenoid stuck): Low control voltage (check 24 VDC supply and contactor), or solenoid plunger stuck (tap gun firmly to dislodge, then service solenoid).
Comparison to Bolted Fastening
Drawn arc studs are faster than bolts once installed (no threading, no wrench), provide higher reliability (no vibration loosening), and enable full-strength connections in thin plate. However, they require capital equipment and operator training. For one-off assemblies, bolts are more economical. For production (100+ studs per build), welded studs save labor and reject rates.
Stud Welding System parts and their functions
7 top-level parts · 37 parts in total · full bill of materials below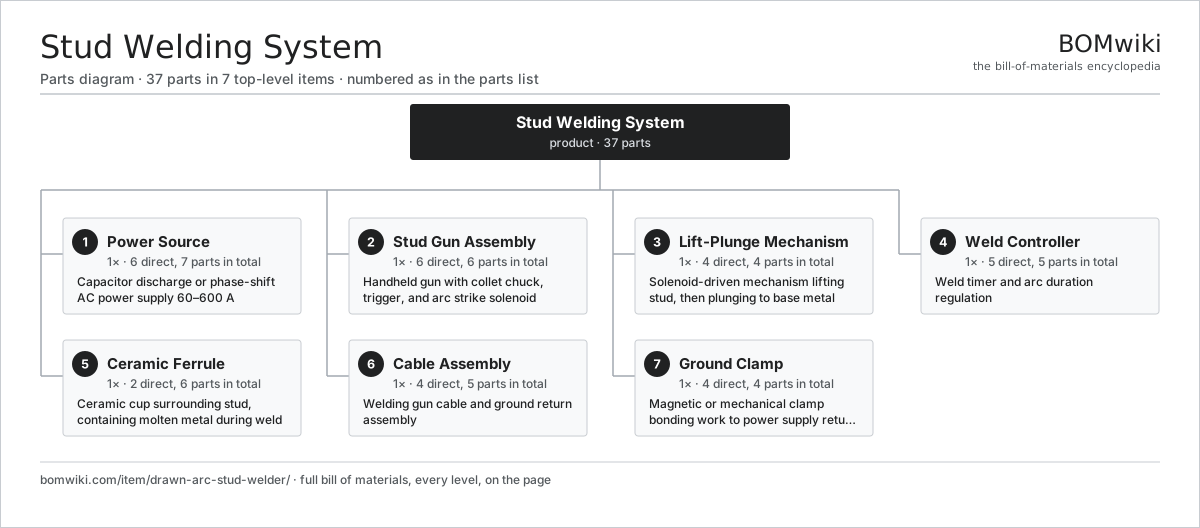
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Power Source 6 parts | 1× | Capacitor discharge or phase-shift AC power supply 60–600 A |
| 2 | Stud Gun Assembly 6 parts | 1× | Handheld gun with collet chuck, trigger, and arc strike solenoid |
| 3 | Lift-Plunge Mechanism 4 parts | 1× | Solenoid-driven mechanism lifting stud, then plunging to base metal |
| 4 | Weld Controller 5 parts | 1× | Weld timer and arc duration regulation |
| 5 | Ceramic Ferrule 2 parts | 1× | Ceramic cup surrounding stud, containing molten metal during weld |
| 6 | Cable Assembly 4 parts | 1× | Welding gun cable and ground return assembly |
| 7 | Ground Clamp 4 parts | 1× | Magnetic or mechanical clamp bonding work to power supply return |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Stud Welding System
7 top-level lines · 38 rows shown · 37 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Power Source 6 parts | drawn-arc-stud-welder-power-source | 1× | 1 | 7 | assembly |
| 1.1 | Input Transformer | drawn-arc-stud-welder-input-transformer | 1× | 1 | · | part |
| 1.2 | Phase Controller | drawn-arc-stud-welder-phase-controller | 1× | 1 | · | part |
| 1.3 | Secondary Transformer | drawn-arc-stud-welder-secondary-transformer | 1× | 1 | · | part |
| 1.4 | Output Choke | drawn-arc-stud-welder-output-choke | 1× | 1 | · | part |
| 1.5 | Control Cabinet | drawn-arc-stud-welder-cabinet | 1× | 1 | · | part |
| 1.6 | Relay | relay | 2× | 2 | · | part |
| 2 | Stud Gun Assembly 6 parts | drawn-arc-stud-welder-stud-gun | 1× | 1 | 6 | assembly |
| 2.1 | Gun Body | drawn-arc-stud-welder-gun-body | 1× | 1 | · | part |
| 2.2 | Lift Solenoid | drawn-arc-stud-welder-gun-solenoid | 1× | 1 | · | part |
| 2.3 | Collet Chuck | drawn-arc-stud-welder-collet-chuck | 1× | 1 | · | part |
| 2.4 | Trigger Switch | drawn-arc-stud-welder-trigger-switch | 1× | 1 | · | part |
| 2.5 | Arc Initiator | drawn-arc-stud-welder-arc-initiator | 1× | 1 | · | part |
| 2.6 | Gun Cable | drawn-arc-stud-welder-cable | 1× | 1 | · | part |
| 3 | Lift-Plunge Mechanism 4 parts | drawn-arc-stud-welder-lift-plunge-mechanism | 1× | 1 | 4 | assembly |
| 3.1 | Lift Solenoid | drawn-arc-stud-welder-lift-solenoid | 1× | 1 | · | part |
| 3.2 | Plunge Spring | drawn-arc-stud-welder-plunge-spring | 1× | 1 | · | part |
| 3.3 | Spring Guide | drawn-arc-stud-welder-spring-guide | 1× | 1 | · | part |
| 3.4 | Ferrule Holder | drawn-arc-stud-welder-ferrule-holder | 1× | 1 | · | part |
| 4 | Weld Controller 5 parts | drawn-arc-stud-welder-weld-controller | 1× | 1 | 5 | assembly |
| 4.1 | Timer Circuit | drawn-arc-stud-welder-timer-circuit | 1× | 1 | · | part |
| 4.2 | Arc Current Sense | drawn-arc-stud-welder-arc-current-sense | 1× | 1 | · | part |
| 4.3 | Contactor Driver | drawn-arc-stud-welder-contactor-driver | 1× | 1 | · | part |
| 4.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 4.5 | Relay | relay | 1× | 1 | · | part |
| 5 | Ceramic Ferrule 2 parts | drawn-arc-stud-welder-ferrule | 1× | 1 | 6 | assembly |
| 5.1 | Ferrule Cup | drawn-arc-stud-welder-ferrule-cup | 5× | 5 | · | part |
| 5.2 | Ferrule Retainer | drawn-arc-stud-welder-ferrule-retainer | 1× | 1 | · | part |
| 6 | Cable Assembly 4 parts | drawn-arc-stud-welder-cable-assembly | 1× | 1 | 5 | assembly |
| 6.1 | Gun Cable | drawn-arc-stud-welder-gun-cable | 1× | 1 | · | part |
| 6.2 | Ground Cable | drawn-arc-stud-welder-ground-cable | 1× | 1 | · | part |
| 6.3 | Connector | connector | 2× | 2 | · | part |
| 6.4 | Cable Guard | drawn-arc-stud-welder-cable-guard | 1× | 1 | · | part |
| 7 | Ground Clamp 4 parts | drawn-arc-stud-welder-ground-clamp | 1× | 1 | 4 | assembly |
| 7.1 | Clamp Magnet | drawn-arc-stud-welder-clamp-magnet | 1× | 1 | · | part |
| 7.2 | Clamp Jaw | drawn-arc-stud-welder-clamp-jaw | 1× | 1 | · | part |
| 7.3 | Clamp Handle | drawn-arc-stud-welder-clamp-handle | 1× | 1 | · | part |
| 7.4 | Connector | connector | 1× | 1 | · | part |
Something wrong in this list? Report a problem with this BOM.
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,468-word article