Flatbed Die Cutter
ProductOverview
Flatbed die cutters are heavy-duty industrial presses that use precisely shaped steel dies to cut complex contours from sheet materials. They are essential in packaging manufacturing, label production, leather working, and foam/rubber fabrication. The machine's hydraulic system delivers controlled force evenly across the entire platen, ensuring clean, burr-free cuts without tearing.
The basic operating cycle is simple: an operator or automatic feeder positions a sheet of material on the lower platen. The upper platen descends, pressing the material against the steel die mounted in the lower chase. The pressure (typically 100-200 bar) forces the die edge through the material cleanly. After dwell time, the upper platen retracts, and a stripper mechanism peels the surrounding matrix waste away from the cut piece, which is then manually or automatically removed.
Die cutting is fundamental to packaging production. Custom dies are fabricated for each product shape, folding cartons, labels, gaskets, leather pieces, and can cost $500 to $5000 depending on complexity. Once a die is set up, a flatbed cutter can run hundreds of identical parts per hour with minimal variation.
How it works
The Hydraulic System is the machine's power source. A 5-7.5 kW motor drives a variable-displacement pump (5-15 cc/rev) that delivers oil at 150-250 bar to the main Hydraulic Cylinder. A PLC controls solenoid pilot valves that route oil to advance or retract the cylinder.
An operator loads a sheet onto the Die Chase, which is mounted on the lower Lower Platen. The custom-shaped steel die is held magnetically or mechanically in the chase, with positioning pins ensuring repeatability to ±0.5 mm.
When the operator presses the start button, the Hydraulic Cylinder extends, pushing the upper platen downward. The Upper Platen (25-50 mm hardened steel) presses the material against the die edge. Pressure builds to the operator's setpoint (typically 100-200 bar for cardboard, up to 250 bar for leather or rubber). The Control System monitors cycle pressure via a Pressure Gauge and holds for a programmed dwell (0.5-2 seconds) to ensure the die fully severs the material.
After dwell, the cylinder retracts. As the upper platen rises, the Stripping Station mechanically or pneumatically separates the waste matrix from the cut piece. Air jets from the Air Manifold (typically 4-6 bar compressed air) blow the waste away, leaving the finished die-cut part on the lower platen for manual removal or transfer to downstream handling.
Materials and Construction
The Frame Structure is fabricated from ductile iron castings or welded steel, engineered to distribute platen forces evenly without deflection. The two vertical columns are tied together with precision-machined crossbeams that resist the lateral shearing forces generated by the uneven cuts.
Both platens are hardened tool steel. The Lower Platen (30-60 mm) is the anvil and is typically ground flat to ±0.1 mm tolerance. The Upper Platen (25-50 mm) is mirror-polished to 0.4 μm Ra to prevent scoring material during descent.
The Die Chase uses either permanent magnets or electromagnets to hold the die. Modern machines favor electromagnets (solenoid-driven) for faster die changeovers, a magnet can be toggled on/off electronically, whereas manual clamps require physical adjustment.
The hydraulic circuit includes a variable-displacement pump that idles at low pressure when not cutting, reducing energy consumption and heat generation. Pressure relief valves protect the system if the operator accidentally engages with a jammed die or foreign object.
Stripper Mechanisms
The Stripper Plate is precision-formed or CNC-drilled to match the die shape. As the upper platen retracts, the stripper rises mechanically (via cam or solenoid linkage) and peels waste away from the cut part. Some machines add air jets; others rely on the stripper's mechanical action alone.
For difficult materials like sticky foam or thin vinyl, air stripping is essential. The Air Manifold has 10-20 precision ports at 0.5-1 mm diameter, directing 4-6 bar compressed air across the stripper surface to blow waste clear.
Operating Parameters
Cutting pressure depends heavily on material thickness and type:
- Cardboard 200-350 gsm: 80-120 bar
- Leather (1-3 mm): 150-200 bar
- Rubber/foam (3-10 mm): 200-250 bar
- Vinyl/plastic sheeting: 50-100 bar
Dwell time (how long the die presses into the material) ranges 0.5-2 seconds. Longer dwell ensures cleaner cuts but reduces throughput. The Control System allows the operator to tune these parameters and save recipes for repeat jobs.
Die Fabrication
Dies are fabricated from hardened tool steel (60-62 HRC) or composite bimetal (hardened steel edge on ductile-iron body). The die edge must be razor-sharp and precisely ground to the desired shape. Dies for simple shapes (rectangles, circles) cost $500-$1500. Complex multi-cut dies with internal windows and notches can exceed $5000.
Die life depends on material abrasiveness. Cutting 100,000 cardboard parts is typical. Cutting 50,000 leather pieces or 10,000 rubber gaskets is more realistic before the die edge dulls enough to require re-sharpening.
Variants
Small tabletop cutting machines operate at 50-100 bar and are suited to label cutting or light foam. Production-class flatbed cutters run 150-250 bar and process 400-800 pieces/hour. Some machines add inline folding or creasing heads to the lower platen, allowing post-cut bending in one pass.
Rotary cutters (cylindrical dies on roller machines) are faster (1000-2000 pcs/hour) but require curved dies and are limited to simpler shapes. Flatbeds remain dominant for complex, irregular geometries because the die can be any shape a tool maker can forge.
Flatbed Die Cutter parts and their functions
7 top-level parts · 50 parts in total · full bill of materials below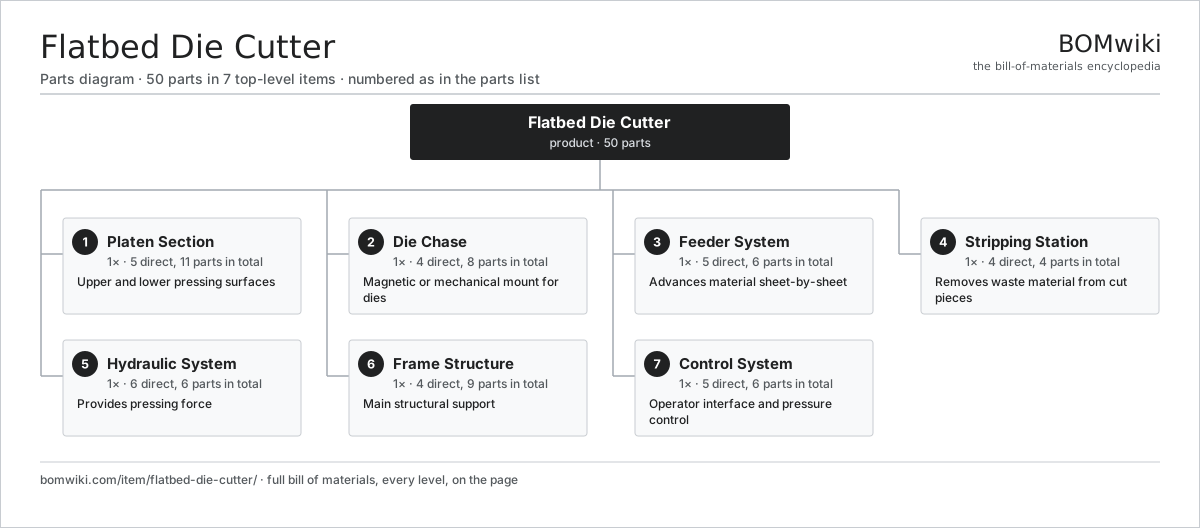
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Platen Section 5 parts | 1× | Upper and lower pressing surfaces |
| 2 | Die Chase 4 parts | 1× | Magnetic or mechanical mount for dies |
| 3 | Feeder System 5 parts | 1× | Advances material sheet-by-sheet |
| 4 | Stripping Station 4 parts | 1× | Removes waste material from cut pieces |
| 5 | Hydraulic System 6 parts | 1× | Provides pressing force |
| 6 | Frame Structure 4 parts | 1× | Main structural support |
| 7 | Control System 5 parts | 1× | Operator interface and pressure control |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Flatbed Die Cutter
7 top-level lines · 40 rows shown · 50 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Platen Section 5 parts | flatbed-die-cutter-platen-section | 1× | 1 | 11 | assembly |
| 1.1 | Upper Platen | flatbed-die-cutter-upper-platen | 1× | 1 | · | part |
| 1.2 | Lower Platen | flatbed-die-cutter-lower-platen | 1× | 1 | · | part |
| 1.3 | Guide Post | flatbed-die-cutter-platen-guide-post | 4× | 4 | · | part |
| 1.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 1.5 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 2 | Die Chase 4 parts | flatbed-die-cutter-die-chase | 1× | 1 | 8 | assembly |
| 2.1 | Magnet Plate | flatbed-die-cutter-magnet-plate | 1× | 1 | · | part |
| 2.2 | Chase Backing Plate | flatbed-die-cutter-chase-backing | 1× | 1 | · | part |
| 2.3 | Chase Rail | flatbed-die-cutter-chase-rail | 2× | 2 | · | part |
| 2.4 | Die Locator Pin | flatbed-die-cutter-die-locator-pin | 4× | 4 | · | part |
| 3 | Feeder System 5 parts | flatbed-die-cutter-feeder | 1× | 1 | 6 | assembly |
| 3.1 | Feed Vacuum Pump | flatbed-die-cutter-feed-vacuum-pump | 1× | 1 | · | part |
| 3.2 | Separator Finger | flatbed-die-cutter-separator-finger | 1× | 1 | · | part |
| 3.3 | Feed Conveyor | flatbed-die-cutter-feed-conveyor | 1× | 1 | · | part |
| 3.4 | Feed Drive Motor | flatbed-die-cutter-feed-motor | 1× | 1 | · | part |
| 3.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 4 | Stripping Station 4 parts | flatbed-die-cutter-stripping-station | 1× | 1 | 4 | assembly |
| 4.1 | Stripper Plate | flatbed-die-cutter-stripper-plate | 1× | 1 | · | part |
| 4.2 | Air Manifold | flatbed-die-cutter-stripper-air-manifold | 1× | 1 | · | part |
| 4.3 | Stripper Lift Rod | flatbed-die-cutter-stripper-lift-rod | 1× | 1 | · | part |
| 4.4 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 5 | Hydraulic System 6 parts | flatbed-die-cutter-hydraulic-system | 1× | 1 | 6 | assembly |
| 5.1 | Hydraulic Pump | flatbed-die-cutter-hydraulic-pump | 1× | 1 | · | part |
| 5.2 | Relief Valve | flatbed-die-cutter-pressure-relief-valve | 1× | 1 | · | part |
| 5.3 | Directional Valve | flatbed-die-cutter-directional-valve | 1× | 1 | · | part |
| 5.4 | Pilot Valve | flatbed-die-cutter-pilot-valve | 1× | 1 | · | part |
| 5.5 | Hydraulic Cylinder | flatbed-die-cutter-hydraulic-cylinder | 1× | 1 | · | part |
| 5.6 | Accumulator | flatbed-die-cutter-accumulator | 1× | 1 | · | part |
| 6 | Frame Structure 4 parts | flatbed-die-cutter-frame | 1× | 1 | 9 | assembly |
| 6.1 | Frame Column | flatbed-die-cutter-frame-column | 2× | 2 | · | part |
| 6.2 | Crossbeam | flatbed-die-cutter-frame-crossbeam | 2× | 2 | · | part |
| 6.3 | Base Frame | flatbed-die-cutter-frame-base | 1× | 1 | · | part |
| 6.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 7 | Control System 5 parts | flatbed-die-cutter-control-system | 1× | 1 | 6 | assembly |
| 7.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.3 | Pressure Gauge | flatbed-die-cutter-pressure-gauge | 1× | 1 | · | part |
| 7.4 | Relay | relay | 2× | 2 | · | part |
| 7.5 | Bare PCB | pcb-bare | 1× | 1 | · | part |
Something wrong in this list? Report a problem with this BOM.
Related products
same domain, ranked by shared parts Aerosol Filling Machine
119 parts · shares 2 with this page
 Automatic Strapping Machine
251 parts · shares 2 with this page
Case Labeling Machine
120 parts · shares 2 with this page
Channel Letter Bender
196 parts · shares 2 with this page
 Continuous Inkjet Coder
501 parts · shares 2 with this page
Counter-Pressure Filler
519 parts · shares 2 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$3M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| heidelberg.com ↗ | Heidelberg, DE | Printing presses | 10 units | 12–22 wks |
|
🇨🇭Bobst
bobst.com ↗
|
Lausanne, CH | Packaging machinery | 10 units | 12–22 wks |
| koenig-bauer.com ↗ | Würzburg, DE | Printing presses | 10 units | 12–22 wks |
| wuh-group.com ↗ | Lengerich, DE | Flexible packaging machines | 10 units | 12–22 wks |
| markandy.com ↗ | Chesterfield, US | Label presses | 10 units | 12–22 wks |
992-word article