Jewelry Rolling Mill
ProductOverview
A jewelry rolling mill is a fundamental bench machine tool for metal fabrication, reducing sheet thickness and adjusting hardness through controlled plastic deformation. Two hardened steel rollers counter-rotate at low speed (10–40 RPM), compressing sheet metal fed between them. A single pass reduces thickness by 30–50% and work-hardens the metal, increasing tensile strength and decreasing ductility. Multiple passes, interspersed with annealing (heating and slow cooling), progressively thin sheet to desired gauge while maintaining workability.
Rolling mills are found in every jewelry shop, silversmithing studio, and metalworking school. They are used not only for thinning gold, silver, copper, and aluminum sheet, but also for flattening ingots, refining grain structure through work-hardening, and producing uniform thickness for die-cutting or stamping operations.
How it works
The operator places a piece of metal sheet at the front of the frame, just outside the feed guide, which is aligned with the nip (gap) between the roller pair. The roller gap is pre-set using the adjustment system, typically 0.010–0.050 inches depending on sheet thickness and desired reduction.
Turning the hand crank rotates the gearbox input shaft at hand speed (50–100 RPM), which meshes with the output spur gear, reducing speed to 10–40 RPM at the roller shafts. Both rollers rotate in opposite directions (counter-rotating); friction between the rollers and the sheet metal draws the sheet forward into the nip. The sheet is compressed between the upper and lower hardened rollers, reducing thickness by the preset gap.
The operator cranks with steady, even pressure; feed resistance increases as the sheet thins and work-hardens. A 0.1 inch thick sheet of silver typically requires hand force equivalent to 30–50 pounds per inch of sheet width. For heavier reductions, geared hand wheels or motorized drives are used. After one pass, the sheet emerges thinner and harder; the operator exits from the same side (no reversal needed, since rollers are fixed).
For progressive thinning, the operator then resets the adjustment gap 0.002–0.005 inches smaller, reinserts the sheet, and makes another pass. After 2–4 passes, the metal becomes so hard (high tensile strength, low ductility) that further rolling would cause cracking. The sheet is then placed in a kiln or torch-heated to 700–900°C and slow-cooled (annealing), restoring ductility. The annealed sheet is pickled (cleaned in dilute sulfuric acid) to remove oxidation, then returned to the mill for continued rolling.
A typical workflow thinning 0.125 inch gold to 0.010 inch (jewelry foil) requires 8–12 annealing cycles and 30–50 rolling passes, taking 8–16 hours of labor. For commercial production, a shop might dedicate one mill to rough rolling (0.125 to 0.050 inch), a second to medium rolling (0.050 to 0.025 inch), and a third to finish rolling (below 0.025 inch), with annealing ovens stationed between each pair of mills.
Roller Geometry and Surface Finish
The rollers are precision-ground steel cylinders with hardness 58–62 HRC (Rockwell Hardness C), achieved through oil quenching. The working surface (face) must be polished to mirror finish (15–20 microinch Ra) to avoid imprinting scratches onto the sheet. Any defect, a groove, pit, or scale, will be transferred to every sheet passed through. Professional-grade mills are hand-polished with progressively finer abrasives (600–2000 grit) once monthly. Budget mills often have stamped or lightly machined surfaces, visible as subtle pattern artifacts on thin foil.
The bearing journals (ends of the shaft where it sits in the bearing blocks) are precision ground to 0.0005 inch runout and hardened to 50–55 HRC, preventing rapid wear from rolling loads. Journals typically run at 100–300 RPM surface speed, cool despite friction, so oil-lubricated bronze or steel-caged ball bearings suffice.
Adjustment System Precision
The thickness adjustment system is critical; inaccuracy results in uneven sheet thickness (thickness variation ≥0.002 inch across the width), causing edge-curling or tearing. The system uses a precision lead screw (20 TPI, acme thread form) with low backlash; one full turn of the adjustment handwheel moves the upper roller exactly 0.050 inches. A micrometer dial indicator shows roller gap in 0.001 inch increments.
High-end mills employ a zero-backlash nut (spring-loaded acme nut) and dial readout to ±0.001 inch. Budget mills use simple acme nuts that can creep (0.002–0.005 inch variation) under rolling load, requiring frequent re-checking with a feeler gauge during use.
Materials Processed
Gold and silver alloys (10K, 14K, 18K, 22K, sterling silver, fine silver) are the most common. Copper and brass are harder, requiring stronger mills and more frequent annealing. Aluminum sheet is soft and sticky; rollers must be kept dry and waxed to prevent adhesion and tearing. Stainless steel, titanium, and hard brasses approach the limits of hand-crank capability; motorized mills are preferred.
Most metals work-harden progressively, with reduction becoming increasingly difficult after 3–4 passes. Annealing reverses this (recrystallization), but repeated cycles coarsen the grain structure, reducing luster and tensile strength. Optimal practice includes limiting total reduction post-annealing to 60–70% before the next anneal cycle.
Motorized Mills
Bench mills are manually cranked; production mills often use 0.5–2 hp electric motors geared down to 10–40 RPM, with variable-speed drives (VFD or belt pulleys) allowing adjustment for different metals and thicknesses. Motorized mills include automatic shutoff (torque-sensing cutout) if rolling load exceeds safe limits, preventing overload and roller breakage. Capacity scales; a motorized 2-inch roller mill can process 0.5 inch thick copper, while hand mills top out around 0.25 inch aluminum.
Maintenance
Rollers must be cleaned and polished after every 10–20 hours of use to maintain surface finish. Oil film on the rollers (residual from gearbox splash lubrication) should be wiped with a lint-free cloth; any grit or metal dust embedded in that oil will scratch subsequent sheets. Bearing blocks should be inspected quarterly; if bearings become loose (wobble visible in the roller face), the shim stack is adjusted to restore clearance. The gearbox is filled with mineral oil (SAE 30 or equivalent), which should be drained and replaced every 3–5 years or if discolored/contaminated.
Jewelry Rolling Mill parts and their functions
7 top-level parts · 34 parts in total · full bill of materials below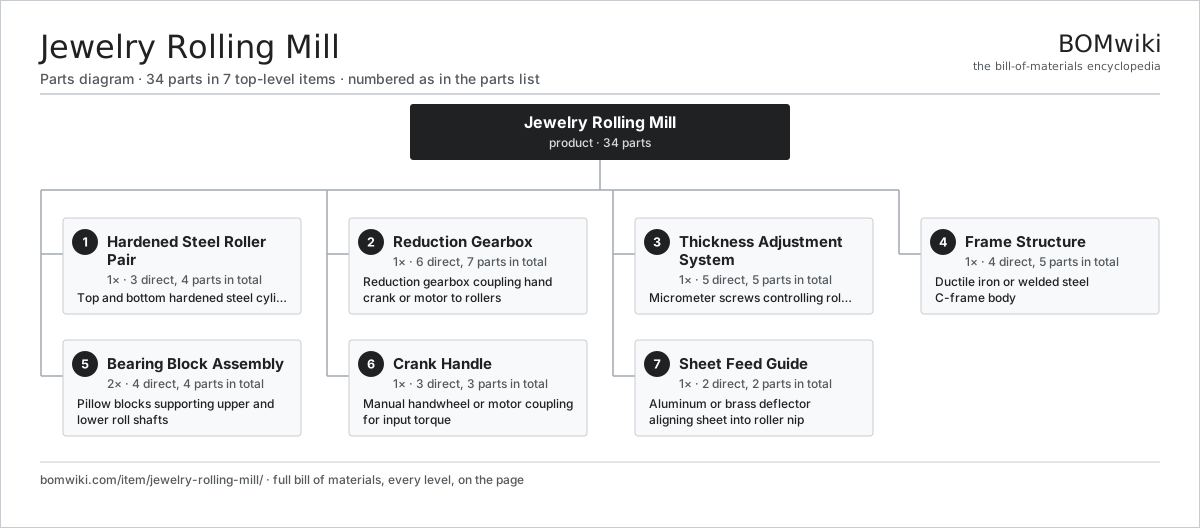
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Hardened Steel Roller Pair 3 parts | 1× | Top and bottom hardened steel cylinders 1–2 inches diameter |
| 2 | Reduction Gearbox 6 parts | 1× | Reduction gearbox coupling hand crank or motor to rollers |
| 3 | Thickness Adjustment System 5 parts | 1× | Micrometer screws controlling roll gap for thickness |
| 4 | Frame Structure 4 parts | 1× | Ductile iron or welded steel C-frame body |
| 5 | Bearing Block Assembly 4 parts | 2× | Pillow blocks supporting upper and lower roll shafts |
| 6 | Crank Handle 3 parts | 1× | Manual handwheel or motor coupling for input torque |
| 7 | Sheet Feed Guide 2 parts | 1× | Aluminum or brass deflector aligning sheet into roller nip |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Jewelry Rolling Mill
7 top-level lines · 34 rows shown · 34 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Hardened Steel Roller Pair 3 parts | jewelry-rolling-mill-roller-pair | 1× | 1 | 4 | assembly |
| 1.1 | Upper Roller Shaft | jewelry-rolling-mill-upper-roller | 1× | 1 | · | part |
| 1.2 | Lower Roller Shaft | jewelry-rolling-mill-lower-roller | 1× | 1 | · | part |
| 1.3 | Roller Journal | jewelry-rolling-mill-roller-journal | 2× | 2 | · | part |
| 2 | Reduction Gearbox 6 parts | jewelry-rolling-mill-gearbox | 1× | 1 | 7 | assembly |
| 2.1 | Gearbox Input Shaft | jewelry-rolling-mill-input-shaft | 1× | 1 | · | part |
| 2.2 | Output Spur Gear | jewelry-rolling-mill-output-gear | 1× | 1 | · | part |
| 2.3 | Gearbox Housing | jewelry-rolling-mill-gear-housing | 1× | 1 | · | part |
| 2.4 | Gearbox Output Shaft | jewelry-rolling-mill-gearbox-shaft | 1× | 1 | · | part |
| 2.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 2.6 | Flexible Coupling | jewelry-rolling-mill-bevel-coupling | 1× | 1 | · | part |
| 3 | Thickness Adjustment System 5 parts | jewelry-rolling-mill-adjustment-system | 1× | 1 | 5 | assembly |
| 3.1 | Adjustment Lead Screw | jewelry-rolling-mill-adj-screw | 1× | 1 | · | part |
| 3.2 | Acme Adjustment Nut | jewelry-rolling-mill-adj-nut | 1× | 1 | · | part |
| 3.3 | Adjustment Handwheel | jewelry-rolling-mill-adj-handle | 1× | 1 | · | part |
| 3.4 | Lock Collar | jewelry-rolling-mill-adj-collar | 1× | 1 | · | part |
| 3.5 | Micrometer Dial | jewelry-rolling-mill-adj-gauge | 1× | 1 | · | part |
| 4 | Frame Structure 4 parts | jewelry-rolling-mill-frame | 1× | 1 | 5 | assembly |
| 4.1 | Frame Base Plate | jewelry-rolling-mill-frame-base | 1× | 1 | · | part |
| 4.2 | Frame Uprights | jewelry-rolling-mill-frame-uprights | 2× | 2 | · | part |
| 4.3 | Frame Top Bar | jewelry-rolling-mill-frame-top | 1× | 1 | · | part |
| 4.4 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 5 | Bearing Block Assembly 4 parts | jewelry-rolling-mill-bearing-block | 2× | 2 | 4 | assembly |
| 5.1 | Pillow Block Housing | jewelry-rolling-mill-bearing-housing | 1× | 2 | · | part |
| 5.2 | Ball Bearing | ball-bearing | 1× | 2 | · | part |
| 5.3 | Bearing Cap | jewelry-rolling-mill-bearing-cap | 1× | 2 | · | part |
| 5.4 | Bearing Shim Stack | jewelry-rolling-mill-bearing-shim | 1× | 2 | · | part |
| 6 | Crank Handle 3 parts | jewelry-rolling-mill-crank-handle | 1× | 1 | 3 | assembly |
| 6.1 | Cast Iron Handwheel | jewelry-rolling-mill-handwheel | 1× | 1 | · | part |
| 6.2 | Crank Shaft | jewelry-rolling-mill-crank-shaft | 1× | 1 | · | part |
| 6.3 | Crank Bearing | jewelry-rolling-mill-crank-bearing | 1× | 1 | · | part |
| 7 | Sheet Feed Guide 2 parts | jewelry-rolling-mill-feed-guide | 1× | 1 | 2 | assembly |
| 7.1 | Guide Plate | jewelry-rolling-mill-guide-plate | 1× | 1 | · | part |
| 7.2 | Guide Bracket | jewelry-rolling-mill-guide-mount | 1× | 1 | · | part |
Something wrong in this list? Report a problem with this BOM.
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,143-word article