Upsetter
ProductOverview
An upsetter (or upset forging machine) is a fully automated metal forging machine that transforms wire or rod stock into headed fasteners, rivets, and similar parts. The machine grips a continuous length of heated wire, holds it stationary, and then rapidly compresses (upsets) the end to form an enlarged head. A single-stroke upsetter may create a simple cylindrical head, while multi-stage machines form complex shapes like bolt heads with flats or hexagons.
Upsetters are the workhorses of fastener manufacturing. A modern fully-automatic upsetter produces 30–120 finished parts per minute, depending on stock diameter and final head geometry. The process is particularly economical for high-volume production because it requires minimal operator intervention, produces minimal scrap, and can be integrated into automated lines with heading, cutting, and heat treatment stations downstream.
How it works
Raw material, a coil of wire or drawn rod, typically 3–25 mm diameter, feeds into the machine. The feed system (a pair of driven rolls) grips the stock and advances it incrementally. The amount advanced per cycle determines the length of the blank before heading.
Just before the heading stroke, an induction heating coil (operating at 1–10 kHz, 10–50 kW) rapidly heats the end section of the wire to 1050–1200 °C in 0.5–3 seconds. This localized heating raises the material above its recrystallization temperature, making it plastic and ready to deform without cracking.
Once heated, the gripper dies (two opposing vertical dies) close around the wire at full force, holding it concentrically and immobile. The header slide (a horizontally-moving platen carrying a shaped cavity die) then accelerates forward at high speed (driven by a flywheel-equipped crank or a hydraulic cylinder). The header die strikes the heated wire end with force (typically 50–500 kN depending on wire size and desired head diameter), rapidly compressing the material into the cavity. This compression, the "upset", concentrates material, thickening the end and forming the head.
The header stroke completes in milliseconds. The impact is cushioned by the inertia flywheel, which absorbs shock. Once the header retracts, the gripper dies open, and the formed part is either sheared off and ejected by gravity, or advanced slightly and cooled before shearing. The cycle time is typically 5–17 milliseconds per part, producing speeds of 60–200 strokes per minute.
Mechanical vs. Hydraulic Drive
Traditional upsetters use a mechanical crank and flywheel. A large AC induction motor (7.5–22 kW) drives the flywheel continuously at 1500 rpm. The flywheel's rotational energy is converted to linear motion via a crankshaft and connecting rod, producing a fixed stroke length and stroke rate. The crank drive is simple, reliable, and inherently energy-efficient because the flywheel stores and releases energy in each cycle.
Modern hybrid or full-hydraulic upsetters replace the mechanical crank with proportional hydraulic cylinders. This allows programmable stroke length and speed, giving flexibility to accommodate different part geometries or materials within a single machine. However, hydraulic drives consume more energy per cycle and require more maintenance.
Most high-speed production machines still use mechanical crank drives because the speed and energy efficiency are unmatched for high-volume fastener production.
Induction Heating
The induction coil is a critical subsystem. For a 10 mm steel wire, the coil must heat the end 10–15 mm in under 2 seconds. Radio-frequency (RF) or medium-frequency (MF) power supplies (solid-state inverters) generate 1–10 kHz excitation, inducing eddy currents in the metallic wire. The resistive heating is extremely localized, only the coil region reaches elevated temperature, while the rest of the wire (clamped in the gripper dies) remains cool.
Modern induction systems use automatic frequency tuning and impedance matching networks to adapt to different wire diameters and materials. Temperature is monitored by infrared pyrometers and logged by the PLC; feedback control adjusts the heating time and power to maintain consistent blank temperature part-to-part.
Gripper Die Design
The gripper dies must hold the wire firmly without deforming it. They typically feature a V-groove profile matching the wire cross-section, or for smaller wires, a simple cylindrical bore. The gripping force is 2000–5000 N, high enough to prevent slipping under the header impact. Gripper dies must resist thermal fatigue (repeated heating cycles) and wear; they are made of tool steel hardened to 40–48 HRC and are often water-cooled to manage die temperature.
Gripper dies are routinely replaced, every 50,000–200,000 cycles depending on wire material and workload. Dies designed for one wire diameter do not work well for another; changeover requires tooling swap, which adds 30–60 minutes of setup time.
Header Die and Cavity Design
The header cavity die shapes the final head geometry. For a simple bolt head, the cavity is a hexagonal prism matching DIN or ISO dimensions. For button heads, the cavity is a shallow dome. Complex geometry (hex-flanged bolts, specialized rivet heads) requires more sophisticated dies with multiple cavity stages or segmented dies.
Cavity depth and diameter determine the maximum upset ratio, the ratio of final head diameter to original wire diameter. For steel, upset ratios of 2–3:1 are typical and economical. Higher ratios require proportionally more material and heating power, making them less cost-effective.
The header die also experiences thermal fatigue. Water cooling (internal passages carrying 40–50 °C cooling fluid) keeps the die face at 80–100 °C during continuous operation. At these temperatures, tool steel die life (before cracking) is typically 100,000–500,000 parts.
Multi-Stage Heading
Complex fastener shapes (e.g., hexagon bolts) often require two or three heading stages. The first stage (primary header) forms a rough enlarged end. The part is then mechanically transferred to a second header position, and a second die cavity refines the shape. A third stage may add a final detail or finish. This multi-station approach trades cycle time for shape complexity, and is common in large-volume automotive fastener lines.
Feed System Precision
The feed roll system must advance stock very precisely, typically ±0.2 mm per cycle, to ensure consistent blank length and therefore consistent upset quality. Overfeeding produces extra-large heads; underfeeding produces undersized heads. Electric stepper motors with integral encoders drive the feed rolls in synchronization with the main crank, ensuring repeatable blank length shot-to-shot.
Integration with Downstream Processes
In a full fastener line, the upsetter output is transferred to a threading machine (for bolts) or directly to a shearing station (for rivets). Heat-treat (case hardening or through hardening) may follow, along with washing, coating, and final inspection. Modern integrated lines are controlled by a central PLC, synchronizing all stations and tracking part genealogy via barcode.
Quality and Traceability
Each cycle is logged: date, time, wire lot, temperature, header load, cycle count. If a part fails in service, the batch can be traced and investigated. Regular sampling (every 100–500 parts) includes dimensional checks, tensile testing, and hardness verification to confirm that heads are meeting strength specifications.
Upsetters achieve high material utilization: scrap is minimal (flash and trim account for only 5–10 % of feed material), making the process economically attractive even for modest production volumes (10,000+ parts per month for a single SKU). The fully automated, repeatable nature of upset forging has made it the dominant technology for mass-produced fasteners worldwide.
Upsetter parts and their functions
8 top-level parts · 46 parts in total · full bill of materials below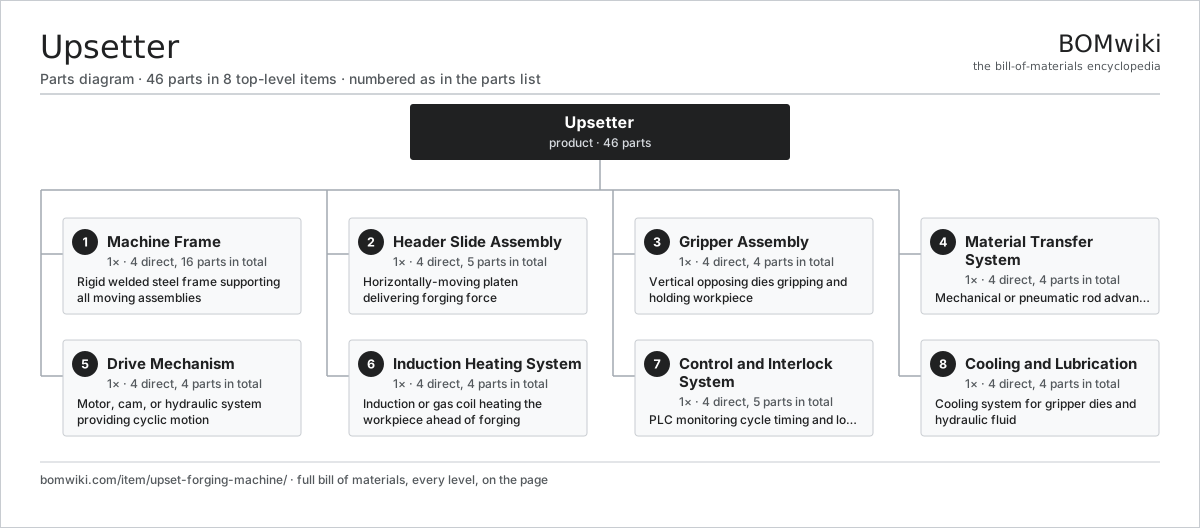
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Machine Frame 4 parts | 1× | Rigid welded steel frame supporting all moving assemblies |
| 2 | Header Slide Assembly 4 parts | 1× | Horizontally-moving platen delivering forging force |
| 3 | Gripper Assembly 4 parts | 1× | Vertical opposing dies gripping and holding workpiece |
| 4 | Material Transfer System 4 parts | 1× | Mechanical or pneumatic rod advance mechanism |
| 5 | Drive Mechanism 4 parts | 1× | Motor, cam, or hydraulic system providing cyclic motion |
| 6 | Induction Heating System 4 parts | 1× | Induction or gas coil heating the workpiece ahead of forging |
| 7 | Control and Interlock System 4 parts | 1× | PLC monitoring cycle timing and load limits |
| 8 | Cooling and Lubrication 4 parts | 1× | Cooling system for gripper dies and hydraulic fluid |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Upsetter
8 top-level lines · 40 rows shown · 46 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Machine Frame 4 parts | upset-forging-machine-frame | 1× | 1 | 16 | assembly |
| 1.1 | Machine Bed | upset-forging-machine-bed | 1× | 1 | · | part |
| 1.2 | Guide Columns | upset-forging-machine-columns | 2× | 2 | · | part |
| 1.3 | Crown Beam | upset-forging-machine-crown | 1× | 1 | · | part |
| 1.4 | Fastener Set | fastener-set | 12× | 12 | · | part |
| 2 | Header Slide Assembly 4 parts | upset-forging-machine-header-slide | 1× | 1 | 5 | assembly |
| 2.1 | Header Platen | upset-forging-machine-header-platen | 1× | 1 | · | part |
| 2.2 | Header Die | upset-forging-machine-header-die | 1× | 1 | · | part |
| 2.3 | Slide Guides | upset-forging-machine-slide-guides | 2× | 2 | · | part |
| 2.4 | Actuator Connection Rod | upset-forging-machine-actuator-connection | 1× | 1 | · | part |
| 3 | Gripper Assembly 4 parts | upset-forging-machine-gripper-dies | 1× | 1 | 4 | assembly |
| 3.1 | Upper Gripper Die | upset-forging-machine-gripper-upper-die | 1× | 1 | · | part |
| 3.2 | Lower Gripper Die | upset-forging-machine-gripper-lower-die | 1× | 1 | · | part |
| 3.3 | Gripper Cylinder | upset-forging-machine-gripper-actuator | 1× | 1 | · | part |
| 3.4 | Die Cooling System | upset-forging-machine-gripper-cooling | 1× | 1 | · | part |
| 4 | Material Transfer System 4 parts | upset-forging-machine-transfer-system | 1× | 1 | 4 | assembly |
| 4.1 | Feed Roll | upset-forging-machine-feed-roll | 1× | 1 | · | part |
| 4.2 | Counter Roll | upset-forging-machine-counter-roll | 1× | 1 | · | part |
| 4.3 | Feed Motor | upset-forging-machine-feed-motor | 1× | 1 | · | part |
| 4.4 | Rod Guide Bushing | upset-forging-machine-rod-guide | 1× | 1 | · | part |
| 5 | Drive Mechanism 4 parts | upset-forging-machine-drive | 1× | 1 | 4 | assembly |
| 5.1 | Main Drive Motor | upset-forging-machine-main-motor | 1× | 1 | · | part |
| 5.2 | Flywheel | upset-forging-machine-flywheel | 1× | 1 | · | part |
| 5.3 | Crankshaft | upset-forging-machine-crankshaft | 1× | 1 | · | part |
| 5.4 | Connecting Rod | upset-forging-machine-connecting-rod | 1× | 1 | · | part |
| 6 | Induction Heating System 4 parts | upset-forging-machine-heating | 1× | 1 | 4 | assembly |
| 6.1 | Induction Coil | upset-forging-machine-coil | 1× | 1 | · | part |
| 6.2 | RF Power Supply | upset-forging-machine-power-supply | 1× | 1 | · | part |
| 6.3 | Matching Capacitor Bank | upset-forging-machine-coil-capacitor | 1× | 1 | · | part |
| 6.4 | Coil Cooling Pump | upset-forging-machine-cooling-pump | 1× | 1 | · | part |
| 7 | Control and Interlock System 4 parts | upset-forging-machine-control | 1× | 1 | 5 | assembly |
| 7.1 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.2 | Header Load Cell | upset-forging-machine-load-cell | 1× | 1 | · | part |
| 7.3 | Position Sensors | upset-forging-machine-proximity-sensors | 2× | 2 | · | part |
| 7.4 | Emergency Stop Circuit | upset-forging-machine-emergency-stop | 1× | 1 | · | part |
| 8 | Cooling and Lubrication 4 parts | upset-forging-machine-cooling | 1× | 1 | 4 | assembly |
| 8.1 | Coolant Pump | upset-forging-machine-coolant-pump | 1× | 1 | · | part |
| 8.2 | Coolant Filter | upset-forging-machine-coolant-filter | 1× | 1 | · | part |
| 8.3 | Cooling Fan | upset-forging-machine-fan | 1× | 1 | · | part |
| 8.4 | Air Filter | upset-forging-machine-air-filter | 1× | 1 | · | part |
Something wrong in this list? Report a problem with this BOM.
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,229-word article