Vinyl Cutting Lathe
ProductOverview
A vinyl cutting lathe is a specialized machine that converts electrical audio signals into physical grooves cut into a lacquer master disc. Unlike a record player, which reads grooves, a lathe cuts them at high precision, making the master from which all commercial vinyl records are eventually manufactured. The master cut on a lathe becomes the source for electroplating: a nickel electroplate is grown on the lacquer master to create a stamper, which then presses thousands of vinyl records.
The core mechanism is deceptively simple: a rotating platter holds a blank lacquer disc, a heated diamond or sapphire stylus is lowered onto the spinning disc, and an amplified audio signal vibrates the stylus side-to-side (left-right) and up-and-down (vertical), carving a spiral groove from the outer edge toward the center. A Feedback Stylus System monitors the groove in real-time to prevent over-modulation.
How it works
The operator mounts a blank lacquer disc on the Rotating Platter, which spins at a precise RPM (33⅓ for LPs, 45 for singles, 78 for classical). Speed is maintained by a Drive Motor controlled by a Speed Controller that monitors actual platter speed via a Speed Encoder, ensuring constant angular velocity (or sometimes linear velocity, depending on desired groove pitch).
Audio enters the Audio Input and EQ Stage, where it passes through a Input Preamp and a Equalization Network that applies the RIAA (Recording Industry Association of America) de-emphasis curve. This curve compensates for groove physics: low frequencies take up more space (larger groove amplitude) and would make the groove too wide; the RIAA curve reduces bass energy during cutting. When a record is played back with an RIAA phono preamp, the bass is restored, and the listener hears the intended mix. A Low-Pass Filter removes ultrasonic content that could damage the stylus or introduce artifacts.
The Cutting Head Assembly contains the Cutting Stylus, a jewel-tipped (diamond or sapphire) cutter kept at 60–80 °C by a Stylus Heater. This temperature is critical: too cool and the stylus will gouge or chip the brittle lacquer; too hot and the lacquer becomes sticky and drags around the stylus, degrading groove fidelity. The Tracking Force applies a precise tracking force (150–400 grams), keeping the stylus in contact with the lacquer without excessive pressure.
The Lead Screw is a precision ball screw that advances the cutting head radially inward as the platter rotates. If the screw advances 2.5 thousandths of an inch per platter revolution, the grooves will be spaced at approximately 2.5 mils apart (roughly 100 grooves per inch), which is typical for a 33⅓ LP. The Cutting Arm holds the stylus on a low-friction pivot; as the audio signal is amplified by a cutting amplifier (not shown in the BOM, but integrated into the lathe electronics), the arm vibrates side-to-side, modulating the groove walls left and right in proportion to the stereo signal (left channel → left wall, right channel → right wall).
Feedback monitoring
The Feedback Stylus System is critical for quality control. A Feedback Stylus (a conventional playback needle) follows the freshly cut groove, reading back what was just cut. The signal passes through a Phono Preamp phono amplifier and is displayed on a Meter or Oscilloscope Display meter or oscilloscope. The operator monitors levels in real-time: if a peak is approaching the cut limit (beyond which the stylus will skip, causing visible drops in the groove), the operator reduces the Input Level Control input gain. This manual "ride the levels" discipline has become automated on modern lathes with automatic gain control (AGC) circuits.
Groove geometry and modulation limits
The width and depth of a groove are determined by the stylus size and tracking force. A 1-mil diamond stylus cutting into soft lacquer creates a groove roughly 0.002–0.004 inches wide. The amplitude of modulation (side-to-side deflection of the groove wall) is typically 6–20 micrometers (0.0002–0.0008 inches). If modulation exceeds the limit, adjacent groove walls can touch (causing cross-talk and skips during playback) or the stylus can punch through the lacquer base (creating a hole and ruining the master).
The vinyl-cutting-lathe-groove-pitch varies with speed and desired playing time: 33⅓ rpm allows narrower pitch (more grooves per inch) because the stylus travels slower, so less distance is needed to fit the audio; 78 rpm requires wider pitch. Modern lathes often use linear tracking, where the groove pitch is constant regardless of radius, allowing more efficient use of disc space.
RIAA equalization
The RIAA curve is a standardized de-emphasis function applied during cutting. It boosts treble (high frequencies) and cuts bass (low frequencies) by specific amounts: −20 dB at 100 Hz, 0 dB at 1 kHz, +17 dB at 10 kHz (approximately). This prevents bass-heavy music from over-modulating the groove (especially at the center of the disc where space is tightest) while allowing treble to be encoded fully. The Equalization Network implements this curve via passive or active filtering.
Lacquer master vs. vinyl record
The lacquer master is not a vinyl record; it is made of a soft cellulose nitrate or acetate base, which is easily damaged and will degrade over decades. Lacquer masters are permanent originals; they are never played on turntables. Instead, they are electroplated immediately after cutting: a conductive layer is sputtered onto the lacquer, then a nickel stamper is electroformed on top. After inspection, the stamper is separated from the lacquer (destroying the master, but the stamper now contains the groove information). The stamper is what actually presses vinyl records. If more records are needed later, a second nickel stamper must be made from the original metal stamper (called a "mother") if the lacquer master is no longer available.
Direct-to-disc recording
Some recording artists and mastering engineers prefer direct-to-disc recording: instead of recording to tape or digital, the audio is cut directly to a lacquer master in real-time during a live performance or mixing session. This eliminates tape coloration or digital processing and was historically the norm before magnetic tape. Modern direct-to-disc sessions use a lathe interfaced with a computer, allowing precise level automation, multiple takes, and editing before final master commitment. However, the tactile, "no redo" nature of direct-to-disc appeals to engineers seeking organic, vintage-sounding recordings.
Vinyl Cutting Lathe parts and their functions
7 top-level parts · 30 parts in total · full bill of materials below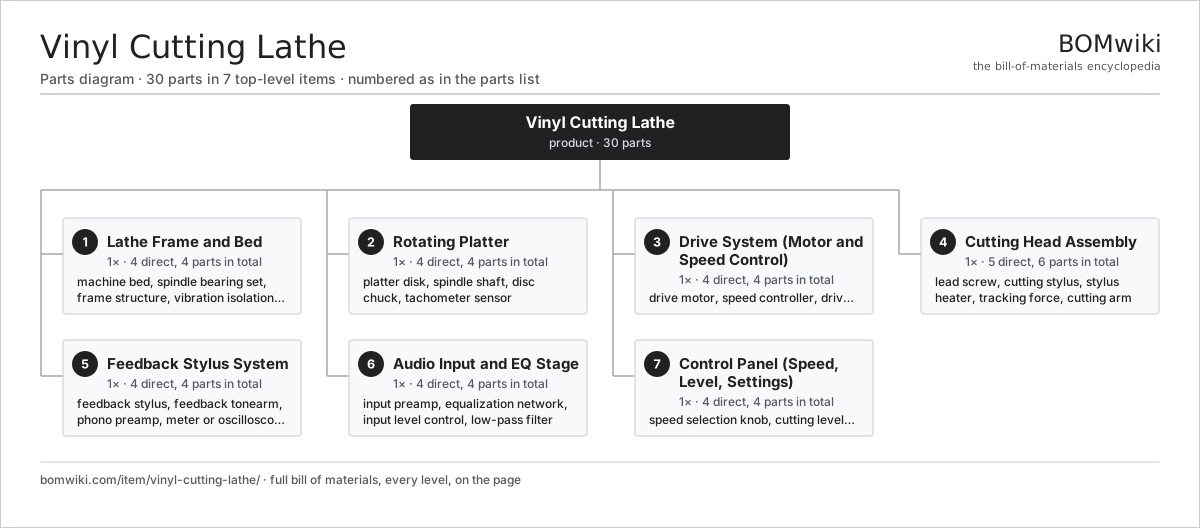
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Lathe Frame and Bed 4 parts | 1× | Precision-cast iron or steel base supporting all cutting mechanisms with minimal vibration. |
| 2 | Rotating Platter 4 parts | 1× | Heavy precision spindle and rotating platter holding the lacquer master disc at exact RPM. |
| 3 | Drive System (Motor and Speed Control) 4 parts | 1× | AC or DC motor with precision speed regulator maintaining constant platter RPM (33⅓, 45, or 78 rpm). |
| 4 | Cutting Head Assembly 5 parts | 1× | Heated cutting stylus mounted on articulated arm with precise lead screw drive for radial traverse. |
| 5 | Feedback Stylus System 4 parts | 1× | Second pickup stylus reading the just-cut groove to monitor groove geometry and modulation in real-time. |
| 6 | Audio Input and EQ Stage 4 parts | 1× | Line-level audio input with RIAA or CCIR curve application (boosting low frequencies to prevent over-modulation). |
| 7 | Control Panel (Speed, Level, Settings) 4 parts | 1× | Operator interface with knobs for speed selection, cutting level, and arm position; optional PC-based control. |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Vinyl Cutting Lathe
7 top-level lines · 38 rows shown · 30 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Lathe Frame and Bed 4 parts | vinyl-cutting-lathe-lathe-body | 1× | 1 | 4 | assembly |
| 1.1 | Machine Bed | vinyl-cutting-lathe-bed | 1× | 1 | · | part |
| 1.2 | Spindle Bearing Set | vinyl-cutting-lathe-spindle-bearings | 1× | 1 | · | part |
| 1.3 | Frame Structure | vinyl-cutting-lathe-frame | 1× | 1 | · | part |
| 1.4 | Vibration Isolation Mount | vinyl-cutting-lathe-vibration-isolation | 1× | 1 | · | part |
| 2 | Rotating Platter 4 parts | vinyl-cutting-lathe-platter | 1× | 1 | 4 | assembly |
| 2.1 | Platter Disk | vinyl-cutting-lathe-platter-disk | 1× | 1 | · | part |
| 2.2 | Spindle Shaft | vinyl-cutting-lathe-spindle-shaft | 1× | 1 | · | part |
| 2.3 | Disc Chuck | vinyl-cutting-lathe-chuck | 1× | 1 | · | part |
| 2.4 | Tachometer Sensor | vinyl-cutting-lathe-tachometer | 1× | 1 | · | part |
| 3 | Drive System (Motor and Speed Control) 4 parts | vinyl-cutting-lathe-drive-system | 1× | 1 | 4 | assembly |
| 3.1 | Drive Motor | vinyl-cutting-lathe-motor | 1× | 1 | · | part |
| 3.2 | Speed Controller | vinyl-cutting-lathe-frequency-converter | 1× | 1 | · | part |
| 3.3 | Drive Belt | vinyl-cutting-lathe-belt-drive | 1× | 1 | · | part |
| 3.4 | Speed Encoder | vinyl-cutting-lathe-speed-encoder | 1× | 1 | · | part |
| 4 | Cutting Head Assembly 5 parts | vinyl-cutting-lathe-cutting-head | 1× | 1 | 6 | assembly |
| 4.1 | Lead Screw | vinyl-cutting-lathe-lead-screw | 1× | 1 | · | part |
| 4.2 | Cutting Stylus 2 parts | vinyl-cutting-lathe-stylus | 1× | 1 | 2 | assembly |
| 4.2.1 | Stylus Tip (Cutting Point) | vinyl-cutting-lathe-stylus-tip | 1× | 1 | · | part |
| 4.2.2 | Stylus Shank | vinyl-cutting-lathe-stylus-shank | 1× | 1 | · | part |
| 4.3 | Stylus Heater | vinyl-cutting-lathe-stylus-heater | 1× | 1 | · | part |
| 4.4 | Tracking Force | vinyl-cutting-lathe-stylus-weight | 1× | 1 | · | part |
| 4.5 | Cutting Arm | vinyl-cutting-lathe-cutting-arm | 1× | 1 | · | part |
| 5 | Feedback Stylus System 4 parts | vinyl-cutting-lathe-feedback-system | 1× | 1 | 4 | assembly |
| 5.1 | Feedback Stylus | vinyl-cutting-lathe-feedback-stylus | 1× | 1 | · | part |
| 5.2 | Feedback Tonearm | vinyl-cutting-lathe-feedback-arm | 1× | 1 | · | part |
| 5.3 | Phono Preamp | vinyl-cutting-lathe-feedback-preamp | 1× | 1 | · | part |
| 5.4 | Meter or Oscilloscope Display | vinyl-cutting-lathe-meter-display | 1× | 1 | · | part |
| 6 | Audio Input and EQ Stage 4 parts | vinyl-cutting-lathe-audio-input-stage | 1× | 1 | 4 | assembly |
| 6.1 | Input Preamp | vinyl-cutting-lathe-input-preamp | 1× | 1 | · | part |
| 6.2 | Equalization Network | vinyl-cutting-lathe-eq-network | 1× | 1 | · | part |
| 6.3 | Input Level Control | vinyl-cutting-lathe-level-control | 1× | 1 | · | part |
| 6.4 | Low-Pass Filter | vinyl-cutting-lathe-low-pass-filter | 1× | 1 | · | part |
| 7 | Control Panel (Speed, Level, Settings) 4 parts | vinyl-cutting-lathe-control-panel | 1× | 1 | 4 | assembly |
| 7.1 | Speed Selection Knob | vinyl-cutting-lathe-speed-knob | 1× | 1 | · | part |
| 7.2 | Cutting Level Potentiometer | vinyl-cutting-lathe-level-knob | 1× | 1 | · | part |
| 7.3 | Start Button | vinyl-cutting-lathe-start-button | 1× | 1 | · | part |
| 7.4 | PC Control Module (Optional) | vinyl-cutting-lathe-optional-pc-interface | 1× | 1 | · | part |
Something wrong in this list? Report a problem with this BOM.
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $50–$3k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇯🇵Sony
sony.com ↗
|
Tokyo, JP | Consumer electronics | 1,000 units | 8–12 wks |
| samsung.com ↗ | Suwon, KR | Electronics & displays | 1,000 units | 8–12 wks |
|
🇺🇸Harman
harman.com ↗
|
Stamford, US | Audio (JBL, AKG) | 1,000 units | 8–12 wks |
|
🇺🇸Bose
bose.com ↗
|
Framingham, US | Audio | 1,000 units | 8–12 wks |
| yamaha.com ↗ | Hamamatsu, JP | Audio & instruments | 1,000 units | 8–12 wks |
1,119-word article