Weld Fume Extractor
ProductOverview
Welding produces airborne metal fumes (iron oxide, manganese oxide, zinc vapor) and gases (ozone from UV arcs, nitrogen oxides from high-current processes). Long-term inhalation causes metal fume fever (acute, reversible) and manganism or silicosis (chronic, irreversible neurological damage). A weld fume extractor captures fumes directly at the source using a flexible gooseneck arm with a capture nozzle, draws them through a multi-stage filter cartridge, and exhausts clean air to ambient or building ductwork.
Portable models (bench-top, foot-print 600 × 600 mm) serve single welding stations. Large shops install centralized ductwork with multiple arms and a single high-capacity fan, serving 5–10 workstations. Regulatory agencies (OSHA, ACGIH) mandate fume extraction in commercial fabrication shops, with maximum time-weighted averages (TWA) of 5 mg/m³ for welding fumes.
How it works
Fume Capture: The welder positions the flexible extraction arm within 6–12 inches of the welding arc. As the arc burns, metal vapors and smoke rise. The capture nozzle (typically 75–150 mm diameter, funnel-shaped) creates a low-pressure zone, drawing fumes into the hood. A properly positioned nozzle captures 85–95% of fumes at the source.
Inlet Air Path: Fumes and air flow through the quick-disconnect hose connector into the main cabinet inlet (100–150 mm diameter). The centrifugal blower pulls approximately 500–2000 CFM, creating negative pressure (200–400 Pa) that sustains the capture.
Filtration: Fume-laden air enters the lower chamber containing the pleated filter cartridge. The cartridge media (10–15 m² surface area) is pleated to maximize area within a compact volume. Fume particles (0.1–5 microns) are captured by mechanical filtration (interception and impaction). Efficiency is 99.7% at design flow rate, removing sub-micron oxides and vapors.
As fumes accumulate on the filter surface, pressure drop increases (measured by the differential pressure gauge). When the gauge reaches the saturation point (typically 400–500 Pa), the pulse-jet cleaning system automatically activates.
Filter Cleaning (Pulse-Jet): The timer circuit energizes the solenoid pulse valve at intervals (every 30 seconds to 5 minutes, adjustable). The valve releases a brief (0.1 second) high-pressure air pulse (6–8 bar) from the compressed air reservoir into the cartridge center. The pulse dislodges accumulated dust and fume particles from the pleats, causing them to fall into the collection hopper below.
This pulse-jet cleaning extends filter life to 6–12 months and prevents complete blockage. Modern automatic systems can detect saturation electronically and pause welding to alert the operator when manual cartridge replacement is needed.
Discharge: Cleaned air exits the filter into the upper discharge chamber, passes through the centrifugal fan, and is exhausted through the discharge outlet. Optional HEPA post-filtering (99.97% at 0.3 micron) can capture remaining trace particles if discharge must meet strict ambient limits (ISO 14644 Class 8, for instance). A silencer reduces discharge noise (typically 80–85 dB).
Automatic Control (Optional): Some units feature arc voltage sensing, which automatically starts the fan when the welder strikes an arc and stops it after a delay (5–30 min adjustable), minimizing energy waste during breaks.
Fume Particle Size and Collection Mechanisms
Welding fumes range from solid particles (iron oxide dust, 1–5 microns) to vapors (zinc, manganese vapor, <0.1 micron). Collection mechanisms:
- Mechanical interception: Large particles (>2 microns) collide with fibers and stick via van der Waals forces.
- Inertial impaction: Particles with momentum cannot follow air streamlines and impact fiber surfaces.
- Diffusion: Very small particles (<0.1 microns) undergo Brownian motion and diffuse to fiber surfaces.
The pleated filter media (1–2 micron nominal) provides efficient multi-stage capture across all fume sizes. Efficiency is rated as:
$$ ext{Efficiency} = 1 - left( rac{ ext{particles out}}{ ext{particles in}} ight)$$
A 99.7% efficient filter passes 0.3% of incoming fumes; a HEPA filter achieves 99.97%. For health compliance, 99.7% is typically adequate if the extraction arm is positioned within 6 inches of the arc.
Filter Media Degradation and Replacement
Filter life is limited by:
Dust cake buildup: Accumulated fume layer increases pressure drop and reduces airflow. Pulse-jet cleaning removes most cake, but some residual buildup remains. After 6–12 months, the cartridge reaches terminal saturation.
Media fiber degeneration: Pleated polyester or composite media can be damaged by:
- Moisture (humid shop air causes fibers to swell and clog)
- Thermal stress (high-temperature steam from splash water vaporizing on hot particles)
- Chemical degradation (acidic or alkaline fumes weakening fiber bonds)
Spatter perforation: Hot spatter from the arc can puncture the filter if the arm nozzle is positioned too close or off-axis. Punctures bypass filtration and defeat the entire system.
Preventive maintenance:
- Position extraction arm 6–12 inches from arc, not touching the work zone
- Replace hood liner sleeves (replaceable inner nozzle) every 3 months to prevent spatter abrasion
- Install a secondary HEPA filter if discharge fumes must be extremely clean
- Store filter cartridges in a dry area; do not use cartridges that have absorbed moisture
Airflow and Static Pressure
Fume extraction requires sufficient airflow to overcome ductwork resistance. For a portable unit with a 1–2 m arm:
- Required capture velocity at nozzle: 50–100 fpm (feet per minute) to overcome thermal updrafts from the hot weld pool
- Typical CFM: 500–1500 CFM (portable units), 1500–4000 CFM (centralized systems)
- Static pressure needed: 200–400 Pa (0.8–1.6" water gauge) for a 1–2 m arm, increasing with ductwork length and number of branches
A 1–2 kW fan producing 1000 CFM develops ~250 Pa static pressure, sufficient for typical portable applications. Longer or more complex ductwork requires higher power or multiple stages.
Centralized vs. Portable Systems
Portable (bench-top):
- Single arm per unit, 500–2000 CFM
- Capital cost USD 2000–8000
- Best for small shops, 1–3 welding stations
- Operator manually positions arm; no automatic capture
- Space-efficient but noisier (no silencer room)
Centralized ductwork:
- Multiple extraction points (5–10 arms) fed by single large fan (3000–5000 CFM, 3–5 kW)
- Capital cost USD 15,000–50,000 (including ductwork installation)
- Quieter (fan is remote, not on welding floor)
- More complex maintenance (ductwork cleaning, balancing airflow to each branch)
- Best for production shops with fixed welding stations
Regulatory Compliance
OSHA PEL (Permissible Exposure Limit):
- General welding fumes: 5 mg/m³ (8-hour TWA)
- Manganese fume (MnO₂): 1 mg/m³ (specific) or 5 mg/m³ (general fume catch-all)
- Chromium VI (stainless welding): 0.005 mg/m³ (Action Level), 0.025 mg/m³ (PEL)
ACGIH TLV (Threshold Limit Value):
- Welding fumes (iron oxide base): 5 mg/m³ (8-hour TWA)
- Manganese: 0.1 mg/m³
- Chromium VI: 0.0002 mg/m³ (inhalable fraction)
Compliance requires:
- Local exhaust ventilation (extraction arm at source)
- Regular air sampling to monitor exposure levels
- Respiratory protection (N95 mask or PAPR) if engineering controls are insufficient
- Worker training on fume hazards and proper arm positioning
Arc Voltage Sensing and Automatic Control
An optional arc voltage sensor can start the fan automatically when welding begins. The sensor detects the arc voltage (15–40 VDC, depending on process) and signals a contactor to energize the fan motor. After the welder stops, a delay timer keeps the fan running for 5–30 minutes to clear residual fumes from the room.
This saves energy (fan only runs during and shortly after welding, not during entire shift) and ensures fume extraction is never forgotten. Manual toggle switches are less reliable; busy shops often forget to turn off the fan, wasting energy, or leave it on all day despite minimal welding.
Maintenance Schedule
Daily: Empty the collection hopper underneath the filter (if manual collection). Inspect the gooseneck arm for blockages or stiff bends.
Weekly: Check the differential pressure gauge. If in the red zone (saturation), plan filter replacement. Visually inspect the discharge hose for leaks or disconnections.
Monthly: Measure the nozzle inner diameter with calipers. If eroded by >10% (from 100 mm to 90 mm), replace or reline the nozzle. Clean the intake flange of surface dust.
Quarterly: Inspect hood liner wear. If visibly pitted or thinned, replace the sleeve. Test the pulse-jet solenoid by manually activating it and confirming air bursts from the cartridge center.
Annually: Replace the main filter cartridge. Inspect motor bearing lubrication (sealed bearings are permanent; if bearing noise increases, bearing replacement is needed). Flush or replace the compressed air tank (drain sediment and water accumulated from compressor moisture).
Every 2 years: Inspect the fan impeller for dust buildup and spatter adhesion. Carefully wipe or brush the impeller blades (do not bend them). Check ductwork for internal obstruction (disconnected sections, crushed areas).
Troubleshooting
No or weak airflow: Cartridge cartridge clogged/saturated (replace), or fan not spinning (check motor power and contactor contacts). Less common: ductwork blockage or disconnection (inspect ductwork from cabinet to discharge).
High noise: Fan impeller rubbing housing (bearing wear, replace bearing cartridge), or silencer inlet clogged (clean or replace silencer media).
Filter saturation too fast (pressure gauge red within days): Heavy welding duty (increase pulse-jet frequency), or leaking ductwork (seal with aluminum tape or clamps). Dirty compressed air source (replace or upgrade air compressor filter).
Captured fumes venting back to shop: Disconnected discharge hose, or inadequate discharge fan power (upgrade motor or reduce capture points if centralized). HEPA post-filter saturated (replace).
Pulse-jet not firing: Solenoid coil not energized (check 24 VDC supply and control relay), or air reservoir depleted (refill from shop compressor). Pulse valve stuck closed (soak in penetrating oil or replace solenoid).
Arm hood liner eroding rapidly: Torch tip too close to nozzle (position 6–12 inches away), or spatter flow too heavy (add splash shield around weld joint). Replace hood liner every 2–3 months if spatter is severe.
Weld Fume Extractor parts and their functions
7 top-level parts · 38 parts in total · full bill of materials below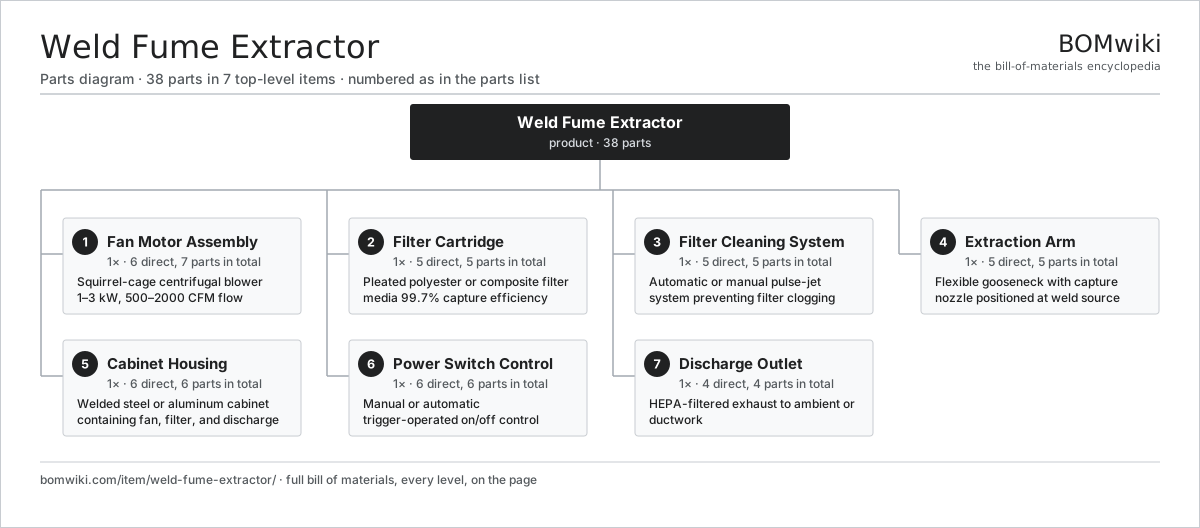
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Fan Motor Assembly 6 parts | 1× | Squirrel-cage centrifugal blower 1–3 kW, 500–2000 CFM flow |
| 2 | Filter Cartridge 5 parts | 1× | Pleated polyester or composite filter media 99.7% capture efficiency |
| 3 | Filter Cleaning System 5 parts | 1× | Automatic or manual pulse-jet system preventing filter clogging |
| 4 | Extraction Arm 5 parts | 1× | Flexible gooseneck with capture nozzle positioned at weld source |
| 5 | Cabinet Housing 6 parts | 1× | Welded steel or aluminum cabinet containing fan, filter, and discharge |
| 6 | Power Switch Control 6 parts | 1× | Manual or automatic trigger-operated on/off control |
| 7 | Discharge Outlet 4 parts | 1× | HEPA-filtered exhaust to ambient or ductwork |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Weld Fume Extractor
7 top-level lines · 44 rows shown · 38 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Fan Motor Assembly 6 parts | weld-fume-extractor-fan-motor | 1× | 1 | 7 | assembly |
| 1.1 | Electric Motor | weld-fume-extractor-electric-motor | 1× | 1 | · | part |
| 1.2 | Fan Impeller | weld-fume-extractor-fan-impeller | 1× | 1 | · | part |
| 1.3 | Motor Bearing | weld-fume-extractor-motor-bearing | 2× | 2 | · | part |
| 1.4 | Fan Housing | weld-fume-extractor-fan-housing | 1× | 1 | · | part |
| 1.5 | Motor Mount | weld-fume-extractor-motor-mount | 1× | 1 | · | part |
| 1.6 | Noise Baffle | weld-fume-extractor-noise-baffle | 1× | 1 | · | part |
| 2 | Filter Cartridge 5 parts | weld-fume-extractor-filter-cartridge | 1× | 1 | 5 | assembly |
| 2.1 | Filter Media | weld-fume-extractor-filter-media | 1× | 1 | · | part |
| 2.2 | Filter Core | weld-fume-extractor-filter-core | 1× | 1 | · | part |
| 2.3 | Filter Gasket | weld-fume-extractor-filter-gasket | 1× | 1 | · | part |
| 2.4 | Filter Cap | weld-fume-extractor-filter-cap | 1× | 1 | · | part |
| 2.5 | Differential Gauge | weld-fume-extractor-differential-gauge | 1× | 1 | · | part |
| 3 | Filter Cleaning System 5 parts | weld-fume-extractor-filter-cleaning | 1× | 1 | 5 | assembly |
| 3.1 | Pulse Valve | weld-fume-extractor-pulse-valve | 1× | 1 | · | part |
| 3.2 | Pulse Timer | weld-fume-extractor-pulse-timer | 1× | 1 | · | part |
| 3.3 | Air Reservoir | weld-fume-extractor-air-reservoir | 1× | 1 | · | part |
| 3.4 | Shake Motor | weld-fume-extractor-filter-shake-motor | 1× | 1 | · | part |
| 3.5 | Pulse Tube | weld-fume-extractor-pulse-tube | 1× | 1 | · | part |
| 4 | Extraction Arm 5 parts | weld-fume-extractor-extraction-arm | 1× | 1 | 5 | assembly |
| 4.1 | Gooseneck | weld-fume-extractor-gooseneck | 1× | 1 | · | part |
| 4.2 | Arm Clamp | weld-fume-extractor-arm-clamp | 1× | 1 | · | part |
| 4.3 | Capture Nozzle | weld-fume-extractor-capture-nozzle | 1× | 1 | · | part |
| 4.4 | Arm Connector | weld-fume-extractor-arm-connector | 1× | 1 | · | part |
| 4.5 | Hood Liner | weld-fume-extractor-hood-liner | 1× | 1 | · | part |
| 5 | Cabinet Housing 6 parts | weld-fume-extractor-housing | 1× | 1 | 6 | assembly |
| 5.1 | Cabinet Body | weld-fume-extractor-cabinet-body | 1× | 1 | · | part |
| 5.2 | Inlet Flange | weld-fume-extractor-inlet-flange | 1× | 1 | · | part |
| 5.3 | Discharge Flange | weld-fume-extractor-discharge-flange | 1× | 1 | · | part |
| 5.4 | Access Door | weld-fume-extractor-access-door | 1× | 1 | · | part |
| 5.5 | Internal Baffle | weld-fume-extractor-internal-baffle | 1× | 1 | · | part |
| 5.6 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 6 | Power Switch Control 6 parts | weld-fume-extractor-power-switch | 1× | 1 | 6 | assembly |
| 6.1 | Toggle Switch | weld-fume-extractor-toggle-switch | 1× | 1 | · | part |
| 6.2 | Foot Pedal | weld-fume-extractor-foot-pedal | 1× | 1 | · | part |
| 6.3 | Arc Trigger Sensor | weld-fume-extractor-arc-trigger | 1× | 1 | · | part |
| 6.4 | Timer Delay | weld-fume-extractor-timer-delay | 1× | 1 | · | part |
| 6.5 | Power Contactor | weld-fume-extractor-contactor | 1× | 1 | · | part |
| 6.6 | Power Supply | power-supply | 1× | 1 | · | part |
| 7 | Discharge Outlet 4 parts | weld-fume-extractor-discharge-outlet | 1× | 1 | 4 | assembly |
| 7.1 | HEPA Post-Filter | weld-fume-extractor-hepa-post-filter | 1× | 1 | · | part |
| 7.2 | Discharge Hose | weld-fume-extractor-discharge-hose | 1× | 1 | · | part |
| 7.3 | Silencer Muffler | weld-fume-extractor-silencer | 1× | 1 | · | part |
| 7.4 | Damper Valve | weld-fume-extractor-damper-valve | 1× | 1 | · | part |
Something wrong in this list? Report a problem with this BOM.
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,802-word article