Wheel Shot Blast Machine
ProductOverview
The wheel shot blast machine is the standard equipment for cleaning castings immediately after removal from sand molds. It uses two or more high-speed rotating steel-wheel impellers to accelerate steel shot (small pellets, 0.7–1.2 mm diameter) to 60–90 m/sec and project them against the casting surface. The impact strips away adhering sand, oxidation scale, and a thin layer of metal (riser stubs), preparing the casting for subsequent heat treatment, machining, or painting.
Modern foundries use wheel blast machines as the primary cleaning tool due to their high throughput (100–300 castings per hour depending on size), low operating cost (shot is recycled indefinitely), and ability to achieve a surface finish suitable for critical components. The process is largely automated, requiring minimal labor and producing castings with minimal inclusions and surface defects, critical for stress-bearing parts.
How it works
A casting is loaded into a rotating basket at the entrance to the blast chamber. The basket, driven by a motor and gearbox, rotates slowly (5–50 rpm, operator-adjustable) while the casting tumbles through the blast zone. Two or more blast wheels, high-speed impellers rotating at 3000–4500 rpm, simultaneously project shot at the casting from multiple angles.
Each blast wheel has a specially shaped acceleration cup that receives steel shot from a gravity-fed hopper and accelerates it to exit velocity via centrifugal force. The shot exits tangentially from the cup at 60–90 m/sec, strikes the casting surface with immense kinetic energy (~200 J per pellet), and either bounces back into the chamber or falls to the floor.
As the casting tumbles and rotates, all external surfaces are progressively exposed to the blast. A casting typically requires 30–120 seconds of continuous blasting, depending on surface oxidation severity and surface finish target. Heavier oxidation (as-cast scale) requires longer exposure; light cleaning requires less time.
Spent shot and loose sand fall to the chamber floor, where they are collected by a shot-recovery system. A rotating scoop hopper feeds material into a bucket elevator that lifts it vertically to overhead return hoppers. From there, shot gravity-flows back to the blast-wheel feed hoppers, creating a closed-loop recycling system.
During this recovery process, the air separator uses a classified air stream to separate heavy steel shot from light sand and oxide dust. The shot is returned to the cycle; dust and fines are directed to a baghouse dust collector, which captures fine particles and maintains factory air quality below occupational exposure limits.
Operating principles
The basket rotation speed is operator-adjustable (typically 5–50 rpm) to optimize surface exposure: slower rotation (5–10 rpm) ensures all surface irregularities receive blast energy; faster rotation (30–50 rpm) reduces cycle time at the cost of potentially missing recessed areas.
The wheel speed (3000–4500 rpm) is also adjustable via VFD. Higher wheel speeds increase shot velocity and kinetic energy, achieving faster surface cleaning but consuming more shot and energy. Wheel speed is typically optimized for cast-iron alloys (3500–4000 rpm) and adjusted downward for softer aluminum or ductile-iron castings to prevent erosion of parent metal.
Cycle time is monitored by a timer in the PLC. When the operator selects "blast," the PLC energizes both wheel motors and the tumble motor. The basket rotates while the wheels spin up to speed. After a preset time (typically 60–120 seconds), the PLC de-energizes the wheels and tumble motor, opening a discharge door (manual or automated) so the operator can unload the cleaned casting.
Shot selection and recycling
Steel shot is standardized (SAE J444: size 170, 210, 230 microns; hardness 40–50 HRC). Over repeated use (typically 200–500 cycles), shot becomes angular or fragmented and loses kinetic efficiency. A foundry periodically removes worn shot from the return hopper using a sieve or magnetic separator, replacing it with fresh stock. The wear rate depends on casting hardness and shot velocity: harder castings and higher speeds increase shot breakage.
The air separator classifies shot by density and size, removing dust and light oxide fragments. A poorly tuned separator either returns shot too early (undersize fragments fail to impact effectively) or loses good shot to the dust stream (wasting material). Foundries adjust the separator's baffle position based on blast results; modern systems include sensors to automate this.
Surface finish and quality
Wheel blasting removes loose oxide scale and adhering sand, yielding a metallic gray surface (Sa 2.5 per ISO 8501-1: 75–100 % of original surface visible). This surface finish is suitable for heat treatment, painting, or machining. For high-precision work, a secondary pass through a second blast machine with smaller shot (SAE 70–100) produces a smoother finish (Ra 1.6–3.2 µm).
Modern foundries measure surface roughness (Ra) using portable profilometers to verify that the cleaning operation meets specification. A typical as-cast surface (Ra 50–100 µm) is reduced to Ra 10–25 µm after standard blasting.
Dust and environmental control
The baghouse removes fine silica dust and iron oxide particles, protecting worker health and meeting OSHA 8-hour TWA limits (<5 mg/m³ for respirable silica). Cartridge filters are pulse-cleaned periodically (every 5–10 minutes) by a solenoid valve injecting compressed air backward, dislodging the dust cake. Collected dust is periodically removed from a collection bin and disposed of according to local regulations (recycling or landfill).
Some foundries feed collected dust back into the sand reclamation circuit or to induction melting as an iron source, reducing landfill volume and recovery costs.
Maintenance and wear
The manganese-steel floor and backing plates experience constant impact from shot ricochet. Manganese steel (8 % Mn alloy) work-hardens under impact, actually becoming harder with each shot strike. However, after 2–5 years of continuous operation, these plates may require replacement.
Wheel impellers also wear from shot contact and occasional stone or casting-gate impact. Impellers are typically replaced every 1–2 years. Regular inspection of wheel bearings is essential; contamination from shot particles can lead to early bearing failure.
Related processes
Castings leave the sand mold with adhering sand and oxidation. The wheel blast machine is the first finishing step. After blasting, castings move to heat treatment (if required), then to grinding or machining to finish critical surfaces, and finally to inspection and assembly. Riser stubs and gates left by the mold are often removed by the blast machine's impact; stubborn gates may require secondary removal (e.g., cutting band saw or oxy-fuel torch).
Wheel Shot Blast Machine parts and their functions
8 top-level parts · 75 parts in total · full bill of materials below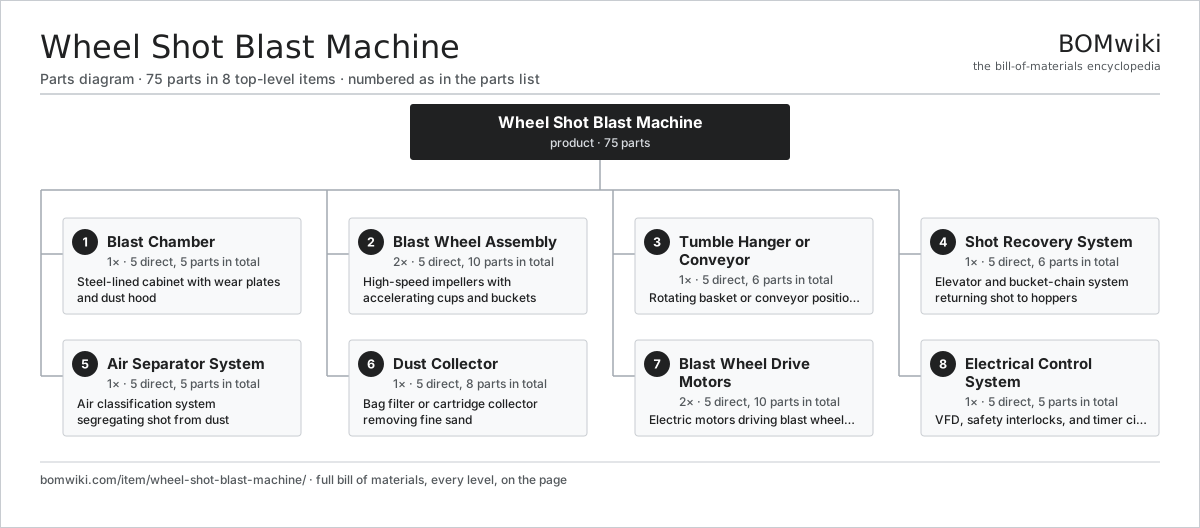
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Blast Chamber 5 parts | 1× | Steel-lined cabinet with wear plates and dust hood |
| 2 | Blast Wheel Assembly 5 parts | 2× | High-speed impellers with accelerating cups and buckets |
| 3 | Tumble Hanger or Conveyor 5 parts | 1× | Rotating basket or conveyor positioning parts in blast path |
| 4 | Shot Recovery System 5 parts | 1× | Elevator and bucket-chain system returning shot to hoppers |
| 5 | Air Separator System 5 parts | 1× | Air classification system segregating shot from dust |
| 6 | Dust Collector 5 parts | 1× | Bag filter or cartridge collector removing fine sand |
| 7 | Blast Wheel Drive Motors 5 parts | 2× | Electric motors driving blast wheels and material handling |
| 8 | Electrical Control System 5 parts | 1× | VFD, safety interlocks, and timer circuits |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Wheel Shot Blast Machine
8 top-level lines · 48 rows shown · 75 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Blast Chamber 5 parts | wheel-shot-blast-machine-blast-chamber | 1× | 1 | 5 | assembly |
| 1.1 | Chamber Steel Frame | wheel-shot-blast-machine-chamber-frame | 1× | 1 | · | part |
| 1.2 | Manganese-Steel Floor | wheel-shot-blast-machine-wear-plate-floor | 1× | 1 | · | part |
| 1.3 | Steel Wear Backing Plates | wheel-shot-blast-machine-wear-plate-walls | 1× | 1 | · | part |
| 1.4 | Access Door with Seal | wheel-shot-blast-machine-access-door | 1× | 1 | · | part |
| 1.5 | Observation Window | wheel-shot-blast-machine-viewing-window | 1× | 1 | · | part |
| 2 | Blast Wheel Assembly 5 parts | wheel-shot-blast-machine-blast-wheels | 2× | 2 | 10 | assembly |
| 2.1 | Blast Wheel Impeller | wheel-shot-blast-machine-wheel-impeller | 2× | 4 | · | part |
| 2.2 | Shot Accelerating Cup | wheel-shot-blast-machine-accelerating-bucket | 1× | 2 | · | part |
| 2.3 | Shot Feed Hopper | wheel-shot-blast-machine-shot-feed-inlet | 1× | 2 | · | part |
| 2.4 | Wheel Bearing Block | wheel-shot-blast-machine-wheel-bearing | 4× | 8 | · | part |
| 2.5 | Wheel Drive Shaft | wheel-shot-blast-machine-wheel-shaft | 2× | 4 | · | part |
| 3 | Tumble Hanger or Conveyor 5 parts | wheel-shot-blast-machine-tumble-hanger | 1× | 1 | 6 | assembly |
| 3.1 | Tumble Basket Frame | wheel-shot-blast-machine-basket-frame | 1× | 1 | · | part |
| 3.2 | Basket Pivot Bearing | wheel-shot-blast-machine-basket-pivot-bearing | 2× | 2 | · | part |
| 3.3 | Tumble Motor | wheel-shot-blast-machine-basket-motor | 1× | 1 | · | part |
| 3.4 | Tumble Speed VFD | wheel-shot-blast-machine-basket-speed-controller | 1× | 1 | · | part |
| 3.5 | Tumble Gearbox | wheel-shot-blast-machine-basket-gearbox | 1× | 1 | · | part |
| 4 | Shot Recovery System 5 parts | wheel-shot-blast-machine-shot-recovery | 1× | 1 | 6 | assembly |
| 4.1 | Floor Scoop Hopper | wheel-shot-blast-machine-scoop-hopper | 1× | 1 | · | part |
| 4.2 | Bucket Elevator | wheel-shot-blast-machine-bucket-elevator | 1× | 1 | · | part |
| 4.3 | Return Shot Hopper | wheel-shot-blast-machine-return-hopper | 2× | 2 | · | part |
| 4.4 | Elevator Drive Motor | wheel-shot-blast-machine-elevator-motor | 1× | 1 | · | part |
| 4.5 | Bucket-Chain Assembly | wheel-shot-blast-machine-bucket-chain | 1× | 1 | · | part |
| 5 | Air Separator System 5 parts | wheel-shot-blast-machine-separator-airflow | 1× | 1 | 5 | assembly |
| 5.1 | Separator Classifier Housing | wheel-shot-blast-machine-separator-housing | 1× | 1 | · | part |
| 5.2 | Classifier Air Fan | wheel-shot-blast-machine-classifier-fan | 1× | 1 | · | part |
| 5.3 | Shot Outlet Port | wheel-shot-blast-machine-shot-outlet | 1× | 1 | · | part |
| 5.4 | Dust Outlet Port | wheel-shot-blast-machine-dust-outlet | 1× | 1 | · | part |
| 5.5 | Separator Baffle Plate | wheel-shot-blast-machine-separator-baffle | 1× | 1 | · | part |
| 6 | Dust Collector 5 parts | wheel-shot-blast-machine-dust-collection | 1× | 1 | 8 | assembly |
| 6.1 | Dust Collector Cabinet | wheel-shot-blast-machine-dust-cabinet | 1× | 1 | · | part |
| 6.2 | Filter Cartridge | wheel-shot-blast-machine-filter-cartridges | 4× | 4 | · | part |
| 6.3 | Pulse Cleaning Valve | wheel-shot-blast-machine-pulse-valve | 1× | 1 | · | part |
| 6.4 | Dust Collection Hopper | wheel-shot-blast-machine-collection-bin | 1× | 1 | · | part |
| 6.5 | Dust Extraction Fan | wheel-shot-blast-machine-dust-motor | 1× | 1 | · | part |
| 7 | Blast Wheel Drive Motors 5 parts | wheel-shot-blast-machine-hoist-motor | 2× | 2 | 10 | assembly |
| 7.1 | Blast Wheel Motor | wheel-shot-blast-machine-wheel-motor | 2× | 4 | · | part |
| 7.2 | Motor Speed Gearbox | wheel-shot-blast-machine-motor-gearbox | 2× | 4 | · | part |
| 7.3 | Motor Vibration Isolator | wheel-shot-blast-machine-motor-base | 2× | 4 | · | part |
| 7.4 | Motor Coupling | wheel-shot-blast-machine-motor-coupling | 2× | 4 | · | part |
| 7.5 | Motor Brake | wheel-shot-blast-machine-motor-brake | 2× | 4 | · | part |
| 8 | Electrical Control System 5 parts | wheel-shot-blast-machine-electrical-controls | 1× | 1 | 5 | assembly |
| 8.1 | Main PLC Controller | wheel-shot-blast-machine-main-plc | 1× | 1 | · | part |
| 8.2 | Wheel Motors VFD | wheel-shot-blast-machine-vfd-wheels | 1× | 1 | · | part |
| 8.3 | Tumble Motor VFD | wheel-shot-blast-machine-vfd-tumble | 1× | 1 | · | part |
| 8.4 | Safety-Rated Relay Module | wheel-shot-blast-machine-safety-relay | 1× | 1 | · | part |
| 8.5 | Control Panel | wheel-shot-blast-machine-start-stop-panel | 1× | 1 | · | part |
Something wrong in this list? Report a problem with this BOM.
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,247-word article