Binder Jetting Printer
ProductOverview
Binder jetting is an additive manufacturing process where a liquid binder (aqueous or organic) is selectively deposited onto a powder bed, bonding particles together without melting. Unlike fusion-based methods (laser sintering, electron-beam melting), binder jetting operates at room temperature, enabling a wider range of powders, ceramics, metals, composites, and lower equipment cost.
The process is also known as Binder Jet (3D Systems term) or BJT. Typical applications include sand molds for metal casting (replacement for lost-foam), ceramic parts (tiles, refractory shapes), metal parts (with infiltration or sintering), and mixed-material composites. Parts are inherently less dense than fully fused alternatives (60–90% bulk density), but the speed and material flexibility make it attractive for prototyping and low-volume production.
How it works
Powder is spread across the build surface by a Recoater Roller, creating a uniform layer 0.05–0.1 mm thick. The Print Bar Assembly contains 128–256 piezoelectric nozzles arranged in a linear array, each capable of ejecting <10 pL droplets at 30 kHz.
As the Build Platform & Stage moves beneath the print bar in a raster pattern (X-axis motion), each nozzle fires on demand according to the sliced CAM data, depositing binder where powder should bond. Droplets penetrate 2–5 particle diameters into the powder, wicking in by capillary action due to the binder's low surface tension.
The Droplet Waveform Generator generates precise waveforms for each nozzle to minimize satellite droplets and ensure consistent penetration depth. The Binder Circulation & Storage keeps binder at 40–80 °C to maintain viscosity within the 2–5 mPa·s range optimal for droplet formation. Lower viscosity increases wetting and penetration; higher viscosity reduces nozzle fouling.
After a layer is complete, the Powder Bed & Recoater lowers the build surface via the Z-stage and spreads a fresh powder layer with the roller. The Vacuum Consolidation Pump applies -0.5 bar suction across the build board, consolidating loose powder and densifying the bonded structure.
This cycle repeats until the part geometry is complete. Unbound powder surrounding the part remains loose and is brushed away; it can often be recycled for the next build.
Binder Chemistry & Curing
Binders are typically aqueous (water-based with suspension stabilizers) or organic (furanic resins, phenolic resins). Water-based binders are safer and cheaper but require longer drying times. Organic binders provide faster strength development but emit VOCs.
After printing, the part is moved to the Post-Print Oven and cured at 60–100 °C for 2–8 hours to evaporate solvent and allow the binder to polymerize or physically set. Thermal cycling also relieves residual stresses from the binder-shrinkage gradients.
For sand castings, cured parts are used directly as molds. For ceramic or metal parts, an additional sintering or infiltration step is required. A ceramic part may be sintered in a kiln at 1100–1400 °C (material-dependent) to develop full density and strength. Metal parts may be infiltrated with liquid metal (e.g., bronze or aluminum) to fill remaining porosity.
Material Flexibility
Binder jetting excels with refractory and difficult-to-melt materials. Silica sand molds for metal casting are the largest market. Zirconia, alumina, and silicon carbide powders produce high-temperature ceramic parts. Tungsten and molybdenum powders, without melting, allow near-net-shape structures.
The binder content is low (typically 5–15% by weight), so the final part composition is dominated by the powder itself. This is attractive for cost-sensitive applications but means post-processing (sintering, infiltration, or impregnation) is often necessary to achieve full strength.
Speed & Economics
Binder jetting is the fastest additive process by throughput. The linear print bar deposits binder across an entire layer width in one pass, unlike raster scanning with a focused laser. Typical build rates are 10–15 cm³/hour, 5–10× faster than laser sintering.
Equipment cost is lower than metal 3D printers. The lack of a laser or electron gun, and operation at room temperature, reduce cooling and optical requirements. A production system costs USD 300 K–800 K, compared to USD 1–3 M for direct metal laser sintering.
Accuracy & Surface Finish
XY resolution is 100–200 µm, determined by nozzle spacing and droplet size. Z resolution (layer thickness) is 0.05–0.1 mm. Surface roughness is 30–100 µm Ra, coarser than laser methods, due to the granular nature of the powder and binder migration into surface layers.
Post-processing (gentle grinding or tumbling) can smooth surfaces. Sand-cast parts intentionally retain surface texture for improved metal-mold contact.
Limitations
Part strength is lower than fully fused structures; green (uncured) parts are fragile. Vertical overhangs are not self-supporting and require powder supports, which are removed post-printing. Complex internal features may trap powder that cannot be fully extracted, leading to voids or contamination if not designed carefully.
Binder Jetting Printer parts and their functions
8 top-level parts · 112 parts in total · full bill of materials below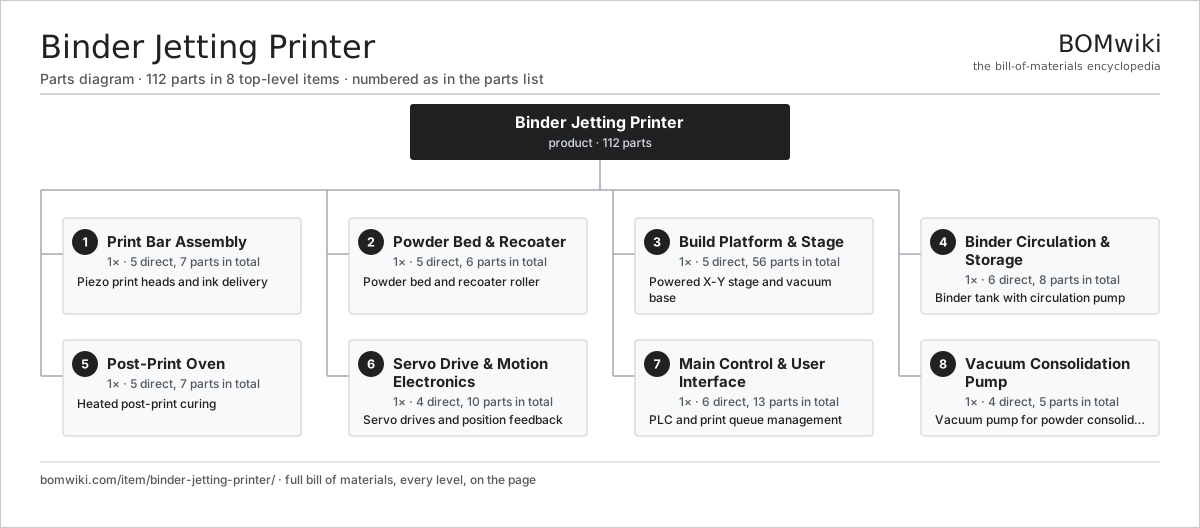
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Print Bar Assembly 5 parts | 1× | Piezo print heads and ink delivery |
| 2 | Powder Bed & Recoater 5 parts | 1× | Powder bed and recoater roller |
| 3 | Build Platform & Stage 5 parts | 1× | Powered X-Y stage and vacuum base |
| 4 | Binder Circulation & Storage 6 parts | 1× | Binder tank with circulation pump |
| 5 | Post-Print Oven 5 parts | 1× | Heated post-print curing |
| 6 | Servo Drive & Motion Electronics 4 parts | 1× | Servo drives and position feedback |
| 7 | Main Control & User Interface 6 parts | 1× | PLC and print queue management |
| 8 | Vacuum Consolidation Pump 4 parts | 1× | Vacuum pump for powder consolidation |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Binder Jetting Printer
8 top-level lines · 52 rows shown · 112 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Print Bar Assembly 5 parts | binder-jetting-printer-print-bar | 1× | 1 | 7 | assembly |
| 1.1 | Piezo Nozzle Array | binder-jetting-printer-nozzle-array | 1× | 1 | · | part |
| 1.2 | Droplet Waveform Generator | binder-jetting-printer-pulse-shaper | 1× | 1 | · | part |
| 1.3 | Connector | connector | 2× | 2 | · | part |
| 1.4 | Fastener Set | fastener-set | 2× | 2 | · | part |
| 1.5 | Heating Element | heating-element | 1× | 1 | · | part |
| 2 | Powder Bed & Recoater 5 parts | binder-jetting-printer-powder-system | 1× | 1 | 6 | assembly |
| 2.1 | Powder Hopper | binder-jetting-printer-powder-hopper | 1× | 1 | · | part |
| 2.2 | Recoater Roller | binder-jetting-printer-roller | 1× | 1 | · | part |
| 2.3 | Stepper Motor | stepper-motor | 1× | 1 | · | part |
| 2.4 | Connector | connector | 1× | 1 | · | part |
| 2.5 | Fastener Set | fastener-set | 2× | 2 | · | part |
| 3 | Build Platform & Stage 5 parts | binder-jetting-printer-build-platform | 1× | 1 | 56 | assembly |
| 3.1 | Servo Motor 4 parts | servo-motor | 2× | 2 | 24 | assembly |
| 3.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 2 | 3 | assembly |
| 3.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 2 | 19 | assembly |
| 3.1.3 | Encoder | encoder | 1× | 2 | · | part |
| 3.1.4 | Motor Housing | motor-housing | 1× | 2 | · | part |
| 3.2 | Encoder | encoder | 2× | 2 | · | part |
| 3.3 | Ball Screw | ball-screw | 2× | 2 | · | part |
| 3.4 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 3.5 | Fastener Set | fastener-set | 3× | 3 | · | part |
| 4 | Binder Circulation & Storage 6 parts | binder-jetting-printer-binder-system | 1× | 1 | 8 | assembly |
| 4.1 | Binder Reservoir | binder-jetting-printer-binder-tank | 1× | 1 | · | part |
| 4.2 | Coolant Pump | coolant-pump | 1× | 1 | · | part |
| 4.3 | Heating Element | heating-element | 1× | 1 | · | part |
| 4.4 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 4.5 | Connector | connector | 3× | 3 | · | part |
| 4.6 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 5 | Post-Print Oven 5 parts | binder-jetting-printer-drying-oven | 1× | 1 | 7 | assembly |
| 5.1 | Heating Element | heating-element | 2× | 2 | · | part |
| 5.2 | Relay | relay | 1× | 1 | · | part |
| 5.3 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 5.4 | Connector | connector | 2× | 2 | · | part |
| 5.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 6 | Servo Drive & Motion Electronics 4 parts | binder-jetting-printer-motion-control | 1× | 1 | 10 | assembly |
| 6.1 | Relay | relay | 2× | 2 | · | part |
| 6.2 | Connector | connector | 4× | 4 | · | part |
| 6.3 | SMD Passive (R/C/L) | smd-passives | 3× | 3 | · | part |
| 6.4 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 7 | Main Control & User Interface 6 parts | binder-jetting-printer-control-panel | 1× | 1 | 13 | assembly |
| 7.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.3 | Power Supply | power-supply | 2× | 2 | · | part |
| 7.4 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.5 | Relay | relay | 2× | 2 | · | part |
| 7.6 | SMD Passive (R/C/L) | smd-passives | 6× | 6 | · | part |
| 8 | Vacuum Consolidation Pump 4 parts | binder-jetting-printer-vacuum-system | 1× | 1 | 5 | assembly |
| 8.1 | Blower Motor | blower-motor | 1× | 1 | · | part |
| 8.2 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 8.3 | Fastener Set | fastener-set | 2× | 2 | · | part |
| 8.4 | Connector | connector | 1× | 1 | · | part |
Something wrong in this list? Report a problem with this BOM.
Related products
same domain, ranked by shared parts Industrial SLA Printer
94 parts · shares 21 with this page
 Industrial FDM Printer
98 parts · shares 14 with this page
Pressure Forming Machine
217 parts · shares 19 with this page
 Material Jetting Printer
129 parts · shares 20 with this page
 Industrial 3D Printer
218 parts · shares 19 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
817-word article