Chain Making Machine
ProductOverview
A chain-making machine is a semi-automated production tool that forms, joins, and spools wire chain at high speed and consistency. The machine feeds wire from a motorized spool, forms it into individual links using precision dies, shears the links to length, positions them for closure or soldering, applies heat to join the seams, and winds the finished chain onto a takeup spool. Chain production that would require hours of skilled hand-labor is accomplished in minutes, making commercial jewelry chain manufacturing economically feasible.
Chain-making machines are found in fine jewelry manufacturers, silver and precious-metal workshops, and artisanal jewelry studios producing branded chains in high volume. A single operator can manage 2–4 machines running in parallel, achieving daily output of 100–500 feet of finished chain depending on link size and complexity.
How it works
The operator loads a spool of wire onto the wire feeder and threads it through a ceramic guide tube leading into the forming die. The operator selects the desired link size (via length preset) and production speed (via speed dial).
Starting the machine, the pinch roller engages and feeds wire into the die set at a controlled rate (determined by the feed motor). The die squeezes the wire, forming it into a coil or loop shape. Simultaneously, a cutting blade shears the formed link to the precise length (e.g., 0.5 inches for a typical round link).
Each cut link falls into a vibratory hopper, which orients and feeds individual links to a soldering station. There, the link seam (open gap) is heated by furnace, induction, or resistance heating, and solder is applied (either pre-positioned or supplied from a molten bath), joining the two ends. A brief cooling phase (air quench or water spray) solidifies the joint.
The finished chain link is immediately drawn onto a takeup spool by a motorized drive. Each link locks into the previous one, forming continuous chain. The machine maintains a steady rhythm: form, cut, solder, link, hundreds of links per hour.
The electronic controller monitors the process, counting links and controlling motor speeds. When the desired chain length is reached (e.g., 18 inches), the controller stops the wire feed, allows the final link to solder and cool, then halts the takeup motor. The finished chain is cut from the takeup spool and packaged.
Wire Feeding System
The wire feeder must deliver wire at precisely controlled speed (0.5–3 inches per second typical). A pinch roller (driven by a stepper or DC motor) grips the wire between itself and a stationary guide, advancing it like a printer feed mechanism.
The tension brake (magnetic or friction) maintains constant tension (5–20 pounds force) on the incoming wire spool, preventing slack or excessive pull. A breakage sensor monitors the wire; if it breaks mid-production, the machine halts and sounds an alarm.
Forming Dies and Link Geometry
The die set is precision-machined with a cavity matching the desired link shape. Dies are interchangeable; a round-link die produces circular loops, while a curb-link die produces flatter, interlocking ovals. The cavity is shallow (0.1–0.2 inches deep), just enough to form the link profile without excessive wire distortion.
As the wire is fed into the die and the die closes, the wire is bent into the cavity shape. Opening the die and retracting, a blade simultaneously shears the formed link at a preset length (determined by a mechanical stop). The link falls free and is immediately collected by the hopper.
Link size ranges from tiny (0.25 inch diameter) for delicate chains to large (1+ inch) for chunky statement pieces. Die changes typically take 10–20 minutes, making mid-production die swaps feasible for small batch runs.
Soldering Station and Joint Quality
The soldering station is the critical link (pun intended) between raw links and finished chain. Most production machines use one of three approaches:
Furnace soldering: Links pass through a small electric furnace (500–800°C) where they are heated and solder is applied from a molten bath or hand-applied as a pre-positioned pellet. A cooling zone with air quench or water spray rapidly cools the joint. This is simple but slower (furnace transit time limits speed).
Induction heating: An induction coil at 50–200 kHz heats only the joint area (the link seam) to soldering temperature in 0.5–2 seconds. Solder is pre-positioned or automatically applied. Fast (milliseconds) but requires careful coil design to focus heat on the seam without overheating adjacent metal.
Resistance welding: Two electrodes clamp the link seam and high current flows through the joint, generating resistive heat that melts and fuses the metal (no solder required). Fast and produces very strong joints but requires precise electrode alignment and current control.
Most manual and small-production machines use furnace soldering. Industrial high-speed (>100 links/min) machines use induction or resistance.
The joint must be strong (exceed the ultimate tensile strength of the wire in normal wear) and smooth (no drips or rough spots catching on fingers). Solder composition is critical: silver-based solders (45–80% Ag) are standard for jewelry (bright, strong, good color match); gold solders are used for gold chain (expensive but color-matched); base-metal solders (tin-lead or cadmium-containing) are avoided due to weakness and color mismatch.
Link Assembly and Orientation
The vibratory hopper ensures links are presented to the soldering station in the correct orientation (seam facing a specific direction for soldering). A small orienter mechanism (often a mechanical escapement) controls feed rate and alignment, preventing jamming or overlap.
For closed links (already soldered from a previous production run), they can be chained directly; the new link is soldered while interlocked with the previous one, forming continuous chain. For open links (just cut, not yet soldered), each link is soldered individually first, then linked.
Production Parameters and Optimization
Production speed depends on:
- Link size: Smaller links cut faster (less wire to form and feed). Tiny chains (0.25 inch links) achieve 100–200 links/min; large chunky chains (1+ inch) achieve 10–30 links/min.
- Solder cycle time: Furnace soldering is slower (requires several seconds per link); induction is faster (0.5–1 sec).
- Operator setup and die quality: Poor die alignment, dull dies, or incorrect solder temperature reduce quality and require rework.
Typical production: a 2 mm wire round-link chain (common size for fine jewelry) runs at 30–50 links/minute, yielding 50–80 feet per 8-hour shift (assuming some setup and die change time).
Quality Control
Links must be:
- Properly formed: Cavity fill is visible; if under-filled, the link is weak and deformed.
- Correct length: Oversized links don't interlock properly; undersized links are too tight and hard to work with.
- Soldered throughout the seam: Cold spots or incomplete solder joints are weak and may break in shipping or use.
- Smooth surface: Solder drips or rough edges are filed smooth by hand (post-production).
A skilled operator inspects the first 5–10 links from each production run, comparing them to a reference sample. Any deviation (size, solder quality, shape) triggers die adjustment before the full run continues.
Safety and Maintenance
Safety hazards include:
- Hot surfaces: The furnace and soldered links exceed 600°C; hand protection (heat-resistant gloves) is required.
- Moving parts: The cutting blade and die mechanism move at high speed; guards prevent finger contact.
- Wire feed: Long hair or loose clothing can be caught by the pinch roller; operators tie back hair and wear fitted clothing.
Maintenance includes:
- Die inspection: Dies wear; surfaces become scarred or dull. Dies are replaced every 5–10 years or when link quality degrades.
- Solder bath: Solder oxidizes, requiring periodic dross (impurity) removal. Baths are drained and cleaned annually.
- Motor and bearing lubrication: Grease-lubricated bearings are inspected quarterly; oil levels checked in splash-lubricated gearboxes.
- Blade sharpening: Blades dull with use; honing or replacement extends life from 6 months to 2+ years.
Production tumblers and multi-operator shops maintain detailed maintenance logs, scheduling preventive service during slack periods.
Chain Making Machine parts and their functions
7 top-level parts · 36 parts in total · full bill of materials below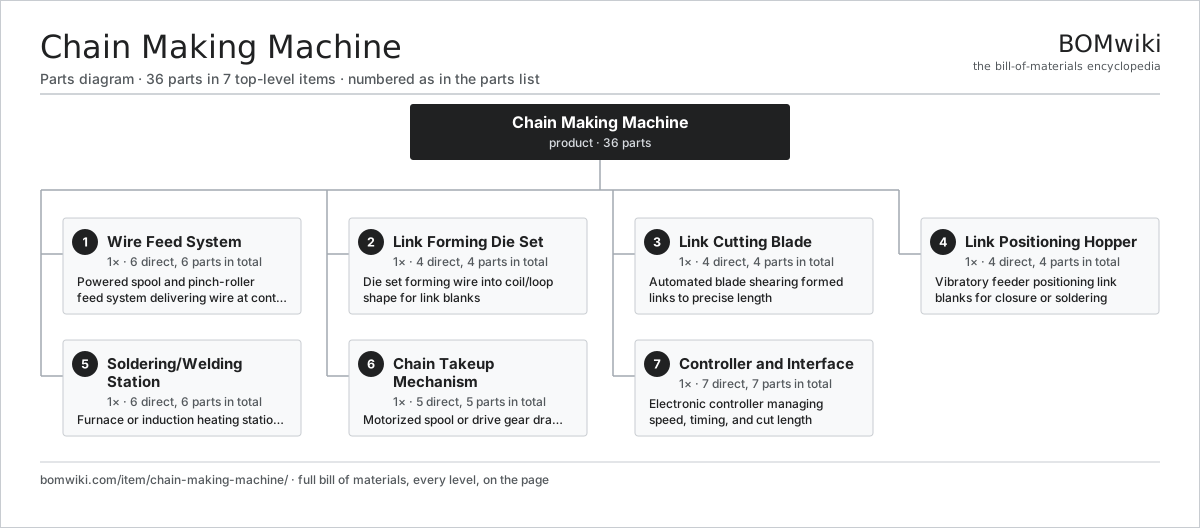
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Wire Feed System 6 parts | 1× | Powered spool and pinch-roller feed system delivering wire at controlled speed |
| 2 | Link Forming Die Set 4 parts | 1× | Die set forming wire into coil/loop shape for link blanks |
| 3 | Link Cutting Blade 4 parts | 1× | Automated blade shearing formed links to precise length |
| 4 | Link Positioning Hopper 4 parts | 1× | Vibratory feeder positioning link blanks for closure or soldering |
| 5 | Soldering/Welding Station 6 parts | 1× | Furnace or induction heating station joining link seams |
| 6 | Chain Takeup Mechanism 5 parts | 1× | Motorized spool or drive gear drawing finished chain onto takeup reel |
| 7 | Controller and Interface 7 parts | 1× | Electronic controller managing speed, timing, and cut length |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Chain Making Machine
7 top-level lines · 43 rows shown · 36 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Wire Feed System 6 parts | chain-making-machine-wire-feeder | 1× | 1 | 6 | assembly |
| 1.1 | Wire Spool Arbor | chain-making-machine-spool-arbor | 1× | 1 | · | part |
| 1.2 | Pinch Roller | chain-making-machine-pinch-roller | 1× | 1 | · | part |
| 1.3 | Feed Motor | chain-making-machine-feed-motor | 1× | 1 | · | part |
| 1.4 | Wire Guide Tube | chain-making-machine-wire-guide | 1× | 1 | · | part |
| 1.5 | Wire Tension Brake | chain-making-machine-tension-brake | 1× | 1 | · | part |
| 1.6 | Wire Breakage Sensor | chain-making-machine-wire-detector | 1× | 1 | · | part |
| 2 | Link Forming Die Set 4 parts | chain-making-machine-forming-die | 1× | 1 | 4 | assembly |
| 2.1 | Upper Forming Die | chain-making-machine-forming-die-upper | 1× | 1 | · | part |
| 2.2 | Lower Forming Die | chain-making-machine-forming-die-lower | 1× | 1 | · | part |
| 2.3 | Die Alignment Dowel | chain-making-machine-die-alignment-pin | 1× | 1 | · | part |
| 2.4 | Die Return Spring | chain-making-machine-die-spring | 1× | 1 | · | part |
| 3 | Link Cutting Blade 4 parts | chain-making-machine-cutting-knife | 1× | 1 | 4 | assembly |
| 3.1 | Cutting Blade | chain-making-machine-knife-blade | 1× | 1 | · | part |
| 3.2 | Blade Drive Arm | chain-making-machine-knife-arm | 1× | 1 | · | part |
| 3.3 | Cut Length Stop | chain-making-machine-knife-stop | 1× | 1 | · | part |
| 3.4 | Blade Safety Guard | chain-making-machine-knife-guard | 1× | 1 | · | part |
| 4 | Link Positioning Hopper 4 parts | chain-making-machine-assembly-hopper | 1× | 1 | 4 | assembly |
| 4.1 | Vibratory Feeder Bowl | chain-making-machine-hopper-bowl | 1× | 1 | · | part |
| 4.2 | Hopper Vibrator Motor | chain-making-machine-hopper-vibrator | 1× | 1 | · | part |
| 4.3 | Link Track | chain-making-machine-hopper-track | 1× | 1 | · | part |
| 4.4 | Link Orienter | chain-making-machine-hopper-orienter | 1× | 1 | · | part |
| 5 | Soldering/Welding Station 6 parts | chain-making-machine-soldering-station | 1× | 1 | 6 | assembly |
| 5.1 | Solder Furnace | chain-making-machine-solder-furnace | 1× | 1 | · | part |
| 5.2 | Solder Bath Pot | chain-making-machine-solder-pot | 1× | 1 | · | part |
| 5.3 | Flux Dispenser | chain-making-machine-solder-flux | 1× | 1 | · | part |
| 5.4 | Cooling Zone | chain-making-machine-solder-cooling-zone | 1× | 1 | · | part |
| 5.5 | Induction Heating Coil | chain-making-machine-induction-coil | 1× | 1 | · | part |
| 5.6 | Induction Power Supply | chain-making-machine-induction-power | 1× | 1 | · | part |
| 6 | Chain Takeup Mechanism 5 parts | chain-making-machine-chain-takeup | 1× | 1 | 5 | assembly |
| 6.1 | Takeup Motor | chain-making-machine-takeup-motor | 1× | 1 | · | part |
| 6.2 | Takeup Drive Wheel | chain-making-machine-takeup-wheel | 1× | 1 | · | part |
| 6.3 | Takeup Spool | chain-making-machine-takeup-spool | 1× | 1 | · | part |
| 6.4 | Takeup Tension Guide | chain-making-machine-takeup-tension | 1× | 1 | · | part |
| 6.5 | Length Counter | chain-making-machine-takeup-counter | 1× | 1 | · | part |
| 7 | Controller and Interface 7 parts | chain-making-machine-control-panel | 1× | 1 | 7 | assembly |
| 7.1 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 7.4 | Speed Control Dial | chain-making-machine-speed-potentiometer | 1× | 1 | · | part |
| 7.5 | Length Input Keypad | chain-making-machine-length-setter | 1× | 1 | · | part |
| 7.6 | LCD Display Panel | chain-making-machine-display | 1× | 1 | · | part |
| 7.7 | Emergency Stop Button | chain-making-machine-emergency-stop | 1× | 1 | · | part |
Something wrong in this list? Report a problem with this BOM.
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,480-word article