Auger Powder Filling Machine
ProductOverview
An auger powder filling machine doses dry product into containers by volume. A rotating screw, the auger, sits in a tube below a hopper and pushes powder down into a funnel and out into the container under it. The dose is set by how far the screw turns: each revolution moves a fixed volume of powder, so the controller counts revolutions to deliver a measured charge. This is how flour, spices, protein powder, drink mixes, detergent, and free-flowing granules are filled into jars, pouches, cans, and tubs at rates from a few containers a minute up to about sixty. The same volumetric principle is shared with a Piston Filling Machine on pastes, while thin liquids are handled by a Liquid Filling Machine with a pump or valve instead of a screw.
The machine is built on a Frame and Guarding that carries a Product Hopper of bulk powder over a Auger Metering Assembly head. The Fill Funnel and Nozzle guides the dose into the container, the Container Handling brings empty containers under it, the Dust Control captures airborne powder and settles the fill, an optional Weigh Feedback system closes the loop on weight, the Control System runs the cycle, and the Pneumatic System drive the air-actuated parts.
How the auger meters
Metering is the core of the machine. The Auger Screw runs inside the Auger Tube, and its pitch and flight count fix the volume of powder carried per turn. A Servo Motor drives the screw through a Helical Gear Pair, and a Revolution Encoder reports exactly how far it has turned. The Revolution Counter in the control compares that count to the recipe target and stops the screw at the right number of revolutions, so a partial turn can trim the dose finely. At the end of the count the Auger Clutch brakes the screw cleanly so powder stops moving at once rather than coasting. The screw runs on two Ball Bearing units with an Oil Seal keeping powder out of the drive, and a Auger Coupling releases the screw and tube for cleaning or for a size change.
Powder will not feed itself reliably, so the Product Hopper keeps it live. The Agitator Paddle on its Agitator Shaft, turned by the Agitator Motor, sweeps the wall of the Hopper Bowl to break bridges and ratholes and to keep a steady column of powder over the screw. A Level Sensor calls for refill before the hopper runs low enough to vary the fill.
Free-flowing and non-free-flowing powders
The behaviour of the powder decides how the machine is set up. Free-flowing products such as sugar, salt, and many granules feed evenly and hold tight dose weights with a simple open-flight screw and a slow agitator. Non-free-flowing powders such as fine flour, cocoa, and some proteins pack, clump, and trap air; they need a tighter agitator speed, sometimes a fluted or compression screw, and slower auger speeds so the charge is consistent. Aerated powders also need the Deck Vibrator and its Settle Deck to deaerate the fill so the settled charge sits below the container neck. Auger profiles are matched to product: an open screw for free flow, a close-pitch screw for fine control of small doses, and a compression screw for light, fluffy material.
Filling the container and controlling dust
When a container reaches the station the Index Gate stops it and the Container Locator squares its mouth under the Fill Funnel and Nozzle. The Container Sensor holds the dose if no container is present, so the machine never fires onto the belt. The powder drops through the Fill Funnel and Nozzle Tube into the container, and at the end of the count the Shutoff Flap, driven by its Flap Cylinder, closes the throat to catch the trailing dribble. Around the nozzle the Dust Hood draws powder that puffs up during the fill into the Extraction Blower and Dust Filter, which keeps the line clean and recovers product.
Volumetric and net-weigh variants
The base machine is volumetric: it trusts the auger count to give the right weight, which works well on uniform free-flowing powder and is the fastest, lowest cost build. When the product varies in density, or when a printed net weight has to be guaranteed, the machine adds the Weigh Feedback feedback. A Load Cell under the Weigh Platform weighs the charge in place and the control trims the next auger count toward the target, while a downstream Checkweigher Belt weighs each filled container in motion and the Reject Arm ejects any that fall outside the band.
Materials and use
Product-contact parts are stainless: the Auger Screw, Auger Tube, and Fill Funnel are 316 stainless, and the Hopper Bowl and Base Weldment are 304 stainless, all built for washdown with tool-free clamps so a line can change product quickly. The Control System runs the cycle from a PLC with recipes set on the HMI Touchscreen, fed by a Power Supply and wired with a Wire Bundle and Connector set. Air-driven moves run off the Pneumatic System through the Valve Bank and Air Cylinder units. Auger fillers are standard equipment in food, nutraceutical, chemical, and household-goods packing, anywhere a dry product has to be dosed into a container by a measured amount.
Auger Powder Filling Machine parts and their functions
9 top-level parts · 102 parts in total · full bill of materials below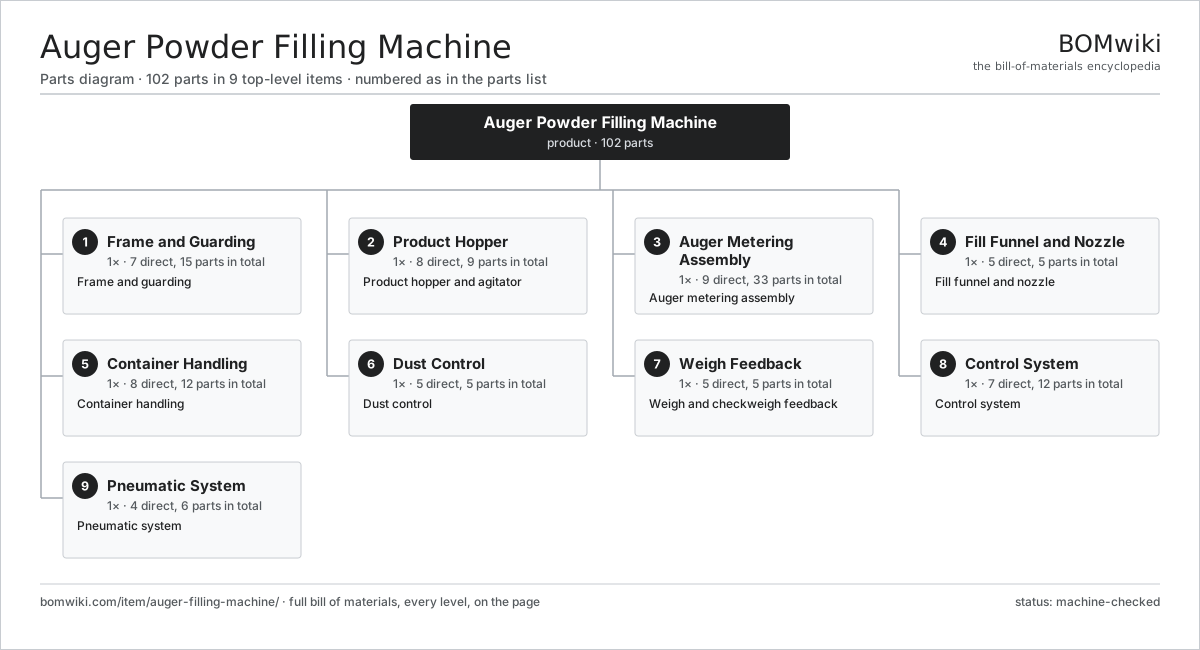
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Frame and Guarding 7 parts | 1× | Frame and guarding |
| 2 | Product Hopper 8 parts | 1× | Product hopper and agitator |
| 3 | Auger Metering Assembly 9 parts | 1× | Auger metering assembly |
| 4 | Fill Funnel and Nozzle 5 parts | 1× | Fill funnel and nozzle |
| 5 | Container Handling 8 parts | 1× | Container handling |
| 6 | Dust Control 5 parts | 1× | Dust control |
| 7 | Weigh Feedback 5 parts | 1× | Weigh and checkweigh feedback |
| 8 | Control System 7 parts | 1× | Control system |
| 9 | Pneumatic System 4 parts | 1× | Pneumatic system |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Auger Powder Filling Machine
9 top-level lines · 71 rows shown · 102 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Frame and Guarding 7 parts | auger-filling-machine-frame | 1× | 1 | 15 | assembly |
| 1.1 | Base Weldment | auger-filling-machine-base-weldment | 1× | 1 | · | part |
| 1.2 | Support Column | auger-filling-machine-column | 1× | 1 | · | part |
| 1.3 | Leveling Foot | auger-filling-machine-leveling-foot | 4× | 4 | · | part |
| 1.4 | Guard Door | auger-filling-machine-guard-door | 2× | 2 | · | part |
| 1.5 | Guard Panel | auger-filling-machine-guard-panel | 4× | 4 | · | part |
| 1.6 | Door Interlock | auger-filling-machine-door-interlock | 2× | 2 | · | part |
| 1.7 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Product Hopper 8 parts | auger-filling-machine-hopper | 1× | 1 | 9 | assembly |
| 2.1 | Hopper Bowl | auger-filling-machine-hopper-bowl | 1× | 1 | · | part |
| 2.2 | Hopper Lid | auger-filling-machine-hopper-lid | 1× | 1 | · | part |
| 2.3 | Agitator Paddle | auger-filling-machine-agitator-paddle | 1× | 1 | · | part |
| 2.4 | Agitator Shaft | auger-filling-machine-agitator-shaft | 1× | 1 | · | part |
| 2.5 | Agitator Motor | auger-filling-machine-agitator-motor | 1× | 1 | · | part |
| 2.6 | Level Sensor | auger-filling-machine-level-sensor | 1× | 1 | · | part |
| 2.7 | Hopper Clamp | auger-filling-machine-hopper-clamp | 1× | 1 | · | part |
| 2.8 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3 | Auger Metering Assembly 9 parts | auger-filling-machine-metering | 1× | 1 | 33 | assembly |
| 3.1 | Auger Screw | auger-filling-machine-auger-screw | 1× | 1 | · | part |
| 3.2 | Auger Tube | auger-filling-machine-auger-tube | 1× | 1 | · | part |
| 3.3 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 3.3.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 3.3.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 3.3.3 | Encoder | encoder | 1× | 1 | · | part |
| 3.3.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 3.4 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 3.5 | Auger Clutch | auger-filling-machine-auger-clutch | 1× | 1 | · | part |
| 3.6 | Auger Coupling | auger-filling-machine-auger-coupling | 1× | 1 | · | part |
| 3.7 | Revolution Encoder | auger-filling-machine-rev-encoder | 1× | 1 | · | part |
| 3.8 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3.9 | Oil Seal | oil-seal | 1× | 1 | · | part |
| 4 | Fill Funnel and Nozzle 5 parts | auger-filling-machine-nozzle | 1× | 1 | 5 | assembly |
| 4.1 | Fill Funnel | auger-filling-machine-fill-funnel | 1× | 1 | · | part |
| 4.2 | Nozzle Tube | auger-filling-machine-nozzle-tube | 1× | 1 | · | part |
| 4.3 | Shutoff Flap | auger-filling-machine-shutoff-flap | 1× | 1 | · | part |
| 4.4 | Flap Cylinder | auger-filling-machine-flap-cylinder | 1× | 1 | · | part |
| 4.5 | Funnel Clamp | auger-filling-machine-funnel-clamp | 1× | 1 | · | part |
| 5 | Container Handling 8 parts | auger-filling-machine-container-handling | 1× | 1 | 12 | assembly |
| 5.1 | Conveyor Belt | auger-filling-machine-conveyor-belt | 1× | 1 | · | part |
| 5.2 | Conveyor Motor | auger-filling-machine-conveyor-motor | 1× | 1 | · | part |
| 5.3 | Index Gate | auger-filling-machine-index-gate | 1× | 1 | · | part |
| 5.4 | Container Locator | auger-filling-machine-container-locator | 1× | 1 | · | part |
| 5.5 | Container Sensor | auger-filling-machine-container-sensor | 1× | 1 | · | part |
| 5.6 | Guide Rail | auger-filling-machine-guide-rail | 2× | 2 | · | part |
| 5.7 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 5.8 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 6 | Dust Control 5 parts | auger-filling-machine-dust-control | 1× | 1 | 5 | assembly |
| 6.1 | Dust Hood | auger-filling-machine-dust-hood | 1× | 1 | · | part |
| 6.2 | Extraction Blower | auger-filling-machine-extract-blower | 1× | 1 | · | part |
| 6.3 | Dust Filter | auger-filling-machine-dust-filter | 1× | 1 | · | part |
| 6.4 | Deck Vibrator | auger-filling-machine-vibrator | 1× | 1 | · | part |
| 6.5 | Settle Deck | auger-filling-machine-vibrator-deck | 1× | 1 | · | part |
| 7 | Weigh Feedback 5 parts | auger-filling-machine-weigh | 1× | 1 | 5 | assembly |
| 7.1 | Load Cell | auger-filling-machine-load-cell | 1× | 1 | · | part |
| 7.2 | Weigh Platform | auger-filling-machine-weigh-platform | 1× | 1 | · | part |
| 7.3 | Checkweigher Belt | auger-filling-machine-checkweigher-belt | 1× | 1 | · | part |
| 7.4 | Reject Arm | auger-filling-machine-reject-arm | 1× | 1 | · | part |
| 7.5 | Weigh Amplifier | auger-filling-machine-weigh-amp | 1× | 1 | · | part |
| 8 | Control System 7 parts | auger-filling-machine-control | 1× | 1 | 12 | assembly |
| 8.1 | PLC | auger-filling-machine-plc | 1× | 1 | · | part |
| 8.2 | HMI Touchscreen | auger-filling-machine-hmi | 1× | 1 | · | part |
| 8.3 | Servo Drive | auger-filling-machine-servo-drive | 1× | 1 | · | part |
| 8.4 | Revolution Counter | auger-filling-machine-rev-counter | 1× | 1 | · | part |
| 8.5 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8.7 | Connector | connector | 6× | 6 | · | part |
| 9 | Pneumatic System 4 parts | auger-filling-machine-pneumatics | 1× | 1 | 6 | assembly |
| 9.1 | Filter-Regulator | auger-filling-machine-fr-unit | 1× | 1 | · | part |
| 9.2 | Valve Bank | auger-filling-machine-valve-bank | 1× | 1 | · | part |
| 9.3 | Air Cylinder | auger-filling-machine-air-cylinder | 3× | 3 | · | part |
| 9.4 | Air Tubing | auger-filling-machine-air-tubing | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Automatic Strapping Machine
251 parts · shares 5 with this page
Case Labeling Machine
120 parts · shares 5 with this page
Counter-Pressure Filler
519 parts · shares 5 with this page
Gravity Filling Machine
177 parts · shares 5 with this page
 Paper Banding Machine
173 parts · shares 5 with this page
Robotic Case Packing Cell
497 parts · shares 5 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$3M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| heidelberg.com ↗ | Heidelberg, DE | Printing presses | 10 units | 12–22 wks |
|
🇨🇭Bobst
bobst.com ↗
|
Lausanne, CH | Packaging machinery | 10 units | 12–22 wks |
| koenig-bauer.com ↗ | Würzburg, DE | Printing presses | 10 units | 12–22 wks |
| wuh-group.com ↗ | Lengerich, DE | Flexible packaging machines | 10 units | 12–22 wks |
| markandy.com ↗ | Chesterfield, US | Label presses | 10 units | 12–22 wks |
1,019-word article