Gravity Filling Machine
ProductOverview
The gravity filling machine fills containers with thin, free-flowing liquids by letting product fall under its own weight from an elevated reservoir into the bottle below. It suits water, juice, wine, spirits, vinegar, thin oils, solvents, and similar products in the 1-200 cP viscosity band. There is no pump pushing product into the container during the fill itself, so shear on the product is low and the mechanism is simple, which is why gravity fillers dominate beverage and low-viscosity liquid lines.
Product is held in the overhead Overhead Header Tank, raised 1.2-1.8 m above the nozzles by the Tank Tower. That height sets the static head, and the head sets the flow rate through each open valve. Containers ride along the Container Conveyor into the Indexing Station station, where eight bottles at a time are registered under the Fill Head Manifold. The Nozzle Lift Gantry dives the nozzles down, the Gravity Fill Valve units open, product flows in by gravity, and each fill stops at a set level. The machine then retracts the nozzles, indexes the next batch, and discharges the filled bottles.
Gravity Head and Fill Rate
The driving force is the column of liquid in the header tank. With the tank kept at a constant level by the Level Float Switch pair and the Level Refill Valve, the static head stays nearly constant from the first bottle to the last, so fill rate does not drift across a run. The Breather Vent keeps the tank at atmospheric pressure, since any vacuum building above the liquid would slow the flow and any back-pressure would speed it up unpredictably.
Because all eight stations share one Manifold Body, the nozzles nearest the inlet would otherwise see slightly more head than the far ones. The Flow Trim Needle at each station trims this out so every bottle fills in the same time. For a water-thin product at the standard head, an 8 mm nozzle passes roughly 0.3-0.5 L/s, so a 750 ml wine bottle fills in around 2 seconds.
Fill-to-Level Mechanism
Gravity fillers fill to a level, not to a volume. This is what makes a row of bottles look identically full on a shelf even when their internal volumes vary slightly, which matters for glass where wall thickness is inconsistent. Each No-Drip Fill Nozzle carries a concentric Fill-to-Level Vent Tube. As product rises in the bottle, displaced air escapes up the vent tube. When the liquid reaches the bottom of the vent tube, the air can no longer escape, the trapped air stops further flow, and the fill self-terminates at that level. Adjusting how far the vent tube extends into the bottle sets the fill height.
The No-Drip Fill Nozzle seals against the bottle mouth during the fill (bottle-up sealing) and shuts off positively when the Gravity Fill Valve closes, which stops stringing and dripping between cycles. Any product that does escape lands in the Drip Tray and Recirculation and is returned to the Overhead Header Tank by the Recirculation Pump through the Return Strainer, so almost nothing is lost.
Container Handling
Containers arrive single-file on the Flat-Top Chain, kept centered by the Container Guide Rail. The Infeed Timing Worm accelerates and spaces them to the 100 mm nozzle pitch, then the Star Wheel carries them into the eight fill positions. The Neck Gripper holds each container by the neck so the nozzle can dive in without tipping it, and the Gate Stop meters bottles into and out of the station.
The worm and star wheel are change parts. A different container diameter needs a matched worm and star wheel, swapped out and registered through the Index Cam Plate. The Index Servo Motor drives the star wheel through a Helical Gear Pair with an absolute encoder so positions repeat exactly after a changeover. The Bottle Presence Sensor units detect arrival and queue backup, holding the index until a full set of eight bottles is present.
Nozzle Dive and Actuation
For bottom-up filling, which reduces foaming on aerating products like beer or juice, the Nozzle Lift Gantry lowers the nozzle bank so each No-Drip Fill Nozzle enters the bottle and fills from near the base, rising with the liquid. A Servo Motor turns a Ball Screw to move the Lift Carriage along its Linear Guide Rail rails, and the Coil Spring under each nozzle gives the seal a controlled preload against the bottle mouth. The dive depth and speed are recipe values, so switching from a tall 1 L bottle to a short 250 ml jar is a screen setting, not a mechanical change.
Pneumatics and Control
Shop air is cleaned and regulated to 6 bar by the Air Preparation Unit unit, buffered in the Air Buffer Tank, and switched by the Solenoid Valve Bank. The valves drive the Gravity Fill Valve poppets, the Pneumatic Cylinder gates, and the gripper banks. A Pressure Sensor watches supply pressure and faults the machine if it drops below the level needed for a clean valve seat.
The Control System cabinet runs the cycle. The PLC sequences index, dive, fill, vent-close, retract, and discharge, while the HMI Panel shows rate and fill count and stores a recipe per product and container. The Conveyor VFD paces the conveyor and the Servo Drive units run the lift and index axes off Power Supply 24 VDC logic power. Dual-channel Emergency Stop buttons and the interlocked Guard Panel doors drop all motion when opened, and the Relay safety chain keeps the machine in a known-safe state on any fault.
Gravity Filling Machine parts and their functions
9 top-level parts · 177 parts in total · full bill of materials below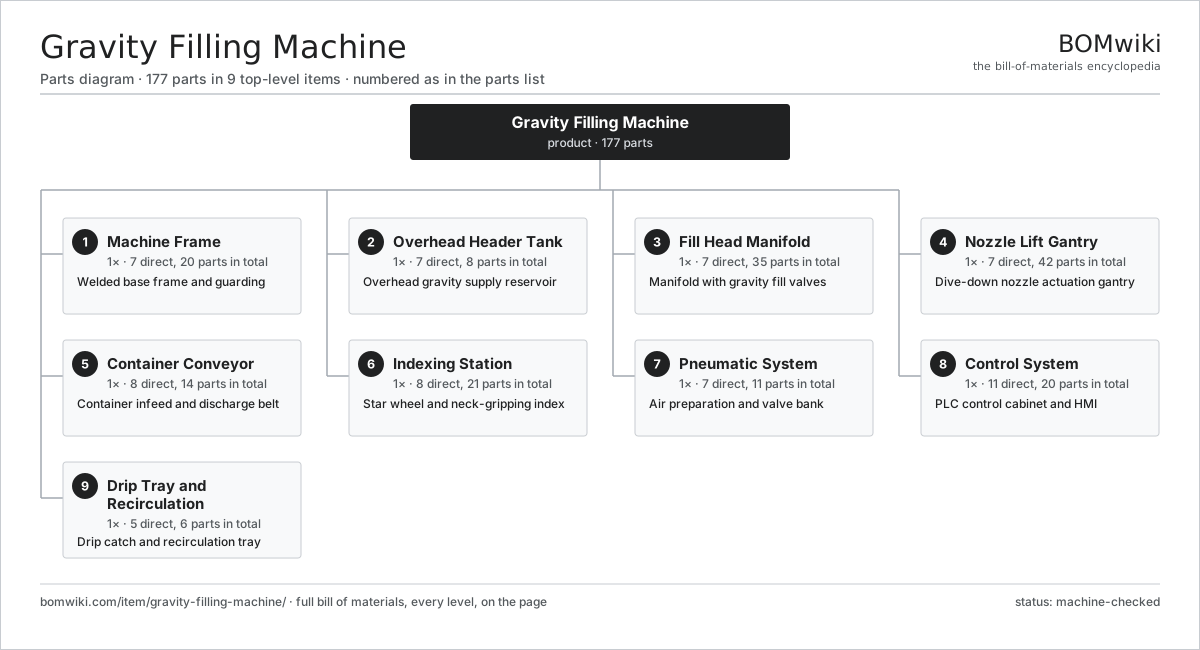
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Machine Frame 7 parts | 1× | Welded base frame and guarding |
| 2 | Overhead Header Tank 7 parts | 1× | Overhead gravity supply reservoir |
| 3 | Fill Head Manifold 7 parts | 1× | Manifold with gravity fill valves |
| 4 | Nozzle Lift Gantry 7 parts | 1× | Dive-down nozzle actuation gantry |
| 5 | Container Conveyor 8 parts | 1× | Container infeed and discharge belt |
| 6 | Indexing Station 8 parts | 1× | Star wheel and neck-gripping index |
| 7 | Pneumatic System 7 parts | 1× | Air preparation and valve bank |
| 8 | Control System 11 parts | 1× | PLC control cabinet and HMI |
| 9 | Drip Tray and Recirculation 5 parts | 1× | Drip catch and recirculation tray |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Gravity Filling Machine
9 top-level lines · 83 rows shown · 177 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Machine Frame 7 parts | gravity-filling-machine-frame | 1× | 1 | 20 | assembly |
| 1.1 | Base Weldment | gravity-filling-machine-base-weldment | 1× | 1 | · | part |
| 1.2 | Tank Tower | gravity-filling-machine-tank-tower | 1× | 1 | · | part |
| 1.3 | Leveling Foot | gravity-filling-machine-leveling-foot | 6× | 6 | · | part |
| 1.4 | Guard Panel | gravity-filling-machine-guard-panel | 4× | 4 | · | part |
| 1.5 | Transport Caster | gravity-filling-machine-caster | 4× | 4 | · | part |
| 1.6 | Sheet Metal Panel | sheet-panel | 3× | 3 | · | part |
| 1.7 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Overhead Header Tank 7 parts | gravity-filling-machine-header-tank | 1× | 1 | 8 | assembly |
| 2.1 | Header Tank Shell | gravity-filling-machine-tank-shell | 1× | 1 | · | part |
| 2.2 | Tank Lid | gravity-filling-machine-tank-lid | 1× | 1 | · | part |
| 2.3 | Level Float Switch | gravity-filling-machine-float-switch | 2× | 2 | · | part |
| 2.4 | Level Refill Valve | gravity-filling-machine-level-valve | 1× | 1 | · | part |
| 2.5 | Breather Vent | gravity-filling-machine-tank-vent | 1× | 1 | · | part |
| 2.6 | Supply Inlet Port | gravity-filling-machine-supply-inlet | 1× | 1 | · | part |
| 2.7 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 3 | Fill Head Manifold 7 parts | gravity-filling-machine-fill-head | 1× | 1 | 35 | assembly |
| 3.1 | Manifold Body | gravity-filling-machine-manifold-body | 1× | 1 | · | part |
| 3.2 | Gravity Fill Valve | gravity-filling-machine-fill-valve | 8× | 8 | · | part |
| 3.3 | No-Drip Fill Nozzle | gravity-filling-machine-no-drip-nozzle | 8× | 8 | · | part |
| 3.4 | Flow Trim Needle | gravity-filling-machine-flow-needle | 8× | 8 | · | part |
| 3.5 | Fill-to-Level Vent Tube | gravity-filling-machine-vent-tube | 8× | 8 | · | part |
| 3.6 | Head Height Adjuster | gravity-filling-machine-head-adjust | 1× | 1 | · | part |
| 3.7 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 4 | Nozzle Lift Gantry 7 parts | gravity-filling-machine-nozzle-lift | 1× | 1 | 42 | assembly |
| 4.1 | Lift Carriage | gravity-filling-machine-lift-carriage | 1× | 1 | · | part |
| 4.2 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 4.2.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 4.2.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 4.2.3 | Encoder | encoder | 1× | 1 | · | part |
| 4.2.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 4.3 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 4.4 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 4.5 | Nozzle Mount Bracket | gravity-filling-machine-lift-bracket | 2× | 2 | · | part |
| 4.6 | Coil Spring | coil-spring | 8× | 8 | · | part |
| 4.7 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 5 | Container Conveyor 8 parts | gravity-filling-machine-conveyor | 1× | 1 | 14 | assembly |
| 5.1 | Conveyor Frame | gravity-filling-machine-conveyor-frame | 1× | 1 | · | part |
| 5.2 | Flat-Top Chain | gravity-filling-machine-chain-belt | 1× | 1 | · | part |
| 5.3 | Chain Sprocket | gravity-filling-machine-drive-sprocket | 2× | 2 | · | part |
| 5.4 | Conveyor Gearmotor | gravity-filling-machine-conveyor-motor | 1× | 1 | · | part |
| 5.5 | Container Guide Rail | gravity-filling-machine-guide-rail | 2× | 2 | · | part |
| 5.6 | Bottle Presence Sensor | gravity-filling-machine-bottle-sensor | 2× | 2 | · | part |
| 5.7 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 5.8 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 6 | Indexing Station 8 parts | gravity-filling-machine-indexing | 1× | 1 | 21 | assembly |
| 6.1 | Infeed Timing Worm | gravity-filling-machine-infeed-worm | 1× | 1 | · | part |
| 6.2 | Star Wheel | gravity-filling-machine-star-wheel | 1× | 1 | · | part |
| 6.3 | Neck Gripper | gravity-filling-machine-neck-gripper | 8× | 8 | · | part |
| 6.4 | Index Cam Plate | gravity-filling-machine-index-cam | 1× | 1 | · | part |
| 6.5 | Gate Stop | gravity-filling-machine-gate-stop | 2× | 2 | · | part |
| 6.6 | Index Servo Motor | gravity-filling-machine-index-motor | 1× | 1 | · | part |
| 6.7 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 6.8 | Ball Bearing | ball-bearing | 6× | 6 | · | part |
| 7 | Pneumatic System 7 parts | gravity-filling-machine-pneumatics | 1× | 1 | 11 | assembly |
| 7.1 | Air Preparation Unit | gravity-filling-machine-air-prep | 1× | 1 | · | part |
| 7.2 | Solenoid Valve Bank | gravity-filling-machine-valve-bank | 1× | 1 | · | part |
| 7.3 | Pneumatic Cylinder | gravity-filling-machine-air-cylinder | 4× | 4 | · | part |
| 7.4 | Air Buffer Tank | gravity-filling-machine-air-reservoir | 1× | 1 | · | part |
| 7.5 | Air Tubing Set | gravity-filling-machine-tubing-set | 1× | 1 | · | part |
| 7.6 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 7.7 | Connector | connector | 2× | 2 | · | part |
| 8 | Control System 11 parts | gravity-filling-machine-controls | 1× | 1 | 20 | assembly |
| 8.1 | PLC | gravity-filling-machine-plc | 1× | 1 | · | part |
| 8.2 | HMI Panel 3 parts | gravity-filling-machine-hmi | 1× | 1 | · | part |
| 8.2.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.2.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.2.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.3 | Conveyor VFD | gravity-filling-machine-vfd | 1× | 1 | · | part |
| 8.4 | Servo Drive | gravity-filling-machine-servo-drive | 2× | 2 | · | part |
| 8.5 | Emergency Stop | gravity-filling-machine-estop | 2× | 2 | · | part |
| 8.6 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.7 | Relay | relay | 6× | 6 | · | part |
| 8.8 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8.9 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.10 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.11 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 9 | Drip Tray and Recirculation 5 parts | gravity-filling-machine-drip-tray | 1× | 1 | 6 | assembly |
| 9.1 | Drip Catch Pan | gravity-filling-machine-tray-pan | 1× | 1 | · | part |
| 9.2 | Return Strainer | gravity-filling-machine-strainer | 1× | 1 | · | part |
| 9.3 | Recirculation Pump | gravity-filling-machine-return-pump | 1× | 1 | · | part |
| 9.4 | Return Line | gravity-filling-machine-return-line | 1× | 1 | · | part |
| 9.5 | Oil Seal | oil-seal | 2× | 2 | · | part |
Related products
same domain, ranked by shared parts Industrial Screen Printing Press
162 parts · shares 10 with this page
 Piston Filling Machine
112 parts · shares 9 with this page
 Digital Inkjet Web Press
3,001 parts · shares 9 with this page
Counter-Pressure Filler
519 parts · shares 9 with this page
Wraparound Case Packer
278 parts · shares 9 with this page
Stick Pack Machine
189 parts · shares 6 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$3M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| heidelberg.com ↗ | Heidelberg, DE | Printing presses | 10 units | 12–22 wks |
|
🇨🇭Bobst
bobst.com ↗
|
Lausanne, CH | Packaging machinery | 10 units | 12–22 wks |
| koenig-bauer.com ↗ | Würzburg, DE | Printing presses | 10 units | 12–22 wks |
| wuh-group.com ↗ | Lengerich, DE | Flexible packaging machines | 10 units | 12–22 wks |
| markandy.com ↗ | Chesterfield, US | Label presses | 10 units | 12–22 wks |
1,042-word article