Solventless Laminator
ProductOverview
A solventless laminator joins two or more flexible webs, such as printed film, plain film, and aluminium foil, into a single multi-layer material used for food and consumer-goods packaging. It applies a very thin layer of two-component polyurethane adhesive that contains no solvent, so there is no drying oven and no solvent recovery to run. The adhesive is mixed on the machine just before it is coated, transferred to the first web in a roll coating head, and the second web is pressed onto it in a nip. The bond is still soft when the laminate winds up; final strength develops over hours or days as the adhesive cures off the machine. Because there is no oven, solventless lines run fast and use far less energy than the older solvent-based laminators they replaced.
The web flows from the Unwind Station stations through the Coating Head, where adhesive from the Adhesive Mixer is applied, into the Lamination Nip that joins the second web, and onto the Rewind Station. The Web Handling guides and tensions every web, the Sectional Drive holds line speed and registration, and the Control System coordinates the whole process.
Unwinding the webs
Each web being laminated has its own Unwind Station. The Air Shaft grips the roll core and a Unwind Drive torque motor pays the web off at a tension held by Tension Load Cell feedback. A Splice Table lets the operator tape a fresh roll onto the running web so the line need not stop between rolls, which matters on a continuous process where a stop can scrap meters of part-cured laminate. A Spreader Roll roll keeps each web flat as it enters the machine.
Mixing the adhesive
Solventless adhesive is reactive and has a short pot life once the two parts meet, so it is mixed continuously and only in the amount the line consumes. The Adhesive Mixer meters the polyol with a Resin Pump and the isocyanate with a Hardener Pump, each verified by a Flow Meter so the ratio stays correct. The two streams combine in a Static Mix Block whose internal elements blend them without folding in air. A Adhesive Heater warms the blend to lower its viscosity for clean coating, and heated Day Tank vessels hold each component ready. Getting the ratio and mix right is central: an off-ratio batch never fully cures and the laminate later delaminates.
The coating head
The mixed adhesive is metered to a precise thin film and transferred to the web in the Coating Head, a smooth five-roll head. The adhesive is picked up and split across the Metering Roll, Doctor Roll, and Transfer Roll, each gap and speed setting reducing the film thickness in stages, until the Applicator Roll lays a coat of one to a few grams per square meter onto the web running over the Backing Roll. Each roll runs at its own temperature through a Roll Heater Circuit circuit, because viscosity and therefore coat weight depend strongly on temperature. The five-roll arrangement is what lets a solventless line lay so little adhesive so evenly at high speed.
Joining and winding
At the Lamination Nip the coated web meets the second web and the two are pressed together. A rubber Nip Roll loaded by a Nip Cylinder presses both webs against a large Heated Drum, warmed by a Drum Heater, so the still-liquid adhesive wets out and the bond starts to build. The fresh laminate then winds onto the Rewind Station: a Rewind Air Shaft driven by a Rewind Drive at tapering tension, with a Lay-On Roll pressing out trapped air so the soft roll does not telescope before it cures. A Cutoff Knife severs the web at roll change.
Drive, control, and use
Tension must be steady through every section or the thin coat varies and the webs shift, so the Sectional Drive uses an independent Servo Motor and Servo Amplifier on each section, all referenced to load-cell feedback through Web Handling dancers and idlers. The Control System system, built around a Line Controller and an operator HMI, sets the mix ratio, coat weight, tension, and roll temperatures from a stored recipe and logs the run for quality records. Finished rolls move to a curing room where the polyurethane reaction completes over one to several days before the laminate is slit and made into pouches or wraps. Solventless lamination dominates flexible food packaging because it is fast, clean, and free of solvent emissions, with the trade-off that the bond is not usable until it has cured off the machine.
Solventless Laminator parts and their functions
9 top-level parts · 631 parts in total · full bill of materials below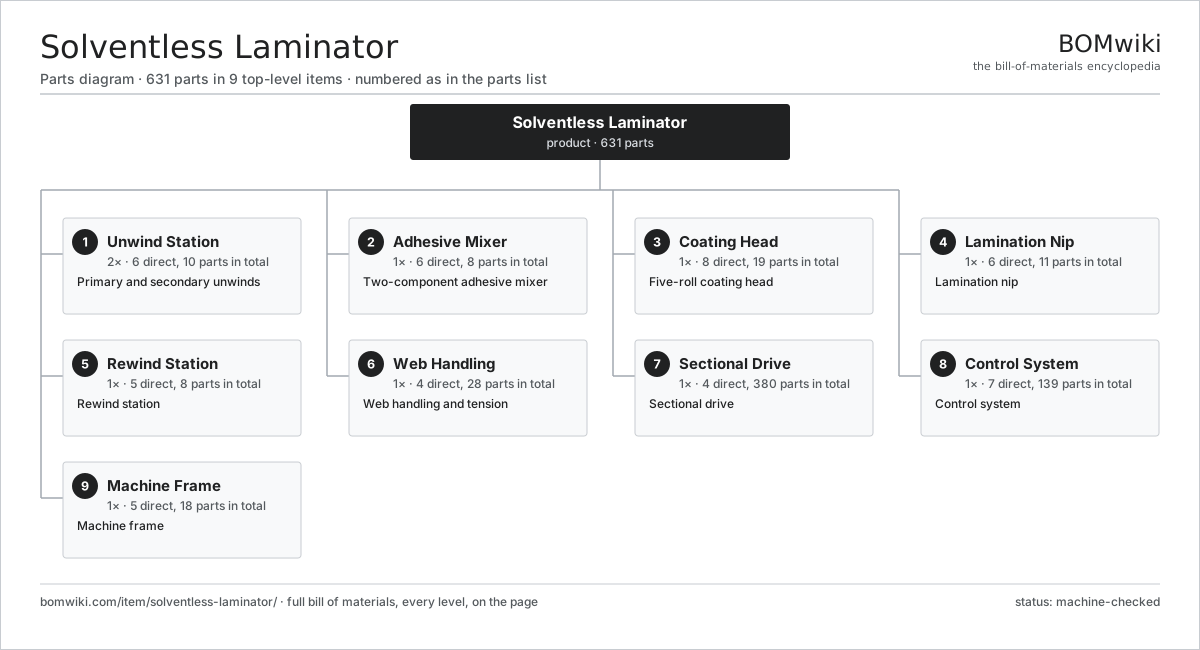
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Unwind Station 6 parts | 2× | Primary and secondary unwinds |
| 2 | Adhesive Mixer 6 parts | 1× | Two-component adhesive mixer |
| 3 | Coating Head 8 parts | 1× | Five-roll coating head |
| 4 | Lamination Nip 6 parts | 1× | Lamination nip |
| 5 | Rewind Station 5 parts | 1× | Rewind station |
| 6 | Web Handling 4 parts | 1× | Web handling and tension |
| 7 | Sectional Drive 4 parts | 1× | Sectional drive |
| 8 | Control System 7 parts | 1× | Control system |
| 9 | Machine Frame 5 parts | 1× | Machine frame |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Solventless Laminator
9 top-level lines · 72 rows shown · 631 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Unwind Station 6 parts | solventless-laminator-unwind | 2× | 2 | 10 | assembly |
| 1.1 | Air Shaft | solventless-laminator-unwind-shaft | 1× | 2 | · | part |
| 1.2 | Unwind Drive | solventless-laminator-unwind-drive | 1× | 2 | · | part |
| 1.3 | Splice Table | solventless-laminator-splice-table | 1× | 2 | · | part |
| 1.4 | Tension Load Cell | solventless-laminator-load-cell | 2× | 4 | · | part |
| 1.5 | Spreader Roll | solventless-laminator-spreader | 1× | 2 | · | part |
| 1.6 | Ball Bearing | ball-bearing | 4× | 8 | · | part |
| 2 | Adhesive Mixer 6 parts | solventless-laminator-mixer | 1× | 1 | 8 | assembly |
| 2.1 | Resin Pump | solventless-laminator-resin-pump | 1× | 1 | · | part |
| 2.2 | Hardener Pump | solventless-laminator-hardener-pump | 1× | 1 | · | part |
| 2.3 | Static Mix Block | solventless-laminator-mix-block | 1× | 1 | · | part |
| 2.4 | Adhesive Heater | solventless-laminator-mix-heater | 1× | 1 | · | part |
| 2.5 | Flow Meter | solventless-laminator-flow-meter | 2× | 2 | · | part |
| 2.6 | Day Tank | solventless-laminator-day-tank | 2× | 2 | · | part |
| 3 | Coating Head 8 parts | solventless-laminator-coater | 1× | 1 | 19 | assembly |
| 3.1 | Metering Roll | solventless-laminator-metering-roll | 1× | 1 | · | part |
| 3.2 | Transfer Roll | solventless-laminator-transfer-roll | 1× | 1 | · | part |
| 3.3 | Applicator Roll | solventless-laminator-applicator-roll | 1× | 1 | · | part |
| 3.4 | Backing Roll | solventless-laminator-rubber-roll | 1× | 1 | · | part |
| 3.5 | Doctor Roll | solventless-laminator-doctor-roll | 1× | 1 | · | part |
| 3.6 | Roll Heater Circuit | solventless-laminator-roll-heater | 4× | 4 | · | part |
| 3.7 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 3.8 | Ball Bearing | ball-bearing | 8× | 8 | · | part |
| 4 | Lamination Nip 6 parts | solventless-laminator-nip | 1× | 1 | 11 | assembly |
| 4.1 | Heated Drum | solventless-laminator-heated-drum | 1× | 1 | · | part |
| 4.2 | Nip Roll | solventless-laminator-nip-roll | 1× | 1 | · | part |
| 4.3 | Nip Cylinder | solventless-laminator-nip-cylinder | 2× | 2 | · | part |
| 4.4 | Drum Heater | solventless-laminator-drum-heater | 1× | 1 | · | part |
| 4.5 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 4.6 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 5 | Rewind Station 5 parts | solventless-laminator-rewind | 1× | 1 | 8 | assembly |
| 5.1 | Rewind Air Shaft | solventless-laminator-rewind-shaft | 1× | 1 | · | part |
| 5.2 | Rewind Drive | solventless-laminator-rewind-drive | 1× | 1 | · | part |
| 5.3 | Lay-On Roll | solventless-laminator-lay-on-roll | 1× | 1 | · | part |
| 5.4 | Cutoff Knife | solventless-laminator-cutoff | 1× | 1 | · | part |
| 5.5 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 6 | Web Handling 4 parts | solventless-laminator-web-control | 1× | 1 | 28 | assembly |
| 6.1 | Idler Roll | solventless-laminator-idler-roll | 8× | 8 | · | part |
| 6.2 | Edge Guide | solventless-laminator-edge-guide | 2× | 2 | · | part |
| 6.3 | Tension Dancer | solventless-laminator-dancer | 2× | 2 | · | part |
| 6.4 | Ball Bearing | ball-bearing | 16× | 16 | · | part |
| 7 | Sectional Drive 4 parts | solventless-laminator-drive | 1× | 1 | 380 | assembly |
| 7.1 | Servo Motor 4 parts | servo-motor | 4× | 4 | 24 | assembly |
| 7.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 4 | 3 | assembly |
| 7.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 4 | 19 | assembly |
| 7.1.3 | Encoder | encoder | 1× | 4 | · | part |
| 7.1.4 | Motor Housing | motor-housing | 1× | 4 | · | part |
| 7.2 | Servo Amplifier 4 parts | solventless-laminator-servo-drive | 4× | 4 | 68 | assembly |
| 7.2.1 | Bare PCB | pcb-bare | 1× | 4 | · | part |
| 7.2.2 | Power MOSFET | mosfet | 6× | 24 | · | part |
| 7.2.3 | Power Supply | power-supply | 1× | 4 | · | part |
| 7.2.4 | SMD Passive (R/C/L) | smd-passives | 60× | 240 | · | part |
| 7.3 | Gearbox Housing | gearbox-housing | 4× | 4 | · | part |
| 7.4 | Ball Bearing | ball-bearing | 8× | 8 | · | part |
| 8 | Control System 7 parts | solventless-laminator-control | 1× | 1 | 139 | assembly |
| 8.1 | Line Controller 4 parts | solventless-laminator-plc | 1× | 1 | 100 | assembly |
| 8.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.1.3 | SMD Passive (R/C/L) | smd-passives | 90× | 90 | · | part |
| 8.1.4 | Connector | connector | 8× | 8 | · | part |
| 8.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.4 | Temperature Controller | solventless-laminator-temp-controller | 4× | 4 | · | part |
| 8.5 | Relay | relay | 12× | 12 | · | part |
| 8.6 | Connector | connector | 20× | 20 | · | part |
| 8.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9 | Machine Frame 5 parts | solventless-laminator-frame | 1× | 1 | 18 | assembly |
| 9.1 | Side Frame | solventless-laminator-side-frame | 2× | 2 | · | part |
| 9.2 | Sheet Metal Panel | sheet-panel | 8× | 8 | · | part |
| 9.3 | Safety Guard | solventless-laminator-safety-guard | 1× | 1 | · | part |
| 9.4 | Leveling Foot | solventless-laminator-leveling-foot | 6× | 6 | · | part |
| 9.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Slitter Rewinder
528 parts · shares 6 with this page
Web Sheeting Machine
487 parts · shares 6 with this page
Automatic Screen Printing Machine
640 parts · shares 3 with this page
 Screen Exposure Unit
83 parts · shares 2 with this page
 Dye-Sublimation Printer
414 parts · shares 2 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$3M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| heidelberg.com ↗ | Heidelberg, DE | Printing presses | 10 units | 12–22 wks |
|
🇨🇭Bobst
bobst.com ↗
|
Lausanne, CH | Packaging machinery | 10 units | 12–22 wks |
| koenig-bauer.com ↗ | Würzburg, DE | Printing presses | 10 units | 12–22 wks |
| wuh-group.com ↗ | Lengerich, DE | Flexible packaging machines | 10 units | 12–22 wks |
| markandy.com ↗ | Chesterfield, US | Label presses | 10 units | 12–22 wks |
835-word article