Folder-Gluer Machine
ProductAlso known as: Carton Folder-Gluer
Overview
A folder-gluer turns flat printed and die-cut carton blanks into finished folding cartons by creasing, folding, and gluing them as they run through the machine in a continuous stream. It is the last machine in the folding-carton process, after printing and die cutting, and it is what makes a stack of flat blanks into the collapsed glued cartons that ship to a packer to be opened, filled, and closed. The machine feeds blanks one after another, breaks their fold lines so they hinge cleanly, lays adhesive on the glue flap, folds the panels over so the glued flap meets its mating panel, then holds the seam closed until it sets and stacks the finished cartons.
A blank enters at the Blank Feeder, is conditioned in the Pre-Break Section section, receives adhesive at the Glue Application station, is folded in the Folding Section section, and is set and collected at the Compression and Delivery section. The Drive System runs the belts in step and the Control System times the glue and counts the cartons.
Feeding the blanks
The Blank Feeder separates blanks from a stack and meters them into the machine. Flat blanks sit in a Blank Hopper, and Feed Roller friction rollers, often helped by a Suction Bar gripping the lead edge, pull the bottom or front blank out one at a time. A Gap Setter gate sets the slot so only a single blank passes, and Feed Belt belts carry the blanks downstream in an even, gapped stream. Steady feeding sets the rhythm for the whole machine, because the glue and fold stations act on each blank based on where it is expected to be.
Pre-breaking and aligning
Carton board holds a memory in its score lines, so before gluing the Pre-Break Section section works the creases. A Pre-Break Rail folds the panels fully over and then back, which cracks the fibers along the score so the final fold is clean and square rather than springy. At the same time Alignment Belt belts and Side Guide guides square each blank, and Hold-Down Wheel wheels keep it flat. A blank that enters skewed will glue and fold crooked, so this conditioning step matters for seam quality.
Applying adhesive
The Glue Application station lays adhesive exactly where the seam will form. Most lines run hot melt: a Hot-Melt Tank melts the adhesive, a Glue Pump feeds it under pressure, and Glue Gun heads fire timed beads onto the glue flap as each blank passes. Each gun uses a Gun Solenoid valve to open its Gun Nozzle for a precise interval, so the bead starts and stops at the right point on the moving blank. A Glue Heater keeps the hose and guns at melt temperature, and a Glue Detector confirms each carton actually got glue. Bead placement and timing decide whether the seam holds, so the glue heads are synchronized to blank position by the control system.
Folding the carton
In the Folding Section section the panels are turned over as the blank runs. Folding Belt belts carry the blank while a Folding Plow, a curved stationary bar, lifts and folds a side panel progressively up and over the moving blank. Hook Folder folders finish folds a plow cannot reach, and Folding Roller rollers crease and support the panels through the motion. A Skew Corrector adjuster keeps the two panels that will form the glued seam aligned so the seam closes square. Folding on the run, rather than in a stop-and-fold press, is what lets the machine reach high speed.
Compression, delivery, and use
A glued seam needs time and pressure to set, so the Compression and Delivery section squeezes the folded carton between Compression Belt belts loaded by Pressure Roller rollers for the seconds the adhesive needs. Finished cartons are counted by a Carton Counter and pushed into batches by a Batch Ejector, while a Reject Gate diverts any carton flagged for missing glue or skew. The Drive System runs the sections in synchronism with Servo Motor axes through Servo Drive amplifiers and Gearbox Housing reducers, and the Control System system, built on a Machine Controller with a Glue Controller, fires the guns from blank position and stores recipes per carton style. Folder-gluers handle straight-line cartons, crash-lock bottoms, and four- and six-corner trays; the more complex the style, the more folding sections and hook folders the machine carries. A straight-line carton needs only a single fold from a Folding Plow, while a crash-lock bottom is folded and tucked so it snaps square when the packer opens it, which calls for extra Hook Folder folders timed to the moving blank. Glue type follows the board and the line speed: hot melt from the Hot-Melt Tank sets in a fraction of a second and suits fast runs, while cold PVA gives a stronger long-term bond on heavy board but needs a longer pass under the Compression Belt to hold the seam until it grabs.
Folder-Gluer Machine parts and their functions
8 top-level parts · 543 parts in total · full bill of materials below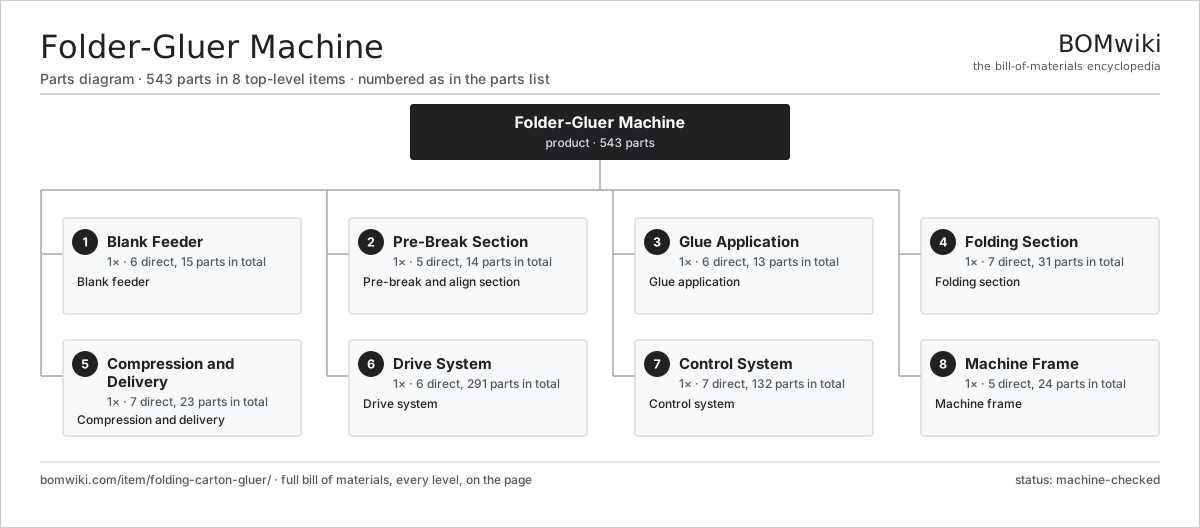
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Blank Feeder 6 parts | 1× | Blank feeder |
| 2 | Pre-Break Section 5 parts | 1× | Pre-break and align section |
| 3 | Glue Application 6 parts | 1× | Glue application |
| 4 | Folding Section 7 parts | 1× | Folding section |
| 5 | Compression and Delivery 7 parts | 1× | Compression and delivery |
| 6 | Drive System 6 parts | 1× | Drive system |
| 7 | Control System 7 parts | 1× | Control system |
| 8 | Machine Frame 5 parts | 1× | Machine frame |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Folder-Gluer Machine
8 top-level lines · 71 rows shown · 543 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Blank Feeder 6 parts | folding-carton-gluer-feeder | 1× | 1 | 15 | assembly |
| 1.1 | Blank Hopper | folding-carton-gluer-hopper | 1× | 1 | · | part |
| 1.2 | Feed Roller | folding-carton-gluer-feed-roller | 4× | 4 | · | part |
| 1.3 | Suction Bar | folding-carton-gluer-suction-bar | 1× | 1 | · | part |
| 1.4 | Feed Belt | folding-carton-gluer-feed-belt | 2× | 2 | · | part |
| 1.5 | Gap Setter | folding-carton-gluer-gap-setter | 1× | 1 | · | part |
| 1.6 | Ball Bearing | ball-bearing | 6× | 6 | · | part |
| 2 | Pre-Break Section 5 parts | folding-carton-gluer-prefold | 1× | 1 | 14 | assembly |
| 2.1 | Pre-Break Rail | folding-carton-gluer-prebreak-rail | 2× | 2 | · | part |
| 2.2 | Alignment Belt | folding-carton-gluer-align-belt | 2× | 2 | · | part |
| 2.3 | Side Guide | folding-carton-gluer-side-guide | 2× | 2 | · | part |
| 2.4 | Hold-Down Wheel | folding-carton-gluer-hold-down | 4× | 4 | · | part |
| 2.5 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 3 | Glue Application 6 parts | folding-carton-gluer-glue | 1× | 1 | 13 | assembly |
| 3.1 | Hot-Melt Tank | folding-carton-gluer-glue-tank | 1× | 1 | · | part |
| 3.2 | Glue Pump | folding-carton-gluer-glue-pump | 1× | 1 | · | part |
| 3.3 | Glue Gun 2 parts | folding-carton-gluer-glue-gun | 4× | 4 | 2 | assembly |
| 3.3.1 | Gun Solenoid | folding-carton-gluer-gun-solenoid | 1× | 4 | · | part |
| 3.3.2 | Gun Nozzle | folding-carton-gluer-gun-nozzle | 1× | 4 | · | part |
| 3.4 | Glue Detector | folding-carton-gluer-glue-detector | 1× | 1 | · | part |
| 3.5 | Glue Heater | folding-carton-gluer-glue-heater | 1× | 1 | · | part |
| 3.6 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 4 | Folding Section 7 parts | folding-carton-gluer-folding | 1× | 1 | 31 | assembly |
| 4.1 | Folding Belt | folding-carton-gluer-fold-belt | 4× | 4 | · | part |
| 4.2 | Folding Plow | folding-carton-gluer-plow | 2× | 2 | · | part |
| 4.3 | Hook Folder | folding-carton-gluer-hook | 2× | 2 | · | part |
| 4.4 | Folding Roller | folding-carton-gluer-fold-roller | 6× | 6 | · | part |
| 4.5 | Skew Corrector | folding-carton-gluer-skew-correct | 1× | 1 | · | part |
| 4.6 | Drive Belt | drive-belt | 4× | 4 | · | part |
| 4.7 | Ball Bearing | ball-bearing | 12× | 12 | · | part |
| 5 | Compression and Delivery 7 parts | folding-carton-gluer-compression | 1× | 1 | 23 | assembly |
| 5.1 | Compression Belt | folding-carton-gluer-compression-belt | 2× | 2 | · | part |
| 5.2 | Pressure Roller | folding-carton-gluer-press-roller | 8× | 8 | · | part |
| 5.3 | Batch Ejector | folding-carton-gluer-ejector | 1× | 1 | · | part |
| 5.4 | Carton Counter | folding-carton-gluer-counter | 1× | 1 | · | part |
| 5.5 | Reject Gate | folding-carton-gluer-reject-gate | 1× | 1 | · | part |
| 5.6 | Drive Belt | drive-belt | 2× | 2 | · | part |
| 5.7 | Ball Bearing | ball-bearing | 8× | 8 | · | part |
| 6 | Drive System 6 parts | folding-carton-gluer-drive | 1× | 1 | 291 | assembly |
| 6.1 | Servo Motor 4 parts | servo-motor | 3× | 3 | 24 | assembly |
| 6.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 3 | 3 | assembly |
| 6.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 3 | 19 | assembly |
| 6.1.3 | Encoder | encoder | 1× | 3 | · | part |
| 6.1.4 | Motor Housing | motor-housing | 1× | 3 | · | part |
| 6.2 | Servo Drive 4 parts | folding-carton-gluer-servo-drive | 3× | 3 | 68 | assembly |
| 6.2.1 | Bare PCB | pcb-bare | 1× | 3 | · | part |
| 6.2.2 | Power MOSFET | mosfet | 6× | 18 | · | part |
| 6.2.3 | Power Supply | power-supply | 1× | 3 | · | part |
| 6.2.4 | SMD Passive (R/C/L) | smd-passives | 60× | 180 | · | part |
| 6.3 | Gearbox Housing | gearbox-housing | 2× | 2 | · | part |
| 6.4 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 6.5 | Drive Belt | drive-belt | 3× | 3 | · | part |
| 6.6 | Ball Bearing | ball-bearing | 8× | 8 | · | part |
| 7 | Control System 7 parts | folding-carton-gluer-control | 1× | 1 | 132 | assembly |
| 7.1 | Machine Controller 4 parts | folding-carton-gluer-plc | 1× | 1 | 100 | assembly |
| 7.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.1.3 | SMD Passive (R/C/L) | smd-passives | 90× | 90 | · | part |
| 7.1.4 | Connector | connector | 8× | 8 | · | part |
| 7.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.4 | Glue Controller | folding-carton-gluer-glue-controller | 1× | 1 | · | part |
| 7.5 | Relay | relay | 10× | 10 | · | part |
| 7.6 | Connector | connector | 18× | 18 | · | part |
| 7.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8 | Machine Frame 5 parts | folding-carton-gluer-frame | 1× | 1 | 24 | assembly |
| 8.1 | Side Frame | folding-carton-gluer-side-frame | 4× | 4 | · | part |
| 8.2 | Sheet Metal Panel | sheet-panel | 10× | 10 | · | part |
| 8.3 | Safety Guard | folding-carton-gluer-safety-guard | 1× | 1 | · | part |
| 8.4 | Leveling Foot | folding-carton-gluer-leveling-foot | 8× | 8 | · | part |
| 8.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Slitter Rewinder
528 parts · shares 6 with this page
Automatic Screen Printing Machine
640 parts · shares 3 with this page
 Automatic Strapping Machine
251 parts · shares 7 with this page
 Film Laminating Machine
229 parts · shares 7 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$3M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| heidelberg.com ↗ | Heidelberg, DE | Printing presses | 10 units | 12–22 wks |
|
🇨🇭Bobst
bobst.com ↗
|
Lausanne, CH | Packaging machinery | 10 units | 12–22 wks |
| koenig-bauer.com ↗ | Würzburg, DE | Printing presses | 10 units | 12–22 wks |
| wuh-group.com ↗ | Lengerich, DE | Flexible packaging machines | 10 units | 12–22 wks |
| markandy.com ↗ | Chesterfield, US | Label presses | 10 units | 12–22 wks |
953-word article