Blister Packaging Machine
ProductOverview
A blister packaging machine makes the familiar push-through pack: a clear formed pocket holding a tablet, capsule, or small part, sealed under a foil lid you peel or punch through. It is the dominant pack for solid-dose pharmaceuticals because it gives each dose its own sealed, dated, tamper-evident cavity. The machine works as a line of indexed stations: a film web is heated and formed into cavities, product is dropped in, lidding foil is sealed over the top, the foil is coded, and the web is punched into finished cards.
The web steps through the Frame and Drive one pitch per cycle. The Forming Film Feed supplies the forming film, the Forming Station station shapes the cavities, the Product Feeder station fills them, the Sealing Station station applies the lid, the Embossing and Coding station marks each card, and the Punching Station station cuts them out. The Control Cabinet cabinet times the whole sequence.
Forming the cavities
The forming film is most often rigid PVC, sometimes laminated with PVDC for a better moisture barrier, or a cold-form aluminium laminate for products that need a total light and moisture barrier. The Forming Film Feed pays the reel off under tension held by the Dancer Arm, with a Splice Table so a new reel can be taped on without stopping.
In the Forming Station station the Heating Plate warms thermoform film to its softening point, typically around 130 to 140 degrees for PVC. The hot film is then shaped against a cooled Forming Mold, usually with a Plug Assist that pushes the film partway into each cavity first so the walls come out an even thickness, followed by compressed air or vacuum that presses the film fully into the mold. Cold-form aluminium does not use heat: it is mechanically stamped into shape by a punch, because the laminate stretches rather than melts.
Filling and inspection
The Product Feeder station drops one item into each cavity. A Vibratory Feeder walks tablets or capsules down a Feed Channel aligned over the cavity rows, and a Brush Box sweeps any product sitting on the web land into the empty cavities and clears the sealing surface. Stray product left on the seal land would spoil the seal, so this clean-off matters.
Before sealing, the Inspection Camera inspects every cavity to confirm it holds exactly one good tablet. A missing, broken or doubled tablet triggers the Reject Valve to mark or divert that card downstream. In pharma this hundred-percent check is a regulatory expectation, not an option.
Sealing and coding
The Sealing Station station unwinds printed aluminium lidding foil from the Lidding Foil Reel and presses it onto the filled web under the heated Sealing Platen. The platen carries the blister pattern so it seals only the land around each cavity, fusing the foil's heat-seal lacquer to the film. A Knurling Roller embosses the characteristic cross-hatch over the seal, which strengthens it and gives the pack its look. Seal temperature is held by a PID loop on the Seal Thermocouple; under-sealing leaks, over-sealing burns through the foil.
The Embossing and Coding station then marks each card. An Embossing Wheel presses the batch number and expiry into the foil, a Print Head adds a readable printed code, and a Perforator cuts tear lines so a single dose can be snapped off.
Punching, control and use
Finally the Punching Station station cuts the sealed, coded web into finished cards. A Punch Die driven by a Servo Motor stamps the card outline, and the Scrap Winder reels up the leftover web skeleton. The cards collect in the Discharge stacker and feed a downstream cartoner.
The Control Cabinet cabinet holds the PLC, the Servo Drive units that keep the index, seal and punch in registration, and the Temperature Controller modules for each heated plate. The operator sets film type, forming and seal temperatures, and card format on the HMI Touchscreen.
The machine runs 100 to 400 blisters a minute depending on web width and format. Web width sets how many cavities fit across, and the index pitch sets how many rows advance per stroke, so a wide-web machine running a small tablet reaches the top of that range. Heat-form PVC machines are faster than cold-form aluminium machines, because the aluminium has to be stamped slowly to avoid pinholing the foil, but cold-form gives the moisture barrier that hygroscopic drugs need.
Pharmaceutical packers are the main users, where the sealed dose, the batch coding, and the missing-tablet inspection are all required by regulation. The same machine packs chewing gum, lozenges, small hardware and electronic components in blister cards for retail display. Changeover from one product to another means swapping the forming mold, the sealing platen and the punch die, and reloading the feed channels to the new cavity layout, which on a well-designed machine is a tooled set that exchanges in under an hour.
Higher-output lines pair the machine with an inline cartoner and a serialization printer so each pack is formed, filled, sealed, coded, boxed and given a unique serial number in one continuous run. That end-to-end line is what lets a single operator produce traceable, sealed, retail-ready cartons of medicine at the rate a large pharmacy or hospital supply chain needs.
Blister Packaging Machine parts and their functions
9 top-level parts · 256 parts in total · full bill of materials below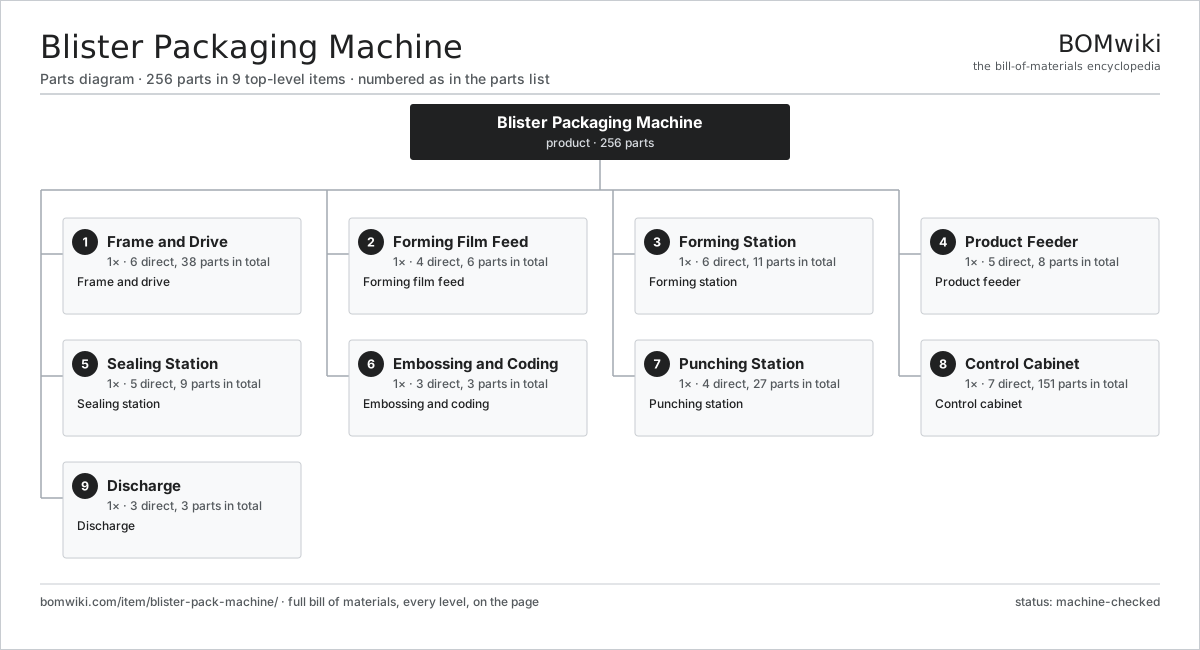
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Frame and Drive 6 parts | 1× | Frame and drive |
| 2 | Forming Film Feed 4 parts | 1× | Forming film feed |
| 3 | Forming Station 6 parts | 1× | Forming station |
| 4 | Product Feeder 5 parts | 1× | Product feeder |
| 5 | Sealing Station 5 parts | 1× | Sealing station |
| 6 | Embossing and Coding 3 parts | 1× | Embossing and coding |
| 7 | Punching Station 4 parts | 1× | Punching station |
| 8 | Control Cabinet 7 parts | 1× | Control cabinet |
| 9 | Discharge 3 parts | 1× | Discharge |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Blister Packaging Machine
9 top-level lines · 71 rows shown · 256 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Frame and Drive 6 parts | blister-pack-machine-frame | 1× | 1 | 38 | assembly |
| 1.1 | Machine Base | blister-pack-machine-base | 1× | 1 | · | part |
| 1.2 | Index Feed Unit | blister-pack-machine-index-feed | 1× | 1 | · | part |
| 1.3 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 1.3.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 1.3.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 1.3.3 | Encoder | encoder | 1× | 1 | · | part |
| 1.3.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 1.4 | Transport Rail | blister-pack-machine-chain-rail | 2× | 2 | · | part |
| 1.5 | Sheet Metal Panel | sheet-panel | 4× | 4 | · | part |
| 1.6 | Ball Bearing | ball-bearing | 6× | 6 | · | part |
| 2 | Forming Film Feed 4 parts | blister-pack-machine-film-feed | 1× | 1 | 6 | assembly |
| 2.1 | Film Reel Shaft | blister-pack-machine-film-reel | 1× | 1 | · | part |
| 2.2 | Dancer Arm | blister-pack-machine-film-dancer | 1× | 1 | · | part |
| 2.3 | Guide Roller | blister-pack-machine-film-roller | 3× | 3 | · | part |
| 2.4 | Splice Table | blister-pack-machine-splice-table | 1× | 1 | · | part |
| 3 | Forming Station 6 parts | blister-pack-machine-forming | 1× | 1 | 11 | assembly |
| 3.1 | Heating Plate | blister-pack-machine-heat-plate | 2× | 2 | · | part |
| 3.2 | Heating Element | heating-element | 4× | 4 | · | part |
| 3.3 | Forming Mold | blister-pack-machine-form-mold | 1× | 1 | · | part |
| 3.4 | Plug Assist | blister-pack-machine-plug-assist | 1× | 1 | · | part |
| 3.5 | Form Thermocouple | blister-pack-machine-form-thermocouple | 2× | 2 | · | part |
| 3.6 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 4 | Product Feeder 5 parts | blister-pack-machine-feeding | 1× | 1 | 8 | assembly |
| 4.1 | Feed Channel | blister-pack-machine-feed-channel | 1× | 1 | · | part |
| 4.2 | Vibratory Feeder | blister-pack-machine-vibratory-feeder | 1× | 1 | · | part |
| 4.3 | Brush Box | blister-pack-machine-brush-box | 1× | 1 | · | part |
| 4.4 | Inspection Camera 2 parts | blister-pack-machine-vision-camera | 1× | 1 | 4 | assembly |
| 4.4.1 | Camera Module 3 parts + deeper › | camera-module | 1× | 1 | 3 | assembly |
| 4.4.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 4.5 | Reject Valve | blister-pack-machine-reject-valve | 1× | 1 | · | part |
| 5 | Sealing Station 5 parts | blister-pack-machine-sealing | 1× | 1 | 9 | assembly |
| 5.1 | Lidding Foil Reel | blister-pack-machine-lid-reel | 1× | 1 | · | part |
| 5.2 | Sealing Platen | blister-pack-machine-seal-platen | 1× | 1 | · | part |
| 5.3 | Heating Element | heating-element | 4× | 4 | · | part |
| 5.4 | Seal Thermocouple | blister-pack-machine-seal-thermocouple | 2× | 2 | · | part |
| 5.5 | Knurling Roller | blister-pack-machine-knurl-roller | 1× | 1 | · | part |
| 6 | Embossing and Coding 3 parts | blister-pack-machine-coding | 1× | 1 | 3 | assembly |
| 6.1 | Embossing Wheel | blister-pack-machine-emboss-wheel | 1× | 1 | · | part |
| 6.2 | Print Head | blister-pack-machine-print-head | 1× | 1 | · | part |
| 6.3 | Perforator | blister-pack-machine-perforator | 1× | 1 | · | part |
| 7 | Punching Station 4 parts | blister-pack-machine-punching | 1× | 1 | 27 | assembly |
| 7.1 | Punch Die | blister-pack-machine-punch-die | 1× | 1 | · | part |
| 7.2 | Punch Press | blister-pack-machine-punch-press | 1× | 1 | · | part |
| 7.3 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 7.3.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 7.3.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 7.3.3 | Encoder | encoder | 1× | 1 | · | part |
| 7.3.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 7.4 | Scrap Winder | blister-pack-machine-scrap-winder | 1× | 1 | · | part |
| 8 | Control Cabinet 7 parts | blister-pack-machine-control | 1× | 1 | 151 | assembly |
| 8.1 | PLC 3 parts | blister-pack-machine-plc | 1× | 1 | 122 | assembly |
| 8.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.1.3 | SMD Passive (R/C/L) | smd-passives | 120× | 120 | · | part |
| 8.2 | HMI Touchscreen 3 parts | blister-pack-machine-hmi | 1× | 1 | 3 | assembly |
| 8.2.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.2.2 | Touch Digitizer | touch-digitizer | 1× | 1 | · | part |
| 8.2.3 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.3 | Servo Drive 3 parts | blister-pack-machine-servo-drive | 3× | 3 | 4 | assembly |
| 8.3.1 | Bare PCB | pcb-bare | 1× | 3 | · | part |
| 8.3.2 | IGBT Power Module | igbt-module | 1× | 3 | · | part |
| 8.3.3 | DC-Link Capacitor | dc-link-cap | 2× | 6 | · | part |
| 8.4 | Temperature Controller | blister-pack-machine-temp-controller | 4× | 4 | · | part |
| 8.5 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.6 | Relay | relay | 8× | 8 | · | part |
| 8.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9 | Discharge 3 parts | blister-pack-machine-discharge | 1× | 1 | 3 | assembly |
| 9.1 | Card Stacker | blister-pack-machine-card-stacker | 1× | 1 | · | part |
| 9.2 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 9.3 | Discharge Motor | blister-pack-machine-discharge-motor | 1× | 1 | · | part |
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$3M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| heidelberg.com ↗ | Heidelberg, DE | Printing presses | 10 units | 12–22 wks |
|
🇨🇭Bobst
bobst.com ↗
|
Lausanne, CH | Packaging machinery | 10 units | 12–22 wks |
| koenig-bauer.com ↗ | Würzburg, DE | Printing presses | 10 units | 12–22 wks |
| wuh-group.com ↗ | Lengerich, DE | Flexible packaging machines | 10 units | 12–22 wks |
| markandy.com ↗ | Chesterfield, US | Label presses | 10 units | 12–22 wks |
991-word article