Stick Pack Machine
ProductOverview
A stick pack machine makes the slim single-serve sachets used for instant coffee, sugar, drink mixes, salt, and powdered supplements. It is closely related to a vertical form-fill-seal machine, but instead of one wide bag it runs several narrow lanes side by side, each forming a thin tube that becomes a stick. A single film web from the Film Unwind is slit into strips, the Forming Stations shape each strip into a tube, the Vertical Sealers close each back seam, the Dosing System drops one serving into every lane at once, and the Cross Seal & Cut seals the ends and separates the finished sticks. The Control System keeps every lane in step and the Frame & Guarding stacks it into a hygienic tower.
Running many lanes in parallel is what gives the machine its speed: a single index produces one stick per lane, so an eight-lane machine makes eight sticks every cycle.
How it works
The cycle is the same form-fill-seal idea as a VFFS machine, repeated across lanes. One wide film reel feeds the Slitter, which divides it into the narrow strips that each lane needs. Each strip runs up to its own Forming Collar, a small shoulder that folds it into a slim tube around a thin Fill Tube. The Vertical Sealers press a heated Seal Bar down the overlap of each tube to make a centre fin seam, the seal that runs down the back of a stick. The film is then indexed down by one stick length for every lane together.
At the bottom the full-width Cross Jaw pair closes across all lanes at once, sealing the top of the sticks just filled and the bottom of the sticks about to be filled. With fresh sealed-bottom tubes open at the top, the Dosing System releases one serving into every lane simultaneously. The next cross seal closes the stick tops, and the Lane Knife separates the sealed web into individual sticks, cutting both between lanes and across between seals.
Film handling across lanes
Because every lane must match, film control is more demanding than on a single-bag machine. The Reel Shaft feeds under brake, the Dancer Arm smooths the tension swings of the intermittent multi-lane pull, and the Registration Sensor reads a print mark so all lanes index exactly one stick length per cycle and the printed graphic stays square on every stick. The slit lanes are routed by Film Roller idlers into the row of forming collars held in line by the Collar Plate.
Dosing
Stick packs almost always carry powders or fine granules, so dosing is volumetric. Each lane has its own Auger Filler, a screw that meters a fixed volume per turn, driven by a Auger Motor that turns a counted number of revolutions to deliver one serving. All augers draw from a shared Product Hopper kept flowing by an Agitator so every lane receives the same fill. The dosed servings drop through a Dosing Funnel into each Fill Tube. For liquids or gels the augers are replaced by piston pumps, but the per-lane parallel layout is unchanged.
Sealing and cutting
Seal quality matters more on a stick because the pack is mostly seal area relative to its tiny volume. The back fin seam from the Seal Bar and the end seals from the Cross Jaw are each held at the film's sealing window by a Seal Thermocouple and Crimp Thermocouple. The jaw faces are serrated to spread heat and squeeze out trapped powder so the seal is not contaminated, a common failure mode when fine product dusts up into the seal zone. The Lane Knife then cuts the multi-up web into separate sticks.
Controls, frame, and use
The Control System runs a Motion Controller that indexes the film and times the cross jaws and all the augers so every lane doses into a sealed-bottom stick on the same cycle. The PLC handles recipe, temperatures, auger counts, and faults, shown on the LCD Panel. The Machine Frame is a stainless tower with the hopper and augers above the multi-lane former and sealer so product falls straight down by gravity, guarded by Guard Interlock switches around the heated jaws. Stick packs suit small fixed portions: a single coffee serving, one sugar dose, a measured scoop of supplement, where the slim shape is easy to carry, tear open, and pour. Compared with a sachet machine that makes flatter four-side-seal pouches, the stick is rounder and longer and is built for pouring a single serve, which is why it dominates portion-control packaging for beverages and nutrition.
Stick Pack Machine parts and their functions
7 top-level parts · 189 parts in total · full bill of materials below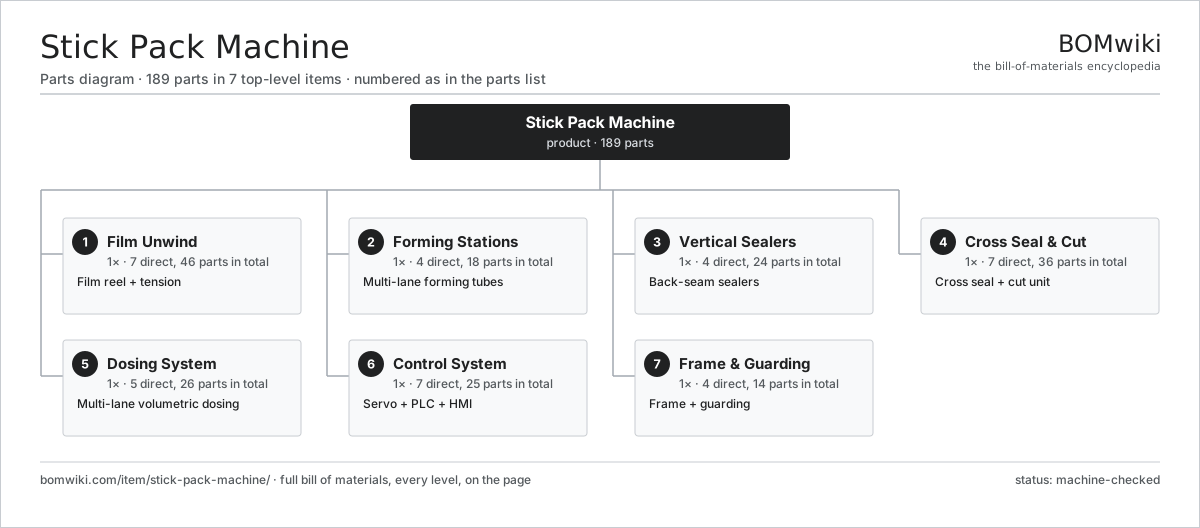
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Film Unwind 7 parts | 1× | Film reel + tension |
| 2 | Forming Stations 4 parts | 1× | Multi-lane forming tubes |
| 3 | Vertical Sealers 4 parts | 1× | Back-seam sealers |
| 4 | Cross Seal & Cut 7 parts | 1× | Cross seal + cut unit |
| 5 | Dosing System 5 parts | 1× | Multi-lane volumetric dosing |
| 6 | Control System 7 parts | 1× | Servo + PLC + HMI |
| 7 | Frame & Guarding 4 parts | 1× | Frame + guarding |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Stick Pack Machine
7 top-level lines · 53 rows shown · 189 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Film Unwind 7 parts | spm-film-unwind | 1× | 1 | 46 | assembly |
| 1.1 | Reel Shaft | spm-reel-shaft | 1× | 1 | · | part |
| 1.2 | Dancer Arm | spm-dancer-arm | 1× | 1 | · | part |
| 1.3 | Slitter | spm-slitter | 1× | 1 | · | part |
| 1.4 | Registration Sensor | spm-registration-sensor | 1× | 1 | · | part |
| 1.5 | Film Roller | spm-film-roller | 8× | 8 | · | part |
| 1.6 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 1.6.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 1.6.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 1.6.3 | Encoder | encoder | 1× | 1 | · | part |
| 1.6.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 1.7 | Ball Bearing | ball-bearing | 10× | 10 | · | part |
| 2 | Forming Stations 4 parts | spm-forming-stations | 1× | 1 | 18 | assembly |
| 2.1 | Forming Collar | spm-forming-collar | 8× | 8 | · | part |
| 2.2 | Fill Tube | spm-fill-tube | 8× | 8 | · | part |
| 2.3 | Collar Plate | spm-collar-plate | 1× | 1 | · | part |
| 2.4 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 3 | Vertical Sealers 4 parts | spm-vertical-sealers | 1× | 1 | 24 | assembly |
| 3.1 | Seal Bar | spm-seal-bar | 8× | 8 | · | part |
| 3.2 | Heating Element | heating-element | 4× | 4 | · | part |
| 3.3 | Seal Thermocouple | spm-seal-thermocouple | 4× | 4 | · | part |
| 3.4 | Coil Spring | coil-spring | 8× | 8 | · | part |
| 4 | Cross Seal & Cut 7 parts | spm-cross-seal-cut | 1× | 1 | 36 | assembly |
| 4.1 | Cross Jaw | spm-cross-jaw | 2× | 2 | · | part |
| 4.2 | Jaw Heater | spm-jaw-heater | 4× | 4 | · | part |
| 4.3 | Lane Knife | spm-lane-knife | 1× | 1 | · | part |
| 4.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 4.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 4.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 4.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 4.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 4.5 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 4.6 | Crimp Thermocouple | spm-crimp-thermocouple | 2× | 2 | · | part |
| 4.7 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 5 | Dosing System 5 parts | spm-dosing-system | 1× | 1 | 26 | assembly |
| 5.1 | Auger Filler | spm-auger-filler | 8× | 8 | · | part |
| 5.2 | Auger Motor | spm-auger-motor | 8× | 8 | · | part |
| 5.3 | Product Hopper | spm-product-hopper | 1× | 1 | · | part |
| 5.4 | Agitator | spm-agitator | 1× | 1 | · | part |
| 5.5 | Dosing Funnel | spm-dosing-funnel | 8× | 8 | · | part |
| 6 | Control System 7 parts | spm-control-system | 1× | 1 | 25 | assembly |
| 6.1 | Motion Controller | spm-motion-controller | 1× | 1 | · | part |
| 6.2 | PLC | spm-plc | 1× | 1 | · | part |
| 6.3 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 6.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 6.5 | Relay | relay | 8× | 8 | · | part |
| 6.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 6.7 | Connector | connector | 12× | 12 | · | part |
| 7 | Frame & Guarding 4 parts | spm-frame-guard | 1× | 1 | 14 | assembly |
| 7.1 | Machine Frame | spm-machine-frame | 1× | 1 | · | part |
| 7.2 | Sheet Metal Panel | sheet-panel | 6× | 6 | · | part |
| 7.3 | Guard Interlock | spm-guard-interlock | 3× | 3 | · | part |
| 7.4 | Leveling Foot | spm-leveling-foot | 4× | 4 | · | part |
Related products
same domain, ranked by shared parts Industrial Screen Printing Press
162 parts · shares 7 with this page
Gravity Filling Machine
177 parts · shares 6 with this page
 Digital Inkjet Web Press
3,001 parts · shares 6 with this page
Ream Wrapping Machine
540 parts · shares 6 with this page
 Piston Filling Machine
112 parts · shares 5 with this page
Film Bundling Machine
437 parts · shares 6 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$3M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| heidelberg.com ↗ | Heidelberg, DE | Printing presses | 10 units | 12–22 wks |
|
🇨🇭Bobst
bobst.com ↗
|
Lausanne, CH | Packaging machinery | 10 units | 12–22 wks |
| koenig-bauer.com ↗ | Würzburg, DE | Printing presses | 10 units | 12–22 wks |
| wuh-group.com ↗ | Lengerich, DE | Flexible packaging machines | 10 units | 12–22 wks |
| markandy.com ↗ | Chesterfield, US | Label presses | 10 units | 12–22 wks |
813-word article