Poly Bag Making Machine
ProductOverview
A poly bag making machine converts a reel of plastic film into finished bags by heat-sealing and cutting the film, with no glue involved. Plastic film welds to itself when heated past its melting point and pressed, so a bag is made by sealing across the film and cutting it free. The machine pulls a measured length of film on each cycle, seals across the web, and cuts the bag at or beside the seal. From one base machine come grocery bags, garment bags, bread bags, mailing bags, and the wicketed bags that fill automatic packing lines.
Film runs from the Film Unwind through the Tension and Tracking section, is pulled to length by the Servo Film Feed, and welded and cut at the Seal and Cut Station. A Handle and Gusset Punch station adds handles or gussets, the Seal Cooling sets the seal, and the Output and Stacker collects finished bags. The Control System system times the cycle and holds the seal temperature.
Film handling
Plastic film is thin and stretchy, so the Film Unwind and Tension and Tracking sections must handle it gently. The reel sits on an air Unwind Shaft, and a Unwind Motor pays film off to match demand so the web is not pulled tight against a braked reel. A Spreader Roll flattens wrinkles. In the tension section, a Dancer Roll roll floats to absorb the difference between steady unwinding and the stop-start pull of the bag cycle, which keeps the elastic film from stretching unevenly. An Edge Sensor and a Steering Frame steer the web straight. Film that wanders or stretches gives crooked seals and wrong-length bags.
Setting the bag length
The Servo Film Feed sets bag length, the single most important dimension. A pair of Nip Feed Roll nip rolls driven by a servo grip the film and advance it an exact distance each cycle, measured by the Feed Encoder. For printed film, a Registration Eye reads a registration mark so each bag is cut in the same place relative to the artwork rather than at a fixed length that would slowly drift off the print. Servo feed gives both repeatable length and the fast index-and-stop motion the seal needs, since the film must be still while the seal bar is down.
Sealing and cutting
The Seal and Cut Station is where the bag is made. Two common methods exist. A hot bar seal uses a heated Heat Seal Bar, held at temperature by a Heating Element and a Seal Thermocouple, that presses the film against a silicone Backing Rubber to weld a wide seal, with a separate knife cutting the bag. A hot wire method uses a single Seal and Cut Wire of nichrome that melts a narrow seal and cuts the film in the same stroke, common for side-weld bags. A PTFE Cover Tape cover stops molten film sticking to the bar, and a Seal Pressure Cylinder drives the seal down with set force. Seal temperature, dwell time, and pressure together decide seal strength: too cold and the seal peels, too hot and the film burns through.
Handles, gussets, and cooling
For carry bags, the Handle and Gusset Punch station adds features. A Punch Die driven by a Punch Cylinder cuts patch handles or the holes that hang a bag on a wicket, and a Scrap Blower clears the chads. Gusset Plate plates tuck the film sides in to make side gussets so the bag opens out for bulky goods. A fresh plastic seal is weak until it cools, so the Seal Cooling section grips the seal on a water-cooled Cooling Bar and a Cooling Fan blows across it. Skipping cooling lets the seal pull apart in the stacker.
Output and control
Finished bags collect at the Output and Stacker. Wicketed bags are caught by their punched holes on Wicket Pins pins to build a stack that loads straight onto a filling line, while plain bags ride a Output Conveyor and are counted into bundles by a Bag Counter. The Control System system runs the cycle: the Machine Controller times the feed, seal, and punch, while a Temperature Controller holds the seal bar at its PID setpoint. Bag jobs are stored so a repeat order recalls length, seal time, and punch position.
Bag styles and use
The base machine makes several styles by changing the seal method and the punch tooling. A bottom-seal bag is welded across the bottom from flat film, a side-weld bag is sealed and cut by the same hot wire, and gusseted or wicketed bags add the punch and gusset stations. Plastic bags remain the cheapest way to wrap and carry goods, so these machines serve food, retail, garment, and industrial packers, and the wicketed output feeds high-speed automatic baggers. Bag length accuracy, seal reliability, and clean cutting are the measures buyers check, alongside how quickly the machine changes from one bag size to the next.
Poly Bag Making Machine parts and their functions
8 top-level parts · 79 parts in total · full bill of materials below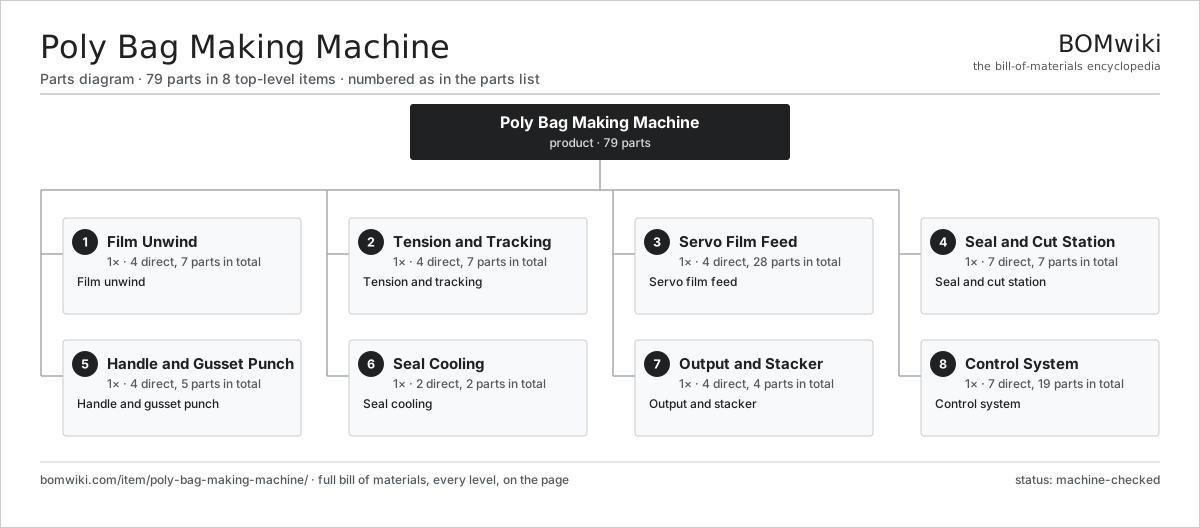
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Film Unwind 4 parts | 1× | Film unwind |
| 2 | Tension and Tracking 4 parts | 1× | Tension and tracking |
| 3 | Servo Film Feed 4 parts | 1× | Servo film feed |
| 4 | Seal and Cut Station 7 parts | 1× | Seal and cut station |
| 5 | Handle and Gusset Punch 4 parts | 1× | Handle and gusset punch |
| 6 | Seal Cooling 2 parts | 1× | Seal cooling |
| 7 | Output and Stacker 4 parts | 1× | Output and stacker |
| 8 | Control System 7 parts | 1× | Control system |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Poly Bag Making Machine
8 top-level lines · 51 rows shown · 79 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Film Unwind 4 parts | poly-bag-making-machine-unwind | 1× | 1 | 7 | assembly |
| 1.1 | Unwind Shaft | poly-bag-making-machine-unwind-shaft | 1× | 1 | · | part |
| 1.2 | Unwind Motor | poly-bag-making-machine-unwind-motor | 1× | 1 | · | part |
| 1.3 | Spreader Roll | poly-bag-making-machine-spreader-roll | 1× | 1 | · | part |
| 1.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 2 | Tension and Tracking 4 parts | poly-bag-making-machine-tension | 1× | 1 | 7 | assembly |
| 2.1 | Dancer Roll | poly-bag-making-machine-dancer | 1× | 1 | · | part |
| 2.2 | Edge Sensor | poly-bag-making-machine-edge-sensor | 1× | 1 | · | part |
| 2.3 | Steering Frame | poly-bag-making-machine-guide-frame | 1× | 1 | · | part |
| 2.4 | Idler Roll | poly-bag-making-machine-idler | 4× | 4 | · | part |
| 3 | Servo Film Feed 4 parts | poly-bag-making-machine-feed | 1× | 1 | 28 | assembly |
| 3.1 | Nip Feed Roll | poly-bag-making-machine-feed-roll | 2× | 2 | · | part |
| 3.2 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 3.2.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 3.2.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 3.2.3 | Encoder | encoder | 1× | 1 | · | part |
| 3.2.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 3.3 | Registration Eye | poly-bag-making-machine-photo-eye | 1× | 1 | · | part |
| 3.4 | Feed Encoder | poly-bag-making-machine-feed-encoder | 1× | 1 | · | part |
| 4 | Seal and Cut Station 7 parts | poly-bag-making-machine-seal-station | 1× | 1 | 7 | assembly |
| 4.1 | Heat Seal Bar | poly-bag-making-machine-seal-bar | 1× | 1 | · | part |
| 4.2 | Heating Element | heating-element | 1× | 1 | · | part |
| 4.3 | Seal and Cut Wire | poly-bag-making-machine-seal-wire | 1× | 1 | · | part |
| 4.4 | PTFE Cover Tape | poly-bag-making-machine-teflon-tape | 1× | 1 | · | part |
| 4.5 | Seal Pressure Cylinder | poly-bag-making-machine-seal-cylinder | 1× | 1 | · | part |
| 4.6 | Backing Rubber | poly-bag-making-machine-seal-rubber | 1× | 1 | · | part |
| 4.7 | Seal Thermocouple | poly-bag-making-machine-temp-sensor | 1× | 1 | · | part |
| 5 | Handle and Gusset Punch 4 parts | poly-bag-making-machine-punch | 1× | 1 | 5 | assembly |
| 5.1 | Punch Die | poly-bag-making-machine-punch-die | 1× | 1 | · | part |
| 5.2 | Punch Cylinder | poly-bag-making-machine-punch-cylinder | 1× | 1 | · | part |
| 5.3 | Gusset Plate | poly-bag-making-machine-gusset-plate | 2× | 2 | · | part |
| 5.4 | Scrap Blower | poly-bag-making-machine-scrap-blower | 1× | 1 | · | part |
| 6 | Seal Cooling 2 parts | poly-bag-making-machine-cooling | 1× | 1 | 2 | assembly |
| 6.1 | Cooling Bar | poly-bag-making-machine-cool-bar | 1× | 1 | · | part |
| 6.2 | Cooling Fan | poly-bag-making-machine-cool-fan | 1× | 1 | · | part |
| 7 | Output and Stacker 4 parts | poly-bag-making-machine-output | 1× | 1 | 4 | assembly |
| 7.1 | Wicket Pins | poly-bag-making-machine-wicket | 1× | 1 | · | part |
| 7.2 | Output Conveyor | poly-bag-making-machine-conveyor | 1× | 1 | · | part |
| 7.3 | Bag Counter | poly-bag-making-machine-counter | 1× | 1 | · | part |
| 7.4 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 8 | Control System 7 parts | poly-bag-making-machine-control | 1× | 1 | 19 | assembly |
| 8.1 | Machine Controller 3 parts | poly-bag-making-machine-controller | 1× | 1 | 3 | assembly |
| 8.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.1.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 8.2 | Temperature Controller | poly-bag-making-machine-temp-controller | 1× | 1 | · | part |
| 8.3 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.5 | Relay | relay | 6× | 6 | · | part |
| 8.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8.7 | Connector | connector | 6× | 6 | · | part |
Related products
same domain, ranked by shared parts Automatic Strapping Machine
251 parts · shares 4 with this page
 Blister Packaging Machine
256 parts · shares 4 with this page
Carton Overwrapping Machine
261 parts · shares 4 with this page
Case Labeling Machine
120 parts · shares 4 with this page
 Digital Inkjet Web Press
3,001 parts · shares 4 with this page
Doypack Pouch Filling Machine
289 parts · shares 4 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$3M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| heidelberg.com ↗ | Heidelberg, DE | Printing presses | 10 units | 12–22 wks |
|
🇨🇭Bobst
bobst.com ↗
|
Lausanne, CH | Packaging machinery | 10 units | 12–22 wks |
| koenig-bauer.com ↗ | Würzburg, DE | Printing presses | 10 units | 12–22 wks |
| wuh-group.com ↗ | Lengerich, DE | Flexible packaging machines | 10 units | 12–22 wks |
| markandy.com ↗ | Chesterfield, US | Label presses | 10 units | 12–22 wks |
959-word article