Automatic Strapping Machine
ProductOverview
An automatic strapping machine wraps a tensioned band of plastic or steel strap around a package, joins the overlap into a closed loop, and cuts it free of the supply coil. It does the job a worker would do with a hand tool, but in a fixed cycle of roughly one to two seconds per strap. The machine sits at the end of a packing line, in a shipping room, or beside a carton sealer, and is used to unitise cartons, bundle boards and pipes, hold pallet loads, and close cases that are too heavy for tape alone. The package is pushed into the open Strap Arch, the strap is fed around it, pulled tight, welded, and cut, and the package leaves with a finished band. A full cycle runs without operator input once the package is in position.
How a strap cycle works
The cycle begins with strap already threaded through the arch track and its tip held in the Sealing Head. When a package is detected, the Strap Feed Unit reverses and retracts the strap. The Track Flap elements in the arch release in sequence, so the strap pulls out of the channel and snaps down onto the package surface. The Front Gripper holds the leading tip while the Tensioner pulls the loop tight against the box. Once the set tension is reached, the Rear Gripper clamps the supply strand, the Weld Unit joins the two layers, the Cutter severs the strap, and the feed unit pushes a fresh tip back around the arch ready for the next package. The whole sequence is timed by the Head Cam, a profiled cam shaft that drives the grippers, welder and cutter from one shaft so their motions cannot collide.
Strap supply and feed
Strap comes on a coil mounted to the Coil Holder, which carries a friction Reel Brake to stop the coil from overrunning when the feed stops. Because the feed unit pulls strap faster than a heavy coil can spin up, the machine buffers a loop of loose strap in the Strap Accumulator. A Strap Detector watches the buffer level and tells the coil drive when to pay out more, so the Strap Feed Unit always pulls from slack strap. The feed unit itself is a Feed Roller driven by a reversible Feed Motor, with a spring-loaded Pinch Roller holding the strap against it. The same rollers feed the strap forward through the arch and retract it during tensioning, so feed direction is controlled by the motor rather than by separate mechanisms.
The arch and how strap is placed
The Strap Arch is the open rectangular guide that surrounds the package opening. Its Arch Track is a continuous channel that carries the strap tip all the way around the loop, with Arch Guide deflectors steering the strap around each corner. The arch size sets the largest package the machine can strap, from a 600 × 600 mm table-top unit up to a 1250 × 1000 mm frame for pallet-edge work. The clever part is the release: the strap is held in the channel only until tensioning begins, then the spring flaps let go and the strap is drawn out of the track and onto the package. This is what lets one feed motion both place and tighten the strap.
Sealing the overlap
Most modern machines use friction welding. The Vibration Welder presses the two overlapping strap layers together against the Weld Anvil and rubs them at high frequency. The friction melts a thin layer of the polypropylene or polyester, and when the motion stops the melt cools and fuses the layers into a joint that holds 70 to 85 percent of the strap break load. Friction welding needs no consumables and works on both PP and PET. Older and lighter machines instead use a Heating Element heat-seal blade that is driven between the strap layers, withdrawn, and the layers pressed together while the surfaces are molten. Steel-strap machines do not weld at all; they crimp a metal seal or make a notch joint, which is why steel models are built around a heavier head and frame.
Tension control
Tension is what makes a strap hold a load, and it is set on the HMI rather than by mechanical adjustment. The Tension Wheel grips the strap and the Tension Motor, a servo with a reduction gearbox, retracts it until a Pressure Sensor reads the target. Light cartons might be strapped at 150 to 300 N to avoid crushing, while bundled timber or a pallet edge can take 1500 to 2500 N. Closed-loop control means the same tension is applied to every package regardless of how compressible it is, which matters when soft and rigid loads run on the same line.
Conveyor, drive and control
The package rides on the Package Conveyor, a powered roller table that carries it into the arch where the Package Stop halts it in the strap path. A Package Sensor confirms position before the cycle starts. The Main Drive supplies the base power, with an electromagnetic Clutch Brake that stops the cam shaft at its home position so the head is always ready. The Control System runs the sequence through a PLC Module, with the HMI Panel used to set tension, strap width, weld time and strap count for multiple bands per package. The Safety Relay and interlocked Safety Guarding keep the operator clear of the sealing head and drive while the machine cycles.
Automatic Strapping Machine parts and their functions
9 top-level parts · 251 parts in total · full bill of materials below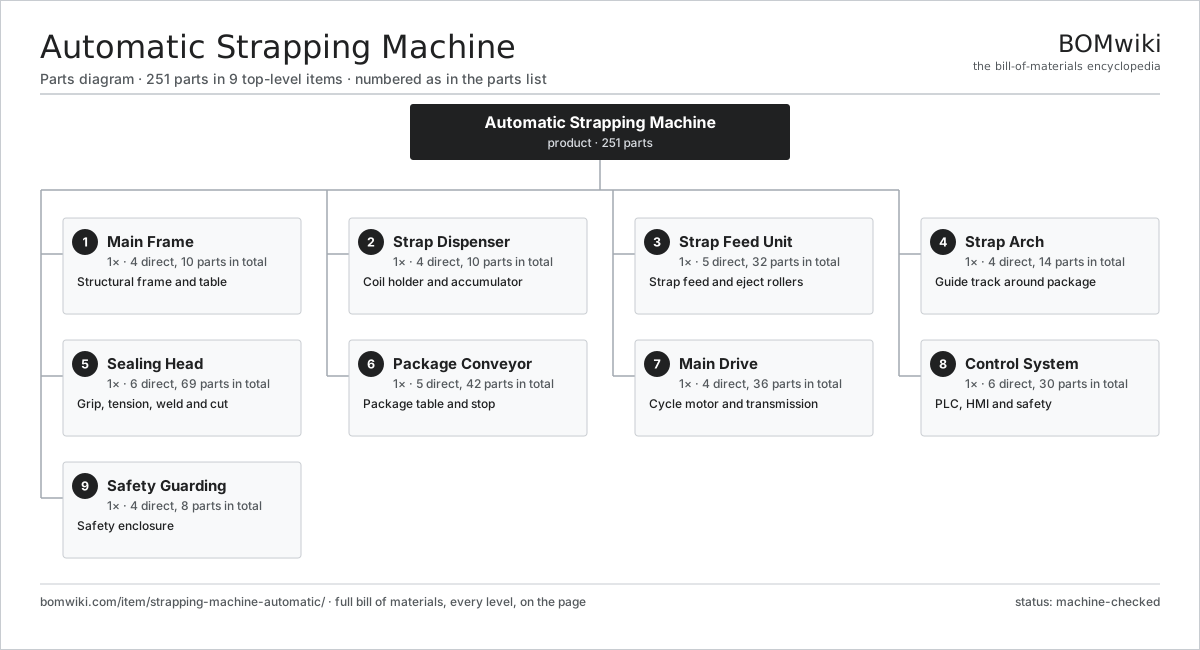
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Main Frame 4 parts | 1× | Structural frame and table |
| 2 | Strap Dispenser 4 parts | 1× | Coil holder and accumulator |
| 3 | Strap Feed Unit 5 parts | 1× | Strap feed and eject rollers |
| 4 | Strap Arch 4 parts | 1× | Guide track around package |
| 5 | Sealing Head 6 parts | 1× | Grip, tension, weld and cut |
| 6 | Package Conveyor 5 parts | 1× | Package table and stop |
| 7 | Main Drive 4 parts | 1× | Cycle motor and transmission |
| 8 | Control System 6 parts | 1× | PLC, HMI and safety |
| 9 | Safety Guarding 4 parts | 1× | Safety enclosure |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Automatic Strapping Machine
9 top-level lines · 92 rows shown · 251 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Main Frame 4 parts | strapping-machine-automatic-main-frame | 1× | 1 | 10 | assembly |
| 1.1 | Frame Weldment | strapping-machine-automatic-frame-weldment | 1× | 1 | · | part |
| 1.2 | Table Top | strapping-machine-automatic-table-top | 1× | 1 | · | part |
| 1.3 | Leveling Foot | strapping-machine-automatic-leveling-foot | 4× | 4 | · | part |
| 1.4 | Sheet Metal Panel | sheet-panel | 4× | 4 | · | part |
| 2 | Strap Dispenser 4 parts | strapping-machine-automatic-strap-dispenser | 1× | 1 | 10 | assembly |
| 2.1 | Coil Holder 3 parts | strapping-machine-automatic-coil-holder | 1× | 1 | 4 | assembly |
| 2.1.1 | Reel Hub | strapping-machine-automatic-reel-hub | 1× | 1 | · | part |
| 2.1.2 | Reel Brake | strapping-machine-automatic-reel-brake | 1× | 1 | · | part |
| 2.1.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 2.2 | Strap Accumulator 2 parts | strapping-machine-automatic-strap-accumulator | 1× | 1 | 3 | assembly |
| 2.2.1 | Accumulator Chamber | strapping-machine-automatic-accumulator-chamber | 1× | 1 | · | part |
| 2.2.2 | Strap Detector | strapping-machine-automatic-strap-detector | 2× | 2 | · | part |
| 2.3 | Strap Guide | strapping-machine-automatic-strap-guide | 2× | 2 | · | part |
| 2.4 | Low Strap Sensor | strapping-machine-automatic-low-strap-sensor | 1× | 1 | · | part |
| 3 | Strap Feed Unit 5 parts | strapping-machine-automatic-feed-unit | 1× | 1 | 32 | assembly |
| 3.1 | Feed Roller | strapping-machine-automatic-feed-roller | 1× | 1 | · | part |
| 3.2 | Pinch Roller | strapping-machine-automatic-pinch-roller | 1× | 1 | · | part |
| 3.3 | Feed Motor 3 parts | strapping-machine-automatic-feed-motor | 1× | 1 | 27 | assembly |
| 3.3.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 3.3.2 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 3.3.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3.4 | Roller Solenoid | strapping-machine-automatic-roller-solenoid | 1× | 1 | · | part |
| 3.5 | Coil Spring | coil-spring | 2× | 2 | · | part |
| 4 | Strap Arch 4 parts | strapping-machine-automatic-strap-arch | 1× | 1 | 14 | assembly |
| 4.1 | Arch Frame | strapping-machine-automatic-arch-frame | 1× | 1 | · | part |
| 4.2 | Arch Track | strapping-machine-automatic-arch-track | 1× | 1 | · | part |
| 4.3 | Track Flap | strapping-machine-automatic-track-flap | 8× | 8 | · | part |
| 4.4 | Arch Guide | strapping-machine-automatic-arch-guide | 4× | 4 | · | part |
| 5 | Sealing Head 6 parts | strapping-machine-automatic-sealing-head | 1× | 1 | 69 | assembly |
| 5.1 | Front Gripper | strapping-machine-automatic-front-gripper | 1× | 1 | · | part |
| 5.2 | Rear Gripper | strapping-machine-automatic-rear-gripper | 1× | 1 | · | part |
| 5.3 | Tensioner 3 parts | strapping-machine-automatic-tensioner | 1× | 1 | 30 | assembly |
| 5.3.1 | Tension Wheel | strapping-machine-automatic-tension-wheel | 1× | 1 | · | part |
| 5.3.2 | Tension Motor 4 parts + deeper › | strapping-machine-automatic-tension-motor | 1× | 1 | 28 | assembly |
| 5.3.3 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 5.4 | Weld Unit 4 parts | strapping-machine-automatic-weld-unit | 1× | 1 | 27 | assembly |
| 5.4.1 | Vibration Welder | strapping-machine-automatic-vibration-welder | 1× | 1 | · | part |
| 5.4.2 | Weld Anvil | strapping-machine-automatic-weld-anvil | 1× | 1 | · | part |
| 5.4.3 | Heating Element | heating-element | 1× | 1 | · | part |
| 5.4.4 | Weld Motor 3 parts + deeper › | strapping-machine-automatic-weld-motor | 1× | 1 | 24 | assembly |
| 5.5 | Cutter | strapping-machine-automatic-cutter | 1× | 1 | · | part |
| 5.6 | Head Cam 4 parts | strapping-machine-automatic-head-cam | 1× | 1 | 9 | assembly |
| 5.6.1 | Cam Shaft | strapping-machine-automatic-cam-shaft | 1× | 1 | · | part |
| 5.6.2 | Cam Follower | strapping-machine-automatic-cam-follower | 4× | 4 | · | part |
| 5.6.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 5.6.4 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 6 | Package Conveyor 5 parts | strapping-machine-automatic-conveyor | 1× | 1 | 42 | assembly |
| 6.1 | Conveyor Roller | strapping-machine-automatic-conveyor-roller | 12× | 12 | · | part |
| 6.2 | Conveyor Motor 4 parts | strapping-machine-automatic-conveyor-motor | 1× | 1 | 25 | assembly |
| 6.2.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 6.2.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 6.2.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 6.2.4 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 6.3 | Package Stop | strapping-machine-automatic-package-stop | 1× | 1 | · | part |
| 6.4 | Package Sensor | strapping-machine-automatic-package-sensor | 2× | 2 | · | part |
| 6.5 | Drive Belt | drive-belt | 2× | 2 | · | part |
| 7 | Main Drive 4 parts | strapping-machine-automatic-main-drive | 1× | 1 | 36 | assembly |
| 7.1 | Cycle Motor 3 parts | strapping-machine-automatic-cycle-motor | 1× | 1 | 24 | assembly |
| 7.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 7.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 7.1.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 7.2 | Drive Gearbox 5 parts | strapping-machine-automatic-drive-gearbox | 1× | 1 | 10 | assembly |
| 7.2.1 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 7.2.2 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 7.2.3 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 7.2.4 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 7.2.5 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 7.3 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 7.4 | Clutch Brake | strapping-machine-automatic-clutch-brake | 1× | 1 | · | part |
| 8 | Control System 6 parts | strapping-machine-automatic-control-system | 1× | 1 | 30 | assembly |
| 8.1 | PLC Module 4 parts | strapping-machine-automatic-plc-module | 1× | 1 | 11 | assembly |
| 8.1.1 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.1.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.1.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 8.1.4 | Connector | connector | 8× | 8 | · | part |
| 8.2 | HMI Panel 4 parts | strapping-machine-automatic-hmi-panel | 1× | 1 | 4 | assembly |
| 8.2.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.2.2 | Touch Digitizer | touch-digitizer | 1× | 1 | · | part |
| 8.2.3 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.2.4 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.3 | Power Supply 2 parts | strapping-machine-automatic-power-supply | 1× | 1 | 5 | assembly |
| 8.3.1 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.3.2 | Connector | connector | 4× | 4 | · | part |
| 8.4 | Safety Relay | strapping-machine-automatic-safety-relay | 1× | 1 | · | part |
| 8.5 | Relay | relay | 8× | 8 | · | part |
| 8.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9 | Safety Guarding 4 parts | strapping-machine-automatic-guarding | 1× | 1 | 8 | assembly |
| 9.1 | Head Cover | strapping-machine-automatic-head-cover | 1× | 1 | · | part |
| 9.2 | Guard Panel | strapping-machine-automatic-guard-panel | 3× | 3 | · | part |
| 9.3 | Interlock Switch | strapping-machine-automatic-interlock-switch | 3× | 3 | · | part |
| 9.4 | Fastener Set | fastener-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Paper Banding Machine
173 parts · shares 11 with this page
Wraparound Case Packer
278 parts · shares 11 with this page
Tray Shrink Packer
386 parts · shares 10 with this page
 Industrial Screen Printing Press
162 parts · shares 10 with this page
Gravity Filling Machine
177 parts · shares 9 with this page
Counter-Pressure Filler
519 parts · shares 9 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$3M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| heidelberg.com ↗ | Heidelberg, DE | Printing presses | 10 units | 12–22 wks |
|
🇨🇭Bobst
bobst.com ↗
|
Lausanne, CH | Packaging machinery | 10 units | 12–22 wks |
| koenig-bauer.com ↗ | Würzburg, DE | Printing presses | 10 units | 12–22 wks |
| wuh-group.com ↗ | Lengerich, DE | Flexible packaging machines | 10 units | 12–22 wks |
| markandy.com ↗ | Chesterfield, US | Label presses | 10 units | 12–22 wks |
1,015-word article