Slitter Rewinder
ProductOverview
A slitter rewinder takes a wide parent roll of film, paper, foil, or laminate and cuts it lengthwise into several narrower rolls, winding each one up separately. It sits at the end of a printing, coating, or lamination line, where material is made in wide master rolls for efficiency but must ship in the narrow widths a packaging or converting machine actually uses. The machine unwinds the parent roll, runs the web through a bank of knives that slit it into strips, and winds each strip onto its own core at controlled tension so the finished rolls are tight, even, and free of defects. Slitting quality decides how well the narrow rolls run downstream, so edge cleanliness, roll hardness, and tension control are the things the machine is built around.
The web travels from the Unwind Stand through the Slitting Section section, along the Web Path, and onto the Dual-Shaft Rewind. The Drive System holds line speed and winding tension, and the Control System sets the slit recipe and stops the line on a web break.
Unwinding the parent roll
The heavy parent roll is loaded onto the Unwind Stand by a Roll Lift set of arms, then gripped on a Unwind Air Shaft that expands into the core. A Unwind Brake or motor controls how fast the web pays off, holding the tension read by Tension Load Cell sensors. A Edge Guide keeps the web centered as it leaves the roll so the slit positions stay correct across the width. Consistent unwind tension is the foundation for everything downstream, because a slack or surging web slits poorly and winds loose.
Slitting the web
The Slitting Section section cuts the full-width web into strips. The most common method on film and laminate is shear slitting, where the Shear Knife Set set pairs a rotating Top Knife against a Bottom Knife on a Knife Shaft, cutting like a row of rotary scissors for a clean dust-free edge. Thin films can instead be razor slit, where a blade in a Razor Holder slices the web against air or over the Anvil Roll. A Knife Positioner sets each knife to the programmed width. Slitting throws off narrow edge trim, which a Trim Removal system pulls away: a Trim Blower suctions the trim through a Trim Duct to a bin so it does not foul the rolls.
Winding the finished rolls
The slit strips wind onto the Dual-Shaft Rewind. Two Rewind Shaft shafts let the machine wind alternate strips on opposite shafts so adjacent narrow rolls do not interfere, and each strip sits on a Differential Core Chuck differential chuck that lets it find its own torque even when strips run at slightly different effective diameters. A Rider Roll presses on the building rolls to control how much air winds in, which sets roll hardness. Each shaft is driven by a Rewind Drive torque motor that tapers tension as the roll grows, so the core is not crushed and the outside is not loose. When the rolls are full, a Roll Pusher strips them off the shaft for unloading.
Web path and tension
Between the stations the Web Path routes and conditions the web. Idler Roll rolls support it, a Spreader Roll pair separates the freshly slit strips so their edges clear each other, and a Tension Dancer buffers tension swings. A driven Nip Roll sets the master line speed and isolates the rewind tension from the unwind, so the slitting zone sees steady tension regardless of what the winding rolls are doing. Stable tension through this section is what keeps the strips tracking straight into their knives and onto their cores.
Drive, control, and use
The Drive System uses several Servo Motor axes through Servo Drive amplifiers and Gearbox Housing reducers, one for the master line and others for the rewind shafts, so every roll winds to its own tension profile while staying in speed with the line. The Control System system, built on a Machine Controller and an HMI, stores slit recipes giving each knife position and winding tension, counts length with a Length Encoder so rolls finish at a set diameter or meterage, and stops on a web break. Slitter rewinders are used wherever wide web is converted to usable rolls: film and foil for flexible packaging, label stock, flexible printing substrates, and paper. Variants include duplex turret rewinders for non-stop roll change and shaftless designs for very large rolls. Knife choice depends on the material: shear knives suit laminate and foil where a clean square edge matters, razor slitting suits thin plain film, and crush slitting against the Anvil Roll suits soft nonwovens and tapes. Knives are consumable and dull with use, so a worn Top Knife that begins to tear rather than cut leaves a ragged edge that telescopes the wound roll, which is why operators check edge quality at every roll change and reset the Knife Positioner when changing slit pattern.
Slitter Rewinder parts and their functions
7 top-level parts · 528 parts in total · full bill of materials below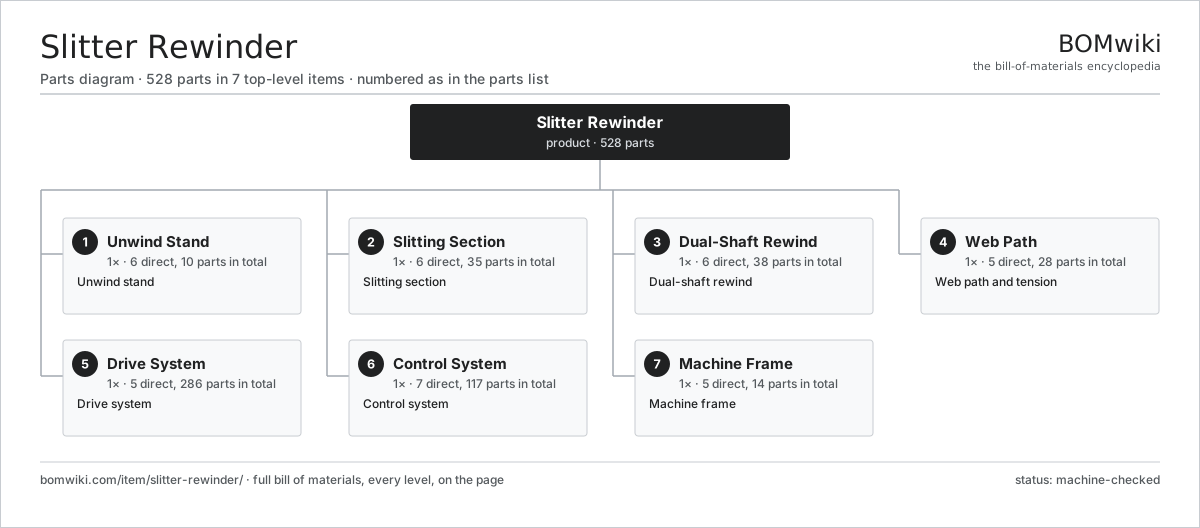
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Unwind Stand 6 parts | 1× | Unwind stand |
| 2 | Slitting Section 6 parts | 1× | Slitting section |
| 3 | Dual-Shaft Rewind 6 parts | 1× | Dual-shaft rewind |
| 4 | Web Path 5 parts | 1× | Web path and tension |
| 5 | Drive System 5 parts | 1× | Drive system |
| 6 | Control System 7 parts | 1× | Control system |
| 7 | Machine Frame 5 parts | 1× | Machine frame |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Slitter Rewinder
7 top-level lines · 64 rows shown · 528 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Unwind Stand 6 parts | slitter-rewinder-unwind | 1× | 1 | 10 | assembly |
| 1.1 | Unwind Air Shaft | slitter-rewinder-unwind-shaft | 1× | 1 | · | part |
| 1.2 | Unwind Brake | slitter-rewinder-unwind-brake | 1× | 1 | · | part |
| 1.3 | Tension Load Cell | slitter-rewinder-load-cell | 2× | 2 | · | part |
| 1.4 | Edge Guide | slitter-rewinder-edge-guide | 1× | 1 | · | part |
| 1.5 | Roll Lift | slitter-rewinder-lift | 1× | 1 | · | part |
| 1.6 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 2 | Slitting Section 6 parts | slitter-rewinder-slitting | 1× | 1 | 35 | assembly |
| 2.1 | Shear Knife Set 3 parts | slitter-rewinder-shear-knife | 1× | 1 | 26 | assembly |
| 2.1.1 | Top Knife | slitter-rewinder-top-knife | 12× | 12 | · | part |
| 2.1.2 | Bottom Knife | slitter-rewinder-bottom-knife | 12× | 12 | · | part |
| 2.1.3 | Knife Shaft | slitter-rewinder-knife-shaft | 2× | 2 | · | part |
| 2.2 | Razor Holder | slitter-rewinder-razor-holder | 1× | 1 | · | part |
| 2.3 | Anvil Roll | slitter-rewinder-anvil-roll | 1× | 1 | · | part |
| 2.4 | Knife Positioner | slitter-rewinder-knife-positioner | 1× | 1 | · | part |
| 2.5 | Trim Removal 2 parts | slitter-rewinder-trim-removal | 1× | 1 | 2 | assembly |
| 2.5.1 | Trim Blower | slitter-rewinder-trim-blower | 1× | 1 | · | part |
| 2.5.2 | Trim Duct | slitter-rewinder-trim-duct | 1× | 1 | · | part |
| 2.6 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 3 | Dual-Shaft Rewind 6 parts | slitter-rewinder-rewind | 1× | 1 | 38 | assembly |
| 3.1 | Rewind Shaft | slitter-rewinder-rewind-shaft | 2× | 2 | · | part |
| 3.2 | Differential Core Chuck | slitter-rewinder-diff-core | 24× | 24 | · | part |
| 3.3 | Rider Roll | slitter-rewinder-rider-roll | 1× | 1 | · | part |
| 3.4 | Rewind Drive | slitter-rewinder-rewind-drive | 2× | 2 | · | part |
| 3.5 | Roll Pusher | slitter-rewinder-pusher | 1× | 1 | · | part |
| 3.6 | Ball Bearing | ball-bearing | 8× | 8 | · | part |
| 4 | Web Path 5 parts | slitter-rewinder-web-path | 1× | 1 | 28 | assembly |
| 4.1 | Idler Roll | slitter-rewinder-idler-roll | 8× | 8 | · | part |
| 4.2 | Spreader Roll | slitter-rewinder-spreader-roll | 2× | 2 | · | part |
| 4.3 | Tension Dancer | slitter-rewinder-dancer | 1× | 1 | · | part |
| 4.4 | Nip Roll | slitter-rewinder-nip-roll | 1× | 1 | · | part |
| 4.5 | Ball Bearing | ball-bearing | 16× | 16 | · | part |
| 5 | Drive System 5 parts | slitter-rewinder-drive | 1× | 1 | 286 | assembly |
| 5.1 | Servo Motor 4 parts | servo-motor | 3× | 3 | 24 | assembly |
| 5.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 3 | 3 | assembly |
| 5.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 3 | 19 | assembly |
| 5.1.3 | Encoder | encoder | 1× | 3 | · | part |
| 5.1.4 | Motor Housing | motor-housing | 1× | 3 | · | part |
| 5.2 | Servo Drive 4 parts | slitter-rewinder-servo-drive | 3× | 3 | 68 | assembly |
| 5.2.1 | Bare PCB | pcb-bare | 1× | 3 | · | part |
| 5.2.2 | Power MOSFET | mosfet | 6× | 18 | · | part |
| 5.2.3 | Power Supply | power-supply | 1× | 3 | · | part |
| 5.2.4 | SMD Passive (R/C/L) | smd-passives | 60× | 180 | · | part |
| 5.3 | Gearbox Housing | gearbox-housing | 2× | 2 | · | part |
| 5.4 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 5.5 | Ball Bearing | ball-bearing | 6× | 6 | · | part |
| 6 | Control System 7 parts | slitter-rewinder-control | 1× | 1 | 117 | assembly |
| 6.1 | Machine Controller 4 parts | slitter-rewinder-plc | 1× | 1 | 88 | assembly |
| 6.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 6.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 6.1.3 | SMD Passive (R/C/L) | smd-passives | 80× | 80 | · | part |
| 6.1.4 | Connector | connector | 6× | 6 | · | part |
| 6.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 6.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 6.4 | Length Encoder | slitter-rewinder-encoder | 2× | 2 | · | part |
| 6.5 | Relay | relay | 8× | 8 | · | part |
| 6.6 | Connector | connector | 16× | 16 | · | part |
| 6.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 7 | Machine Frame 5 parts | slitter-rewinder-frame | 1× | 1 | 14 | assembly |
| 7.1 | Side Frame | slitter-rewinder-side-frame | 2× | 2 | · | part |
| 7.2 | Sheet Metal Panel | sheet-panel | 6× | 6 | · | part |
| 7.3 | Safety Guard | slitter-rewinder-safety-guard | 1× | 1 | · | part |
| 7.4 | Leveling Foot | slitter-rewinder-leveling-foot | 4× | 4 | · | part |
| 7.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Dye-Sublimation Printer
414 parts · shares 2 with this page
 Induction Cap Sealer
44 parts · shares 1 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$3M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| heidelberg.com ↗ | Heidelberg, DE | Printing presses | 10 units | 12–22 wks |
|
🇨🇭Bobst
bobst.com ↗
|
Lausanne, CH | Packaging machinery | 10 units | 12–22 wks |
| koenig-bauer.com ↗ | Würzburg, DE | Printing presses | 10 units | 12–22 wks |
| wuh-group.com ↗ | Lengerich, DE | Flexible packaging machines | 10 units | 12–22 wks |
| markandy.com ↗ | Chesterfield, US | Label presses | 10 units | 12–22 wks |
892-word article