Profile Wrapping Machine
ProductOverview
A profile wrapping machine covers a long molding with a thin decorative film, turning a plain extruded or machined profile into a finished part that looks like wood, stone, or a colored surface. The profiles are things like picture-frame moldings, door casings, skirting boards, window trim, and furniture edges, made from MDF, PVC, aluminium, or wood. The machine runs the bare profile through at a steady speed while it pays out a foil web, coats one side with adhesive, and then presses the foil down onto every face and radius of the profile with a series of shaped rollers so it follows the shape exactly with no air pockets or loose edges. The result is a wrapped length that goes on to be cut into finished pieces.
The machine drives the profile through the Infeed Drive, pays out film from the Foil Unwind Station, coats it in the Glue Unit unit, presses it on at the Pressure Roller Station, cleans the edges in the Trim and Finishing section, sets the bond in the Cooling Outfeed outfeed, and runs from the Machine Controller.
Feeding the profile
The Infeed Drive pulls the bare profile through at a constant, accurate speed, because every other station is timed to that motion. A set of rubber-faced Feed Roller units driven by a Servo Motor through a Gearbox Housing grips the profile, while Side Guide Roller rollers keep it centered so the foil wraps symmetrically on both sides. Straight, centered feed is the foundation of a good wrap: if the profile wanders, the foil overhang is uneven and the corners do not fold cleanly. The rollers run on Ball Bearing supports and are set to the profile width before a run.
Foil unwind and tension
The Foil Unwind Station station presents the decorative film. The foil reel mounts on an air-expanding Reel Shaft, and a Web Brake sets the back tension while a Dancer Arm arm buffers the web and holds tension steady as the reel diameter shrinks through the run. An Edge Sensor reads the foil edge and steers the web so it stays aligned to the profile within a fraction of a millimetre. When a reel runs low, the Splice Table lets the operator tape a fresh reel to the running web for a flying splice, so the line never has to stop and reheat. Tension control matters because a slack web wrinkles and an over-tight web can neck down or tear the foil at a corner.
Gluing
The bond comes from the Glue Unit unit. A Adhesive Melter melts hot-melt EVA or moisture-curing PUR granules to application viscosity, a Metering Pump meters it in proportion to line speed, and a heated Heated Hose carries it to a Slot Nozzle that lays an even film across the foil back, with Heating Element heaters holding every part of the path molten. Even, thin, correctly timed adhesive is what makes a wrap last: too little glue and the foil lifts at the edges in service, too much and it squeezes out and fouls the rollers. PUR adhesives give the strongest, most heat- and water-resistant bond and are used where the finished molding will see sun or moisture.
Pressing the foil on
The Pressure Roller Station is where the foil actually takes the shape of the profile. A bank of shaped Pressure Roller units, each carried on an adjustable Roller Arm, presses the glued foil onto one face or radius of the profile in sequence, so the flat top is laid first, then each side, then the curves, and finally the back edges. Stationary Folding Shoe guides progressively fold the foil around the sharp corners between rollers. Setting up this station for a new profile is the main skill in running the machine: each roller is positioned and loaded so the foil seats tight into every detail without stretching thin over a corner or trapping air on a flat.
Trimming, cooling, and use
After wrapping, the Trim and Finishing section cleans up the part. A Trim Knife slits off the overhang foil along the back groove, Corner Roller rollers seat the foil into sharp corners, and a Burnishing Brush rubs the surface down to a clean, tight finish. The wrapped profile then runs through the Cooling Outfeed outfeed, where chilled Cooling Roller rollers set the adhesive so the part can be handled, and a Outfeed Belt carries it to the cutoff. The Machine Controller cabinet ties the stations together: an Microcontroller synchronizes feed speed, web tension, and glue dosing, and the operator works from the Operator Screen to load a recipe for each profile and film. These machines run in molding and furniture-component plants, producing the wrapped trim that ends up as door frames, baseboards, cabinet edges, and picture-frame stock, where a clean wrap with no lifted edges is the whole point of the product.
Profile Wrapping Machine parts and their functions
7 top-level parts · 173 parts in total · full bill of materials below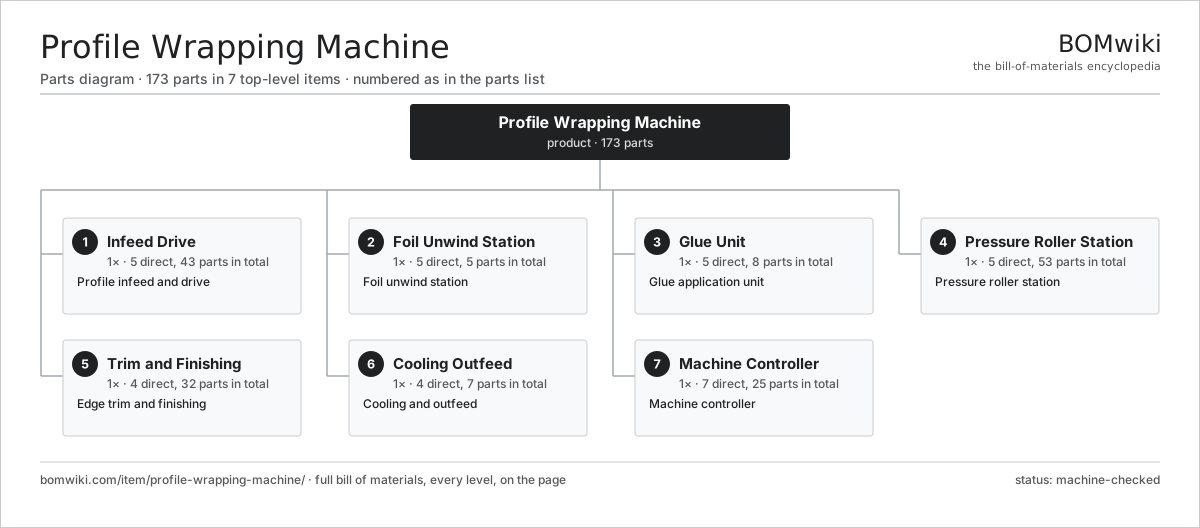
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Infeed Drive 5 parts | 1× | Profile infeed and drive |
| 2 | Foil Unwind Station 5 parts | 1× | Foil unwind station |
| 3 | Glue Unit 5 parts | 1× | Glue application unit |
| 4 | Pressure Roller Station 5 parts | 1× | Pressure roller station |
| 5 | Trim and Finishing 4 parts | 1× | Edge trim and finishing |
| 6 | Cooling Outfeed 4 parts | 1× | Cooling and outfeed |
| 7 | Machine Controller 7 parts | 1× | Machine controller |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Profile Wrapping Machine
7 top-level lines · 50 rows shown · 173 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Infeed Drive 5 parts | profile-wrapping-machine-infeed | 1× | 1 | 43 | assembly |
| 1.1 | Feed Roller | profile-wrapping-machine-feed-roller | 6× | 6 | · | part |
| 1.2 | Side Guide Roller | profile-wrapping-machine-side-guide | 4× | 4 | · | part |
| 1.3 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 1.3.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 1.3.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 1.3.3 | Encoder | encoder | 1× | 1 | · | part |
| 1.3.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 1.4 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 1.5 | Ball Bearing | ball-bearing | 8× | 8 | · | part |
| 2 | Foil Unwind Station 5 parts | profile-wrapping-machine-unwind | 1× | 1 | 5 | assembly |
| 2.1 | Reel Shaft | profile-wrapping-machine-reel-shaft | 1× | 1 | · | part |
| 2.2 | Dancer Arm | profile-wrapping-machine-dancer | 1× | 1 | · | part |
| 2.3 | Splice Table | profile-wrapping-machine-splice-table | 1× | 1 | · | part |
| 2.4 | Web Brake | profile-wrapping-machine-brake | 1× | 1 | · | part |
| 2.5 | Edge Sensor | profile-wrapping-machine-edge-sensor | 1× | 1 | · | part |
| 3 | Glue Unit 5 parts | profile-wrapping-machine-glue | 1× | 1 | 8 | assembly |
| 3.1 | Adhesive Melter | profile-wrapping-machine-melter | 1× | 1 | · | part |
| 3.2 | Slot Nozzle | profile-wrapping-machine-glue-nozzle | 1× | 1 | · | part |
| 3.3 | Metering Pump | profile-wrapping-machine-glue-pump | 1× | 1 | · | part |
| 3.4 | Heated Hose | profile-wrapping-machine-glue-hose | 1× | 1 | · | part |
| 3.5 | Heating Element | heating-element | 4× | 4 | · | part |
| 4 | Pressure Roller Station 5 parts | profile-wrapping-machine-roller-station | 1× | 1 | 53 | assembly |
| 4.1 | Pressure Roller | profile-wrapping-machine-press-roller | 12× | 12 | · | part |
| 4.2 | Roller Arm | profile-wrapping-machine-roller-arm | 12× | 12 | · | part |
| 4.3 | Folding Shoe | profile-wrapping-machine-folding-shoe | 4× | 4 | · | part |
| 4.4 | Ball Bearing | ball-bearing | 24× | 24 | · | part |
| 4.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 5 | Trim and Finishing 4 parts | profile-wrapping-machine-trim | 1× | 1 | 32 | assembly |
| 5.1 | Trim Knife | profile-wrapping-machine-trim-knife | 2× | 2 | · | part |
| 5.2 | Burnishing Brush | profile-wrapping-machine-burnish-brush | 2× | 2 | · | part |
| 5.3 | Corner Roller | profile-wrapping-machine-corner-roller | 4× | 4 | · | part |
| 5.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 5.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 5.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 5.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 5.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 6 | Cooling Outfeed 4 parts | profile-wrapping-machine-cooling | 1× | 1 | 7 | assembly |
| 6.1 | Cooling Roller | profile-wrapping-machine-cooling-roller | 4× | 4 | · | part |
| 6.2 | Outfeed Belt | profile-wrapping-machine-outfeed-belt | 1× | 1 | · | part |
| 6.3 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 6.4 | Coolant Pump | coolant-pump | 1× | 1 | · | part |
| 7 | Machine Controller 7 parts | profile-wrapping-machine-control | 1× | 1 | 25 | assembly |
| 7.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.3 | Operator Screen | profile-wrapping-machine-hmi | 1× | 1 | · | part |
| 7.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.5 | Relay | relay | 6× | 6 | · | part |
| 7.6 | Connector | connector | 14× | 14 | · | part |
| 7.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Induction Cap Sealer
44 parts · shares 1 with this page
 Automatic Strapping Machine
251 parts · shares 5 with this page
Carton Overwrapping Machine
261 parts · shares 5 with this page
Case Labeling Machine
120 parts · shares 5 with this page
Film Bundling Machine
437 parts · shares 5 with this page
 Film Laminating Machine
229 parts · shares 5 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$3M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| heidelberg.com ↗ | Heidelberg, DE | Printing presses | 10 units | 12–22 wks |
|
🇨🇭Bobst
bobst.com ↗
|
Lausanne, CH | Packaging machinery | 10 units | 12–22 wks |
| koenig-bauer.com ↗ | Würzburg, DE | Printing presses | 10 units | 12–22 wks |
| wuh-group.com ↗ | Lengerich, DE | Flexible packaging machines | 10 units | 12–22 wks |
| markandy.com ↗ | Chesterfield, US | Label presses | 10 units | 12–22 wks |
897-word article