En-Masse Conveyor
ProductOverview
An en-masse conveyor moves bulk material as a solid flowing column rather than dragging it across a floor. A central chain fitted with open skeleton flights runs through an enclosed casing, and the flights set the entire body of material in motion together, so it travels en masse at the chain speed. The internal friction of the grain or powder against itself carries far more material than the flights touch directly, which lets a slim casing convey a high tonnage gently and with very little dust. It is a staple of grain handling, feed milling, malting, and biomass plants where product must be moved cleanly without breakage.
The conveyor is built around an Enclosed Casing that contains the column, an Chain & Skeleton Flights assembly that moves it, a Head Drive at the discharge end, and an Tail & Take-Up that tensions the chain. Long runs are supported by Intermediate Idlers idlers, material enters and leaves through the Feed & Discharge spouts, the casing is protected by Wear Liners, the Safety & Monitoring sensors watch for jams and breakage, and the Control Panel panel runs the drive.
How it works
The principle is the en-masse effect. When a casing is kept full and a chain with open Skeleton Flight flights moves through it, the flights grip the column and the material flows with them as a continuous mass. Because grain and powders have internal cohesion and friction, layers above and beside the flights are carried along too, so the conveyor moves far more material than the flights physically sweep. The open skeleton shape lets material flow through and around each flight, which avoids the scraping and grinding of a closed scraper and keeps the product intact. This is why en-masse units are preferred over drag chain conveyors for friable products such as malt, pellets, and processed feed.
The casing is normally kept choked, meaning full, so the column conveys as one body. The Feed Inlet fills the casing and the Discharge Outlet releases the material at the far end or at an intermediate gate.
Chain and skeleton flights
The Chain & Skeleton Flights assembly runs down the centre of the casing. The Central Chain is a case-hardened forged-link chain that carries the flights and takes the conveying pull. Each Skeleton Flight is an open U- or H-shaped skeleton bolted to an Attachment Link link, sized so material can flow through it while still gripping the column. A Connecting Link closes the loop and lets a crew break the chain to remove flights or take out stretch.
Drive, tail, and supports
The Head Drive sits at the discharge end so the loaded run is pulled in tension. A Drive Motor feeds a helical reducer turning the Head Shaft and its Head Sprocket. The Tail & Take-Up carries an idler sprocket on a Screw Take-Up screw that keeps the chain correctly tensioned. On long horizontal runs the Intermediate Idlers idlers, with Idler Roller rollers on Ball Bearing units and a Guide Rail to keep the chain centred, support both the loaded and return chain so it does not sag and foul the casing.
Casing, liners, and enclosure
The Enclosed Casing is a bolted dust-tight enclosure, which is the main reason en-masse conveyors are chosen for food and feed handling where dust control and hygiene matter. Each Casing Section bolts end to end with a gasketed Casing Cover, and an Inspection Door gives access for cleanout between product batches. Inside, Wear Liners protect the wear surfaces with a bolt-in Floor Liner and Side Liner that can be replaced without scrapping the casing.
Safety and monitoring
The Safety & Monitoring group protects the hidden chain. A Speed Sensor on the tail shaft trips the drive if the chain slips or breaks, a Plug Switch catches a blockage before the drive overloads, and Bearing Temperature Sensor RTDs warn of bearing overheating. A Pull-Cord Stop gives operators an emergency stop from any point. The Control Panel panel ties these together through its Controller Board, which carries an Microcontroller that sequences the start, monitors the sensors through Relay outputs, and trips the drive on any fault.
Variants and use
En-masse conveyors run horizontally, on an incline, and around L- and Z-shaped paths formed by joining straight casing runs at sprocketed corners. They handle grain into and out of silos, meal and pellets in feed mills, malt in breweries and distilleries, wood pellets and chips in biomass plants, and fine powders in process industries. The dust-tight gentle handling is the reason they are chosen over belt conveyors for friable or dusty products, and over screw conveyors when the run is long or the product must not be sheared. The Feed & Discharge arrangement can include several gated outlets so one conveyor distributes material to multiple bins along its length.
En-Masse Conveyor parts and their functions
9 top-level parts · 307 parts in total · full bill of materials below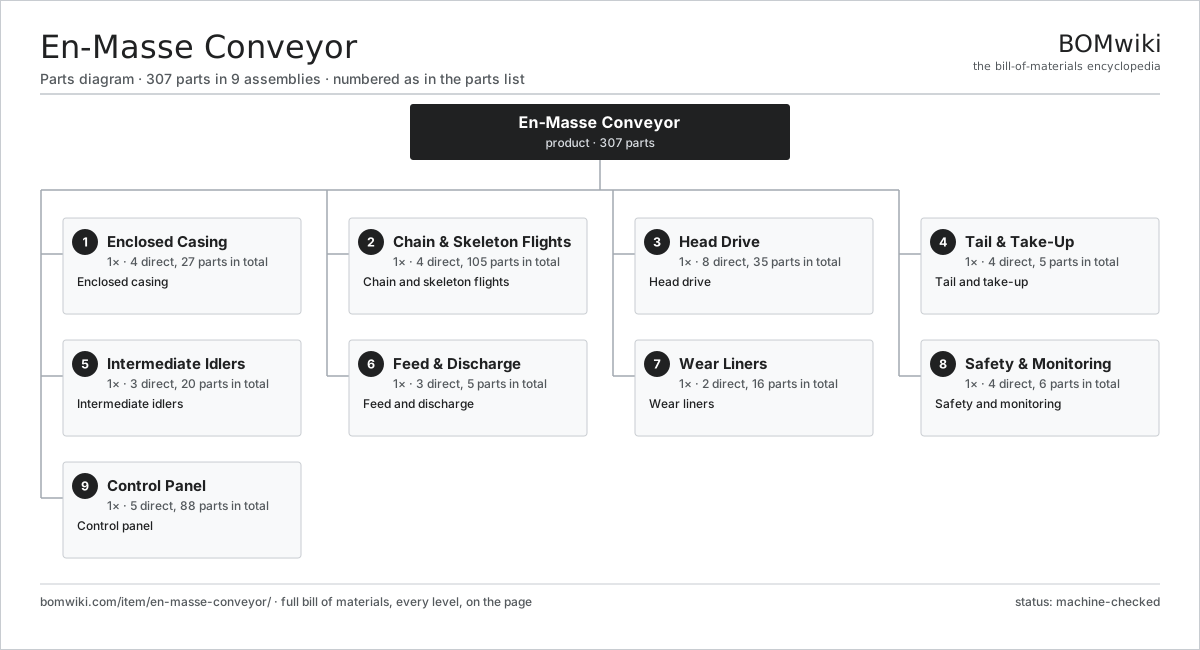
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Enclosed Casing 4 parts | 1× | Enclosed casing |
| 2 | Chain & Skeleton Flights 4 parts | 1× | Chain and skeleton flights |
| 3 | Head Drive 8 parts | 1× | Head drive |
| 4 | Tail & Take-Up 4 parts | 1× | Tail and take-up |
| 5 | Intermediate Idlers 3 parts | 1× | Intermediate idlers |
| 6 | Feed & Discharge 3 parts | 1× | Feed and discharge |
| 7 | Wear Liners 2 parts | 1× | Wear liners |
| 8 | Safety & Monitoring 4 parts | 1× | Safety and monitoring |
| 9 | Control Panel 5 parts | 1× | Control panel |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for En-Masse Conveyor
9 top-level lines · 54 rows shown · 307 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Enclosed Casing 4 parts | en-masse-conveyor-casing | 1× | 1 | 27 | assembly |
| 1.1 | Casing Section | en-masse-conveyor-casing-section | 8× | 8 | · | part |
| 1.2 | Casing Cover | en-masse-conveyor-cover | 8× | 8 | · | part |
| 1.3 | Inspection Door | en-masse-conveyor-inspection-door | 3× | 3 | · | part |
| 1.4 | Fastener Set | fastener-set | 8× | 8 | · | part |
| 2 | Chain & Skeleton Flights 4 parts | en-masse-conveyor-chain-flights | 1× | 1 | 105 | assembly |
| 2.1 | Central Chain | en-masse-conveyor-chain | 1× | 1 | · | part |
| 2.2 | Skeleton Flight | en-masse-conveyor-flight | 50× | 50 | · | part |
| 2.3 | Attachment Link | en-masse-conveyor-attachment | 50× | 50 | · | part |
| 2.4 | Connecting Link | en-masse-conveyor-connector-link | 4× | 4 | · | part |
| 3 | Head Drive 8 parts | en-masse-conveyor-drive | 1× | 1 | 35 | assembly |
| 3.1 | Drive Motor 4 parts | en-masse-conveyor-drive-motor | 1× | 1 | 25 | assembly |
| 3.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 3.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 3.1.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3.1.4 | Motor Frame | en-masse-conveyor-motor-frame | 1× | 1 | · | part |
| 3.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 3.3 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 3.4 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 3.5 | Head Sprocket | en-masse-conveyor-head-sprocket | 1× | 1 | · | part |
| 3.6 | Head Shaft | en-masse-conveyor-head-shaft | 1× | 1 | · | part |
| 3.7 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3.8 | Drive Coupling | en-masse-conveyor-coupling | 1× | 1 | · | part |
| 4 | Tail & Take-Up 4 parts | en-masse-conveyor-tail | 1× | 1 | 5 | assembly |
| 4.1 | Tail Sprocket | en-masse-conveyor-tail-sprocket | 1× | 1 | · | part |
| 4.2 | Tail Shaft | en-masse-conveyor-tail-shaft | 1× | 1 | · | part |
| 4.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 4.4 | Screw Take-Up | en-masse-conveyor-takeup | 1× | 1 | · | part |
| 5 | Intermediate Idlers 3 parts | en-masse-conveyor-intermediate | 1× | 1 | 20 | assembly |
| 5.1 | Idler Roller | en-masse-conveyor-idler-roller | 6× | 6 | · | part |
| 5.2 | Ball Bearing | ball-bearing | 12× | 12 | · | part |
| 5.3 | Guide Rail | en-masse-conveyor-guide-rail | 2× | 2 | · | part |
| 6 | Feed & Discharge 3 parts | en-masse-conveyor-feed-discharge | 1× | 1 | 5 | assembly |
| 6.1 | Feed Inlet | en-masse-conveyor-inlet | 1× | 1 | · | part |
| 6.2 | Discharge Outlet | en-masse-conveyor-outlet | 2× | 2 | · | part |
| 6.3 | Slide Gate | en-masse-conveyor-slide-gate | 2× | 2 | · | part |
| 7 | Wear Liners 2 parts | en-masse-conveyor-liners | 1× | 1 | 16 | assembly |
| 7.1 | Floor Liner | en-masse-conveyor-floor-liner | 8× | 8 | · | part |
| 7.2 | Side Liner | en-masse-conveyor-side-liner | 8× | 8 | · | part |
| 8 | Safety & Monitoring 4 parts | en-masse-conveyor-safety | 1× | 1 | 6 | assembly |
| 8.1 | Speed Sensor | en-masse-conveyor-speed-sensor | 1× | 1 | · | part |
| 8.2 | Plug Switch | en-masse-conveyor-plug-sensor | 1× | 1 | · | part |
| 8.3 | Bearing Temperature Sensor | en-masse-conveyor-temp-sensor | 2× | 2 | · | part |
| 8.4 | Pull-Cord Stop | en-masse-conveyor-pullcord | 2× | 2 | · | part |
| 9 | Control Panel 5 parts | en-masse-conveyor-control | 1× | 1 | 88 | assembly |
| 9.1 | Controller Board 4 parts | en-masse-conveyor-control-board | 1× | 1 | 76 | assembly |
| 9.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.1.3 | SMD Passive (R/C/L) | smd-passives | 70× | 70 | · | part |
| 9.1.4 | Connector | connector | 4× | 4 | · | part |
| 9.2 | Power Supply | power-supply | 1× | 1 | · | part |
| 9.3 | Relay | relay | 4× | 4 | · | part |
| 9.4 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9.5 | Connector | connector | 6× | 6 | · | part |
Related products
same domain, ranked by shared parts Articulated Forklift
2,417 parts · shares 2 with this page
 Bag Palletizer
951 parts · shares 2 with this page
Coal Yard Stacker
571 parts · shares 2 with this page
 Cross-Belt Sorter
25,040 parts · shares 2 with this page
Dense-Phase Conveying System
446 parts · shares 2 with this page
 Dilute-Phase Conveying System
509 parts · shares 2 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $2k–$300k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| toyota-industries.com ↗ | Kariya, JP | Forklifts & logistics | 20 units | 10–16 wks |
| kiongroup.com ↗ | Frankfurt, DE | Forklifts (Linde, STILL) | 20 units | 10–16 wks |
| jungheinrich.com ↗ | Hamburg, DE | Warehouse trucks | 20 units | 10–16 wks |
| crown.com ↗ | New Bremen, US | Forklifts | 20 units | 10–16 wks |
|
🇨🇳Hangcha
hcforklift.com ↗
|
Hangzhou, CN | Forklifts & material handling | 20 units | 10–16 wks |
903-word article