Open-Mouth Sack Filler
ProductOverview
An Open-Mouth Sack Filler is a machine that fills open-mouth bags with a weighed charge of bulk product, then settles and closes them. Open-mouth bags are the open-top sacks used for cement, flour, sugar, animal feed, seed, fertilizer, plastic pellets, and chemicals, distinct from valve bags, which fill through a small self-sealing spout. The filler doses each bag to a target weight, supports it during filling, settles the product so the charge fits, and sews or heat-seals the top closed. The result is a uniform, accurately weighed, sealed bag ready for palletizing.
The economics turn on weight accuracy. Overfilling gives product away on every bag; underfilling risks short-weight complaints and legal trouble. A net-weigh filler typically holds plus or minus 0.1 to 0.25 percent of target, which over millions of bags a year is the difference between profit and loss on the giveaway alone.
Frame and surge hopper
The Machine Frame is a welded steel structure carrying the weigher and feed system above the bag station. Frame Upright support the load, a Service Platform gives access to the upper machinery, and a Product Surge Hopper holds a buffer of product feeding the metering device so the supply line upstream does not have to deliver in perfect sync with each fill.
Feed and metering
The Feed System meters product into the weigher. A Feed Auger driven by a servo or VFD Auger Motor runs fast for the bulk phase, delivering most of the charge quickly, then slows to a dribble as the weight approaches target so the final grams land precisely. A fast-acting Feed Gate cuts flow sharply at cutoff. A slow Hopper Agitator in the surge hopper keeps cohesive product from bridging over the auger inlet. The two-speed bulk-then-dribble approach is what makes high speed and high accuracy possible at the same time: most of the fill is fast, and only the last fraction is slow and precise.
Net weighing
The Weigh System is the accuracy element. Product is metered not directly into the bag but into a suspended Weigh Hopper carried by three Load Cell sensors. This is net weighing: a full charge is weighed in the hopper, independent of the bag, then released. Once the load cells read the target, the feed stops and a Dump Gate opens to drop the charge through a telescoping Fill Spout into the bag. The spout extends into the bag mouth and retracts as the bag fills, cutting the free-fall height and the dust it would otherwise raise.
Net weighing decouples accuracy from the bag. The scale never has to tare out a variable empty-bag weight or fight the disturbance of clamping, so each charge is weighed under identical, stable conditions.
Holding and supporting the bag
The Bag Clamp Station presents and holds the bag during fill. A Bag Spreader opens the flat bag mouth, and an Inflatable Clamp grips it against the spout with an air bladder, sealing the joint so product does not spill or dust escape. A powered Bag Rest supports the bag bottom and lowers as the bag fills and its weight grows, keeping the bag upright and the mouth square. Clamp Cylinder actuators release the filled bag onto the takeaway conveyor.
Settling and deaeration
Many powders trap air when they fall into a bag, fluffing up so the full charge will not fit or the bag is soft and unstackable. The Densifier settles them. A Vibration Table driven by an eccentric Vibrator Motor shakes the bag during and after fill, packing the product down, raising bulk density, and squaring the bag for clean palletizing. For fine fluidized powders such as cement or flour, a Deaeration Probe draws entrained air out so the powder compacts instead of overflowing. A well-densified bag holds its shape on the pallet and resists slumping in storage.
Closing the bag
The Bag Sealer closes the filled bag as it moves on the Takeaway Conveyor. For paper and woven polypropylene bags, a Sewing Head folds the top and runs a chain stitch across it: a Needle Bar drives the needle, a Looper forms the stitch, and a Thread Cutter trims the tail after each bag. For polyethylene or plastic-lined bags, a Heat Seal Bar fuses the mouth shut instead, giving a moisture-tight seal. The choice of closure follows the bag material and whether the product needs a sealed barrier.
Control and operation
The Control System coordinate the cycle. A Weigh Controller reads the load cells and switches the feed from bulk to dribble at the right crossover point, learning the in-flight material to refine cutoff over successive bags. A HMI Touchscreen holds target weights and product recipes and shows throughput. An Air Manifold drives the clamp, dump gate, and densifier pneumatics, and a Control Panel houses the drives and safety circuit.
Materials and variants
Machines are painted carbon steel for cement, minerals, and fertilizer, and 304 stainless for food and feed where washdown and hygiene apply. Variants include gross-weigh fillers that weigh directly in the bag for coarse free-flowing products, multi-spout carousels that run several bags in parallel for very high throughput, fully automatic lines with robotic bag placing instead of a manual operator, and integrated lines that feed directly into a palletizer and stretch wrapper. Filler choice follows the product: free-flowing pellets suit a simple gravity gate, while fine cohesive powders need an auger feed, aggressive densification, and deaeration.
Open-Mouth Sack Filler parts and their functions
7 top-level parts · 214 parts in total · full bill of materials below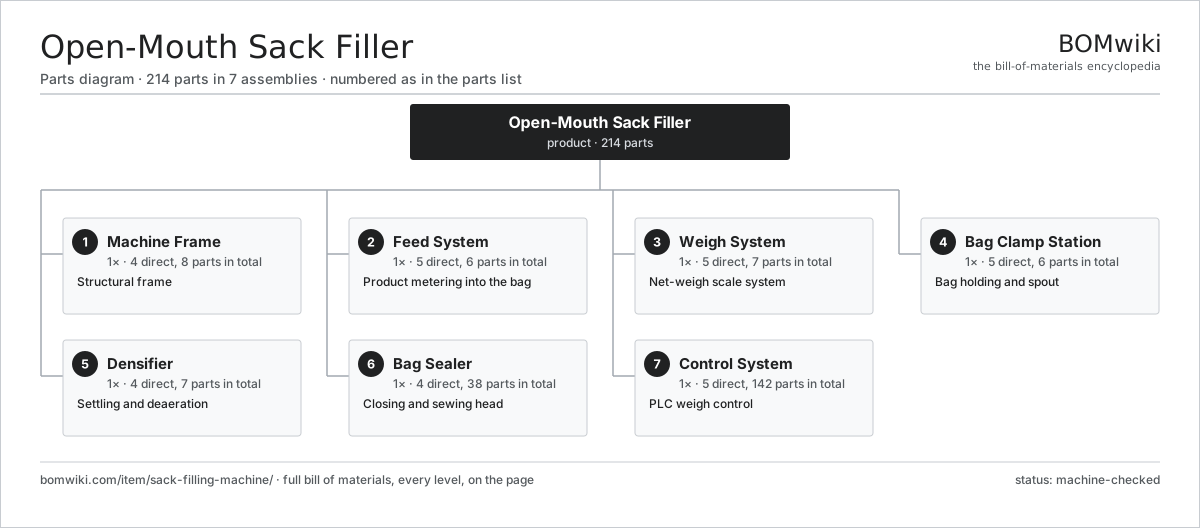
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Machine Frame 4 parts | 1× | Structural frame |
| 2 | Feed System 5 parts | 1× | Product metering into the bag |
| 3 | Weigh System 5 parts | 1× | Net-weigh scale system |
| 4 | Bag Clamp Station 5 parts | 1× | Bag holding and spout |
| 5 | Densifier 4 parts | 1× | Settling and deaeration |
| 6 | Bag Sealer 4 parts | 1× | Closing and sewing head |
| 7 | Control System 5 parts | 1× | PLC weigh control |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Open-Mouth Sack Filler
7 top-level lines · 58 rows shown · 214 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Machine Frame 4 parts | sack-filling-machine-frame | 1× | 1 | 8 | assembly |
| 1.1 | Frame Upright | sack-filling-machine-frame-uprights | 4× | 4 | · | part |
| 1.2 | Service Platform | sack-filling-machine-platform | 1× | 1 | · | part |
| 1.3 | Product Surge Hopper | sack-filling-machine-product-hopper | 1× | 1 | · | part |
| 1.4 | Fastener Set | fastener-set | 2× | 2 | · | part |
| 2 | Feed System 5 parts | sack-filling-machine-feed-system | 1× | 1 | 6 | assembly |
| 2.1 | Feed Auger | sack-filling-machine-feed-auger | 1× | 1 | · | part |
| 2.2 | Auger Motor | sack-filling-machine-auger-motor | 1× | 1 | · | part |
| 2.3 | Feed Gate | sack-filling-machine-feed-gate | 1× | 1 | · | part |
| 2.4 | Hopper Agitator | sack-filling-machine-agitator | 1× | 1 | · | part |
| 2.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3 | Weigh System 5 parts | sack-filling-machine-weigher | 1× | 1 | 7 | assembly |
| 3.1 | Weigh Hopper | sack-filling-machine-weigh-hopper | 1× | 1 | · | part |
| 3.2 | Load Cell | sack-filling-machine-load-cell | 3× | 3 | · | part |
| 3.3 | Dump Gate | sack-filling-machine-dump-gate | 1× | 1 | · | part |
| 3.4 | Fill Spout | sack-filling-machine-weigh-spout | 1× | 1 | · | part |
| 3.5 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 4 | Bag Clamp Station 5 parts | sack-filling-machine-bag-clamp | 1× | 1 | 6 | assembly |
| 4.1 | Inflatable Clamp | sack-filling-machine-inflatable-clamp | 1× | 1 | · | part |
| 4.2 | Bag Spreader | sack-filling-machine-bag-spreader | 1× | 1 | · | part |
| 4.3 | Bag Rest | sack-filling-machine-bag-rest | 1× | 1 | · | part |
| 4.4 | Clamp Cylinder | sack-filling-machine-clamp-cylinder | 2× | 2 | · | part |
| 4.5 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 5 | Densifier 4 parts | sack-filling-machine-densifier | 1× | 1 | 7 | assembly |
| 5.1 | Vibration Table | sack-filling-machine-vibration-table | 1× | 1 | · | part |
| 5.2 | Vibrator Motor | sack-filling-machine-vibrator-motor | 1× | 1 | · | part |
| 5.3 | Deaeration Probe | sack-filling-machine-deaeration-probe | 1× | 1 | · | part |
| 5.4 | Coil Spring | coil-spring | 4× | 4 | · | part |
| 6 | Bag Sealer 4 parts | sack-filling-machine-sealer | 1× | 1 | 38 | assembly |
| 6.1 | Sewing Head 3 parts | sack-filling-machine-sewing-head | 1× | 1 | 3 | assembly |
| 6.1.1 | Needle Bar | sack-filling-machine-needle-bar | 1× | 1 | · | part |
| 6.1.2 | Looper | sack-filling-machine-looper | 1× | 1 | · | part |
| 6.1.3 | Thread Cutter | sack-filling-machine-thread-cutter | 1× | 1 | · | part |
| 6.2 | Heat Seal Bar | sack-filling-machine-heat-bar | 1× | 1 | · | part |
| 6.3 | Takeaway Conveyor 4 parts | sack-filling-machine-takeaway-conveyor | 1× | 1 | 10 | assembly |
| 6.3.1 | Conveyor Belt | sack-filling-machine-conveyor-belt | 1× | 1 | · | part |
| 6.3.2 | Conveyor Roller | sack-filling-machine-conveyor-roller | 4× | 4 | · | part |
| 6.3.3 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 6.3.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 6.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 6.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 6.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 6.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 6.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 7 | Control System 5 parts | sack-filling-machine-controls | 1× | 1 | 142 | assembly |
| 7.1 | Control Panel | sack-filling-machine-control-panel | 1× | 1 | · | part |
| 7.2 | Weigh Controller 4 parts | sack-filling-machine-weigh-controller | 1× | 1 | 96 | assembly |
| 7.2.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.2.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.2.3 | SMD Passive (R/C/L) | smd-passives | 90× | 90 | · | part |
| 7.2.4 | Relay | relay | 4× | 4 | · | part |
| 7.3 | HMI Touchscreen 4 parts | sack-filling-machine-hmi | 1× | 1 | 43 | assembly |
| 7.3.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.3.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.3.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.3.4 | SMD Passive (R/C/L) | smd-passives | 40× | 40 | · | part |
| 7.4 | Air Manifold | sack-filling-machine-air-manifold | 1× | 1 | · | part |
| 7.5 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Bag Palletizer
951 parts · shares 7 with this page
 Tilt-Tray Sorter
6,031 parts · shares 7 with this page
Pallet Shuttle System
208 parts · shares 7 with this page
 Container Handler
552 parts · shares 8 with this page
 Reach Truck
832 parts · shares 8 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $2k–$300k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| toyota-industries.com ↗ | Kariya, JP | Forklifts & logistics | 20 units | 10–16 wks |
| kiongroup.com ↗ | Frankfurt, DE | Forklifts (Linde, STILL) | 20 units | 10–16 wks |
| jungheinrich.com ↗ | Hamburg, DE | Warehouse trucks | 20 units | 10–16 wks |
| crown.com ↗ | New Bremen, US | Forklifts | 20 units | 10–16 wks |
|
🇨🇳Hangcha
hcforklift.com ↗
|
Hangzhou, CN | Forklifts & material handling | 20 units | 10–16 wks |
1,015-word article