Overhead Trolley Conveyor
ProductOverview
An overhead trolley conveyor is the simplest form of overhead conveyor: a single endless chain runs around a fixed loop of track hung from the roof, and every carrier attached to that chain moves together at one steady speed. There is no accumulation and no routing, so it is the right choice when a process is continuous and every part takes the same path, such as a paint line, a plating line, or an oven where parts hang from the chain and move through the work at a fixed rate. By lifting the load off the floor it frees the floor for people and other equipment, and by hanging parts it presents every side of them to spray, dip, or weld.
The conveyor is built from a Overhead Track loop, a single Conveyor Chain that runs it, the Trolleys and Carriers that ride the track and carry the load, a Drive Unit that pulls the chain, a Take-Up Unit that keeps it taut, the Turns and Vertical Curves that route it around the plant, and a Control and Safety for safe operation.
The track loop
The Overhead Track is a continuous rail that the trolley wheels run on, usually an I-beam or a formed-steel section. It is made up of straight Track Section lengths joined by bolted Track Joint splices, and the whole loop hangs from the building on Hanger Rod rods through Support Bracket brackets. The track layout is the route the parts will travel, so it is designed to weave the loop through the spray booths, ovens, and load and unload stations, climbing and dropping as needed. Because all carriers share the loop, the track length and the chain speed together set how long a part spends in each zone.
Chain and trolleys
A single Conveyor Chain carries the whole load. It is built from forged Chain Link links joined by hardened Chain Pin pins, with Pendant Attachment links at regular spacing that hang the carriers. Each carrier rides on a Trolley, a pair of Trolley Wheel wheels on Ball Bearing bearings held in a Trolley Yoke yoke and turning on an Trolley Axle. Below the trolley a Pendant drops to a Load Carrier that holds the part, and a Swivel Joint joint lets the carrier rotate so parts keep their orientation through corners. Carriers are matched to the job, from simple hooks for painting to baskets for plating to shaped fixtures for assembly.
Drive and take-up
The Drive Unit pulls the chain at one constant speed. A Drive Gearmotor feeds a Drive Shaft carrying a Drive Sprocket that meshes the chain, and a Shear Pin breaks on overload to protect the gearbox if a carrier snags. Because the chain stretches as the pins wear and the line heats up, a Take-Up Unit unit keeps it taut. A spring-loaded Take-Up Carriage slides a Take-Up Sprocket to add or remove chain length, which stops the chain jumping the drive sprocket and keeps wheel spacing even. On long ovens an air take-up is used instead of springs so tension stays steady as the chain expands with heat.
Turns and elevation changes
Routing the loop through a plant needs corners and rises, which the Turns and Vertical Curves section provides. A horizontal corner is taken on a large Turn Wheel or a Roller Turn bank of small rollers that guides the chain around with low friction. To move between floor levels or to lift parts over equipment the loop uses Vertical Curve Section sections, which are curved track that the trolleys follow up and down. The radius of every turn is set by the chain and the load so the chain articulates freely and the carriers do not swing into each other.
Control and safety
The Control and Safety is simpler than on a power-and-free system because there is nothing to route. A Variable-Frequency Drive sets the chain speed and ramps it smoothly, and a Control Board runs the line logic and watches the safety devices. Jam Switch switches along the track stop the drive if a carrier snags or the chain breaks, and a Pull-Cord E-Stop pull-cord lets anyone stop the loop from any point. The electronics share a Power Supply and report to an LCD Panel screen.
Use and variants
Overhead trolley conveyors are chosen where a steady, single-speed pass is what the process needs. In a paint or powder-coat line the loop carries parts through cleaning, spraying, and a curing oven at a rate that matches the cure time. In plating and anodizing it dips parts through tanks in sequence. In assembly it presents parts at a fixed pace to a row of workers. The main variants are by track type, light formed-rail systems for small parts and heavy I-beam systems for large weldments, and by environment, with high-temperature chain and lubricant for oven duty and corrosion-resistant finishes for plating areas. What stays constant is the principle: one chain, one loop, one speed, with every carrier moving in lockstep.
Overhead Trolley Conveyor parts and their functions
7 top-level parts · 2,614 parts in total · full bill of materials below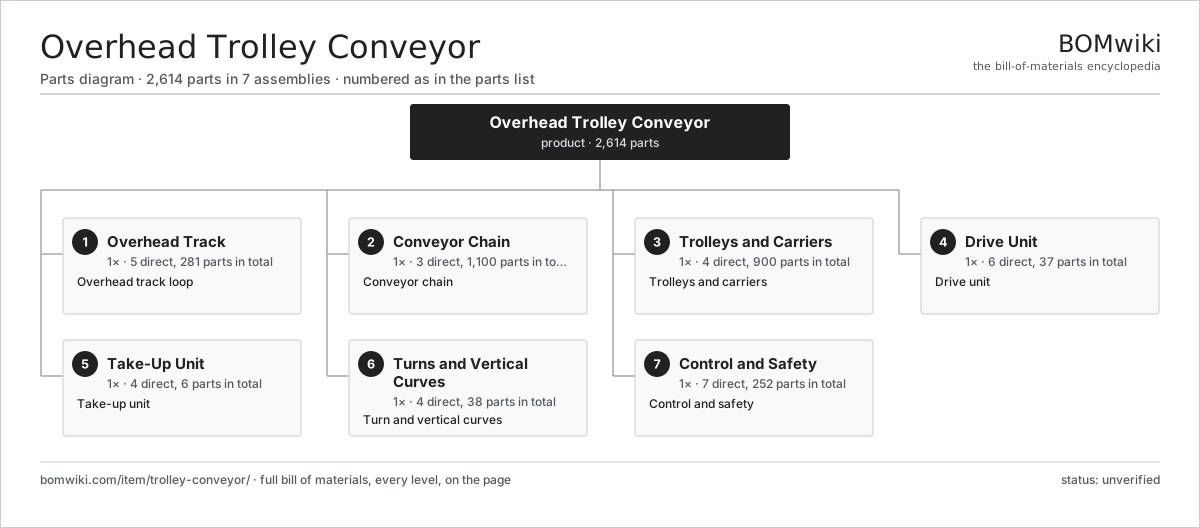
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Overhead Track 5 parts | 1× | Overhead track loop |
| 2 | Conveyor Chain 3 parts | 1× | Conveyor chain |
| 3 | Trolleys and Carriers 4 parts | 1× | Trolleys and carriers |
| 4 | Drive Unit 6 parts | 1× | Drive unit |
| 5 | Take-Up Unit 4 parts | 1× | Take-up unit |
| 6 | Turns and Vertical Curves 4 parts | 1× | Turn and vertical curves |
| 7 | Control and Safety 7 parts | 1× | Control and safety |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Overhead Trolley Conveyor
7 top-level lines · 60 rows shown · 2,614 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Overhead Track 5 parts | trolley-conveyor-track | 1× | 1 | 281 | assembly |
| 1.1 | Track Section | trolley-conveyor-track-section | 60× | 60 | · | part |
| 1.2 | Track Joint | trolley-conveyor-track-joint | 60× | 60 | · | part |
| 1.3 | Hanger Rod | trolley-conveyor-hanger-rod | 80× | 80 | · | part |
| 1.4 | Support Bracket | trolley-conveyor-support-bracket | 80× | 80 | · | part |
| 1.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Conveyor Chain 3 parts | trolley-conveyor-chain | 1× | 1 | 1,100 | assembly |
| 2.1 | Chain Link | trolley-conveyor-chain-link | 500× | 500 | · | part |
| 2.2 | Chain Pin | trolley-conveyor-chain-pin | 500× | 500 | · | part |
| 2.3 | Pendant Attachment | trolley-conveyor-pendant-attachment | 100× | 100 | · | part |
| 3 | Trolleys and Carriers 4 parts | trolley-conveyor-trolleys | 1× | 1 | 900 | assembly |
| 3.1 | Trolley 4 parts | trolley-conveyor-trolley | 100× | 100 | 6 | assembly |
| 3.1.1 | Trolley Wheel | trolley-conveyor-trolley-wheel | 2× | 200 | · | part |
| 3.1.2 | Ball Bearing | ball-bearing | 2× | 200 | · | part |
| 3.1.3 | Trolley Yoke | trolley-conveyor-trolley-yoke | 1× | 100 | · | part |
| 3.1.4 | Trolley Axle | trolley-conveyor-axle | 1× | 100 | · | part |
| 3.2 | Pendant | trolley-conveyor-pendant | 100× | 100 | · | part |
| 3.3 | Load Carrier | trolley-conveyor-carrier | 100× | 100 | · | part |
| 3.4 | Swivel Joint | trolley-conveyor-swivel | 100× | 100 | · | part |
| 4 | Drive Unit 6 parts | trolley-conveyor-drive | 1× | 1 | 37 | assembly |
| 4.1 | Drive Gearmotor 6 parts | trolley-conveyor-drive-gearmotor | 1× | 1 | 31 | assembly |
| 4.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 4.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 4.1.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 4.1.4 | Helical Gear Pair | gear-pair | 3× | 3 | · | part |
| 4.1.5 | Ball Bearing | ball-bearing | 3× | 3 | · | part |
| 4.1.6 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 4.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 4.3 | Drive Sprocket | trolley-conveyor-drive-sprocket | 1× | 1 | · | part |
| 4.4 | Drive Shaft | trolley-conveyor-drive-shaft | 1× | 1 | · | part |
| 4.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 4.6 | Shear Pin | trolley-conveyor-shear-pin | 1× | 1 | · | part |
| 5 | Take-Up Unit 4 parts | trolley-conveyor-takeup | 1× | 1 | 6 | assembly |
| 5.1 | Take-Up Sprocket | trolley-conveyor-takeup-sprocket | 1× | 1 | · | part |
| 5.2 | Take-Up Carriage | trolley-conveyor-takeup-carriage | 1× | 1 | · | part |
| 5.3 | Coil Spring | coil-spring | 2× | 2 | · | part |
| 5.4 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 6 | Turns and Vertical Curves 4 parts | trolley-conveyor-turns | 1× | 1 | 38 | assembly |
| 6.1 | Turn Wheel | trolley-conveyor-turn-wheel | 8× | 8 | · | part |
| 6.2 | Vertical Curve Section | trolley-conveyor-vertical-curve | 6× | 6 | · | part |
| 6.3 | Roller Turn | trolley-conveyor-roller-turn | 8× | 8 | · | part |
| 6.4 | Ball Bearing | ball-bearing | 16× | 16 | · | part |
| 7 | Control and Safety 7 parts | trolley-conveyor-control | 1× | 1 | 252 | assembly |
| 7.1 | Variable-Frequency Drive 5 parts | trolley-conveyor-vfd | 1× | 1 | 131 | assembly |
| 7.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.1.2 | Power MOSFET | mosfet | 6× | 6 | · | part |
| 7.1.3 | Gate Driver IC | gate-driver-ic | 3× | 3 | · | part |
| 7.1.4 | Power Inductor | power-inductor | 1× | 1 | · | part |
| 7.1.5 | SMD Passive (R/C/L) | smd-passives | 120× | 120 | · | part |
| 7.2 | Control Board 5 parts | trolley-conveyor-control-board | 1× | 1 | 110 | assembly |
| 7.2.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.2.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.2.3 | Relay | relay | 6× | 6 | · | part |
| 7.2.4 | Connector | connector | 12× | 12 | · | part |
| 7.2.5 | SMD Passive (R/C/L) | smd-passives | 90× | 90 | · | part |
| 7.3 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.5 | Jam Switch | trolley-conveyor-jam-switch | 4× | 4 | · | part |
| 7.6 | Pull-Cord E-Stop | trolley-conveyor-estop | 4× | 4 | · | part |
| 7.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Sliding-Shoe Sorter
4,321 parts · shares 9 with this page
 Tilt-Tray Sorter
6,031 parts · shares 8 with this page
 Vertical Spiral Conveyor
2,482 parts · shares 8 with this page
 Cross-Belt Sorter
25,040 parts · shares 7 with this page
Order Picker
708 parts · shares 6 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $2k–$300k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| toyota-industries.com ↗ | Kariya, JP | Forklifts & logistics | 20 units | 10–16 wks |
| kiongroup.com ↗ | Frankfurt, DE | Forklifts (Linde, STILL) | 20 units | 10–16 wks |
| jungheinrich.com ↗ | Hamburg, DE | Warehouse trucks | 20 units | 10–16 wks |
| crown.com ↗ | New Bremen, US | Forklifts | 20 units | 10–16 wks |
|
🇨🇳Hangcha
hcforklift.com ↗
|
Hangzhou, CN | Forklifts & material handling | 20 units | 10–16 wks |
900-word article