FDY Filament Spinning Line
ProductOverview
An FDY filament spinning line makes fully drawn yarn in one continuous pass, from dry polymer chips at the top to wound packages at the bottom. The yarn it makes is already drawn and heat-set when it leaves the line, so it needs no separate draw-twisting step before it goes to weaving or knitting. That is the difference between FDY and partially oriented yarn: a POY line spins and winds at high speed but leaves the drawing for a later machine, while an FDY line draws the filaments between heated godet rolls inside the same threadline and winds the finished, stable yarn directly.
The two polymers it handles most are polyester, which is PET, and nylon, which is PA. Both are spun the same way: melt the chips, push the melt through fine holes, cool the filaments, oil them, draw them, and wind them. The line is laid out vertically in a tower so the filaments fall under their own path from the spinneret down through quench and drawing to the winders.
Melt supply
Dried chips feed from the Chip Feed Hopper into the Single-Screw Extruder, where a nitrided Extruder Screw turns inside a heated Extruder Barrel and melts the polymer across several temperature zones. Drying matters because any moisture left in the chips breaks the polymer chains during melting and weakens the yarn. The molten polymer then passes through a Continuous Melt Filter that traps gels and unmelted particles before they can block a spinneret hole.
From the filter the melt goes to the Melt Booster Pump and along the diphyl-jacketed Heated Melt Distribution Pipe, which holds it at uniform temperature on the way to each spin beam. The single component that fixes yarn denier is the Metering Spin Pump. This precision gear pump meters an exact volume of melt per revolution, so the amount delivered to a position depends only on pump speed and not on pressure swings upstream. Set the pump speed against the winding speed and the denier is fixed.
Spinning and quench
Each Spin Beam & Spinneret Pack is a vapour-heated block that seats several Spinneret Pack cartridges and holds them all at the same spinning temperature using diphyl vapour from the Diphyl Vapour Heater. Inside a pack the melt passes the Sand Filter Media for a final filtration, spreads across the Distribution Plate, and extrudes through the hundreds of capillaries in the Spinneret Plate as a curtain of molten filaments.
The filaments fall straight into the Quench Chamber chamber. Cross-flow air from the Quench Supply Fan, conditioned to set temperature and humidity by the Quench Air Conditioner and straightened through the Air Rectifier Screen, blows across the descending curtain and solidifies the molten threads. Even cooling is what keeps every filament the same diameter, so quench air uniformity decides how level the finished yarn turns out.
Finish and drawing
Below the quench the cooled filaments gather at the Convergence Guide and pass the Metered Oiling Roller, which lays a thin even film of spin finish onto the bundle. The finish binds the filaments, gives antistatic protection, and lubricates the yarn for the godets and winder. The Finish Metering Pump meters the oil so pick-up stays constant.
Drawing happens in the Godet Drawing Section. Each Heated Godet Duo is a pair of induction-heated rolls that the yarn wraps several times, kept apart by a Separator Roll. The first duo holds the spun yarn at a moderate temperature. The next duos run faster and hotter, and the speed difference between successive duos stretches the filaments by the draw ratio, typically 1.4 to 1.8 times. Drawing aligns the polymer molecules along the filament axis, which is what gives FDY its strength and low shrinkage, and the hot godet surface heat-sets that orientation so the yarn stays stable. The Induction Heating Coil inside each godet heats the Godet Roll Shell shell directly, and the Godet Servo Drive holds each roll at its set speed so the ratios stay exact.
Intermingling and winding
After the last godet the yarn runs through the Intermingling Jet jet. The Air Entangling Nozzle injects pulses of compressed air across the bundle to tangle the filaments into regular nips, which holds the bundle together as one coherent yarn through later handling without needing a twist.
The yarn then reaches the Take-Up Winder. At winding speeds of 4,500 to 6,000 metres a minute the Contact Roll holds package speed constant while the Traverse Unit lays the yarn across the package for a firm build. When a package is full the Revolving Turret Head indexes a fresh tube into place and the Automatic Doffer transfers the yarn without stopping the line, so the threadline never breaks during a package change.
Control and structure
The Line Control System cabinet holds the full recipe: melt temperatures, spin pump speeds, quench air volume, godet speeds and temperatures, and winder settings. The Line PLC coordinates these and logs production per position, and the operator works from a touchscreen. The whole line stacks on the Spinning Tower Structure, a welded steel structure with Service Platform floors for access to the spin beam, godets and winders. Because the yarn path is vertical, the order of the floors follows the order of the process, from melt at the top down to the wound package at the bottom.
FDY Filament Spinning Line parts and their functions
11 top-level parts · 679 parts in total · full bill of materials below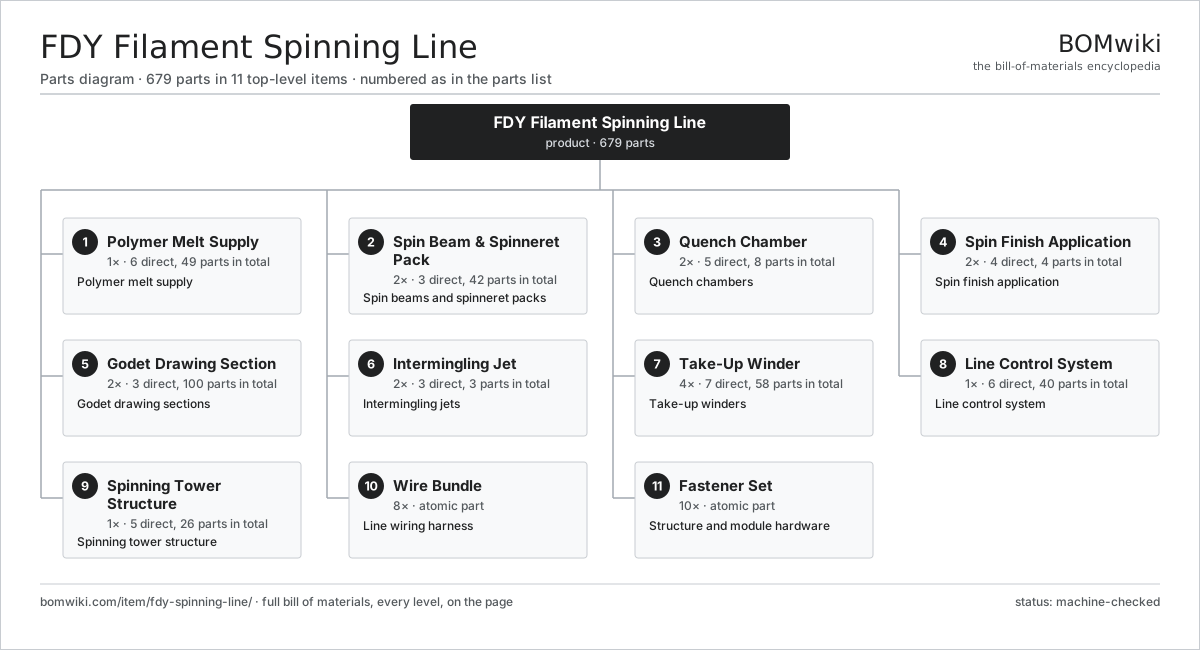
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Polymer Melt Supply 6 parts | 1× | Polymer melt supply |
| 2 | Spin Beam & Spinneret Pack 3 parts | 2× | Spin beams and spinneret packs |
| 3 | Quench Chamber 5 parts | 2× | Quench chambers |
| 4 | Spin Finish Application 4 parts | 2× | Spin finish application |
| 5 | Godet Drawing Section 3 parts | 2× | Godet drawing sections |
| 6 | Intermingling Jet 3 parts | 2× | Intermingling jets |
| 7 | Take-Up Winder 7 parts | 4× | Take-up winders |
| 8 | Line Control System 6 parts | 1× | Line control system |
| 9 | Spinning Tower Structure 5 parts | 1× | Spinning tower structure |
| 10 | Wire Bundle | 8× | Line wiring harness |
| 11 | Fastener Set | 10× | Structure and module hardware |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for FDY Filament Spinning Line
11 top-level lines · 83 rows shown · 679 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Polymer Melt Supply 6 parts | fdy-spinning-line-melt-supply | 1× | 1 | 49 | assembly |
| 1.1 | Single-Screw Extruder 7 parts | fdy-spinning-line-extruder | 1× | 1 | 38 | assembly |
| 1.1.1 | Extruder Screw | fdy-spinning-line-extruder-screw | 1× | 1 | · | part |
| 1.1.2 | Extruder Barrel | fdy-spinning-line-extruder-barrel | 1× | 1 | · | part |
| 1.1.3 | Chip Feed Hopper | fdy-spinning-line-feed-hopper | 1× | 1 | · | part |
| 1.1.4 | Heating Element | heating-element | 6× | 6 | · | part |
| 1.1.5 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 1.1.6 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 1.1.7 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 1.2 | Continuous Melt Filter | fdy-spinning-line-melt-filter | 1× | 1 | · | part |
| 1.3 | Melt Booster Pump | fdy-spinning-line-booster-pump | 1× | 1 | · | part |
| 1.4 | Metering Spin Pump | fdy-spinning-line-spin-pump | 4× | 4 | · | part |
| 1.5 | Heated Melt Distribution Pipe | fdy-spinning-line-melt-pipe | 1× | 1 | · | part |
| 1.6 | Pressure Sensor | pressure-sensor | 4× | 4 | · | part |
| 2 | Spin Beam & Spinneret Pack 3 parts | fdy-spinning-line-spin-beam | 2× | 2 | 42 | assembly |
| 2.1 | Vapour-Heated Beam Body | fdy-spinning-line-beam-body | 1× | 2 | · | part |
| 2.2 | Spinneret Pack 5 parts | fdy-spinning-line-spinneret-pack | 8× | 16 | 5 | assembly |
| 2.2.1 | Spinneret Plate | fdy-spinning-line-spinneret-plate | 1× | 16 | · | part |
| 2.2.2 | Distribution Plate | fdy-spinning-line-distribution-plate | 1× | 16 | · | part |
| 2.2.3 | Sand Filter Media | fdy-spinning-line-sand-filter | 1× | 16 | · | part |
| 2.2.4 | Breaker Plate | fdy-spinning-line-breaker-plate | 1× | 16 | · | part |
| 2.2.5 | O-Ring Set | oring-set | 1× | 16 | · | part |
| 2.3 | Diphyl Vapour Heater | fdy-spinning-line-vapour-heater | 1× | 2 | · | part |
| 3 | Quench Chamber 5 parts | fdy-spinning-line-quench | 2× | 2 | 8 | assembly |
| 3.1 | Quench Cabinet | fdy-spinning-line-quench-cabinet | 1× | 2 | · | part |
| 3.2 | Air Rectifier Screen | fdy-spinning-line-quench-screen | 1× | 2 | · | part |
| 3.3 | Quench Candle | fdy-spinning-line-quench-candle | 4× | 8 | · | part |
| 3.4 | Quench Air Conditioner | fdy-spinning-line-air-conditioner | 1× | 2 | · | part |
| 3.5 | Quench Supply Fan | fdy-spinning-line-quench-fan | 1× | 2 | · | part |
| 4 | Spin Finish Application 4 parts | fdy-spinning-line-finish | 2× | 2 | 4 | assembly |
| 4.1 | Metered Oiling Roller | fdy-spinning-line-oiling-roller | 1× | 2 | · | part |
| 4.2 | Finish Metering Pump | fdy-spinning-line-finish-pump | 1× | 2 | · | part |
| 4.3 | Finish Supply Tank | fdy-spinning-line-finish-tank | 1× | 2 | · | part |
| 4.4 | Convergence Guide | fdy-spinning-line-finish-guide | 1× | 2 | · | part |
| 5 | Godet Drawing Section 3 parts | fdy-spinning-line-godet-section | 2× | 2 | 100 | assembly |
| 5.1 | Heated Godet Duo 6 parts | fdy-spinning-line-godet-duo | 3× | 6 | 27 | assembly |
| 5.1.1 | Godet Roll Shell | fdy-spinning-line-godet-roll | 1× | 6 | · | part |
| 5.1.2 | Induction Heating Coil | fdy-spinning-line-induction-heater | 1× | 6 | · | part |
| 5.1.3 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 6 | 3 | assembly |
| 5.1.4 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 6 | 19 | assembly |
| 5.1.5 | Roll Surface Temperature Sensor | fdy-spinning-line-temp-sensor | 1× | 6 | · | part |
| 5.1.6 | Ball Bearing | ball-bearing | 2× | 12 | · | part |
| 5.2 | Separator Roll | fdy-spinning-line-separator-roll | 3× | 6 | · | part |
| 5.3 | Godet Drive & Heat Control 4 parts | fdy-spinning-line-godet-control | 1× | 2 | 16 | assembly |
| 5.3.1 | Godet Servo Drive | fdy-spinning-line-godet-drive | 3× | 6 | · | part |
| 5.3.2 | Bare PCB | pcb-bare | 1× | 2 | · | part |
| 5.3.3 | Relay | relay | 4× | 8 | · | part |
| 5.3.4 | Connector | connector | 8× | 16 | · | part |
| 6 | Intermingling Jet 3 parts | fdy-spinning-line-intermingling | 2× | 2 | 3 | assembly |
| 6.1 | Intermingling Jet Block | fdy-spinning-line-jet-block | 1× | 2 | · | part |
| 6.2 | Air Entangling Nozzle | fdy-spinning-line-jet-nozzle | 1× | 2 | · | part |
| 6.3 | Jet Air Regulator | fdy-spinning-line-air-regulator | 1× | 2 | · | part |
| 7 | Take-Up Winder 7 parts | fdy-spinning-line-winder | 4× | 4 | 58 | assembly |
| 7.1 | Revolving Turret Head | fdy-spinning-line-turret | 1× | 4 | · | part |
| 7.2 | Winding Chuck | fdy-spinning-line-chuck | 2× | 8 | · | part |
| 7.3 | Traverse Unit | fdy-spinning-line-traverse-unit | 1× | 4 | · | part |
| 7.4 | Contact Roll | fdy-spinning-line-contact-roll | 1× | 4 | · | part |
| 7.5 | Automatic Doffer | fdy-spinning-line-doffer | 1× | 4 | · | part |
| 7.6 | Servo Motor 4 parts | servo-motor | 2× | 8 | 24 | assembly |
| 7.6.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 8 | 3 | assembly |
| 7.6.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 8 | 19 | assembly |
| 7.6.3 | Encoder | encoder | 1× | 8 | · | part |
| 7.6.4 | Motor Housing | motor-housing | 1× | 8 | · | part |
| 7.7 | Ball Bearing | ball-bearing | 4× | 16 | · | part |
| 8 | Line Control System 6 parts | fdy-spinning-line-control | 1× | 1 | 40 | assembly |
| 8.1 | Line PLC 4 parts | fdy-spinning-line-plc | 1× | 1 | 9 | assembly |
| 8.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.1.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 8.1.4 | Connector | connector | 6× | 6 | · | part |
| 8.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.3 | Power Supply | power-supply | 2× | 2 | · | part |
| 8.4 | Microcontroller | mcu | 4× | 4 | · | part |
| 8.5 | Relay | relay | 8× | 8 | · | part |
| 8.6 | Connector | connector | 16× | 16 | · | part |
| 9 | Spinning Tower Structure 5 parts | fdy-spinning-line-tower | 1× | 1 | 26 | assembly |
| 9.1 | Welded Tower Frame | fdy-spinning-line-tower-frame | 1× | 1 | · | part |
| 9.2 | Service Platform | fdy-spinning-line-platform | 3× | 3 | · | part |
| 9.3 | Running-Part Guard | fdy-spinning-line-guard | 8× | 8 | · | part |
| 9.4 | Sheet Metal Panel | sheet-panel | 10× | 10 | · | part |
| 9.5 | Coil Spring | coil-spring | 4× | 4 | · | part |
| 10 | Wire Bundle | wire-bundle | 8× | 8 | · | part |
| 11 | Fastener Set | fastener-set | 10× | 10 | · | part |
Related products
same domain, ranked by shared parts Industrial Quilting Machine
1,090 parts · shares 8 with this page
Jigger Dyeing Machine
276 parts · shares 8 with this page
Spunlace Nonwoven Line
1,735 parts · shares 7 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇨🇭Rieter
rieter.com ↗
|
Winterthur, CH | Spinning machinery | 10 units | 14–24 wks |
| truetzschler.com ↗ | Mönchengladbach, DE | Textile machinery | 10 units | 14–24 wks |
|
🇧🇪Picanol
picanol.be ↗
|
Ypres, BE | Weaving machines | 10 units | 14–24 wks |
| karlmayer.com ↗ | Obertshausen, DE | Warp knitting machines | 10 units | 14–24 wks |
|
🇨🇭Saurer
saurer.com ↗
|
Arbon, CH | Spinning & embroidery | 10 units | 14–24 wks |
976-word article