Meltblown Nonwoven Line
ProductOverview
A meltblown nonwoven line turns polypropylene pellets into a fabric in one continuous pass, without ever spinning a yarn or weaving a thread. It melts the resin, pushes it through a row of tiny holes, and uses a sheet of hot fast air to draw each soft stream down to a fiber a few microns across. Those fibers cool in flight, land on a moving surface still slightly tacky, and tangle and self-bond into a web. The web is wound into rolls. The whole process is what gives meltblown its defining trait: extremely fine fibers, far finer than spunbond or carded webs, which is why the material is the filtration layer in surgical and respirator masks, in liquid and air filter cartridges, in oil-absorbent pads and in battery separators.
The line here is a single-beam machine built around the Meltblown Die Assembly, with an extruder feeding it, a melt pump metering it, a process air system attenuating the fiber, and a collector and winder turning out the finished roll.
How it works
Pellets fall from the Resin Feeding System into the Single-Screw Extruder, a single screw inside a heated barrel. As the screw turns, the resin is conveyed forward, compressed, and melted by a combination of barrel heat and shear until it leaves the barrel as a uniform melt near 250 °C. From there a Melt Gear Pump takes over the metering. A gear pump displaces a fixed volume per revolution, so output is set by its rpm and is steady regardless of small pressure swings upstream; this is what makes basis weight repeatable. Just ahead of it a Screen Changer holds a Filter Screen Pack that catches gels and grit, because a single contaminated particle can plug a die hole and leave a streak in the web.
The melt then enters the die. The Die Body carries a coat-hanger manifold that spreads the flow evenly across the full width, and the Die Tip / Nosepiece is a knife-edged nosepiece drilled with hundreds of capillary holes, roughly 0.3 mm each, across the working width. Melt extrudes from every hole as a thin stream. On both sides of the tip, the Air Knife Plate plates form a narrow slot that fires a sheet of hot, high-velocity air converging right at the hole exits. That air does the real work of meltblown: it grabs each soft filament and stretches it, thinning it from the hole diameter down to one to five microns before it cools and sets.
The process air system
Because attenuation is done by air, the Process Air System system is as important as the extruder. A high-pressure Process Air Blower supplies a large volume of air, and an inline Process Air Heater brings it up to roughly melt temperature so it stretches the fiber rather than quenching it. Two settings on this air, its temperature and its pressure, are the main levers for fiber diameter. Hotter, faster air makes finer fiber; cooler, slower air makes coarser fiber and a more open web. A Air Pressure Sensor at the die confirms the air is delivering the value the recipe calls for, and a Air Manifold splits the flow evenly to both air knives so the web is uniform from edge to edge.
Collecting and winding the web
The attenuated fibers blow downward onto the Web Collector. A perforated Collector Drum turns under the die, and a Suction Box beneath it pulls air through the holes to pin the fibers as they land and to carry the spent process air away through a Suction Fan. The fibers arrive still warm and slightly tacky, so they fuse at their crossing points and the web is self-bonded; no separate calender or adhesive is needed for a basic meltblown. The gap between die and drum, set by the Die-to-Collector Adjuster, controls how much the fiber cools in flight and therefore how lofty or dense the web is. From the drum the Winder pulls the web at controlled tension, trims and slits it to width, and winds it into rolls.
Materials and properties
The standard polymer is a high-melt-flow fiber-grade polypropylene, chosen because it melts cleanly, draws to fine fiber, and is cheap. The Additive Feeder can blend in masterbatch for colour or for special function. The most important add-on for filter media is an electret charge: many meltblown webs are charged after forming so that, on top of the mechanical sieving the fine fibers already do, electrostatic attraction pulls even smaller particles out of the air. That charge is what lets a thin meltblown layer reach N95 or FFP2 efficiency. Basis weight on this line ranges from light 10 g/m² facing layers up to 100 g/m² filter media, set by the ratio of pump output to collector speed.
Control and operation
The Control & HMI ties the line together. It holds every barrel and die zone to its setpoint through the Zone Temperature Controller modules, coordinates the screw, pump, collector and blower speeds through the Variable Frequency Drive drives, and runs the whole sequence from a saved recipe on the Operator HMI. An operator selects a product, the line heats up, purges, and comes to steady state; from there a single line can run for hours producing the same web. The hot die and the high-velocity air make guarding essential, so the Frame & Guarding carries interlocked panels and emergency stops around the forming zone.
Meltblown Nonwoven Line parts and their functions
9 top-level parts · 933 parts in total · full bill of materials below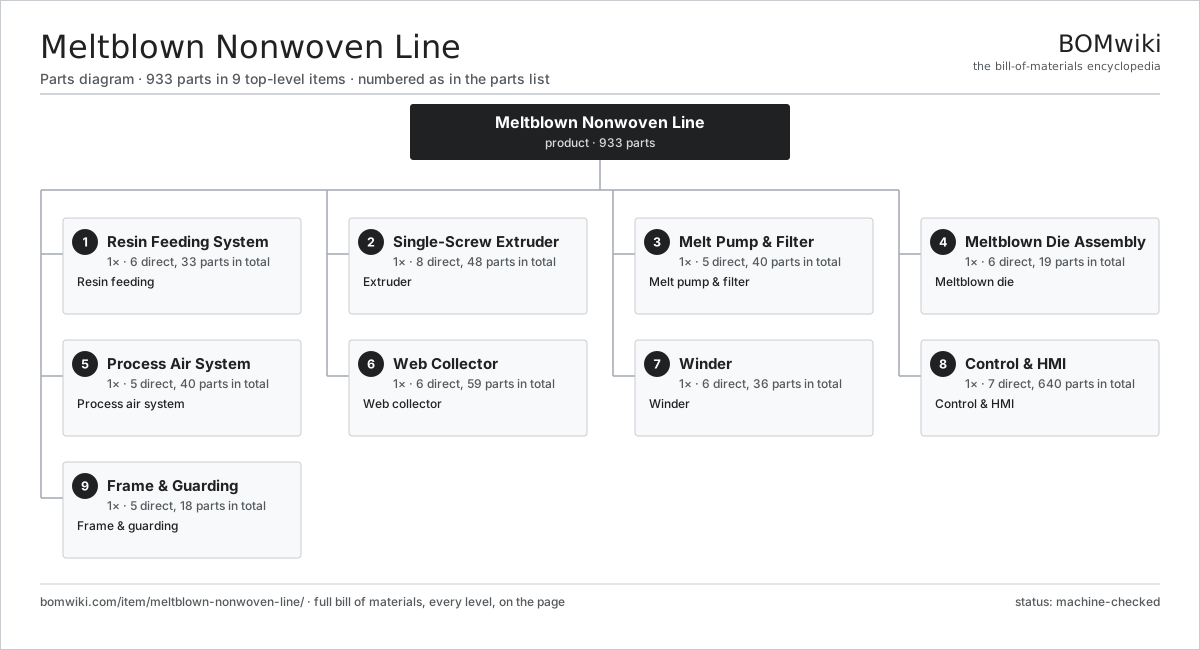
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Resin Feeding System 6 parts | 1× | Resin feeding |
| 2 | Single-Screw Extruder 8 parts | 1× | Extruder |
| 3 | Melt Pump & Filter 5 parts | 1× | Melt pump & filter |
| 4 | Meltblown Die Assembly 6 parts | 1× | Meltblown die |
| 5 | Process Air System 5 parts | 1× | Process air system |
| 6 | Web Collector 6 parts | 1× | Web collector |
| 7 | Winder 6 parts | 1× | Winder |
| 8 | Control & HMI 7 parts | 1× | Control & HMI |
| 9 | Frame & Guarding 5 parts | 1× | Frame & guarding |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Meltblown Nonwoven Line
9 top-level lines · 117 rows shown · 933 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Resin Feeding System 6 parts | meltblown-nonwoven-line-resin-feed | 1× | 1 | 33 | assembly |
| 1.1 | Resin Hopper | meltblown-nonwoven-line-hopper | 1× | 1 | · | part |
| 1.2 | Hopper Dryer 3 parts | meltblown-nonwoven-line-hopper-dryer | 1× | 1 | 4 | assembly |
| 1.2.1 | Heating Element | heating-element | 2× | 2 | · | part |
| 1.2.2 | Drying Blower | meltblown-nonwoven-line-dryer-blower | 1× | 1 | · | part |
| 1.2.3 | Desiccant Cartridge | meltblown-nonwoven-line-desiccant-cartridge | 1× | 1 | · | part |
| 1.3 | Metering Feed Screw | meltblown-nonwoven-line-feed-screw | 1× | 1 | · | part |
| 1.4 | Feed Drive 2 parts | meltblown-nonwoven-line-feed-motor | 1× | 1 | · | part |
| 1.4.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 1.4.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 1.5 | Additive Feeder | meltblown-nonwoven-line-additive-feeder | 1× | 1 | · | part |
| 1.6 | Hopper Level Sensor | meltblown-nonwoven-line-level-sensor | 1× | 1 | · | part |
| 2 | Single-Screw Extruder 8 parts | meltblown-nonwoven-line-extruder | 1× | 1 | 48 | assembly |
| 2.1 | Extruder Barrel | meltblown-nonwoven-line-barrel | 1× | 1 | · | part |
| 2.2 | Extruder Screw | meltblown-nonwoven-line-screw | 1× | 1 | · | part |
| 2.3 | Barrel Band Heater 1 parts | meltblown-nonwoven-line-barrel-heaters | 6× | 6 | · | part |
| 2.3.1 | Heating Element | heating-element | 1× | 6 | · | part |
| 2.4 | Barrel Cooling Fan | meltblown-nonwoven-line-barrel-cooling | 4× | 4 | · | part |
| 2.5 | Screw Drive 4 parts | meltblown-nonwoven-line-extruder-drive | 1× | 1 | 28 | assembly |
| 2.5.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 2.5.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 2.5.3 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 2.5.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 2.6 | Thrust Bearing Block 2 parts | meltblown-nonwoven-line-thrust-bearing | 1× | 1 | · | part |
| 2.6.1 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 2.6.2 | Oil Seal | oil-seal | 1× | 1 | · | part |
| 2.7 | Melt Thermocouple | meltblown-nonwoven-line-melt-thermocouple | 4× | 4 | · | part |
| 2.8 | Head Pressure Sensor 1 parts | meltblown-nonwoven-line-head-pressure-sensor | 1× | 1 | · | part |
| 2.8.1 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 3 | Melt Pump & Filter 5 parts | meltblown-nonwoven-line-melt-pump-filter | 1× | 1 | 40 | assembly |
| 3.1 | Melt Gear Pump 4 parts | meltblown-nonwoven-line-gear-pump | 1× | 1 | 8 | assembly |
| 3.1.1 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 3.1.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 3.1.3 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 3.1.4 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 3.2 | Pump Drive 2 parts | meltblown-nonwoven-line-pump-drive | 1× | 1 | · | part |
| 3.2.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 3.2.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 3.3 | Screen Changer | meltblown-nonwoven-line-screen-changer | 1× | 1 | · | part |
| 3.4 | Filter Screen Pack | meltblown-nonwoven-line-filter-screen | 4× | 4 | · | part |
| 3.5 | Heated Transfer Pipe 1 parts | meltblown-nonwoven-line-transfer-pipe | 1× | 1 | · | part |
| 3.5.1 | Heating Element | heating-element | 2× | 2 | · | part |
| 4 | Meltblown Die Assembly 6 parts | meltblown-nonwoven-line-die-assembly | 1× | 1 | 19 | assembly |
| 4.1 | Die Body | meltblown-nonwoven-line-die-body | 1× | 1 | · | part |
| 4.2 | Die Tip / Nosepiece | meltblown-nonwoven-line-die-tip | 1× | 1 | · | part |
| 4.3 | Air Knife Plate | meltblown-nonwoven-line-air-knife | 2× | 2 | · | part |
| 4.4 | Die Band Heater 1 parts | meltblown-nonwoven-line-die-heaters | 8× | 8 | · | part |
| 4.4.1 | Heating Element | heating-element | 1× | 8 | · | part |
| 4.5 | Die Thermocouple | meltblown-nonwoven-line-die-thermocouple | 6× | 6 | · | part |
| 4.6 | Die Clamp Bolting 1 parts | meltblown-nonwoven-line-die-bolt | 1× | 1 | · | part |
| 4.6.1 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 5 | Process Air System 5 parts | meltblown-nonwoven-line-process-air | 1× | 1 | 40 | assembly |
| 5.1 | Process Air Blower 4 parts | meltblown-nonwoven-line-air-blower | 1× | 1 | 28 | assembly |
| 5.1.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 5.1.2 | Blower Impeller | meltblown-nonwoven-line-impeller | 1× | 1 | · | part |
| 5.1.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 5.1.4 | Blower Housing | meltblown-nonwoven-line-blower-housing | 1× | 1 | · | part |
| 5.2 | Process Air Heater 3 parts | meltblown-nonwoven-line-air-heater | 1× | 1 | 9 | assembly |
| 5.2.1 | Heating Element | heating-element | 6× | 6 | · | part |
| 5.2.2 | Air Heater Shell | meltblown-nonwoven-line-heater-shell | 1× | 1 | · | part |
| 5.2.3 | Air Thermocouple | meltblown-nonwoven-line-air-thermocouple | 2× | 2 | · | part |
| 5.3 | Air Intake Filter | meltblown-nonwoven-line-air-filter | 1× | 1 | · | part |
| 5.4 | Air Manifold | meltblown-nonwoven-line-air-manifold | 1× | 1 | · | part |
| 5.5 | Air Pressure Sensor 1 parts | meltblown-nonwoven-line-air-pressure-sensor | 1× | 1 | · | part |
| 5.5.1 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 6 | Web Collector 6 parts | meltblown-nonwoven-line-collector | 1× | 1 | 59 | assembly |
| 6.1 | Collector Drum | meltblown-nonwoven-line-collector-drum | 1× | 1 | · | part |
| 6.2 | Collector Drive 2 parts | meltblown-nonwoven-line-collector-drive | 1× | 1 | · | part |
| 6.2.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 6.2.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 6.3 | Suction Box | meltblown-nonwoven-line-suction-box | 1× | 1 | · | part |
| 6.4 | Suction Fan 3 parts | meltblown-nonwoven-line-suction-fan | 1× | 1 | 27 | assembly |
| 6.4.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 6.4.2 | Blower Impeller | meltblown-nonwoven-line-impeller | 1× | 1 | · | part |
| 6.4.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 6.5 | Die-to-Collector Adjuster 2 parts | meltblown-nonwoven-line-dcd-adjuster | 1× | 1 | · | part |
| 6.5.1 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 6.5.2 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 6.6 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 7 | Winder 6 parts | meltblown-nonwoven-line-winder | 1× | 1 | 36 | assembly |
| 7.1 | Winding Shaft | meltblown-nonwoven-line-wind-shaft | 1× | 1 | · | part |
| 7.2 | Winder Drive 2 parts | meltblown-nonwoven-line-wind-drive | 1× | 1 | · | part |
| 7.2.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 7.2.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 7.3 | Nip Roll | meltblown-nonwoven-line-nip-roll | 2× | 2 | · | part |
| 7.4 | Tension Dancer 1 parts | meltblown-nonwoven-line-tension-roll | 1× | 1 | · | part |
| 7.4.1 | Coil Spring | coil-spring | 2× | 2 | · | part |
| 7.5 | Slitter Knife | meltblown-nonwoven-line-slitter | 2× | 2 | · | part |
| 7.6 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 8 | Control & HMI 7 parts | meltblown-nonwoven-line-control | 1× | 1 | 640 | assembly |
| 8.1 | PLC 4 parts | meltblown-nonwoven-line-plc | 1× | 1 | 171 | assembly |
| 8.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.1.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 8.1.3 | Relay | relay | 8× | 8 | · | part |
| 8.1.4 | SMD Passive (R/C/L) | smd-passives | 160× | 160 | · | part |
| 8.2 | Operator HMI 4 parts | meltblown-nonwoven-line-hmi | 1× | 1 | 63 | assembly |
| 8.2.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.2.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.2.3 | Touch Digitizer | touch-digitizer | 1× | 1 | · | part |
| 8.2.4 | SMD Passive (R/C/L) | smd-passives | 60× | 60 | · | part |
| 8.3 | Zone Temperature Controller 3 parts | meltblown-nonwoven-line-temp-controller | 4× | 4 | · | part |
| 8.3.1 | Bare PCB | pcb-bare | 1× | 4 | · | part |
| 8.3.2 | Microcontroller | mcu | 1× | 4 | · | part |
| 8.3.3 | Relay | relay | 1× | 4 | · | part |
| 8.4 | Variable Frequency Drive 3 parts | meltblown-nonwoven-line-vfd | 4× | 4 | · | part |
| 8.4.1 | Bare PCB | pcb-bare | 1× | 4 | · | part |
| 8.4.2 | Microcontroller | mcu | 1× | 4 | · | part |
| 8.4.3 | SMD Passive (R/C/L) | smd-passives | 90× | 360 | · | part |
| 8.5 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8.7 | Connector | connector | 24× | 24 | · | part |
| 9 | Frame & Guarding 5 parts | meltblown-nonwoven-line-frame | 1× | 1 | 18 | assembly |
| 9.1 | Base Frame | meltblown-nonwoven-line-base-frame | 1× | 1 | · | part |
| 9.2 | Sheet Metal Panel | sheet-panel | 8× | 8 | · | part |
| 9.3 | Guard Interlock | meltblown-nonwoven-line-interlock | 3× | 3 | · | part |
| 9.4 | Emergency Stop | meltblown-nonwoven-line-estop | 2× | 2 | · | part |
| 9.5 | Fastener Set | fastener-set | 4× | 4 | · | part |
Related products
same domain, ranked by shared parts Automatic Fabric Cutting Machine
1,695 parts · shares 12 with this page
 Rotary Screen Textile Printer
3,441 parts · shares 11 with this page
Textile Calendering Machine
623 parts · shares 10 with this page
Mercerizing Range
585 parts · shares 11 with this page
Laser Fabric Cutting Machine
297 parts · shares 10 with this page
 Industrial Quilting Machine
1,090 parts · shares 10 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇨🇭Rieter
rieter.com ↗
|
Winterthur, CH | Spinning machinery | 10 units | 14–24 wks |
| truetzschler.com ↗ | Mönchengladbach, DE | Textile machinery | 10 units | 14–24 wks |
|
🇧🇪Picanol
picanol.be ↗
|
Ypres, BE | Weaving machines | 10 units | 14–24 wks |
| karlmayer.com ↗ | Obertshausen, DE | Warp knitting machines | 10 units | 14–24 wks |
|
🇨🇭Saurer
saurer.com ↗
|
Arbon, CH | Spinning & embroidery | 10 units | 14–24 wks |
976-word article