Metal Roofing Roll Former
ProductOverview
A metal roofing roll former turns a flat coil of coated steel into finished standing-seam roof panels in one continuous pass. Coil enters at one end, the strip is bent a small amount at each of sixteen to twenty stations, and a cut panel of the chosen length comes off the other end ready to load onto a truck. The Coil Decoiler pays the coil off, the Entry Guide and Feed feeds it square into the rolls, the Roll-Forming Station Bank shapes the profile, the Length-Measure Encoder counts length, and the Hydraulic Cutoff Shear cuts each panel without stopping the line. A typical line runs 12 to 30 metres a minute, so a crew can roll a roof's worth of panels on site in an hour or two and avoid shipping long finished panels over the road.
Roll forming suits roofing because the same set of rollers makes panels of any length from the same coil. The tooling is fixed to one profile, but length is just a number the operator types in, so a run of short panels for a porch and long panels for a barn comes off the same machine with no tooling change.
Decoiler and strip feed
The Coil Decoiler carries the steel coil on an Expanding Mandrel that expands inside the coil bore to grip it. The Decoiler Stand takes the full coil weight, often several tonnes, and a Drag Brake holds back tension so the coil does not overrun and dump loose strip when the line slows. A Decoiler Motor pays the coil off in step with the line, and a Loop Arm dancer senses slack between coil and machine so the two stay matched.
From there the Entry Guide and Feed sets the strip up for the rolls. Two Side Guide rails hold the strip edges so it enters centered, a pair of Pinch Roller units grip and push it into the first station, and an Edge Sensor reports tracking. If the strip enters off center, the seam legs land in the wrong place and panels will not lock, so this stage decides whether the finished panels fit together on the roof.
The forming station bank
The Roll-Forming Station Bank is the heart of the machine. It holds the Forming Station passes in line on a single machined Base Beam so every station sits at the same height. Each station carries a Top Roller Die and a Bottom Roller Die mounted on two Roller Shaft shafts in a Station Housing. Each pass bends the strip only a few degrees more than the last, which spreads the work so the coating does not crack and the steel does not tear. The first stations turn up the edges, the middle stations raise the seam legs, and two Center Rib Station passes roll a stiffening rib into the flat pan with Rib Roller tools so a wide panel stays flat and does not oil-can in the sun. A Roller Shim Set sets the roller gap to the exact coil thickness.
Drive line
Every roller shaft has to turn at the same surface speed or the strip would stretch or bunch between stations. The Drive Line handles this with one Main Drive Motor feeding a Reduction Gearbox, whose output runs a Drive Chain over a Shaft Sprocket on each shaft. Driving every shaft from one chain keeps the line in time. A Chain Tensioner holds chain slack and a Chain Guard encloses the run and keeps the oil in.
Cutoff, measure, and seam tooling
Length comes from the Length-Measure Encoder unit, where a Measuring Wheel rides on the moving panel and turns a Rotary Encoder held down by an Encoder Arm. When the count reaches the set length, the Hydraulic Cutoff Shear fires. Its Shear Cylinder drives a profiled Shear Blade through the panel, with oil from the Hydraulic Power Pack. The blade is ground to the panel profile so it cuts across the seams and ribs without crushing them. The last passes in the Seaming Profile Tooling form the Male Leg Roller and Female Leg Roller legs of the standing seam, with a Clip Relief Roller leaving room for the hidden clip.
Run-out and control
Finished panels run onto the Run-Out Table table, where free Run-Out Roller rollers carry the panel without scratching its coating and Stacking Arm arms lift it onto the stack. The Control Cabinet cabinet ties it together: a PLC runs the logic and reads the encoder, a Operator Panel panel takes the length and batch count, and a Variable Frequency Drive sets motor speed so length count and shear timing stay accurate. Many of these lines are built into a trailer so a roofing crew can roll panels in the yard or at the job site straight from coil.
Metal Roofing Roll Former parts and their functions
9 top-level parts · 704 parts in total · full bill of materials below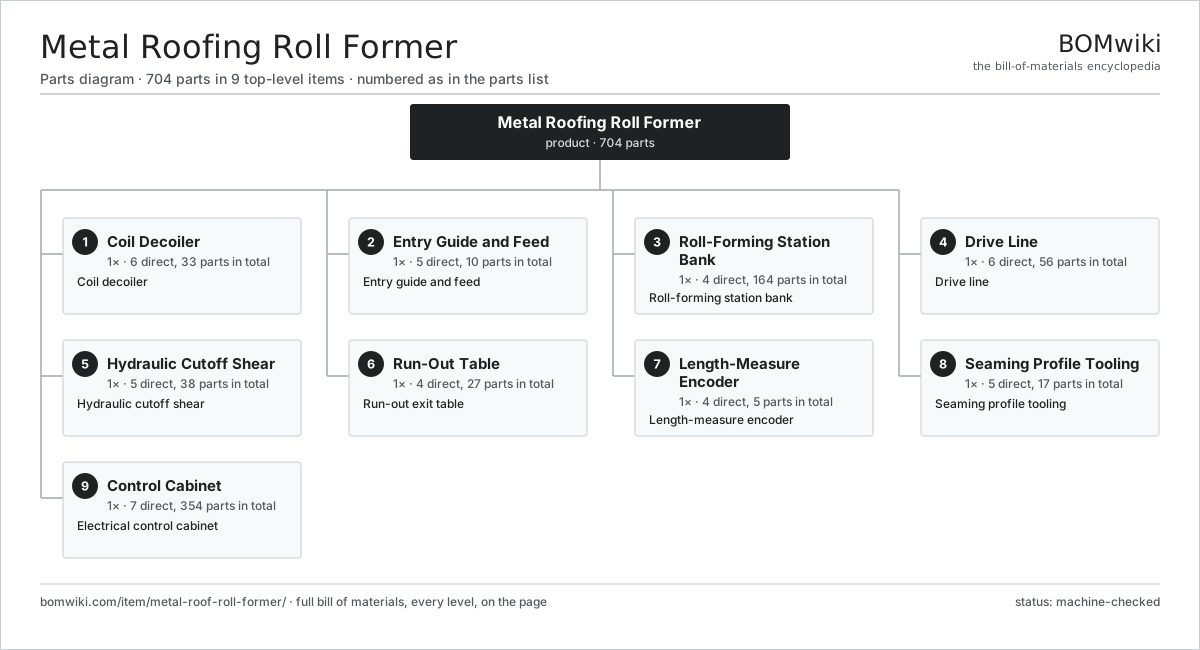
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Coil Decoiler 6 parts | 1× | Coil decoiler |
| 2 | Entry Guide and Feed 5 parts | 1× | Entry guide and feed |
| 3 | Roll-Forming Station Bank 4 parts | 1× | Roll-forming station bank |
| 4 | Drive Line 6 parts | 1× | Drive line |
| 5 | Hydraulic Cutoff Shear 5 parts | 1× | Hydraulic cutoff shear |
| 6 | Run-Out Table 4 parts | 1× | Run-out exit table |
| 7 | Length-Measure Encoder 4 parts | 1× | Length-measure encoder |
| 8 | Seaming Profile Tooling 5 parts | 1× | Seaming profile tooling |
| 9 | Control Cabinet 7 parts | 1× | Electrical control cabinet |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Metal Roofing Roll Former
9 top-level lines · 95 rows shown · 704 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Coil Decoiler 6 parts | metal-roof-roll-former-decoiler | 1× | 1 | 33 | assembly |
| 1.1 | Expanding Mandrel | metal-roof-roll-former-mandrel | 1× | 1 | · | part |
| 1.2 | Decoiler Stand | metal-roof-roll-former-decoiler-frame | 1× | 1 | · | part |
| 1.3 | Drag Brake | metal-roof-roll-former-coil-brake | 1× | 1 | · | part |
| 1.4 | Decoiler Motor 4 parts | metal-roof-roll-former-decoiler-motor | 1× | 1 | 25 | assembly |
| 1.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 1.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 1.4.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 1.4.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 1.5 | Loop Arm | metal-roof-roll-former-loop-arm | 1× | 1 | · | part |
| 1.6 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 2 | Entry Guide and Feed 5 parts | metal-roof-roll-former-entry-guide | 1× | 1 | 10 | assembly |
| 2.1 | Side Guide | metal-roof-roll-former-side-guide | 2× | 2 | · | part |
| 2.2 | Pinch Roller | metal-roof-roll-former-pinch-roller | 2× | 2 | · | part |
| 2.3 | Entry Table | metal-roof-roll-former-entry-table | 1× | 1 | · | part |
| 2.4 | Edge Sensor | metal-roof-roll-former-edge-sensor | 1× | 1 | · | part |
| 2.5 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 3 | Roll-Forming Station Bank 4 parts | metal-roof-roll-former-forming-bank | 1× | 1 | 164 | assembly |
| 3.1 | Forming Station 5 parts | metal-roof-roll-former-forming-station | 16× | 16 | 9 | assembly |
| 3.1.1 | Top Roller Die | metal-roof-roll-former-top-roller | 1× | 16 | · | part |
| 3.1.2 | Bottom Roller Die | metal-roof-roll-former-bottom-roller | 1× | 16 | · | part |
| 3.1.3 | Roller Shaft | metal-roof-roll-former-roller-shaft | 2× | 32 | · | part |
| 3.1.4 | Station Housing | metal-roof-roll-former-station-housing | 1× | 16 | · | part |
| 3.1.5 | Ball Bearing | ball-bearing | 4× | 64 | · | part |
| 3.2 | Base Beam | metal-roof-roll-former-bank-base | 1× | 1 | · | part |
| 3.3 | Center Rib Station 4 parts | metal-roof-roll-former-rib-station | 2× | 2 | 9 | assembly |
| 3.3.1 | Rib Roller | metal-roof-roll-former-rib-roller | 2× | 4 | · | part |
| 3.3.2 | Roller Shaft | metal-roof-roll-former-roller-shaft | 2× | 4 | · | part |
| 3.3.3 | Station Housing | metal-roof-roll-former-station-housing | 1× | 2 | · | part |
| 3.3.4 | Ball Bearing | ball-bearing | 4× | 8 | · | part |
| 3.4 | Roller Shim Set | metal-roof-roll-former-shim-set | 1× | 1 | · | part |
| 4 | Drive Line 6 parts | metal-roof-roll-former-drive-line | 1× | 1 | 56 | assembly |
| 4.1 | Main Drive Motor 4 parts | metal-roof-roll-former-main-motor | 1× | 1 | 25 | assembly |
| 4.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 4.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 4.1.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 4.1.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 4.2 | Reduction Gearbox 4 parts | metal-roof-roll-former-gearbox | 1× | 1 | 9 | assembly |
| 4.2.1 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 4.2.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 4.2.3 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 4.2.4 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 4.3 | Drive Chain | metal-roof-roll-former-drive-chain | 1× | 1 | · | part |
| 4.4 | Shaft Sprocket | metal-roof-roll-former-sprocket | 18× | 18 | · | part |
| 4.5 | Chain Guard | metal-roof-roll-former-chain-guard | 1× | 1 | · | part |
| 4.6 | Chain Tensioner | metal-roof-roll-former-tensioner | 2× | 2 | · | part |
| 5 | Hydraulic Cutoff Shear 5 parts | metal-roof-roll-former-shear | 1× | 1 | 38 | assembly |
| 5.1 | Shear Blade | metal-roof-roll-former-shear-blade | 2× | 2 | · | part |
| 5.2 | Shear Cylinder 3 parts | metal-roof-roll-former-shear-cylinder | 1× | 1 | 3 | assembly |
| 5.2.1 | Shear Cylinder Tube | metal-roof-roll-former-shear-tube | 1× | 1 | · | part |
| 5.2.2 | Shear Cylinder Rod | metal-roof-roll-former-shear-rod | 1× | 1 | · | part |
| 5.2.3 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 5.3 | Shear Frame | metal-roof-roll-former-shear-frame | 1× | 1 | · | part |
| 5.4 | Hydraulic Power Pack 5 parts | metal-roof-roll-former-power-pack | 1× | 1 | 31 | assembly |
| 5.4.1 | Hydraulic Pump | metal-roof-roll-former-hyd-pump | 1× | 1 | · | part |
| 5.4.2 | Pump Motor 4 parts + deeper › | metal-roof-roll-former-hyd-motor | 1× | 1 | 25 | assembly |
| 5.4.3 | Oil Tank | metal-roof-roll-former-oil-tank | 1× | 1 | · | part |
| 5.4.4 | Valve Block 3 parts + deeper › | metal-roof-roll-former-valve-block | 1× | 1 | 3 | assembly |
| 5.4.5 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 5.5 | Die Shoe | metal-roof-roll-former-die-shoe | 1× | 1 | · | part |
| 6 | Run-Out Table 4 parts | metal-roof-roll-former-runout | 1× | 1 | 27 | assembly |
| 6.1 | Run-Out Roller | metal-roof-roll-former-runout-roller | 8× | 8 | · | part |
| 6.2 | Run-Out Frame | metal-roof-roll-former-runout-frame | 1× | 1 | · | part |
| 6.3 | Stacking Arm | metal-roof-roll-former-stack-arm | 2× | 2 | · | part |
| 6.4 | Ball Bearing | ball-bearing | 16× | 16 | · | part |
| 7 | Length-Measure Encoder 4 parts | metal-roof-roll-former-measure | 1× | 1 | 5 | assembly |
| 7.1 | Measuring Wheel | metal-roof-roll-former-measure-wheel | 1× | 1 | · | part |
| 7.2 | Rotary Encoder | metal-roof-roll-former-encoder | 1× | 1 | · | part |
| 7.3 | Encoder Arm | metal-roof-roll-former-encoder-arm | 1× | 1 | · | part |
| 7.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 8 | Seaming Profile Tooling 5 parts | metal-roof-roll-former-seamer-tooling | 1× | 1 | 17 | assembly |
| 8.1 | Male Leg Roller | metal-roof-roll-former-male-leg-roller | 2× | 2 | · | part |
| 8.2 | Female Leg Roller | metal-roof-roll-former-female-leg-roller | 2× | 2 | · | part |
| 8.3 | Seam Roller Shaft | metal-roof-roll-former-seam-shaft | 4× | 4 | · | part |
| 8.4 | Clip Relief Roller | metal-roof-roll-former-clip-relief-roller | 1× | 1 | · | part |
| 8.5 | Ball Bearing | ball-bearing | 8× | 8 | · | part |
| 9 | Control Cabinet 7 parts | metal-roof-roll-former-control | 1× | 1 | 354 | assembly |
| 9.1 | PLC 3 parts | metal-roof-roll-former-plc | 1× | 1 | 143 | assembly |
| 9.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.1.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 9.1.3 | SMD Passive (R/C/L) | smd-passives | 140× | 140 | · | part |
| 9.2 | Operator Panel 4 parts | metal-roof-roll-former-hmi | 1× | 1 | 83 | assembly |
| 9.2.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 9.2.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.2.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.2.4 | SMD Passive (R/C/L) | smd-passives | 80× | 80 | · | part |
| 9.3 | Variable Frequency Drive 4 parts | metal-roof-roll-former-vfd | 1× | 1 | 94 | assembly |
| 9.3.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.3.2 | IGBT Power Module | igbt-module | 1× | 1 | · | part |
| 9.3.3 | DC-Link Capacitor | dc-link-cap | 2× | 2 | · | part |
| 9.3.4 | SMD Passive (R/C/L) | smd-passives | 90× | 90 | · | part |
| 9.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 9.5 | Relay | relay | 8× | 8 | · | part |
| 9.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9.7 | Connector | connector | 24× | 24 | · | part |
Related products
same domain, ranked by shared parts Fiber Cement Sheet Machine
819 parts · shares 21 with this page
Insulated Sandwich Panel Line
1,856 parts · shares 21 with this page
Roof Tile Press
443 parts · shares 18 with this page
 Hollowcore Slab Extruder
547 parts · shares 17 with this page
 Precast Concrete Mold
493 parts · shares 17 with this page
 Geomembrane Welding Machine
273 parts · shares 16 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $50–$10k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| assaabloy.com ↗ | Stockholm, SE | Locks & access | 1,000 units | 8–12 wks |
|
🇺🇸Allegion
allegion.com ↗
|
Dublin, US | Security products (Schlage) | 1,000 units | 8–12 wks |
| dormakaba.com ↗ | Rümlang, CH | Access & door systems | 1,000 units | 8–12 wks |
| honeywell.com ↗ | Charlotte, US | Building & safety tech | 1,000 units | 8–12 wks |
| hikvision.com ↗ | Hangzhou, CN | Surveillance & security | 1,000 units | 8–12 wks |
975-word article