Roof Tile Press
ProductOverview
A roof tile press forms one interlocking roofing tile at a time by squeezing a measured charge of stiff concrete or clay mix between two shaped dies. Each cycle the Feed System doses a level charge of mix into the lower die, the Vibration Table table settles it, then the Pressing Ram drives the upper die down at several hundred kilonewtons to compact the mix into a dense green tile with its curved face, hanging nibs, and side interlock fully formed. The Demoulding Unit unit lifts the tile on its pallet clear of the mould and sends it to curing, while an empty pallet is placed for the next stroke. A small machine makes twenty tiles a minute and a large automatic line makes sixty or more, which is why a single press can supply a roof's worth of tiles in a few hours.
The press is built around a stiff Press Frame that reacts the pressing load, a Hydraulic Power Pack that supplies controlled high-pressure oil, the Mould Set that defines the tile shape, and a Control Cabinet cabinet that sequences the whole cycle. Because the tile profile carries water and locks to its neighbours, the tooling and the compaction matter as much as the raw force.
The press frame and ram
The Press Frame is a welded four-column structure. A heavy Base Frame anchors the machine to the floor and carries the Bed Plate, a ground wear plate that keeps every tile the same thickness. Four Guide Column tie rods run up to the Head Beam, which mounts the pressing cylinder and reacts the full ram force back into the frame. Using columns in tension rather than a closed C-frame keeps the press from springing open under load, so the tile thickness holds steady.
The Pressing Ram is the moving half. Its Main Cylinder is a large-bore hydraulic cylinder with a honed Cylinder Tube and a hard-chromed Piston Rod sealed by a Piston Seal Kit kit. The rod pushes the Moving Platen, which slides on the columns through four bronze Guide Bush sleeves and a pair of Linear Guide Rail rails so it stays square. The Upper Mould Mount lets the operator swap tooling quickly when changing tile profiles.
Tooling and tile shape
The Mould Set is the part that decides what tile comes out. The Upper Mould forms the weather face, the curved barrel of a pantile, and the small nibs, while the Lower Mould forms the underside and the hanging nib that hooks over the batten on the roof. Both dies are hardened tool steel because the abrasive mix would quickly wear soft tooling. The Interlock Insert pieces form the overlapping side channel that locks each tile to its neighbour and sheds rain at the joint. Every tile is pressed onto a steel Tile Pallet that carries the fragile green tile through curing without handling it directly.
Feeding, vibration, and compaction
Tile density comes from combining vibration with pressure, so two subsystems work together. The Feed System holds mix in a Mix Hopper fed by a Feed Belt, then a Dosing Slide driven by a Feed Cylinder carries a fixed volume of mix over the mould and the Scraper strikes it level. Volumetric dosing keeps tile weight consistent without weighing every charge. The Vibration Table table then shakes the mould with eccentric Vibrator units mounted on rubber Isolation Mount isolators, which de-airs the mix and lets it flow into the corners of the die before the ram presses. Without that vibration the pressed tile would carry voids that let water through and weaken it.
Hydraulics and power
The Hydraulic Power Pack supplies the muscle. A variable Hydraulic Pump driven by the Pump Motor draws oil from the Oil Tank and feeds the Valve Block, where Directional Valve spools route oil to extend and retract each cylinder and a Relief Valve caps the pressure. An Accumulator stores oil so the pressing stroke is fast and an Oil Cooler sheds the heat that high-rate cycling generates. Two Pressure Sensor units report line pressure so the controller can verify each press reached its target force.
Demoulding, control, and use
After the press, the Demoulding Unit unit drives the Ejector to lift the tile and pallet, and the Pallet Conveyor carries it away while the Pickup Arm sets a fresh pallet. The Control Cabinet cabinet runs the sequence: a PLC holds the cycle logic and interlocks, a Operator Panel panel selects the tile recipe and shows counts and faults, and a Variable Frequency Drive sets the pump and conveyor speeds. Concrete tiles cure for hours on their pallets before stacking, while clay tiles go on to drying and a kiln. Roof tile presses run in tile plants and in regional yards near construction demand, since shipping finished tiles is costly and local pressing from local aggregate is the cheaper route to a roof.
Roof Tile Press parts and their functions
8 top-level parts · 443 parts in total · full bill of materials below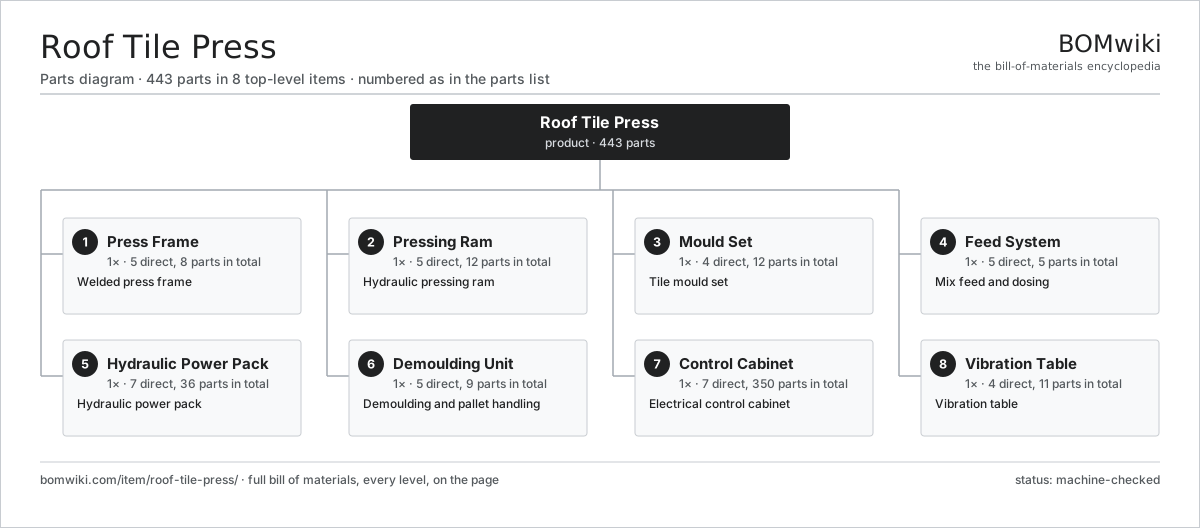
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Press Frame 5 parts | 1× | Welded press frame |
| 2 | Pressing Ram 5 parts | 1× | Hydraulic pressing ram |
| 3 | Mould Set 4 parts | 1× | Tile mould set |
| 4 | Feed System 5 parts | 1× | Mix feed and dosing |
| 5 | Hydraulic Power Pack 7 parts | 1× | Hydraulic power pack |
| 6 | Demoulding Unit 5 parts | 1× | Demoulding and pallet handling |
| 7 | Control Cabinet 7 parts | 1× | Electrical control cabinet |
| 8 | Vibration Table 4 parts | 1× | Vibration table |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Roof Tile Press
8 top-level lines · 72 rows shown · 443 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Press Frame 5 parts | roof-tile-press-frame | 1× | 1 | 8 | assembly |
| 1.1 | Base Frame | roof-tile-press-base-frame | 1× | 1 | · | part |
| 1.2 | Head Beam | roof-tile-press-head-beam | 1× | 1 | · | part |
| 1.3 | Guide Column | roof-tile-press-guide-column | 4× | 4 | · | part |
| 1.4 | Bed Plate | roof-tile-press-bed-plate | 1× | 1 | · | part |
| 1.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Pressing Ram 5 parts | roof-tile-press-ram | 1× | 1 | 12 | assembly |
| 2.1 | Main Cylinder 4 parts | roof-tile-press-main-cylinder | 1× | 1 | 4 | assembly |
| 2.1.1 | Cylinder Tube | roof-tile-press-cylinder-tube | 1× | 1 | · | part |
| 2.1.2 | Piston Rod | roof-tile-press-cylinder-rod | 1× | 1 | · | part |
| 2.1.3 | Piston Seal Kit | roof-tile-press-piston-seal | 1× | 1 | · | part |
| 2.1.4 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 2.2 | Moving Platen | roof-tile-press-platen | 1× | 1 | · | part |
| 2.3 | Guide Bush | roof-tile-press-guide-bush | 4× | 4 | · | part |
| 2.4 | Upper Mould Mount | roof-tile-press-upper-mould-mount | 1× | 1 | · | part |
| 2.5 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 3 | Mould Set 4 parts | roof-tile-press-mould-set | 1× | 1 | 12 | assembly |
| 3.1 | Upper Mould | roof-tile-press-upper-mould | 1× | 1 | · | part |
| 3.2 | Lower Mould | roof-tile-press-lower-mould | 1× | 1 | · | part |
| 3.3 | Tile Pallet | roof-tile-press-pallet | 8× | 8 | · | part |
| 3.4 | Interlock Insert | roof-tile-press-interlock-insert | 2× | 2 | · | part |
| 4 | Feed System 5 parts | roof-tile-press-feed-system | 1× | 1 | 5 | assembly |
| 4.1 | Mix Hopper | roof-tile-press-hopper | 1× | 1 | · | part |
| 4.2 | Dosing Slide | roof-tile-press-dosing-slide | 1× | 1 | · | part |
| 4.3 | Feed Cylinder | roof-tile-press-feed-cylinder | 1× | 1 | · | part |
| 4.4 | Scraper | roof-tile-press-scraper | 1× | 1 | · | part |
| 4.5 | Feed Belt | roof-tile-press-feed-belt | 1× | 1 | · | part |
| 5 | Hydraulic Power Pack 7 parts | roof-tile-press-hydraulic-unit | 1× | 1 | 36 | assembly |
| 5.1 | Hydraulic Pump | roof-tile-press-hyd-pump | 1× | 1 | · | part |
| 5.2 | Pump Motor 4 parts | roof-tile-press-hyd-motor | 1× | 1 | 25 | assembly |
| 5.2.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 5.2.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 5.2.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 5.2.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 5.3 | Oil Tank | roof-tile-press-oil-tank | 1× | 1 | · | part |
| 5.4 | Valve Block 3 parts | roof-tile-press-valve-block | 1× | 1 | 5 | assembly |
| 5.4.1 | Directional Valve | roof-tile-press-directional-valve | 3× | 3 | · | part |
| 5.4.2 | Relief Valve | roof-tile-press-relief-valve | 1× | 1 | · | part |
| 5.4.3 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 5.5 | Accumulator | roof-tile-press-accumulator | 1× | 1 | · | part |
| 5.6 | Oil Cooler | roof-tile-press-oil-cooler | 1× | 1 | · | part |
| 5.7 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 6 | Demoulding Unit 5 parts | roof-tile-press-demould | 1× | 1 | 9 | assembly |
| 6.1 | Ejector | roof-tile-press-ejector | 1× | 1 | · | part |
| 6.2 | Pallet Conveyor | roof-tile-press-pallet-conveyor | 1× | 1 | · | part |
| 6.3 | Pickup Arm | roof-tile-press-pickup | 1× | 1 | · | part |
| 6.4 | Drive Belt | drive-belt | 2× | 2 | · | part |
| 6.5 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 7 | Control Cabinet 7 parts | roof-tile-press-control | 1× | 1 | 350 | assembly |
| 7.1 | PLC 3 parts | roof-tile-press-plc | 1× | 1 | 143 | assembly |
| 7.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.1.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 7.1.3 | SMD Passive (R/C/L) | smd-passives | 140× | 140 | · | part |
| 7.2 | Operator Panel 4 parts | roof-tile-press-hmi | 1× | 1 | 83 | assembly |
| 7.2.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.2.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.2.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.2.4 | SMD Passive (R/C/L) | smd-passives | 80× | 80 | · | part |
| 7.3 | Variable Frequency Drive 4 parts | roof-tile-press-vfd | 1× | 1 | 94 | assembly |
| 7.3.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.3.2 | IGBT Power Module | igbt-module | 1× | 1 | · | part |
| 7.3.3 | DC-Link Capacitor | dc-link-cap | 2× | 2 | · | part |
| 7.3.4 | SMD Passive (R/C/L) | smd-passives | 90× | 90 | · | part |
| 7.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.5 | Relay | relay | 8× | 8 | · | part |
| 7.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 7.7 | Connector | connector | 20× | 20 | · | part |
| 8 | Vibration Table 4 parts | roof-tile-press-vibration | 1× | 1 | 11 | assembly |
| 8.1 | Vibrator | roof-tile-press-vibrator | 2× | 2 | · | part |
| 8.2 | Isolation Mount | roof-tile-press-vibration-mount | 4× | 4 | · | part |
| 8.3 | Table Plate | roof-tile-press-table-plate | 1× | 1 | · | part |
| 8.4 | Coil Spring | coil-spring | 4× | 4 | · | part |
Related products
same domain, ranked by shared parts Fiber Cement Sheet Machine
819 parts · shares 21 with this page
Insulated Sandwich Panel Line
1,856 parts · shares 20 with this page
Metal Roofing Roll Former
704 parts · shares 18 with this page
 Precast Concrete Mold
493 parts · shares 17 with this page
 Hollowcore Slab Extruder
547 parts · shares 15 with this page
 Geomembrane Welding Machine
273 parts · shares 15 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $50–$10k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| assaabloy.com ↗ | Stockholm, SE | Locks & access | 1,000 units | 8–12 wks |
|
🇺🇸Allegion
allegion.com ↗
|
Dublin, US | Security products (Schlage) | 1,000 units | 8–12 wks |
| dormakaba.com ↗ | Rümlang, CH | Access & door systems | 1,000 units | 8–12 wks |
| honeywell.com ↗ | Charlotte, US | Building & safety tech | 1,000 units | 8–12 wks |
| hikvision.com ↗ | Hangzhou, CN | Surveillance & security | 1,000 units | 8–12 wks |
957-word article