Paving Block Machine
ProductOverview
A paving block machine presses interlocking concrete pavers, kerbs, and hollow blocks from a stiff, almost dry concrete mix. The mix has near zero slump, so the block holds its shape the instant the mould lifts and can be carried away green on a pallet straight after pressing. That immediate demould is what makes the machine fast: it turns out a full board of blocks every 15 to 25 seconds rather than waiting on any cure. Strength and density come from combining heavy vibration with hydraulic pressure, which drives the aggregate into tight contact and forces out trapped air while the cement is still loose.
The machine is built around a Machine Frame that carries the press loads, a Mould and Tamper Set and tamper set that shapes the block, a Vibration Table table that compacts the concrete, a Concrete Feed System that fills the cavities, a Pallet Handling handler that moves the production boards, a Hydraulic Power Unit unit that powers every stroke, a Control System system that sequences the cycle, and an optional Face Mix Unit unit that lays a coloured wear surface.
Mould and tamper
Every block is shaped between two tools. The Mould Box holds a Cavity Insert that sets the block pattern, so the same machine runs pavers one day and hollow blocks the next once the insert and the matching Tamper Head are changed. The tamper carries a Tamper Shoe for each cavity that forms the top face and takes the press wear, and a Stripper Shoe that pushes the green block down out of the box on the demould stroke. Mould steel is hardened and ground, because grit-laden concrete wears the cavity fast and any worn edge prints onto thousands of blocks. A Mould Wear Plate protects the box at the pallet face where abrasion is worst.
Vibration and pressing
Dry-cast concrete will not flow, so it has to be shaken and squeezed into place at the same time. The Vibration Table table carries a pair of Eccentric Exciter units, each an eccentric mass spun by a Exciter Motor on a hardened Exciter Shaft. The two exciters are timed so their horizontal forces cancel and only a strong vertical shake reaches the mould. The shafts run on sealed Ball Bearing sets behind an Oil Seal at each end, since dust and grout destroy an open bearing in days. The table sits on a Isolation Mount set of rubber springs that let it vibrate freely while keeping the shock out of the frame. As the table shakes, the hydraulic tamper presses down from above, so the block is compacted from both faces at once.
Feeding and pallets
Concrete reaches the mould through the Concrete Feed System system. A Charging Conveyor delivers mix from the batching plant into the Feed Hopper, and a Feeder Drawer shuttles forward over the open mould to drop a measured charge, then scrapes the top level on the way back. A Drawer Agitator grid rakes the concrete in the drawer so every cavity fills to the same weight, which is what keeps block height consistent. Each cycle starts with the Pallet Handling handler: a Pallet Feeder draws an empty board from the Pallet Magazine and sets it on the table, and after demould a Board Pusher ejects the loaded board onto the take-off conveyor.
Hydraulics and control
The Hydraulic Power Unit unit supplies the muscle. Its Hydraulic Pump draws from the Oil Tank and feeds a Valve Block that routes oil to the Tamper Cylinder that presses the block and the Mould Lift Cylinder units that lift the box on demould. An Accumulator stores energy for the fast press stroke, a Oil Cooler holds the oil temperature steady under continuous duty, and a full O-Ring Set keeps the system tight. Sequencing comes from the Control System cabinet, where a PLC reads several Pressure Sensor inputs and a set of Proximity Switch units that confirm drawer, mould, and pallet positions before each step. The operator picks a recipe at the Operator Panel, and a Variable Frequency Drive ramps the exciter frequency to tune compaction.
Face mix and use
For coloured pavers the Face Mix Unit unit lays a thin layer of fine pigmented concrete on top of the base block just before the tamper presses. A Metering Screw meters mix from the Face Mix Hopper and the Face Mix Drawer spreads it even, so the wear surface and colour sit in a layer a few millimetres thick over a cheaper grey core. The finished blocks go to municipal paving, driveways, walkways, and kerb lines, where buyers want square edges, consistent height, and the crush strength that comes from dense compaction. Output is limited by curing yard space and the take-off line, not by the press, since the mould is free again the moment each board lifts away.
Paving Block Machine parts and their functions
8 top-level parts · 154 parts in total · full bill of materials below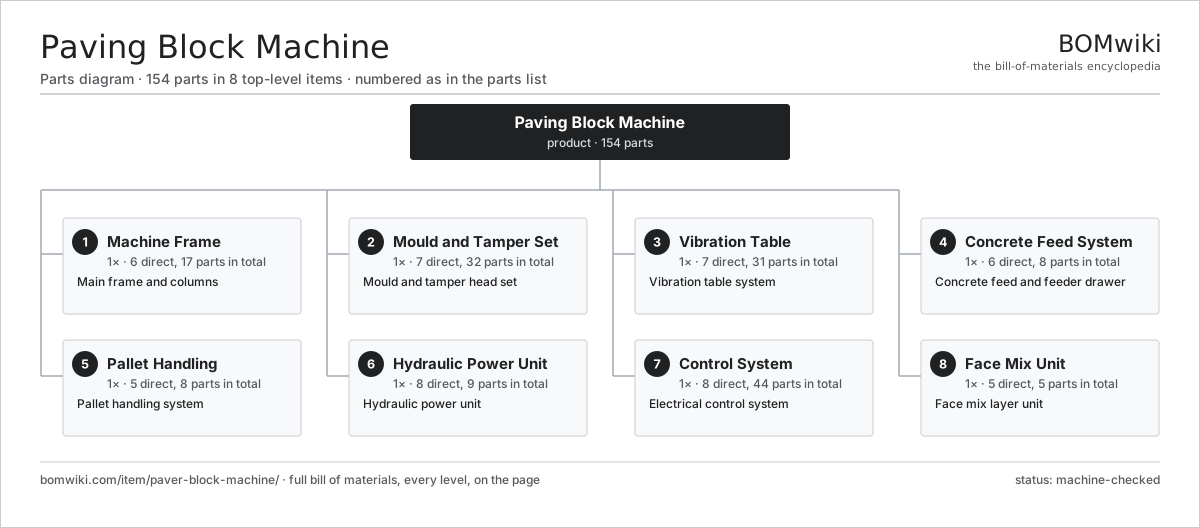
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Machine Frame 6 parts | 1× | Main frame and columns |
| 2 | Mould and Tamper Set 7 parts | 1× | Mould and tamper head set |
| 3 | Vibration Table 7 parts | 1× | Vibration table system |
| 4 | Concrete Feed System 6 parts | 1× | Concrete feed and feeder drawer |
| 5 | Pallet Handling 5 parts | 1× | Pallet handling system |
| 6 | Hydraulic Power Unit 8 parts | 1× | Hydraulic power unit |
| 7 | Control System 8 parts | 1× | Electrical control system |
| 8 | Face Mix Unit 5 parts | 1× | Face mix layer unit |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Paving Block Machine
8 top-level lines · 67 rows shown · 154 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Machine Frame 6 parts | paver-block-machine-frame | 1× | 1 | 17 | assembly |
| 1.1 | Base Frame | paver-block-machine-base-frame | 1× | 1 | · | part |
| 1.2 | Guide Column | paver-block-machine-column | 4× | 4 | · | part |
| 1.3 | Upper Crosshead | paver-block-machine-crosshead | 1× | 1 | · | part |
| 1.4 | Guide Bushing | paver-block-machine-guide-bush | 8× | 8 | · | part |
| 1.5 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 1.6 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Mould and Tamper Set 7 parts | paver-block-machine-mould | 1× | 1 | 32 | assembly |
| 2.1 | Mould Box | paver-block-machine-mould-box | 1× | 1 | · | part |
| 2.2 | Cavity Insert | paver-block-machine-cavity-insert | 1× | 1 | · | part |
| 2.3 | Tamper Head | paver-block-machine-tamper-head | 1× | 1 | · | part |
| 2.4 | Tamper Shoe | paver-block-machine-tamper-shoe | 12× | 12 | · | part |
| 2.5 | Stripper Shoe | paver-block-machine-stripper-shoe | 12× | 12 | · | part |
| 2.6 | Mould Carrier Frame | paver-block-machine-mould-frame | 1× | 1 | · | part |
| 2.7 | Mould Wear Plate | paver-block-machine-wear-plate | 4× | 4 | · | part |
| 3 | Vibration Table 7 parts | paver-block-machine-vibration | 1× | 1 | 31 | assembly |
| 3.1 | Vibration Table Plate | paver-block-machine-vib-table | 1× | 1 | · | part |
| 3.2 | Eccentric Exciter | paver-block-machine-exciter | 2× | 2 | · | part |
| 3.3 | Exciter Shaft | paver-block-machine-exciter-shaft | 2× | 2 | · | part |
| 3.4 | Exciter Motor | paver-block-machine-vib-motor | 2× | 2 | · | part |
| 3.5 | Isolation Mount | paver-block-machine-vib-mount | 8× | 8 | · | part |
| 3.6 | Ball Bearing | ball-bearing | 8× | 8 | · | part |
| 3.7 | Oil Seal | oil-seal | 8× | 8 | · | part |
| 4 | Concrete Feed System 6 parts | paver-block-machine-feed | 1× | 1 | 8 | assembly |
| 4.1 | Feed Hopper | paver-block-machine-feed-hopper | 1× | 1 | · | part |
| 4.2 | Feeder Drawer | paver-block-machine-feeder-drawer | 1× | 1 | · | part |
| 4.3 | Drawer Agitator | paver-block-machine-agitator | 1× | 1 | · | part |
| 4.4 | Drawer Cylinder | paver-block-machine-feed-cylinder | 2× | 2 | · | part |
| 4.5 | Charging Conveyor | paver-block-machine-conveyor | 1× | 1 | · | part |
| 4.6 | Drive Belt | drive-belt | 2× | 2 | · | part |
| 5 | Pallet Handling 5 parts | paver-block-machine-pallet | 1× | 1 | 8 | assembly |
| 5.1 | Pallet Magazine | paver-block-machine-pallet-magazine | 1× | 1 | · | part |
| 5.2 | Pallet Feeder | paver-block-machine-pallet-feeder | 1× | 1 | · | part |
| 5.3 | Board Pusher | paver-block-machine-pallet-pusher | 1× | 1 | · | part |
| 5.4 | Roller Track | paver-block-machine-roller-track | 1× | 1 | · | part |
| 5.5 | Coil Spring | coil-spring | 4× | 4 | · | part |
| 6 | Hydraulic Power Unit 8 parts | paver-block-machine-hydraulic | 1× | 1 | 9 | assembly |
| 6.1 | Oil Tank | paver-block-machine-hpu-tank | 1× | 1 | · | part |
| 6.2 | Hydraulic Pump | paver-block-machine-hpu-pump | 1× | 1 | · | part |
| 6.3 | Valve Block | paver-block-machine-valve-block | 1× | 1 | · | part |
| 6.4 | Tamper Cylinder | paver-block-machine-tamper-cylinder | 1× | 1 | · | part |
| 6.5 | Mould Lift Cylinder | paver-block-machine-mould-cylinder | 2× | 2 | · | part |
| 6.6 | Accumulator | paver-block-machine-accumulator | 1× | 1 | · | part |
| 6.7 | Oil Cooler | paver-block-machine-cooler | 1× | 1 | · | part |
| 6.8 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 7 | Control System 8 parts | paver-block-machine-control | 1× | 1 | 44 | assembly |
| 7.1 | PLC 4 parts | paver-block-machine-plc | 1× | 1 | 10 | assembly |
| 7.1.1 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.1.2 | Bare PCB | pcb-bare | 2× | 2 | · | part |
| 7.1.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 7.1.4 | Relay | relay | 6× | 6 | · | part |
| 7.2 | Operator Panel 3 parts | paver-block-machine-hmi | 1× | 1 | 4 | assembly |
| 7.2.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.2.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.2.3 | Connector | connector | 2× | 2 | · | part |
| 7.3 | Motor Contactor | paver-block-machine-contactor | 6× | 6 | · | part |
| 7.4 | Variable Frequency Drive | paver-block-machine-vfd | 2× | 2 | · | part |
| 7.5 | Pressure Sensor | pressure-sensor | 3× | 3 | · | part |
| 7.6 | Proximity Switch | paver-block-machine-prox-switch | 8× | 8 | · | part |
| 7.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 7.8 | Connector | connector | 10× | 10 | · | part |
| 8 | Face Mix Unit 5 parts | paver-block-machine-facemix | 1× | 1 | 5 | assembly |
| 8.1 | Face Mix Hopper | paver-block-machine-facemix-hopper | 1× | 1 | · | part |
| 8.2 | Face Mix Drawer | paver-block-machine-facemix-drawer | 1× | 1 | · | part |
| 8.3 | Face Mix Cylinder | paver-block-machine-facemix-cylinder | 1× | 1 | · | part |
| 8.4 | Metering Screw | paver-block-machine-facemix-screw | 1× | 1 | · | part |
| 8.5 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Clay Brick Extruder
154 parts · shares 11 with this page
Concrete Pipe Making Machine
154 parts · shares 11 with this page
 Fiber Cement Sheet Machine
819 parts · shares 11 with this page
 AAC Block Plant
155 parts · shares 10 with this page
 Gypsum Board Production Line
207 parts · shares 10 with this page
Insulated Sandwich Panel Line
1,856 parts · shares 10 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $50–$10k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| assaabloy.com ↗ | Stockholm, SE | Locks & access | 1,000 units | 8–12 wks |
|
🇺🇸Allegion
allegion.com ↗
|
Dublin, US | Security products (Schlage) | 1,000 units | 8–12 wks |
| dormakaba.com ↗ | Rümlang, CH | Access & door systems | 1,000 units | 8–12 wks |
| honeywell.com ↗ | Charlotte, US | Building & safety tech | 1,000 units | 8–12 wks |
| hikvision.com ↗ | Hangzhou, CN | Surveillance & security | 1,000 units | 8–12 wks |
913-word article