Gypsum Board Production Line
ProductOverview
A gypsum board production line turns powdered calcined gypsum, water and two paper webs into finished wallboard in one continuous run. Stucco and gauge water meet in a fast mixer, the slurry is sandwiched between a face and a back paper, and the ribbon of wet board travels along a setting belt while the gypsum rehydrates and stiffens. A flying knife cuts the ribbon into panels, a dryer drives off the water left over from mixing, and the dry boards are trimmed, printed and bundled. The line runs without stopping for hours at a time, so every station has to hold its setpoint while the board moves under it at up to 200 metres per minute.
The line is organized as a wet end and a dry end. The wet end covers the Stucco and Slurry System system, the Forming Station, the Setting Belt and the Wet Cut-off Knife. The dry end covers the Wet Transfer and Turnover, the Board Dryer and the Finishing Section section. A Line Control System system ties the two ends together so the whole line behaves as a single speed-locked machine.
Mixing the slurry
Board quality starts in the Stucco and Slurry System system. Calcined stucco sits in a Stucco Surge Bin and is metered out by a pair of Stucco Screw Feeder units that weigh the mass flow as they run. Tempered water comes from the Gauge Water Skid, where a Gauge Water Pump and a Magnetic Flow Meter hold the water-to-stucco ratio, the single number that most affects board weight and strength. A Foam Generator whips foaming agent into stable bubbles that lower the finished density without weakening the core, and several Additive Metering Pump units dose accelerator, retarder and starch in small amounts. All of it enters the Pin Mixer, whose Pinned Rotor Disc spins on a hardened Mixer Drive Shaft driven by the Mixer Drive Motor. The mix spends less than two seconds in the mixer because gypsum starts to set the moment it gets wet, so the slurry must reach the paper before it stiffens. The blended slurry leaves through the Slurry Canister, which splits it into a face stream and a core stream.
Forming the board
In the Forming Station the slurry is laid onto a moving paper web. Two Paper Unwind Stand units pay out the face and back papers under steady tension, each with a Reel Shaft, a Dancer Tension Roll and a Flying Splicer that joins a fresh reel without stopping the line. A Face Paper Creaser scores the face paper so it folds cleanly around the edges, and a Roll Coater skims slurry onto the back paper for bond. The slurry pours onto the face paper, the back paper drops on top, and the sandwich passes under the Forming Plate that sets the wet thickness. A pair of Edge Forming Guide units fold the face paper to form the long edges, square or tapered depending on the product, and the Master Forming Roll pulls the wrapped board out at line speed.
Setting and cutting
The board is still soft when it leaves the former, so it rides the Setting Belt, a conveyor a hundred metres or more long. The Conveyor Belt runs on dozens of Idler Roll supports and is driven by the Belt Drive Pulley through a Helical Gear Pair in a Gearbox Housing, with a Belt Tracking Unit unit keeping the wide belt centered. Over this distance the gypsum crystals interlock and the board gains enough green strength to be cut and handled. At the end of the belt the Wet Cut-off Knife cuts the ribbon into panels. Its Flying Carriage rides on a Linear Guide Rail pair, driven by a Carriage Servo Drive and a Ball Screw, and matches line speed so the Cut-off Blade cuts square ends while the board keeps moving. A Length Encoder on a measuring wheel triggers each cut at the ordered length.
Drying
Cut panels still hold the free water that was added for mixing, so they go through the Board Dryer. First the Wet Transfer and Turnover section opens gaps with Accelerating Belt runs and uses a Board Turnover to flip panels so their good faces stay clean. The dryer stacks several Dryer Deck conveyors so many boards dry at once in a short building. A Air Heater Burner heats the air through a Heat Exchanger kept safe by its Gas Safety Train, Circulation Fan units blow it across the boards, and Exhaust Fan units pull the moist air out. The dryer runs hot at the inlet and cooler toward the outlet so the board does not overheat once its surface is dry, since driving the temperature too high would calcine the gypsum back to powder and ruin the panel. A Pressure Sensor watches gas and air pressure throughout.
Finishing and use
At the dry end the Finishing Section section squares the panels with an End Trim Saw pair, marks them with the Back Printer, and pairs them good face out at the Board Bundler before a Bundle Taper and a Stacker make them ready for the forklift. The whole run is coordinated by the Line Control System cabinet, where a Line PLC keeps every Conveyor Drive locked to the master speed and a Operator Station lets the operator load a product recipe.
Standard wallboard suits walls and ceilings; variants change the additives and paper for moisture resistance, fire rating or impact strength, but the line stays the same. Because the process is continuous and the gypsum cures in minutes, a single line supplies tens of millions of square metres a year for the drywall that most interior partitions are built from.
Gypsum Board Production Line parts and their functions
8 top-level parts · 207 parts in total · full bill of materials below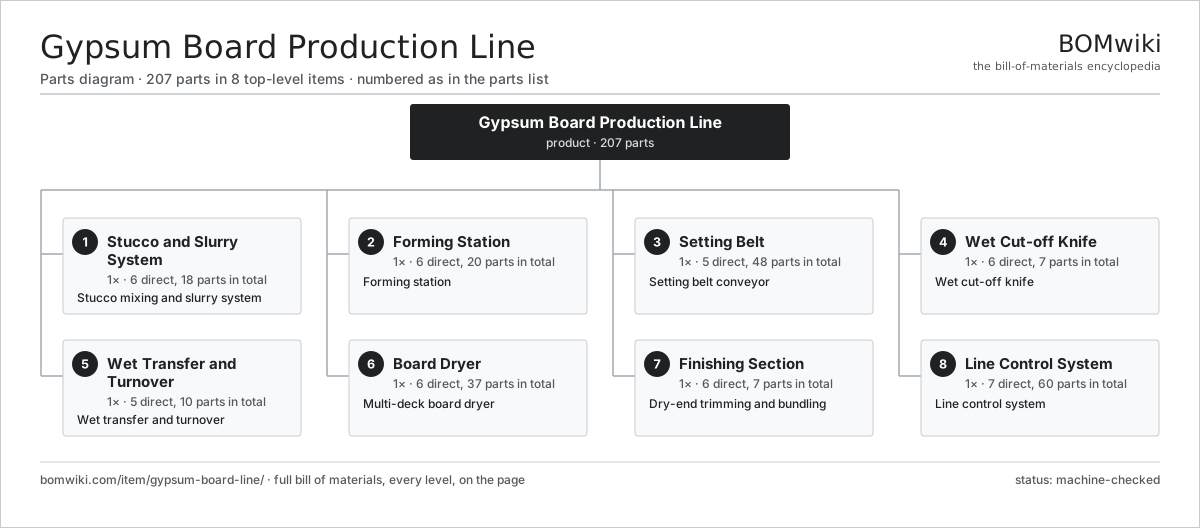
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Stucco and Slurry System 6 parts | 1× | Stucco mixing and slurry system |
| 2 | Forming Station 6 parts | 1× | Forming station |
| 3 | Setting Belt 5 parts | 1× | Setting belt conveyor |
| 4 | Wet Cut-off Knife 6 parts | 1× | Wet cut-off knife |
| 5 | Wet Transfer and Turnover 5 parts | 1× | Wet transfer and turnover |
| 6 | Board Dryer 6 parts | 1× | Multi-deck board dryer |
| 7 | Finishing Section 6 parts | 1× | Dry-end trimming and bundling |
| 8 | Line Control System 7 parts | 1× | Line control system |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model. STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Gypsum Board Production Line
8 top-level lines · 84 rows shown · 207 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Stucco and Slurry System 6 parts | gypsum-board-line-slurry | 1× | 1 | 18 | assembly |
| 1.1 | Stucco Surge Bin | gypsum-board-line-stucco-bin | 1× | 1 | · | part |
| 1.2 | Stucco Screw Feeder | gypsum-board-line-screw-feeder | 2× | 2 | · | part |
| 1.3 | Gauge Water Skid 3 parts | gypsum-board-line-water-skid | 1× | 1 | 3 | assembly |
| 1.3.1 | Gauge Water Pump | gypsum-board-line-water-pump | 1× | 1 | · | part |
| 1.3.2 | Magnetic Flow Meter | gypsum-board-line-flow-meter | 1× | 1 | · | part |
| 1.3.3 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 1.4 | Foam Generator | gypsum-board-line-foam-gen | 1× | 1 | · | part |
| 1.5 | Pin Mixer 6 parts | gypsum-board-line-pin-mixer | 1× | 1 | 8 | assembly |
| 1.5.1 | Pinned Rotor Disc | gypsum-board-line-mixer-disc | 1× | 1 | · | part |
| 1.5.2 | Mixer Drive Shaft | gypsum-board-line-mixer-shaft | 1× | 1 | · | part |
| 1.5.3 | Mixer Drive Motor | gypsum-board-line-mixer-motor | 1× | 1 | · | part |
| 1.5.4 | Slurry Canister | gypsum-board-line-canister | 1× | 1 | · | part |
| 1.5.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 1.5.6 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 1.6 | Additive Metering Pump | gypsum-board-line-additive-pump | 3× | 3 | · | part |
| 2 | Forming Station 6 parts | gypsum-board-line-former | 1× | 1 | 20 | assembly |
| 2.1 | Paper Unwind Stand 4 parts | gypsum-board-line-paper-stand | 2× | 2 | 7 | assembly |
| 2.1.1 | Reel Shaft | gypsum-board-line-reel-shaft | 1× | 2 | · | part |
| 2.1.2 | Dancer Tension Roll | gypsum-board-line-tension-roll | 1× | 2 | · | part |
| 2.1.3 | Flying Splicer | gypsum-board-line-splicer | 1× | 2 | · | part |
| 2.1.4 | Ball Bearing | ball-bearing | 4× | 8 | · | part |
| 2.2 | Face Paper Creaser | gypsum-board-line-creaser | 1× | 1 | · | part |
| 2.3 | Forming Plate | gypsum-board-line-forming-plate | 1× | 1 | · | part |
| 2.4 | Roll Coater | gypsum-board-line-roll-coater | 1× | 1 | · | part |
| 2.5 | Edge Forming Guide | gypsum-board-line-edge-guide | 2× | 2 | · | part |
| 2.6 | Master Forming Roll | gypsum-board-line-master-roll | 1× | 1 | · | part |
| 3 | Setting Belt 5 parts | gypsum-board-line-setting-belt | 1× | 1 | 48 | assembly |
| 3.1 | Conveyor Belt | gypsum-board-line-belt | 1× | 1 | · | part |
| 3.2 | Belt Drive Pulley 4 parts | gypsum-board-line-belt-drive | 1× | 1 | 5 | assembly |
| 3.2.1 | Head Pulley | gypsum-board-line-head-pulley | 1× | 1 | · | part |
| 3.2.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 3.2.3 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 3.2.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3.3 | Idler Roll | gypsum-board-line-idler-roll | 40× | 40 | · | part |
| 3.4 | Belt Tracking Unit | gypsum-board-line-tracking | 1× | 1 | · | part |
| 3.5 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 4 | Wet Cut-off Knife 6 parts | gypsum-board-line-knife | 1× | 1 | 7 | assembly |
| 4.1 | Cut-off Blade | gypsum-board-line-knife-blade | 1× | 1 | · | part |
| 4.2 | Flying Carriage | gypsum-board-line-knife-carriage | 1× | 1 | · | part |
| 4.3 | Carriage Servo Drive | gypsum-board-line-knife-servo | 1× | 1 | · | part |
| 4.4 | Length Encoder | gypsum-board-line-length-encoder | 1× | 1 | · | part |
| 4.5 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 4.6 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 5 | Wet Transfer and Turnover 5 parts | gypsum-board-line-transfer | 1× | 1 | 10 | assembly |
| 5.1 | Accelerating Belt | gypsum-board-line-accel-belt | 3× | 3 | · | part |
| 5.2 | Board Turnover | gypsum-board-line-turnover | 1× | 1 | · | part |
| 5.3 | Synchronizing Belt | gypsum-board-line-synchro-belt | 1× | 1 | · | part |
| 5.4 | Booking Station | gypsum-board-line-booking | 1× | 1 | · | part |
| 5.5 | Drive Belt | drive-belt | 4× | 4 | · | part |
| 6 | Board Dryer 6 parts | gypsum-board-line-dryer | 1× | 1 | 37 | assembly |
| 6.1 | Dryer Deck | gypsum-board-line-dryer-deck | 8× | 8 | · | part |
| 6.2 | Air Heater Burner 4 parts | gypsum-board-line-burner | 2× | 2 | 4 | assembly |
| 6.2.1 | Burner Head | gypsum-board-line-burner-head | 1× | 2 | · | part |
| 6.2.2 | Gas Safety Train | gypsum-board-line-gas-train | 1× | 2 | · | part |
| 6.2.3 | Heat Exchanger | gypsum-board-line-heat-exch | 1× | 2 | · | part |
| 6.2.4 | Heating Element | heating-element | 1× | 2 | · | part |
| 6.3 | Circulation Fan | gypsum-board-line-circ-fan | 6× | 6 | · | part |
| 6.4 | Exhaust Fan | gypsum-board-line-exhaust-fan | 2× | 2 | · | part |
| 6.5 | Dryer Roller Conveyor | gypsum-board-line-roller-conveyor | 1× | 1 | · | part |
| 6.6 | Zone Damper | gypsum-board-line-zone-damper | 12× | 12 | · | part |
| 7 | Finishing Section 6 parts | gypsum-board-line-finishing | 1× | 1 | 7 | assembly |
| 7.1 | End Trim Saw | gypsum-board-line-end-saw | 2× | 2 | · | part |
| 7.2 | Back Printer | gypsum-board-line-printer | 1× | 1 | · | part |
| 7.3 | Board Bundler | gypsum-board-line-bundler | 1× | 1 | · | part |
| 7.4 | Bundle Taper | gypsum-board-line-taper | 1× | 1 | · | part |
| 7.5 | Stacker | gypsum-board-line-stacker | 1× | 1 | · | part |
| 7.6 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 8 | Line Control System 7 parts | gypsum-board-line-control | 1× | 1 | 60 | assembly |
| 8.1 | Line PLC 4 parts | gypsum-board-line-plc | 1× | 1 | 13 | assembly |
| 8.1.1 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.1.2 | Bare PCB | pcb-bare | 3× | 3 | · | part |
| 8.1.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 8.1.4 | Relay | relay | 8× | 8 | · | part |
| 8.2 | Operator Station 4 parts | gypsum-board-line-hmi | 1× | 1 | 6 | assembly |
| 8.2.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.2.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.2.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.2.4 | Connector | connector | 3× | 3 | · | part |
| 8.3 | Conveyor Drive | gypsum-board-line-vfd | 8× | 8 | · | part |
| 8.4 | Dryer Thermocouple | gypsum-board-line-temp-sensor | 12× | 12 | · | part |
| 8.5 | Pressure Sensor | pressure-sensor | 4× | 4 | · | part |
| 8.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8.7 | Connector | connector | 16× | 16 | · | part |
Related products
same domain, ranked by shared parts Precast Concrete Mold
493 parts · shares 11 with this page
 AAC Block Plant
155 parts · shares 12 with this page
 Clay Brick Extruder
154 parts · shares 12 with this page
 Fiber Cement Sheet Machine
819 parts · shares 12 with this page
Concrete Pipe Making Machine
154 parts · shares 10 with this page
Sourcing: possible vendors
Browse the supplier directory → Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $50–$10k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| assaabloy.com ↗ | Stockholm, SE | Locks & access | 1,000 units | 8–12 wks |
|
🇺🇸Allegion
allegion.com ↗
|
Dublin, US | Security products (Schlage) | 1,000 units | 8–12 wks |
| dormakaba.com ↗ | Rümlang, CH | Access & door systems | 1,000 units | 8–12 wks |
| honeywell.com ↗ | Charlotte, US | Building & safety tech | 1,000 units | 8–12 wks |
| hikvision.com ↗ | Hangzhou, CN | Surveillance & security | 1,000 units | 8–12 wks |
1,072-word article