Continuous Dough Divider
ProductOverview
A continuous dough divider portions a bulk mass of mixed dough into pieces of uniform weight, the first shaping step after mixing in a bread line. Accurate dividing matters for two reasons: the bakery sells bread by count but is governed on minimum weight, so light pieces risk regulatory trouble while heavy pieces give away product. The divider must hit a target piece weight closely, piece after piece, while handling dough gently so it does not crush out the gas already developed in the mixer. The machine described here is a volumetric suction divider, which fills a measuring pocket by gentle vacuum and then crops the measured slug, a method kinder to the dough than the high-pressure ram dividers it replaced.
The divider works as a cycle of fill, measure, cut, and discharge. The Dough Hopper holds the bulk dough, the Feed and Suction draws it into the Measuring Chamber by suction, the Cutting Mechanism crops each slug, and the piece drops to the Frame and Outfeed outfeed. A Flour Duster duster and a Oil Lubrication system keep the dough from sticking, the Drive System times everything, and the Control System holds the weight.
Gentle feed
Dough reaches the divider full of gas from fermentation, and the divider's job is to portion it without knocking that gas out. The Dough Hopper holds a working stock in a stainless Hopper Shell, and slow Feed Roller rollers draw dough downward without crushing it. A Hopper Gate sets how much dough is presented, and a Level Sensor tells the operator when to refill. From there the Feed and Suction uses a Feed Piston working with light suction from a Vacuum Pump to draw dough into the measuring pocket. Filling by suction rather than by force is what protects the dough structure.
Volumetric measuring
The divider portions by volume, not by weight directly, because weighing each piece would be too slow. The Measuring Chamber holds a set of Measuring Pocket pockets in a turning Pocket Block. Each pocket fills to a volume set by its Volume Piston stroke, and that volume becomes one piece. Because the divider measures volume but the bakery cares about weight, the operator sets the Volume Adjuster adjuster to dial in piece weight, and the Control System trims it as dough density drifts through a run. Dough density changes with temperature, hydration, and how long it has rested, so continuous weight trimming is what keeps the pieces on target.
Cutting and discharge
Once a pocket is full it must release a clean piece. The Cutting Mechanism mechanism shears the dough column at the pocket mouth with a Cutting Knife, then a Discharge Piston pushes the measured slug out onto the belt. A Timing Cam times the fill, cut, and discharge so they happen in the right order as the block indexes. The cut and the discharge are the moments where dough is most likely to stick, which is why lubrication and dusting are built in around them.
Anti-stick: flour and oil
Bread dough is sticky, and a divider that smears would lose accuracy and need constant cleaning. Two systems keep surfaces clean. The Flour Duster duster lays a thin film of flour on the contact faces with a Dusting Brush fed from a Flour Hopper, so dough releases instead of clinging. The Oil Lubrication system sprays a fine food-grade oil mist through Oil Nozzle nozzles onto the pistons and knife, both to release dough and to slow wear on the moving metal. Together they let the divider run long shifts at steady weight.
Drive and control
Timing is everything in a divider, so the Drive System uses a Main Servo Motor servo to index the pocket block and synchronize the machine with the outfeed and the rounder beyond it. The Control System cabinet runs the sequence from a PLC Controller, sets the rate through a Drive (VFD) drive, and presents piece weight and count on a Operator Panel (HMI) panel. Operators set a target weight and a rate in pieces per minute, and the machine holds both, logging counts for the production record.
Place in the line and construction
The divider sits between the mixer and the rounder. It receives mixed and rested dough, portions it, and drops uniform pieces onto its Outfeed Belt for the rounder to shape. Because it handles food and runs all day, the whole machine is stainless steel for washdown, carried on a welded Base Frame with Sheet Metal Panel guards and Guard Interlock interlocks. Its accuracy and gentleness set the quality of every loaf downstream: uniform weight keeps bake times consistent, and preserved gas structure keeps the crumb open, so the divider is tuned carefully whenever dough or product changes.
Continuous Dough Divider parts and their functions
9 top-level parts · 270 parts in total · full bill of materials below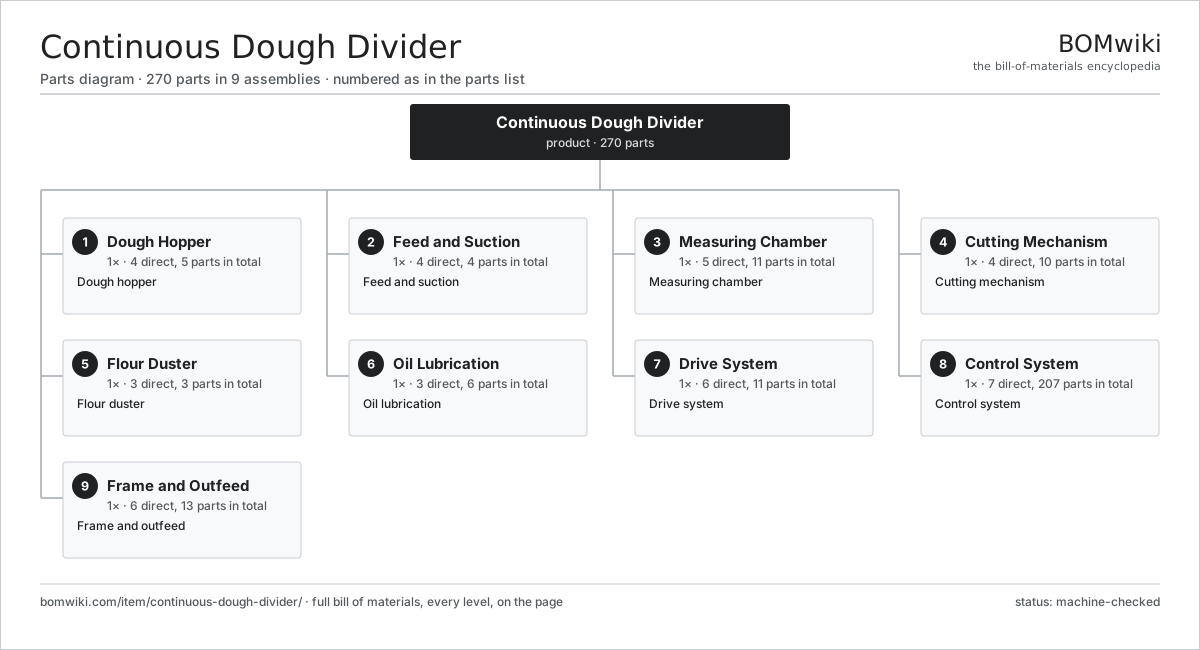
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Dough Hopper 4 parts | 1× | Dough hopper |
| 2 | Feed and Suction 4 parts | 1× | Feed and suction |
| 3 | Measuring Chamber 5 parts | 1× | Measuring chamber |
| 4 | Cutting Mechanism 4 parts | 1× | Cutting mechanism |
| 5 | Flour Duster 3 parts | 1× | Flour duster |
| 6 | Oil Lubrication 3 parts | 1× | Oil lubrication |
| 7 | Drive System 6 parts | 1× | Drive system |
| 8 | Control System 7 parts | 1× | Control system |
| 9 | Frame and Outfeed 6 parts | 1× | Frame and outfeed |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Continuous Dough Divider
9 top-level lines · 58 rows shown · 270 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Dough Hopper 4 parts | continuous-dough-divider-hopper | 1× | 1 | 5 | assembly |
| 1.1 | Hopper Shell | continuous-dough-divider-hopper-shell | 1× | 1 | · | part |
| 1.2 | Feed Roller | continuous-dough-divider-feed-roller | 2× | 2 | · | part |
| 1.3 | Hopper Gate | continuous-dough-divider-hopper-gate | 1× | 1 | · | part |
| 1.4 | Level Sensor | continuous-dough-divider-level-sensor | 1× | 1 | · | part |
| 2 | Feed and Suction 4 parts | continuous-dough-divider-feed | 1× | 1 | 4 | assembly |
| 2.1 | Feed Piston | continuous-dough-divider-feed-piston | 1× | 1 | · | part |
| 2.2 | Suction Valve | continuous-dough-divider-suction-valve | 1× | 1 | · | part |
| 2.3 | Vacuum Pump | continuous-dough-divider-vacuum-pump | 1× | 1 | · | part |
| 2.4 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 3 | Measuring Chamber 5 parts | continuous-dough-divider-chamber | 1× | 1 | 11 | assembly |
| 3.1 | Measuring Pocket | continuous-dough-divider-pocket | 4× | 4 | · | part |
| 3.2 | Volume Piston | continuous-dough-divider-volume-piston | 4× | 4 | · | part |
| 3.3 | Volume Adjuster | continuous-dough-divider-volume-adjust | 1× | 1 | · | part |
| 3.4 | Pocket Block | continuous-dough-divider-pocket-block | 1× | 1 | · | part |
| 3.5 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 4 | Cutting Mechanism 4 parts | continuous-dough-divider-knife | 1× | 1 | 10 | assembly |
| 4.1 | Cutting Knife | continuous-dough-divider-knife-blade | 1× | 1 | · | part |
| 4.2 | Discharge Piston | continuous-dough-divider-discharge-piston | 4× | 4 | · | part |
| 4.3 | Timing Cam | continuous-dough-divider-cam | 1× | 1 | · | part |
| 4.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 5 | Flour Duster 3 parts | continuous-dough-divider-flour | 1× | 1 | 3 | assembly |
| 5.1 | Flour Hopper | continuous-dough-divider-flour-hopper | 1× | 1 | · | part |
| 5.2 | Dusting Brush | continuous-dough-divider-flour-brush | 1× | 1 | · | part |
| 5.3 | Duster Motor | continuous-dough-divider-flour-motor | 1× | 1 | · | part |
| 6 | Oil Lubrication 3 parts | continuous-dough-divider-oil | 1× | 1 | 6 | assembly |
| 6.1 | Oil Pump | continuous-dough-divider-oil-pump | 1× | 1 | · | part |
| 6.2 | Oil Tank | continuous-dough-divider-oil-tank | 1× | 1 | · | part |
| 6.3 | Oil Nozzle | continuous-dough-divider-oil-nozzle | 4× | 4 | · | part |
| 7 | Drive System 6 parts | continuous-dough-divider-drive | 1× | 1 | 11 | assembly |
| 7.1 | Main Servo Motor | continuous-dough-divider-main-motor | 1× | 1 | · | part |
| 7.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 7.3 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 7.4 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 7.5 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 7.6 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 8 | Control System 7 parts | continuous-dough-divider-control | 1× | 1 | 207 | assembly |
| 8.1 | PLC Controller 3 parts | continuous-dough-divider-plc | 1× | 1 | 123 | assembly |
| 8.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.1.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 8.1.3 | SMD Passive (R/C/L) | smd-passives | 120× | 120 | · | part |
| 8.2 | Drive (VFD) | continuous-dough-divider-vfd | 1× | 1 | · | part |
| 8.3 | Operator Panel (HMI) 4 parts | continuous-dough-divider-hmi | 1× | 1 | 53 | assembly |
| 8.3.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.3.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.3.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.3.4 | SMD Passive (R/C/L) | smd-passives | 50× | 50 | · | part |
| 8.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.5 | Relay | relay | 6× | 6 | · | part |
| 8.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8.7 | Connector | connector | 22× | 22 | · | part |
| 9 | Frame and Outfeed 6 parts | continuous-dough-divider-frame | 1× | 1 | 13 | assembly |
| 9.1 | Base Frame | continuous-dough-divider-base-frame | 1× | 1 | · | part |
| 9.2 | Outfeed Belt | continuous-dough-divider-outfeed-belt | 1× | 1 | · | part |
| 9.3 | Outfeed Roller | continuous-dough-divider-outfeed-roller | 2× | 2 | · | part |
| 9.4 | Sheet Metal Panel | sheet-panel | 6× | 6 | · | part |
| 9.5 | Guard Interlock | continuous-dough-divider-interlock | 2× | 2 | · | part |
| 9.6 | Fastener Set | fastener-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Edible Oil Refining Line
3,224 parts · shares 13 with this page
Egg Breaking and Separating Line
1,126 parts · shares 13 with this page
 Hydrostatic Sterilizer
9,247 parts · shares 13 with this page
Industrial Bowl Cutter
280 parts · shares 13 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $1k–$500k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| gea.com ↗ | Düsseldorf, DE | Process technology | 20 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 20 units | 12–20 wks |
| tetrapak.com ↗ | Pully, CH | Food packaging & processing | 20 units | 12–20 wks |
| jbtc.com ↗ | Chicago, US | Food processing equipment | 20 units | 12–20 wks |
| alfalaval.com ↗ | Lund, SE | Heat transfer & separation | 20 units | 12–20 wks |
884-word article