Dough Sheeting Line
ProductOverview
A dough sheeting line turns a lump or block of dough into a continuous, even sheet of controlled thickness, the starting point for laminated and flat products such as croissants, puff pastry, pizza bases, pie crust, and crackers. Rolling dough by hand thins it but also tears the gluten and traps uneven stress; a sheeting line does the same job in many small steps so the gluten relaxes between them and the finished sheet lies flat, uniform, and free of internal tension. The line is a row of roller pairs and conveyors: dough enters thick at one end and leaves as a thin, trimmed sheet at the other, ready to be folded, filled, or cut.
The line is built as stages in sequence. The Infeed and Gauging forms a thick starting sheet, the Reduction Stations stations thin it in steps, the Conveyor System belts carry it between them, the Flour Dusting dusters stop it sticking, and the Trimming and Cutting squares and cuts it. The Drive System and Control System keep every stage in step.
Forming the starting sheet
The line must first turn loose dough into a coherent slab. The Infeed and Gauging holds bulk dough in an Infeed Hopper and feeds it through a pair of Gauging Roller rollers that press it into a thick, even starting sheet. Roller Scraper blades keep the soft dough from wrapping around a roller instead of passing through. The starting sheet is deliberately thick, because the thinning is done gradually downstream rather than all at once.
Gradual reduction
The core idea of sheeting is gradual reduction. The Reduction Stations section is a series of Roller Station stations, each a pair of Reduction Roller rollers set to a smaller gap than the last. Reducing the sheet a little at each step lets the gluten relax between stations, so the dough thins without tearing or springing back. Each station has a Gap Actuator to set its gap, and a Thickness Gauge at the end measures the finished sheet so the controller can trim the gaps to hold the target. The number of stations sets how thin the sheet can go: a croissant sheet may pass four or more stages to reach a few millimetres without damage.
Conveyors and rising speed
As a sheet is thinned it gets longer, so each stage must run faster than the one before it or the sheet would bunch up. The Conveyor System system carries the sheet on food-grade Conveyor Belt belts over Conveyor Roller rollers, with Belt Tensioner tensioners keeping each belt taut and tracking straight. The belts run at rising speeds matched to the thinning, so the sheet stays flat and under gentle, even tension. Getting these speed ratios right is what keeps the sheet from stretching, which would thin it unevenly and weaken it.
Flour dusting
A dough sheet is sticky on every surface it touches, so the line floors it constantly. The Flour Dusting system places dusters over the stations, each metering a thin film of flour from a Flour Hopper through a Dusting Roller onto the rollers and belts. The film lets the sheet release cleanly at every nip and lay-down. Dusting is light and even, because too much flour dries the sheet surface and shows as white streaks in the baked product.
Trimming, cutting, and scrap
A rolled sheet has ragged edges and is not yet cut to size. The Trimming and Cutting section squares it with two Edge Trimmer rotary trimmers that crop the sheet to a fixed width, and a Cross-Cutter cuts it across into lengths or blanks. The trimmed edge is dough that would otherwise be wasted, so a Scrap Return conveyor carries it back to the infeed to be rolled in again. Reworking trim this way keeps yield high on an expensive raw material.
Drive, control, and construction
A sheeting line is really a motion-control machine. The Drive System uses a Roller Servo Motor servo on each roller pair and a Belt Servo Motor servo on each conveyor, all coordinated. The Control System cabinet runs a motion PLC Controller that holds the speed ratios and the gap profile, driving the servos through Servo Drive drives and closing the loop on the thickness gauge, with a Operator Panel (HMI) panel for recipes. The whole line is stainless steel for washdown on a long Base Frame, and because the roller nips are dangerous, it carries Nip Guard guards and Guard Interlock interlocks at every pinch point.
Place in the bakery
A sheeting line feeds the makeup end of a bakery. Its even sheet goes on to a laminator that folds in butter for croissants and puff pastry, to a cutter and filler for pies and turnovers, or to a docker and cutter for crackers. The thickness and evenness it produces set the layer count and bake of everything downstream, so the gap profile and speed ratios are dialed in for each product and held tightly through the run.
Dough Sheeting Line parts and their functions
8 top-level parts · 456 parts in total · full bill of materials below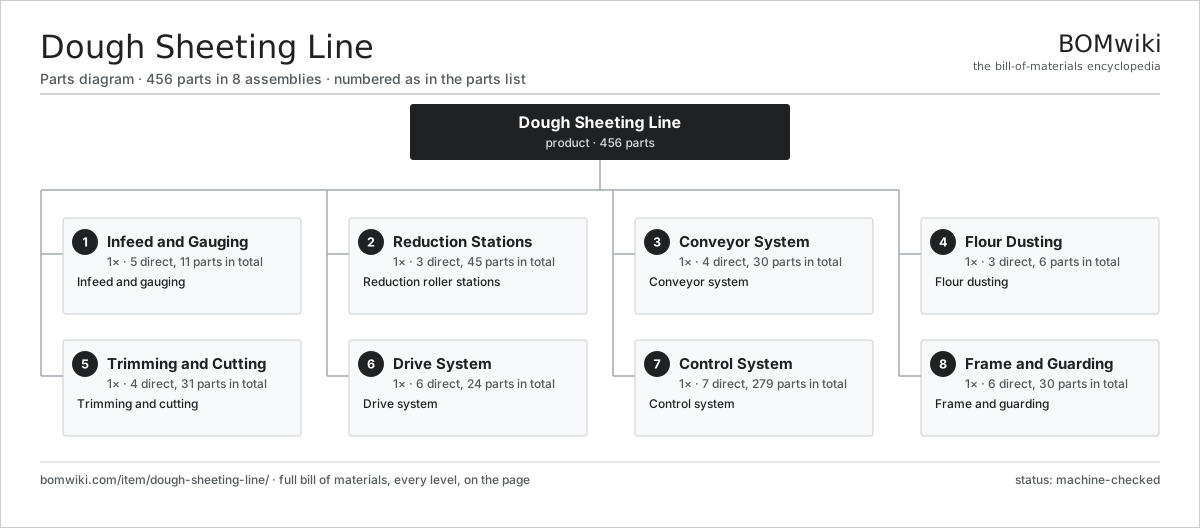
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Infeed and Gauging 5 parts | 1× | Infeed and gauging |
| 2 | Reduction Stations 3 parts | 1× | Reduction roller stations |
| 3 | Conveyor System 4 parts | 1× | Conveyor system |
| 4 | Flour Dusting 3 parts | 1× | Flour dusting |
| 5 | Trimming and Cutting 4 parts | 1× | Trimming and cutting |
| 6 | Drive System 6 parts | 1× | Drive system |
| 7 | Control System 7 parts | 1× | Control system |
| 8 | Frame and Guarding 6 parts | 1× | Frame and guarding |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Dough Sheeting Line
8 top-level lines · 64 rows shown · 456 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Infeed and Gauging 5 parts | dough-sheeting-line-infeed | 1× | 1 | 11 | assembly |
| 1.1 | Infeed Hopper | dough-sheeting-line-infeed-hopper | 1× | 1 | · | part |
| 1.2 | Gauging Roller | dough-sheeting-line-gauge-roller | 2× | 2 | · | part |
| 1.3 | Roller Scraper | dough-sheeting-line-gauge-scraper | 2× | 2 | · | part |
| 1.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 1.5 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 2 | Reduction Stations 3 parts | dough-sheeting-line-reduction | 1× | 1 | 45 | assembly |
| 2.1 | Roller Station 4 parts | dough-sheeting-line-roller-station | 4× | 4 | 10 | assembly |
| 2.1.1 | Reduction Roller | dough-sheeting-line-reduction-roller | 2× | 8 | · | part |
| 2.1.2 | Reduction Scraper | dough-sheeting-line-roller-scraper | 2× | 8 | · | part |
| 2.1.3 | Ball Bearing | ball-bearing | 4× | 16 | · | part |
| 2.1.4 | Oil Seal | oil-seal | 2× | 8 | · | part |
| 2.2 | Gap Actuator | dough-sheeting-line-gap-actuator | 4× | 4 | · | part |
| 2.3 | Thickness Gauge | dough-sheeting-line-thickness-gauge | 1× | 1 | · | part |
| 3 | Conveyor System 4 parts | dough-sheeting-line-conveyor | 1× | 1 | 30 | assembly |
| 3.1 | Conveyor Belt | dough-sheeting-line-belt | 3× | 3 | · | part |
| 3.2 | Conveyor Roller | dough-sheeting-line-conv-roller | 8× | 8 | · | part |
| 3.3 | Belt Tensioner | dough-sheeting-line-belt-tensioner | 3× | 3 | · | part |
| 3.4 | Ball Bearing | ball-bearing | 16× | 16 | · | part |
| 4 | Flour Dusting 3 parts | dough-sheeting-line-flour | 1× | 1 | 6 | assembly |
| 4.1 | Flour Hopper | dough-sheeting-line-flour-hopper | 2× | 2 | · | part |
| 4.2 | Dusting Roller | dough-sheeting-line-flour-roller | 2× | 2 | · | part |
| 4.3 | Duster Motor | dough-sheeting-line-flour-motor | 2× | 2 | · | part |
| 5 | Trimming and Cutting 4 parts | dough-sheeting-line-cutter | 1× | 1 | 31 | assembly |
| 5.1 | Edge Trimmer | dough-sheeting-line-edge-cutter | 2× | 2 | · | part |
| 5.2 | Cross-Cutter 3 parts | dough-sheeting-line-cross-cutter | 1× | 1 | 4 | assembly |
| 5.2.1 | Cross Blade | dough-sheeting-line-cross-blade | 1× | 1 | · | part |
| 5.2.2 | Cross Anvil | dough-sheeting-line-cross-anvil | 1× | 1 | · | part |
| 5.2.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 5.3 | Scrap Return | dough-sheeting-line-scrap-return | 1× | 1 | · | part |
| 5.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 5.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 5.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 5.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 5.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 6 | Drive System 6 parts | dough-sheeting-line-drive | 1× | 1 | 24 | assembly |
| 6.1 | Roller Servo Motor | dough-sheeting-line-roller-motor | 4× | 4 | · | part |
| 6.2 | Belt Servo Motor | dough-sheeting-line-belt-motor | 3× | 3 | · | part |
| 6.3 | Gearbox Housing | gearbox-housing | 4× | 4 | · | part |
| 6.4 | Helical Gear Pair | gear-pair | 4× | 4 | · | part |
| 6.5 | Drive Belt | drive-belt | 3× | 3 | · | part |
| 6.6 | Ball Bearing | ball-bearing | 6× | 6 | · | part |
| 7 | Control System 7 parts | dough-sheeting-line-control | 1× | 1 | 279 | assembly |
| 7.1 | PLC Controller 3 parts | dough-sheeting-line-plc | 1× | 1 | 163 | assembly |
| 7.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.1.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 7.1.3 | SMD Passive (R/C/L) | smd-passives | 160× | 160 | · | part |
| 7.2 | Servo Drive | dough-sheeting-line-vfd | 7× | 7 | · | part |
| 7.3 | Operator Panel (HMI) 4 parts | dough-sheeting-line-hmi | 1× | 1 | 63 | assembly |
| 7.3.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.3.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.3.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.3.4 | SMD Passive (R/C/L) | smd-passives | 60× | 60 | · | part |
| 7.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.5 | Relay | relay | 8× | 8 | · | part |
| 7.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 7.7 | Connector | connector | 36× | 36 | · | part |
| 8 | Frame and Guarding 6 parts | dough-sheeting-line-frame | 1× | 1 | 30 | assembly |
| 8.1 | Base Frame | dough-sheeting-line-base-frame | 1× | 1 | · | part |
| 8.2 | Sheet Metal Panel | sheet-panel | 10× | 10 | · | part |
| 8.3 | Nip Guard | dough-sheeting-line-nip-guard | 4× | 4 | · | part |
| 8.4 | Guard Interlock | dough-sheeting-line-interlock | 6× | 6 | · | part |
| 8.5 | Leveling Foot | dough-sheeting-line-leveling-foot | 8× | 8 | · | part |
| 8.6 | Fastener Set | fastener-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Flour Milling Plant
2,774 parts · shares 23 with this page
Fruit Grading Line
3,765 parts · shares 23 with this page
 Hydrostatic Sterilizer
9,247 parts · shares 23 with this page
 Industrial Coffee Grinder
788 parts · shares 23 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $1k–$500k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| gea.com ↗ | Düsseldorf, DE | Process technology | 20 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 20 units | 12–20 wks |
| tetrapak.com ↗ | Pully, CH | Food packaging & processing | 20 units | 12–20 wks |
| jbtc.com ↗ | Chicago, US | Food processing equipment | 20 units | 12–20 wks |
| alfalaval.com ↗ | Lund, SE | Heat transfer & separation | 20 units | 12–20 wks |
917-word article