Extruded Snack Line
ProductOverview
An extruded snack line turns cereal meal into light, puffed snacks such as corn curls, cheese puffs, and rice snacks. The process is direct expansion: a twin-screw extruder cooks a stiff dough under heat, pressure, and shear, and when that dough leaves the die into open air, the superheated water in it flashes to steam and blows the piece up into a porous puff. The line covers ingredient feeding, extrusion, cutting, drying, and seasoning, with gentle conveying between each step because the puffs are fragile. A Line Control System holds the feed rate, screw speed, barrel temperatures, and cutter speed in balance, since all four together set the texture of the finished snack.
Feeding the extruder
The line starts at the Ingredient Feed System. Corn or rice meal is held in the Meal Silo and metered out by gravimetric Loss-in-Weight Feeder units that hold the rate to within 0.5 percent, with separate feeders for minor ingredients. A Feed Screw delivers the blended meal evenly to the extruder inlet, and a Water Dosing Pump injects process water directly into the barrel to set the dough moisture at 14-22 percent. Feed accuracy matters because the extruder is starve-fed: screw speed and feed rate are set independently, so a wandering feed rate changes how full the screws run and shifts the cook.
Cooking and puffing
The heart of the line is the Twin-Screw Extruder. Two co-rotating, intermeshing Twin Screw Shaft turn inside a segmented Extruder Barrel, conveying the meal forward while kneading and shearing elements work it into a melt. A Main Drive Motor drives both screws through a Splitter Gearbox that splits torque and carries the thrust load. The barrel is divided into zones: Barrel Zone Heater bring it up to temperature at start-up, and a Barrel Cooling Jacket jacket pulls heat back out of the high-shear zones, because once the line is running the screws generate much of the cooking energy themselves. The amount of mechanical work put into each kilogram, the specific mechanical energy, is the single most useful number for tracking expansion, and a Pressure Sensor at the die tracks the buildup that drives puffing.
At the barrel exit sits the Die and Face Cutter. A hardened Die Plate sets the cross-section of the extrudate, and the moment the dough exits, the pressure drop flashes its water to steam and expands the piece. A rotating Face Cutter Head driven by the Cutter Motor slices the expanding rope flush against the die face, and cutter speed against throughput sets the length of each puff. A Die Heater keeps the die plate hot so every hole puffs the same way.
Drying
Fresh puffs still hold too much moisture to be crisp or shelf-stable, so they go to the Snack Dryer. A perforated Dryer Band carries them through hot-air zones supplied by a Dryer Burner and circulated by Dryer Recirculation Fan, with insulated Insulated Dryer Panel holding in the heat. Drying brings the puffs from extrusion moisture down to 1-3 percent, the level that gives the snap and shelf life consumers expect. Drying too hard scorches and shrinks the puff, too little leaves it tough, so the dryer runs in graded zones rather than one hot blast.
Seasoning
Dried puffs reach the Seasoning System. They tumble through a rotating Coating Drum where a heated Oil Spray Bar bar lays down a fine oil mist fed from the Seasoning Oil Tank, and a Powder Feeder doses seasoning powder proportional to product flow. The oil is what makes the powder stick, so spray rate and powder rate are tied together. Tumbling rather than spraying on a belt gives an even coat on all sides, which is what produces a consistently flavored cheese puff or curl.
Conveying
Because puffs are fragile and break into fines easily, the line uses gentle Product Conveying throughout. Vibratory Vibratory Conveyor pans move product with little tumbling, a Bucket Elevator lifts it between levels without dropping it, and a Distribution Belt splits the flow to several weighers feeding the baggers. Minimizing breakage protects both yield and the appearance of the packaged snack.
Materials and drives
Wetted and product-contact parts are 304 and 316 stainless steel, with hardened wear surfaces in the extruder barrel and die where shear and abrasion are highest. Screw shafts run on heavy thrust Ball Bearing units, and the dryer band, coating drum, and conveyors are turned by toothed Drive Belt drives. Barrel and dryer zones are regulated by the control system's temperature controllers, and the line's feeders, heaters, and fans are switched through a bank of Relay outputs powered from a 24 V Power Supply. The extruder is the most highly stressed machine on the line, so its barrel liners and screw elements are treated as wear items on a planned replacement schedule.
Variants and use
Recipe and die set the product. A corn-curl line runs a simple die and a high-shear screw for maximum expansion, while a rice-snack line runs cooler and wetter for a denser texture. Co-extrusion lines add a center pump that fills a hollow puff with a cream or cheese paste. Pellet lines stop after extrusion and drying to make a half-product that is later puffed by frying or hot air. Throughput scales with extruder size, from a pilot line at 200 kg per hour to a high-capacity line above 1,000 kg per hour using the same module layout. Recipes loaded from the HMI on the control system store feed rates, screw speed, barrel profile, cutter speed, and seasoning doses so a product reproduces run to run with little operator judgment.
Extruded Snack Line parts and their functions
7 top-level parts · 129 parts in total · full bill of materials below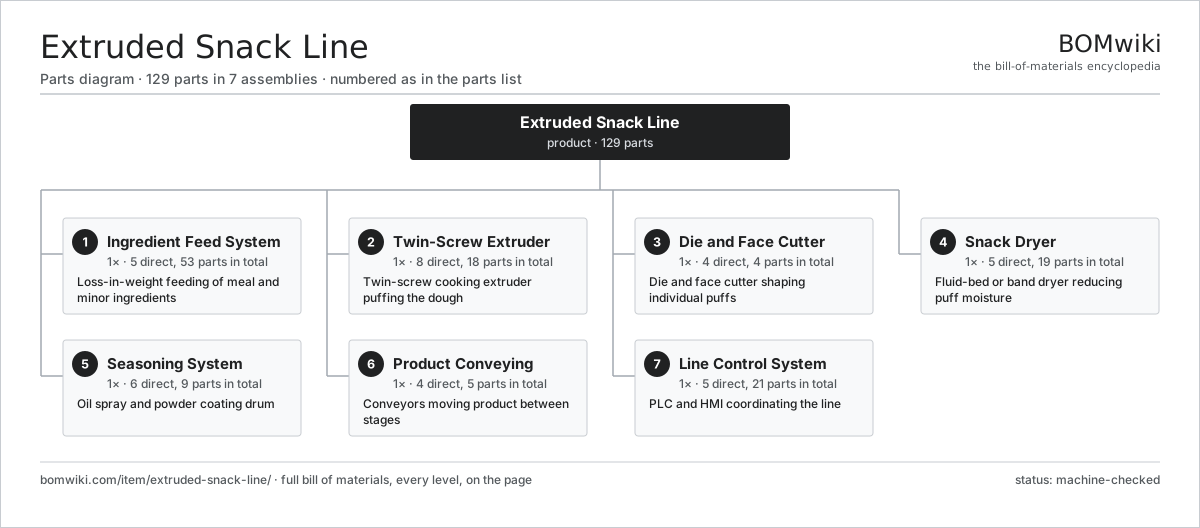
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Ingredient Feed System 5 parts | 1× | Loss-in-weight feeding of meal and minor ingredients |
| 2 | Twin-Screw Extruder 8 parts | 1× | Twin-screw cooking extruder puffing the dough |
| 3 | Die and Face Cutter 4 parts | 1× | Die and face cutter shaping individual puffs |
| 4 | Snack Dryer 5 parts | 1× | Fluid-bed or band dryer reducing puff moisture |
| 5 | Seasoning System 6 parts | 1× | Oil spray and powder coating drum |
| 6 | Product Conveying 4 parts | 1× | Conveyors moving product between stages |
| 7 | Line Control System 5 parts | 1× | PLC and HMI coordinating the line |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Extruded Snack Line
7 top-level lines · 48 rows shown · 129 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Ingredient Feed System 5 parts | extruded-snack-line-feed-system | 1× | 1 | 53 | assembly |
| 1.1 | Meal Silo | extruded-snack-line-meal-silo | 1× | 1 | · | part |
| 1.2 | Loss-in-Weight Feeder | extruded-snack-line-lw-feeder | 2× | 2 | · | part |
| 1.3 | Water Dosing Pump | extruded-snack-line-water-doser | 1× | 1 | · | part |
| 1.4 | Feed Screw | extruded-snack-line-feed-screw | 1× | 1 | · | part |
| 1.5 | Servo Motor 4 parts | servo-motor | 2× | 2 | 24 | assembly |
| 1.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 2 | 3 | assembly |
| 1.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 2 | 19 | assembly |
| 1.5.3 | Encoder | encoder | 1× | 2 | · | part |
| 1.5.4 | Motor Housing | motor-housing | 1× | 2 | · | part |
| 2 | Twin-Screw Extruder 8 parts | extruded-snack-line-extruder | 1× | 1 | 18 | assembly |
| 2.1 | Extruder Barrel | extruded-snack-line-barrel | 1× | 1 | · | part |
| 2.2 | Twin Screw Shaft | extruded-snack-line-screws | 2× | 2 | · | part |
| 2.3 | Splitter Gearbox | extruded-snack-line-gearbox | 1× | 1 | · | part |
| 2.4 | Main Drive Motor | extruded-snack-line-main-motor | 1× | 1 | · | part |
| 2.5 | Barrel Zone Heater | extruded-snack-line-barrel-heaters | 6× | 6 | · | part |
| 2.6 | Barrel Cooling Jacket | extruded-snack-line-barrel-cooling | 1× | 1 | · | part |
| 2.7 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 2.8 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 3 | Die and Face Cutter 4 parts | extruded-snack-line-die-cutter | 1× | 1 | 4 | assembly |
| 3.1 | Die Plate | extruded-snack-line-die-plate | 1× | 1 | · | part |
| 3.2 | Face Cutter Head | extruded-snack-line-cutter-head | 1× | 1 | · | part |
| 3.3 | Cutter Motor | extruded-snack-line-cutter-motor | 1× | 1 | · | part |
| 3.4 | Die Heater | extruded-snack-line-die-heater | 1× | 1 | · | part |
| 4 | Snack Dryer 5 parts | extruded-snack-line-dryer | 1× | 1 | 19 | assembly |
| 4.1 | Dryer Band | extruded-snack-line-dryer-band | 1× | 1 | · | part |
| 4.2 | Dryer Burner | extruded-snack-line-dryer-burner | 1× | 1 | · | part |
| 4.3 | Dryer Recirculation Fan | extruded-snack-line-dryer-fans | 4× | 4 | · | part |
| 4.4 | Insulated Dryer Panel | extruded-snack-line-dryer-panels | 12× | 12 | · | part |
| 4.5 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 5 | Seasoning System 6 parts | extruded-snack-line-seasoning-system | 1× | 1 | 9 | assembly |
| 5.1 | Coating Drum | extruded-snack-line-coating-drum | 1× | 1 | · | part |
| 5.2 | Oil Spray Bar | extruded-snack-line-oil-spray | 1× | 1 | · | part |
| 5.3 | Powder Feeder | extruded-snack-line-powder-feeder | 1× | 1 | · | part |
| 5.4 | Seasoning Oil Tank | extruded-snack-line-oil-tank | 1× | 1 | · | part |
| 5.5 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 5.6 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 6 | Product Conveying 4 parts | extruded-snack-line-conveying | 1× | 1 | 5 | assembly |
| 6.1 | Vibratory Conveyor | extruded-snack-line-vibratory-conveyor | 2× | 2 | · | part |
| 6.2 | Bucket Elevator | extruded-snack-line-bucket-elevator | 1× | 1 | · | part |
| 6.3 | Distribution Belt | extruded-snack-line-distribution-belt | 1× | 1 | · | part |
| 6.4 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 7 | Line Control System 5 parts | extruded-snack-line-control-system | 1× | 1 | 21 | assembly |
| 7.1 | Master PLC | extruded-snack-line-plc | 1× | 1 | · | part |
| 7.2 | HMI Touchscreen | extruded-snack-line-hmi | 1× | 1 | · | part |
| 7.3 | Zone Temperature Controller | extruded-snack-line-zone-controllers | 6× | 6 | · | part |
| 7.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.5 | Relay | relay | 12× | 12 | · | part |
Related products
same domain, ranked by shared parts Bottle Washing Machine
2,388 parts · shares 14 with this page
Brine Chilling System
239 parts · shares 14 with this page
 Drum Drying Machine
634 parts · shares 14 with this page
Egg Breaking and Separating Line
1,126 parts · shares 14 with this page
Egg Grading and Packing Line
705 parts · shares 14 with this page
 Flour Milling Plant
2,774 parts · shares 14 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $1k–$500k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| gea.com ↗ | Düsseldorf, DE | Process technology | 20 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 20 units | 12–20 wks |
| tetrapak.com ↗ | Pully, CH | Food packaging & processing | 20 units | 12–20 wks |
| jbtc.com ↗ | Chicago, US | Food processing equipment | 20 units | 12–20 wks |
| alfalaval.com ↗ | Lund, SE | Heat transfer & separation | 20 units | 12–20 wks |
1,027-word article