Hard Candy Forming Line
ProductOverview
A hard candy forming line converts cooked sugar syrup into shaped, individually wrapped boiled sweets in one continuous flow. Where a depositing line casts mass into molds, a forming line works the cooked mass mechanically: it cools and kneads the batch, rolls it into a cone, draws that cone down to a thin rope, and stamps individual candies from the rope with a die. The line covers seven stages, cooking, kneading, batch rolling, rope sizing, die forming, cooling, and wrapping, with a Line Control System keeping all of them in proportion. This approach suits high-volume boiled sweets, lollipops, and striped or filled candies where the rope can carry a center or a color pattern.
Cooking the mass
The line begins at the Vacuum Cooker. Sugar and glucose syrup are dissolved in the jacketed Premix Dissolving Tank, then pumped by the Syrup Pump through a steam-heated Cooking Coil that boils a thin film of syrup to 150-160 C. The hot syrup passes into the Vacuum Vessel, where a Vacuum Pump flashes off residual water to leave 1-2 percent moisture, the level that gives hard candy its glassy bite. A Mass Discharge Valve discharges the finished mass continuously without breaking the vacuum. Cooking as a film keeps the heat history short, so the sugar stays clear instead of developing the amber tint that long boiling produces.
Kneading in color and flavor
The discharged mass lands on the Cooling Kneader. A water-cooled Water-Cooled Table drops the mass from cooking temperature to a workable 80-90 C, while counter-rotating Kneading Arms fold and stretch it. At this point a Additive Doser meters in liquid color, citric acid, and flavor. Adding these after cooking protects the heat-sensitive flavors and lets a single cooked batch be split into several colors. Kneading also works air out of the mass and develops the even, plastic texture the forming rollers need. For striped candies the operator lays colored ropes onto the batch by hand or by a side feeder before it enters the rollers.
Forming the rope
The kneaded mass is loaded into the Batch Roller, where four heated Tapered Roller Cone rotate the mass into a slowly turning cone. A Roller Heater keeps the rollers at 70-90 C so the surface stays tacky enough to feed without tearing. The tip of the cone feeds the Rope Sizer, a series of grooved Sizing Wheel Pair that draw the cone down in stages to a uniform rope. A Rope Diameter Sensor reads the rope diameter and trims the sizer speed in a feedback loop, since a rope that is too thick or thin throws off piece weight at the die.
The rope enters the Die Former, where a shaped Forming Die carried on a Die Chain pinches and stamps each candy, embossing the surface pattern and cutting the piece free. A Die Air Cooler blows compressed air across the dies so the hot candy releases cleanly instead of sticking and smearing. Die changeover sets the shape and weight of the finished sweet.
Cooling and wrapping
Formed candies drop onto the Cooling Conveyor. A wide Cooling Belt carries them under banks of Cooling Fan that harden the surface and core, and a Vibrating Spreader spreads the pieces into a single layer and breaks any clusters before wrapping. The candies must be fully set and below their sticking point before they reach the wrapper, or they will deform in the pockets.
Wrapping is done by the High-Speed Wrapper, which can run at up to 1,000 pieces per minute. A Feed Turret places each candy into a wrapping pocket in time with film drawn from two Film Unwind Reel reels. Rotating Twist Head Set seal the wrapper by twist or fold, and a Reject Gate ejects any unwrapped, doubled, or off-weight pieces so only good product reaches the case packer.
Materials and drives
Wetted surfaces are 304 and 316 stainless steel built for clean-in-place and the abrasive, sticky nature of sugar. The cooker and rollers are held at temperature by zone-controlled Heating Element units, while forming and cooling rely on chilled water and air. Shafts run on sealed Ball Bearing units, the cooling and wrapper drives use a toothed Drive Belt, and the batch roller carries its load through a gear set inside a Gearbox Housing with a matched Helical Gear Pair. Vacuum joints are sealed with a standard O-Ring Set. Each station has its own Variable Frequency Drive so the control system can hold the cook output, forming speed, and wrapping rate in a fixed ratio.
Variants and use
Configuration follows the product. A plain boiled-sweet line runs a single rope and a basic die, while a lollipop line adds a stick inserter at the die and a longer cooling section for the heavier head. Filled-candy lines add a center pump that injects syrup, jam, or chocolate into the rope before sizing, and striped lines add side feeders for colored ropes. Throughput scales with rope count and die width, so the same modules serve a regional confectioner and a high-volume plant. Recipes loaded from the HMI on the control system store cook profiles, additive doses, forming speeds, and reject limits, letting a product be reproduced run to run with little operator judgment.
Hard Candy Forming Line parts and their functions
8 top-level parts · 223 parts in total · full bill of materials below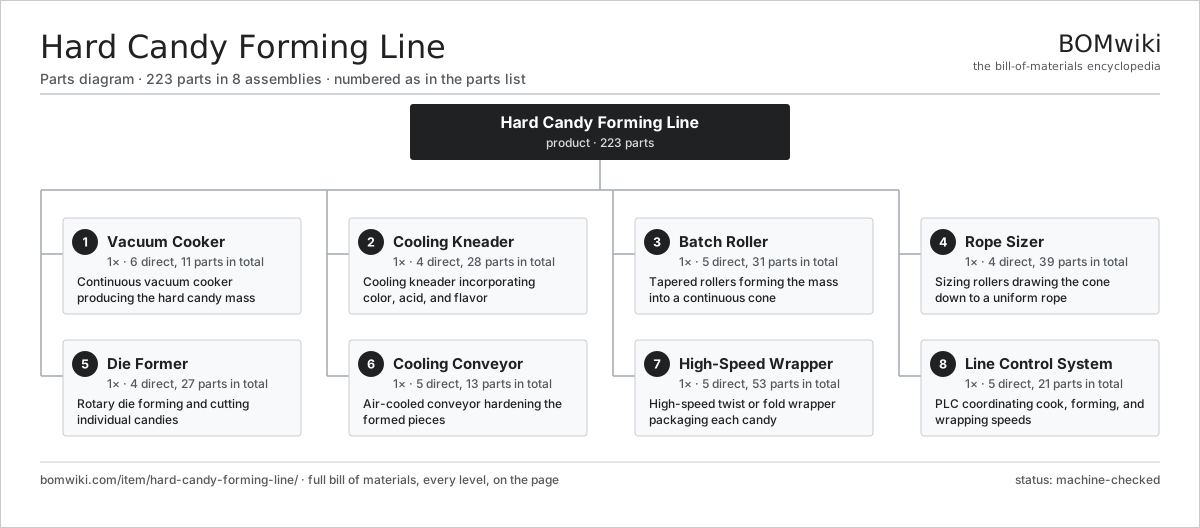
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Vacuum Cooker 6 parts | 1× | Continuous vacuum cooker producing the hard candy mass |
| 2 | Cooling Kneader 4 parts | 1× | Cooling kneader incorporating color, acid, and flavor |
| 3 | Batch Roller 5 parts | 1× | Tapered rollers forming the mass into a continuous cone |
| 4 | Rope Sizer 4 parts | 1× | Sizing rollers drawing the cone down to a uniform rope |
| 5 | Die Former 4 parts | 1× | Rotary die forming and cutting individual candies |
| 6 | Cooling Conveyor 5 parts | 1× | Air-cooled conveyor hardening the formed pieces |
| 7 | High-Speed Wrapper 5 parts | 1× | High-speed twist or fold wrapper packaging each candy |
| 8 | Line Control System 5 parts | 1× | PLC coordinating cook, forming, and wrapping speeds |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Hard Candy Forming Line
8 top-level lines · 69 rows shown · 223 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Vacuum Cooker 6 parts | hard-candy-forming-line-cooker | 1× | 1 | 11 | assembly |
| 1.1 | Premix Dissolving Tank | hard-candy-forming-line-premix-tank | 1× | 1 | · | part |
| 1.2 | Cooking Coil | hard-candy-forming-line-cook-coil | 1× | 1 | · | part |
| 1.3 | Vacuum Vessel 3 parts | hard-candy-forming-line-vacuum-vessel | 1× | 1 | 4 | assembly |
| 1.3.1 | Vacuum Pump | hard-candy-forming-line-vacuum-pump | 1× | 1 | · | part |
| 1.3.2 | Mass Discharge Valve | hard-candy-forming-line-mass-valve | 1× | 1 | · | part |
| 1.3.3 | O-Ring Set | oring-set | 2× | 2 | · | part |
| 1.4 | Syrup Pump | hard-candy-forming-line-syrup-pump | 1× | 1 | · | part |
| 1.5 | Heating Element | heating-element | 2× | 2 | · | part |
| 1.6 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 2 | Cooling Kneader 4 parts | hard-candy-forming-line-kneader | 1× | 1 | 28 | assembly |
| 2.1 | Water-Cooled Table | hard-candy-forming-line-cooling-table | 1× | 1 | · | part |
| 2.2 | Kneading Arms | hard-candy-forming-line-kneader-arms | 2× | 2 | · | part |
| 2.3 | Additive Doser | hard-candy-forming-line-additive-doser | 1× | 1 | · | part |
| 2.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 2.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 2.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 2.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 2.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 3 | Batch Roller 5 parts | hard-candy-forming-line-batch-roller | 1× | 1 | 31 | assembly |
| 3.1 | Tapered Roller Cone | hard-candy-forming-line-roller-cones | 4× | 4 | · | part |
| 3.2 | Roller Heater | hard-candy-forming-line-roller-heater | 1× | 1 | · | part |
| 3.3 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 3.4 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 3.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 3.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 3.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 3.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 3.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 4 | Rope Sizer 4 parts | hard-candy-forming-line-rope-sizer | 1× | 1 | 39 | assembly |
| 4.1 | Sizing Wheel Pair | hard-candy-forming-line-sizing-wheels | 6× | 6 | · | part |
| 4.2 | Rope Diameter Sensor | hard-candy-forming-line-rope-sensor | 1× | 1 | · | part |
| 4.3 | Ball Bearing | ball-bearing | 8× | 8 | · | part |
| 4.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 4.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 4.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 4.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 4.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 5 | Die Former 4 parts | hard-candy-forming-line-die-former | 1× | 1 | 27 | assembly |
| 5.1 | Forming Die | hard-candy-forming-line-forming-die | 1× | 1 | · | part |
| 5.2 | Die Chain | hard-candy-forming-line-die-chain | 1× | 1 | · | part |
| 5.3 | Die Air Cooler | hard-candy-forming-line-die-cooler | 1× | 1 | · | part |
| 5.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 5.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 5.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 5.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 5.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 6 | Cooling Conveyor 5 parts | hard-candy-forming-line-cooling-conveyor | 1× | 1 | 13 | assembly |
| 6.1 | Cooling Belt | hard-candy-forming-line-cooling-belt | 1× | 1 | · | part |
| 6.2 | Cooling Fan | hard-candy-forming-line-cooling-fans | 4× | 4 | · | part |
| 6.3 | Vibrating Spreader | hard-candy-forming-line-vibrating-section | 1× | 1 | · | part |
| 6.4 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 6.5 | Ball Bearing | ball-bearing | 6× | 6 | · | part |
| 7 | High-Speed Wrapper 5 parts | hard-candy-forming-line-wrapper | 1× | 1 | 53 | assembly |
| 7.1 | Feed Turret | hard-candy-forming-line-feed-turret | 1× | 1 | · | part |
| 7.2 | Film Unwind Reel | hard-candy-forming-line-film-unwind | 2× | 2 | · | part |
| 7.3 | Twist Head Set | hard-candy-forming-line-twist-heads | 1× | 1 | · | part |
| 7.4 | Reject Gate | hard-candy-forming-line-reject-gate | 1× | 1 | · | part |
| 7.5 | Servo Motor 4 parts | servo-motor | 2× | 2 | 24 | assembly |
| 7.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 2 | 3 | assembly |
| 7.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 2 | 19 | assembly |
| 7.5.3 | Encoder | encoder | 1× | 2 | · | part |
| 7.5.4 | Motor Housing | motor-housing | 1× | 2 | · | part |
| 8 | Line Control System 5 parts | hard-candy-forming-line-control-system | 1× | 1 | 21 | assembly |
| 8.1 | Master PLC | hard-candy-forming-line-plc | 1× | 1 | · | part |
| 8.2 | HMI Touchscreen | hard-candy-forming-line-hmi | 1× | 1 | · | part |
| 8.3 | Variable Frequency Drive | hard-candy-forming-line-vfd | 6× | 6 | · | part |
| 8.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.5 | Relay | relay | 12× | 12 | · | part |
Related products
same domain, ranked by shared parts Bottle Washing Machine
2,388 parts · shares 18 with this page
Egg Breaking and Separating Line
1,126 parts · shares 18 with this page
Yogurt Production Line
271 parts · shares 18 with this page
Chocolate Ball Mill
134 parts · shares 17 with this page
 Chocolate Conching Machine
161 parts · shares 17 with this page
Aseptic Filler
1,020 parts · shares 17 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $1k–$500k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| gea.com ↗ | Düsseldorf, DE | Process technology | 20 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 20 units | 12–20 wks |
| tetrapak.com ↗ | Pully, CH | Food packaging & processing | 20 units | 12–20 wks |
| jbtc.com ↗ | Chicago, US | Food processing equipment | 20 units | 12–20 wks |
| alfalaval.com ↗ | Lund, SE | Heat transfer & separation | 20 units | 12–20 wks |
1,000-word article