Pasta Extruder
ProductAlso known as: Pasta Extruder Line
Overview
A pasta extruder line turns durum semolina and water into shaped pasta by mixing the two into a stiff dough and then forcing that dough through a die under high pressure. Unlike a sheeting line, which rolls dough flat and cuts it, an extruder presses dough through holes whose shape becomes the pasta cross-section, so the same machine can make spaghetti, penne, macaroni, or fusilli simply by changing the Bronze Die. The line runs continuously: dry semolina and metered water enter one end, and finished wet pasta leaves the other onto a conveyor that carries it to a dryer. The press is the heart of a dry-pasta factory, and the quality of the strand, its color, its surface, and how it cooks, is set here before any drying happens.
The machine is built as a sequence. The Mixing Trough blends semolina and water into damp crumbs, the Vacuum De-aeration Unit pulls air out of those crumbs, the Extrusion Screw compresses them into a dense plastic mass, the Extrusion Head pushes that mass through the die, and the Cutting Unit crops the strands to length. A Water Dosing System system meters hydration, the Main Drive Train turns the screw, and the Control Cabinet holds the recipe across all of it.
Mixing and hydration
Pasta dough is not kneaded smooth like bread dough; it is mixed only until the water is evenly spread through the semolina, leaving a coarse crumb. The Mixing Trough does this with two slow Mixing Shaft shafts carrying many Mixing Paddle paddles inside a stainless Mixing Trough Body. Hydration is the single most important variable. Too little water and the dough will not press; too much and the pasta is sticky and weak. The Water Dosing System system meters water through a Water Dosing Pump and reads back actual flow with a Water Flow Meter, spraying it onto the dry feed through Spray Nozzle nozzles so the mixer sees an even blend. Target hydration sits near 30 percent, and the controller trims it to keep the head pressure steady.
De-aeration
Air trapped in the dough is the enemy of good pasta. Bubbles make the dried product chalky white and brittle, and they leave it cloudy when cooked. The Vacuum De-aeration Unit unit solves this by drawing the crumbly dough through a sealed Vacuum Chamber held below atmospheric pressure by a Vacuum Pump. Removing the air lets the screw compress the dough into a void-free mass that dries to the translucent amber color buyers associate with good durum pasta. A Pressure Sensor watches the vacuum level, and Vacuum Valve valves let the chamber be isolated for cleaning between runs.
The screw, head, and die
The Extrusion Screw is a single hard-chromed Extrusion Screw Shaft turning slowly inside a wear-resistant Screw Barrel. Its flight pitch decreases toward the outlet, so the dough is squeezed into a dense plug that builds pressure of 80 to 120 bar. That pressure would heat the dough and damage its gluten, so a Barrel Cooling Jacket holds the barrel near 45 C with cooling water. The compressed dough reaches the Extrusion Head, where a Dough Spreader fans it evenly across the Bronze Die. The die is a bronze plate drilled with the shape of the pasta; each hole carries a PTFE Die Insert of PTFE that gives a smooth, glassy surface, while bronze-faced inserts give the rough surface that holds sauce. A Die Clamp Ring locks the die against full pressure, and a Die Air Cooler blows air on the emerging strands to set them.
Cutting and take-away
As pasta leaves the die it must be cropped to length. The Cutting Unit does this with a Cutting Blade driven by a Cutter Servo Motor servo; the ratio of blade speed to extrusion rate sets the length of each short shape, while long pasta such as spaghetti is hung over rods instead. A Product Fan scatters short shapes evenly so they do not clump, and the Take-away Conveyor carries the wet product away. The conveyor runs a food-grade Conveyor Belt over Belt Roller rollers and feeds the dryer, which is a separate machine downstream.
Drive and control
Pressing dough takes steady, high torque at low speed. The Main Drive Train supplies it with a Main Drive Motor of 22 to 45 kW through a reducer that turns the screw at only a few dozen rpm. The Control Cabinet cabinet coordinates the whole line: an PLC Controller runs the recipe, Variable-Frequency Drive drives set screw and conveyor speed, and an Operator Panel (HMI) panel lets the operator pick a shape and watch the line. The controller links water dosing, screw speed, and cut length so that one recipe gives the same product run after run.
Construction and use
Because pasta is a food, the whole line is stainless steel and built for washdown. The Frame and Guarding carries everything on a welded Base Frame with Sheet Metal Panel guards and Guard Interlock interlocks that stop the machine if a cover opens. Lines like this run in dry-pasta plants making hundreds to thousands of kilograms per hour, feeding directly into a dryer and then packaging. Changeover between shapes is a die swap and a recipe change, which is why one press can serve a whole catalog of products. The extruder sets pasta quality at the source: hydration, de-aeration, temperature control, and die choice together decide color, texture, and how the pasta will cook on the plate.
Pasta Extruder parts and their functions
9 top-level parts · 472 parts in total · full bill of materials below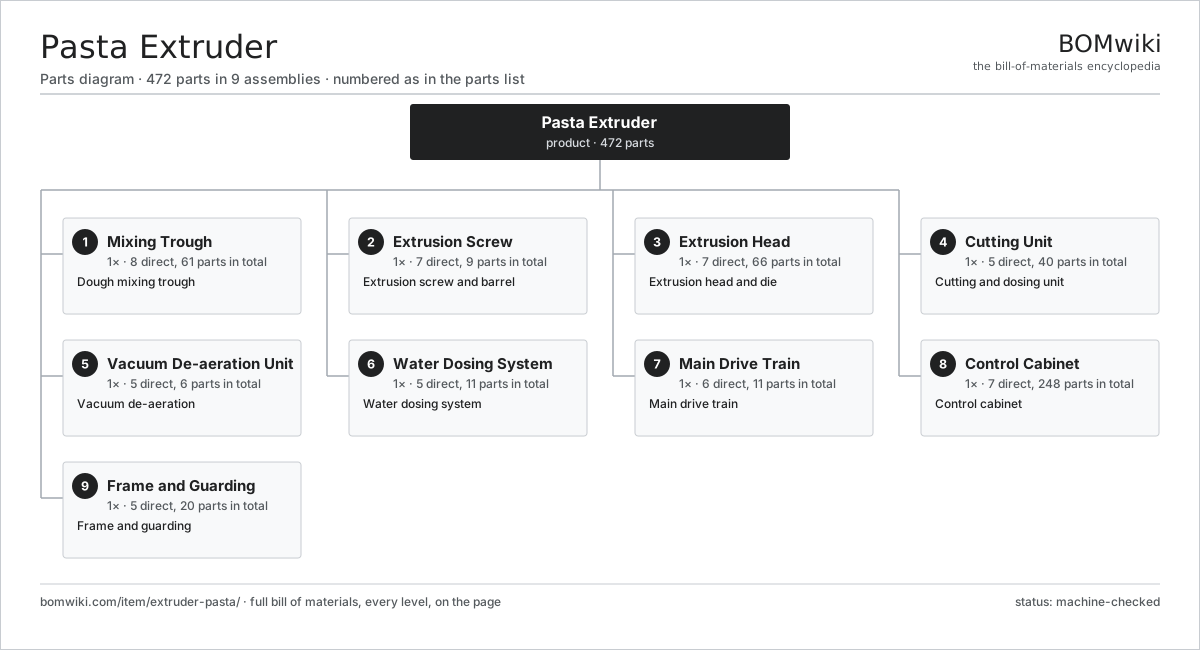
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Mixing Trough 8 parts | 1× | Dough mixing trough |
| 2 | Extrusion Screw 7 parts | 1× | Extrusion screw and barrel |
| 3 | Extrusion Head 7 parts | 1× | Extrusion head and die |
| 4 | Cutting Unit 5 parts | 1× | Cutting and dosing unit |
| 5 | Vacuum De-aeration Unit 5 parts | 1× | Vacuum de-aeration |
| 6 | Water Dosing System 5 parts | 1× | Water dosing system |
| 7 | Main Drive Train 6 parts | 1× | Main drive train |
| 8 | Control Cabinet 7 parts | 1× | Control cabinet |
| 9 | Frame and Guarding 5 parts | 1× | Frame and guarding |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Pasta Extruder
9 top-level lines · 82 rows shown · 472 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Mixing Trough 8 parts | extruder-pasta-mixer | 1× | 1 | 61 | assembly |
| 1.1 | Mixing Trough Body | extruder-pasta-trough | 1× | 1 | · | part |
| 1.2 | Mixing Shaft | extruder-pasta-mix-shaft | 2× | 2 | · | part |
| 1.3 | Mixing Paddle | extruder-pasta-mix-paddle | 24× | 24 | · | part |
| 1.4 | Trough Cover | extruder-pasta-trough-cover | 1× | 1 | · | part |
| 1.5 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 1.6 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 1.6.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 1.6.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 1.6.3 | Encoder | encoder | 1× | 1 | · | part |
| 1.6.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 1.7 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 1.8 | Oil Seal | oil-seal | 4× | 4 | · | part |
| 2 | Extrusion Screw 7 parts | extruder-pasta-screw | 1× | 1 | 9 | assembly |
| 2.1 | Extrusion Screw Shaft | extruder-pasta-screw-shaft | 1× | 1 | · | part |
| 2.2 | Screw Barrel | extruder-pasta-barrel | 1× | 1 | · | part |
| 2.3 | Barrel Cooling Jacket | extruder-pasta-barrel-jacket | 1× | 1 | · | part |
| 2.4 | Screw Tip | extruder-pasta-screw-tip | 1× | 1 | · | part |
| 2.5 | Thrust Bearing | extruder-pasta-thrust-bearing | 1× | 1 | · | part |
| 2.6 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 2.7 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 3 | Extrusion Head 7 parts | extruder-pasta-head | 1× | 1 | 66 | assembly |
| 3.1 | Head Body | extruder-pasta-head-body | 1× | 1 | · | part |
| 3.2 | Bronze Die | extruder-pasta-die | 1× | 1 | · | part |
| 3.3 | PTFE Die Insert | extruder-pasta-die-insert | 60× | 60 | · | part |
| 3.4 | Dough Spreader | extruder-pasta-spreader | 1× | 1 | · | part |
| 3.5 | Die Clamp Ring | extruder-pasta-die-clamp | 1× | 1 | · | part |
| 3.6 | Die Air Cooler | extruder-pasta-die-cooler | 1× | 1 | · | part |
| 3.7 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 4 | Cutting Unit 5 parts | extruder-pasta-cutter | 1× | 1 | 40 | assembly |
| 4.1 | Cutting Blade | extruder-pasta-cutter-blade | 1× | 1 | · | part |
| 4.2 | Cutter Servo Motor | extruder-pasta-cutter-motor | 1× | 1 | · | part |
| 4.3 | Product Fan | extruder-pasta-spreader-fan | 1× | 1 | · | part |
| 4.4 | Take-away Conveyor 3 parts | extruder-pasta-conveyor | 1× | 1 | 13 | assembly |
| 4.4.1 | Conveyor Belt | extruder-pasta-belt | 1× | 1 | · | part |
| 4.4.2 | Belt Roller | extruder-pasta-roller | 4× | 4 | · | part |
| 4.4.3 | Ball Bearing | ball-bearing | 8× | 8 | · | part |
| 4.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 4.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 4.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 4.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 4.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 5 | Vacuum De-aeration Unit 5 parts | extruder-pasta-vacuum | 1× | 1 | 6 | assembly |
| 5.1 | Vacuum Chamber | extruder-pasta-vacuum-chamber | 1× | 1 | · | part |
| 5.2 | Vacuum Pump | extruder-pasta-vacuum-pump | 1× | 1 | · | part |
| 5.3 | Vacuum Valve | extruder-pasta-vacuum-valve | 2× | 2 | · | part |
| 5.4 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 5.5 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 6 | Water Dosing System 5 parts | extruder-pasta-water | 1× | 1 | 11 | assembly |
| 6.1 | Water Dosing Pump | extruder-pasta-water-pump | 1× | 1 | · | part |
| 6.2 | Water Flow Meter | extruder-pasta-flow-meter | 1× | 1 | · | part |
| 6.3 | Spray Nozzle | extruder-pasta-water-nozzle | 6× | 6 | · | part |
| 6.4 | Water Buffer Tank | extruder-pasta-water-tank | 1× | 1 | · | part |
| 6.5 | Water Valve | extruder-pasta-water-valve | 2× | 2 | · | part |
| 7 | Main Drive Train 6 parts | extruder-pasta-drive | 1× | 1 | 11 | assembly |
| 7.1 | Main Drive Motor | extruder-pasta-main-motor | 1× | 1 | · | part |
| 7.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 7.3 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 7.4 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 7.5 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 7.6 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 8 | Control Cabinet 7 parts | extruder-pasta-control | 1× | 1 | 248 | assembly |
| 8.1 | PLC Controller 3 parts | extruder-pasta-plc | 1× | 1 | 143 | assembly |
| 8.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.1.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 8.1.3 | SMD Passive (R/C/L) | smd-passives | 140× | 140 | · | part |
| 8.2 | Variable-Frequency Drive | extruder-pasta-vfd | 2× | 2 | · | part |
| 8.3 | Operator Panel (HMI) 4 parts | extruder-pasta-hmi | 1× | 1 | 63 | assembly |
| 8.3.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.3.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.3.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.3.4 | SMD Passive (R/C/L) | smd-passives | 60× | 60 | · | part |
| 8.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.5 | Relay | relay | 8× | 8 | · | part |
| 8.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8.7 | Connector | connector | 30× | 30 | · | part |
| 9 | Frame and Guarding 5 parts | extruder-pasta-frame | 1× | 1 | 20 | assembly |
| 9.1 | Base Frame | extruder-pasta-base-frame | 1× | 1 | · | part |
| 9.2 | Sheet Metal Panel | sheet-panel | 8× | 8 | · | part |
| 9.3 | Leveling Foot | extruder-pasta-leveling-foot | 6× | 6 | · | part |
| 9.4 | Guard Interlock | extruder-pasta-interlock | 4× | 4 | · | part |
| 9.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Hydrostatic Sterilizer
9,247 parts · shares 25 with this page
 Industrial Coffee Grinder
788 parts · shares 25 with this page
 Sausage Linking Machine
518 parts · shares 25 with this page
 Bottle Washing Machine
2,388 parts · shares 24 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $1k–$500k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| gea.com ↗ | Düsseldorf, DE | Process technology | 20 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 20 units | 12–20 wks |
| tetrapak.com ↗ | Pully, CH | Food packaging & processing | 20 units | 12–20 wks |
| jbtc.com ↗ | Chicago, US | Food processing equipment | 20 units | 12–20 wks |
| alfalaval.com ↗ | Lund, SE | Heat transfer & separation | 20 units | 12–20 wks |
966-word article