Food Extruder
ProductOverview
A food extruder cooks and shapes starch- and protein-based ingredients in a single continuous step. Dry meal and water enter at one end, and a few seconds later finished product, breakfast cereal, expanded snacks, pasta, pet food kibble, or texturized vegetable protein, exits a die at the other. The cooking happens inside a heated barrel where two intermeshing screws knead the mass under heat and pressure. The combination of mechanical shear from the screws and thermal energy from the barrel gelatinizes starch and denatures protein, turning a dry powder into a hot, plasticized melt. When that melt is forced through a die and the pressure drops to atmospheric, the superheated water flashes to steam and the product puffs and sets into its final shape.
The twin-screw cooking extruder is the dominant type for cooked foods because the two co-rotating screws are self-wiping, conveying positively regardless of how sticky the material becomes and giving precise control over residence time and shear. The parts that define it are the Extruder Barrel and the Screw Element Set inside it, fed by the Feed System and powered by the Drive Unit.
Feed and preconditioning
Output quality depends on a perfectly steady feed, so the Feed System uses a gravimetric loss-in-weight feeder: an Feed Auger Screw driven by a servo Feeder Servo Motor meters dry meal from the hopper while an Loss-in-Weight Load Cell continuously weighs the system and corrects the rate. Many lines add a Preconditioner ahead of the extruder, a paddle vessel that mixes the meal with steam and water to pre-hydrate and pre-heat it. Preconditioning raises capacity, cuts wear, and improves cook uniformity by starting hydration before the material reaches the screws.
Barrel and screws
The Extruder Barrel is built from Barrel Segment sections clamped end to end, each lined with a hardened Hardened Barrel Liner of carbide-coated steel because the cooking mass is abrasive. Segmenting the barrel lets each zone be heated or cooled separately and lets a worn liner be replaced without scrapping the whole barrel. A Vent / Degas Port near the end releases excess steam, and an Barrel Thermocouple in each zone feeds the temperature control.
The Screw Element Set is modular: Conveying Screw Element sections, Kneading Block sections, and Reverse-Flight Element sections slide onto a splined Splined Screw Shaft in a sequence chosen for the product. Conveying elements move material forward, kneading blocks generate the shear and mixing that cook it, and reverse elements create a pressure dam that builds residence time and fills the screw. Changing the element order, in effect reprogramming the screw, lets one machine make a gently cooked pasta or an aggressively sheared expanded snack.
Drive
Twin-screw extruders run at high torque and high speed, so the Drive Unit is heavily built. A Main Drive Motor of 50 to 800 kW drives a Torque Distribution Gearbox that splits torque to the two parallel screw shafts and holds them in phase so the intermeshing flights never touch. Because the screws push back hard against the die pressure, a Tandem Thrust Bearing tandem set absorbs the axial load, and a Gearbox Lube System with its own pump, cooler, and filter keeps the high-load gearbox alive. Screw speed is set by the Variable Frequency Drive.
Die, cutting, and thermal control
At the discharge the melt is forced through the Die and Cutter. A Die Plate carrying replaceable carbide Die Insert holes shapes the strands, and a rotating Face Cutter Head with Cutter Blade knives slices them to length at the die face, setting the piece size. The Thermal System holds each zone on profile using band Heating Element heaters and an Barrel Cooling Jacket fed by a water pump, with a Zone Temperature Controller per zone, since cooking extrusion is exothermic and many zones need cooling, not heating, once the screws are doing work.
Liquid injection and control
The Liquid Injection system meters process water through an Water Injection Nozzle and, where steam cooking is wanted, an Steam Injection Nozzle, using a high-pressure High-Pressure Injection Pump and a Liquid Flow Meter to set the moisture at the die, the variable that most controls expansion and texture. Everything is coordinated by the Control Panel, where a PLC Module and HMI Touchscreen run the recipe and a Screw Torque Monitor watches screw torque and die pressure, the early signs of a developing blockage.
Materials and use
Wear parts, screw elements, barrel liners, and die inserts, are nitrided or carbide-faced to survive the abrasive cook, while product-contact surfaces elsewhere are stainless steel finished to sanitary standards. The same platform makes a wide range of products by changing screw configuration, die, moisture, and temperature profile, which is why extrusion underpins so much of the cereal, snack, pet-food, and plant-protein industry: one continuous machine that cooks, mixes, shapes, and expands in seconds.
Food Extruder parts and their functions
9 top-level parts · 860 parts in total · full bill of materials below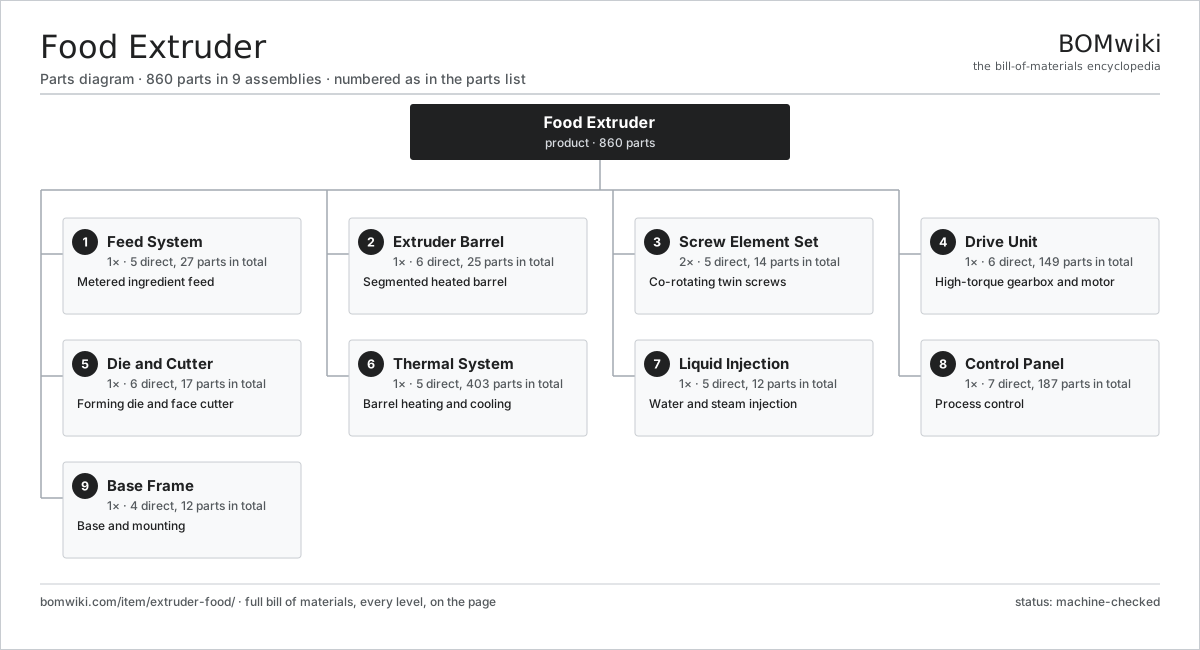
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Feed System 5 parts | 1× | Metered ingredient feed |
| 2 | Extruder Barrel 6 parts | 1× | Segmented heated barrel |
| 3 | Screw Element Set 5 parts | 2× | Co-rotating twin screws |
| 4 | Drive Unit 6 parts | 1× | High-torque gearbox and motor |
| 5 | Die and Cutter 6 parts | 1× | Forming die and face cutter |
| 6 | Thermal System 5 parts | 1× | Barrel heating and cooling |
| 7 | Liquid Injection 5 parts | 1× | Water and steam injection |
| 8 | Control Panel 7 parts | 1× | Process control |
| 9 | Base Frame 4 parts | 1× | Base and mounting |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Food Extruder
9 top-level lines · 93 rows shown · 860 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Feed System 5 parts | extruder-food-feed-system | 1× | 1 | 27 | assembly |
| 1.1 | Feed Hopper | extruder-food-feed-hopper | 1× | 1 | · | part |
| 1.2 | Feed Auger Screw | extruder-food-feed-screw | 1× | 1 | · | part |
| 1.3 | Feeder Servo Motor | extruder-food-feed-motor | 1× | 1 | · | part |
| 1.4 | Loss-in-Weight Load Cell | extruder-food-feed-loadcell | 1× | 1 | · | part |
| 1.5 | Preconditioner 5 parts | extruder-food-preconditioner | 1× | 1 | 23 | assembly |
| 1.5.1 | Preconditioner Shell | extruder-food-precond-shell | 1× | 1 | · | part |
| 1.5.2 | Preconditioner Paddle | extruder-food-precond-paddle | 12× | 12 | · | part |
| 1.5.3 | Preconditioner Shaft | extruder-food-precond-shaft | 2× | 2 | · | part |
| 1.5.4 | Steam Injection Port | extruder-food-steam-port | 4× | 4 | · | part |
| 1.5.5 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 2 | Extruder Barrel 6 parts | extruder-food-barrel | 1× | 1 | 25 | assembly |
| 2.1 | Barrel Segment | extruder-food-barrel-segment | 6× | 6 | · | part |
| 2.2 | Hardened Barrel Liner | extruder-food-barrel-liner | 6× | 6 | · | part |
| 2.3 | Segment Clamp Ring | extruder-food-clamp-ring | 5× | 5 | · | part |
| 2.4 | Vent / Degas Port | extruder-food-vent-port | 1× | 1 | · | part |
| 2.5 | Barrel Thermocouple | extruder-food-thermocouple | 6× | 6 | · | part |
| 2.6 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 3 | Screw Element Set 5 parts | extruder-food-screw-set | 2× | 2 | 14 | assembly |
| 3.1 | Splined Screw Shaft | extruder-food-screw-shaft | 1× | 2 | · | part |
| 3.2 | Conveying Screw Element | extruder-food-conveying-element | 6× | 12 | · | part |
| 3.3 | Kneading Block | extruder-food-kneading-block | 4× | 8 | · | part |
| 3.4 | Reverse-Flight Element | extruder-food-reverse-element | 2× | 4 | · | part |
| 3.5 | Screw Tip | extruder-food-screw-tip | 1× | 2 | · | part |
| 4 | Drive Unit 6 parts | extruder-food-drive | 1× | 1 | 149 | assembly |
| 4.1 | Main Drive Motor 4 parts | extruder-food-main-motor | 1× | 1 | 25 | assembly |
| 4.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 4.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 4.1.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 4.1.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 4.2 | Torque Distribution Gearbox 5 parts | extruder-food-distribution-gearbox | 1× | 1 | 15 | assembly |
| 4.2.1 | Helical Gear Pair | gear-pair | 3× | 3 | · | part |
| 4.2.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 4.2.3 | Ball Bearing | ball-bearing | 6× | 6 | · | part |
| 4.2.4 | Oil Seal | oil-seal | 4× | 4 | · | part |
| 4.2.5 | Gear Oil | gear-oil | 1× | 1 | · | part |
| 4.3 | Tandem Thrust Bearing | extruder-food-thrust-bearing | 2× | 2 | · | part |
| 4.4 | Drive Coupling | extruder-food-coupling | 1× | 1 | · | part |
| 4.5 | Variable Frequency Drive 4 parts | extruder-food-vfd | 1× | 1 | 103 | assembly |
| 4.5.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 4.5.2 | IGBT Power Module | igbt-module | 1× | 1 | · | part |
| 4.5.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 4.5.4 | SMD Passive (R/C/L) | smd-passives | 100× | 100 | · | part |
| 4.6 | Gearbox Lube System 3 parts | extruder-food-lube-system | 1× | 1 | 3 | assembly |
| 4.6.1 | Lube Oil Pump | extruder-food-lube-pump | 1× | 1 | · | part |
| 4.6.2 | Oil Cooler | extruder-food-oil-cooler | 1× | 1 | · | part |
| 4.6.3 | Oil Filter | extruder-food-oil-filter | 1× | 1 | · | part |
| 5 | Die and Cutter 6 parts | extruder-food-die-cutter | 1× | 1 | 17 | assembly |
| 5.1 | Die Plate | extruder-food-die-plate | 1× | 1 | · | part |
| 5.2 | Die Insert | extruder-food-die-insert | 8× | 8 | · | part |
| 5.3 | Face Cutter Head | extruder-food-cutter-head | 1× | 1 | · | part |
| 5.4 | Cutter Blade | extruder-food-cutter-blade | 4× | 4 | · | part |
| 5.5 | Cutter Motor | extruder-food-cutter-motor | 1× | 1 | · | part |
| 5.6 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 6 | Thermal System 5 parts | extruder-food-thermal-system | 1× | 1 | 403 | assembly |
| 6.1 | Heating Element | heating-element | 6× | 6 | · | part |
| 6.2 | Barrel Cooling Jacket | extruder-food-cooling-jacket | 6× | 6 | · | part |
| 6.3 | Cooling Water Pump | extruder-food-water-pump | 1× | 1 | · | part |
| 6.4 | Cooling Solenoid Valve | extruder-food-solenoid-valve | 6× | 6 | · | part |
| 6.5 | Zone Temperature Controller 4 parts | extruder-food-temp-controller | 6× | 6 | 64 | assembly |
| 6.5.1 | Bare PCB | pcb-bare | 1× | 6 | · | part |
| 6.5.2 | Microcontroller | mcu | 1× | 6 | · | part |
| 6.5.3 | Relay | relay | 2× | 12 | · | part |
| 6.5.4 | SMD Passive (R/C/L) | smd-passives | 60× | 360 | · | part |
| 7 | Liquid Injection 5 parts | extruder-food-liquid-injection | 1× | 1 | 12 | assembly |
| 7.1 | Water Injection Nozzle | extruder-food-water-injector | 2× | 2 | · | part |
| 7.2 | Steam Injection Nozzle | extruder-food-steam-injector | 2× | 2 | · | part |
| 7.3 | High-Pressure Injection Pump 3 parts | extruder-food-injection-pump | 1× | 1 | 4 | assembly |
| 7.3.1 | Pump Piston | extruder-food-pump-piston | 1× | 1 | · | part |
| 7.3.2 | Pump Motor | extruder-food-pump-motor | 1× | 1 | · | part |
| 7.3.3 | O-Ring Set | oring-set | 2× | 2 | · | part |
| 7.4 | Liquid Flow Meter | extruder-food-flow-meter | 2× | 2 | · | part |
| 7.5 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 8 | Control Panel 7 parts | extruder-food-control-panel | 1× | 1 | 187 | assembly |
| 8.1 | NEMA 4X Enclosure | extruder-food-enclosure | 1× | 1 | · | part |
| 8.2 | PLC Module 4 parts | extruder-food-plc | 1× | 1 | 175 | assembly |
| 8.2.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.2.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 8.2.3 | Relay | relay | 12× | 12 | · | part |
| 8.2.4 | SMD Passive (R/C/L) | smd-passives | 160× | 160 | · | part |
| 8.3 | HMI Touchscreen 3 parts | extruder-food-hmi | 1× | 1 | 3 | assembly |
| 8.3.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.3.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.3.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.4 | Screw Torque Monitor | extruder-food-torque-monitor | 1× | 1 | · | part |
| 8.5 | DC Contactor | contactor | 4× | 4 | · | part |
| 8.6 | E-Stop Button | extruder-food-estop | 2× | 2 | · | part |
| 8.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9 | Base Frame 4 parts | extruder-food-frame | 1× | 1 | 12 | assembly |
| 9.1 | Base Weldment | extruder-food-base-weldment | 1× | 1 | · | part |
| 9.2 | Leveling Foot | extruder-food-leveling-foot | 6× | 6 | · | part |
| 9.3 | Guard Panel | extruder-food-guard-panel | 4× | 4 | · | part |
| 9.4 | Fastener Set | fastener-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Drum Drying Machine
634 parts · shares 21 with this page
 Steam-Jacketed Kettle
133 parts · shares 10 with this page
 Continuous Cooker
789 parts · shares 22 with this page
Scraped Cooking Kettle
334 parts · shares 22 with this page
 Paddle Mixer
388 parts · shares 21 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $1k–$500k. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| gea.com ↗ | Düsseldorf, DE | Process technology | 20 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 20 units | 12–20 wks |
| tetrapak.com ↗ | Pully, CH | Food packaging & processing | 20 units | 12–20 wks |
| jbtc.com ↗ | Chicago, US | Food processing equipment | 20 units | 12–20 wks |
| alfalaval.com ↗ | Lund, SE | Heat transfer & separation | 20 units | 12–20 wks |
870-word article