Electron Beam Welding Machine
ProductOverview
An electron beam welding machine joins metal by firing a focused stream of high-speed electrons at the joint inside a vacuum chamber. When the electrons strike the work their kinetic energy converts to heat in a spot a fraction of a millimetre across, melting and vaporizing metal so fast that the beam drills a narrow vapour cavity, called a keyhole, deep into the joint. As the part moves under the beam the cavity travels with it and molten metal closes in behind, leaving a weld that is deep, narrow, and almost parallel sided. A single pass can fuse plate over a hundred millimetres thick in one shot, something arc welding cannot do without many passes and large amounts of filler.
The machine is built around four problems: making the beam, keeping it in vacuum, focusing it, and moving the part precisely beneath it. The Electron Gun makes and accelerates the beam, the Vacuum Chamber and Vacuum System hold the working vacuum, the Beam Optics focus and steer it, and the Work Manipulator carries the work. The High-Voltage Power Supply feeds the accelerating voltage, the Control Cabinet sequences everything, and the Cooling Unit removes the waste heat.
The electron gun
The beam starts in the Electron Gun, a triode column that works like an oversized vacuum tube. A Tungsten Cathode of tungsten is heated white hot by the Filament Supply until it boils off electrons by thermionic emission. Around it sits the Wehnelt Cylinder, a biased cup that both shapes the emitted cloud and meters how much current passes, so adjusting its bias is how the operator turns the beam up or down. The electrons are then pulled through the apertured Accelerating Anode, which is held at ground while the cathode floats at tens of thousands of volts negative, and they accelerate across that gap to a large fraction of the speed of light. The whole stack is held off by the HV Ceramic Insulator inside the Gun Housing, with the heater floated at full potential by the Filament Isolation Transformer.
Vacuum and X-ray containment
Electrons scatter off air molecules, so the beam will not survive outside vacuum. The Vacuum Chamber is a heavy welded Chamber Shell strong enough to resist the crushing load of atmospheric pressure once it is empty, closed by a Chamber Door and its Door Seal. The Vacuum System pulls it down: a Roughing Pump takes it from atmosphere to medium vacuum, then a Turbomolecular Pump carries it to the working range near a hundred-thousandth of a millibar, with Vacuum Valve gates isolating the stages and Vacuum Gauge heads reading pressure across the whole span. Because high-speed electrons hitting metal generate X-rays, the operator watches through a lead glass Leaded Viewport and the chamber walls double as radiation shielding.
Focusing and steering the beam
A raw beam is too broad to weld with, so the Beam Optics use magnetic fields rather than glass to shape it. The Magnetic Focus Lens is a solenoid lens that converges the beam to a spot a tenth of a millimetre across at the work surface, and the Stigmator Coil trims any oval distortion so the spot stays round. The Alignment Coil centers the beam through the lens to remove off-axis blur, while the Deflection Coil can scan the spot rapidly to widen the weld, oscillate it across a gap, or rastered into an imaging mode that lets the operator see the joint before welding. All of these coils are fed precise currents by the Coil Driver, and changing focus current on the fly is how the machine controls penetration depth during a weld.
Power, motion, and control
The accelerating voltage comes from the High-Voltage Power Supply, where a HV Step-Up Transformer steps the mains up and a HV Rectifier Stack turns it to DC, both submerged in the HV Oil Tank of insulating oil to stop arc-over, then carried to the gun by the screened HV Cable. Beam current is regulated by the Bias Control Board driving the Wehnelt. Inside the chamber the Work Manipulator moves the part: a XY Cross Table on Linear Guide Rail rails and Ball Screw drives positions it, a Rotary Table spins cylinders for circular seams, and vacuum-rated Servo Motors drive both. The Control Cabinet cabinet ties it together with a CNC Controller running the weld program, an Operator Console console, an Safety Interlock that forbids the beam unless vacuum and shielding are confirmed, and an I/O Rack switching valves and pumps.
Use, advantages, and limits
Electron beam welding goes where heat input must be tiny and penetration deep: turbine disks, gear assemblies, sensor housings, nuclear and aerospace components, and dissimilar-metal joints that would crack with arc heat. Because the weld is narrow and the heat-affected zone small, parts distort little and finished machined surfaces near the joint often survive unmarked. Most welds are autogenous, fusing the parent metal with no filler, which keeps the joint chemically clean. The limits are the cost and the cycle: every part must fit in the Vacuum Chamber and wait through pump-down, the High-Voltage Power Supply and Cooling Unit are expensive, and X-ray shielding is mandatory. For high-value parts that demand a deep, clean, low-distortion weld, those costs are justified, and no other process matches its depth-to-width ratio in a single pass.
Electron Beam Welding Machine parts and their functions
8 top-level parts · 670 parts in total · full bill of materials below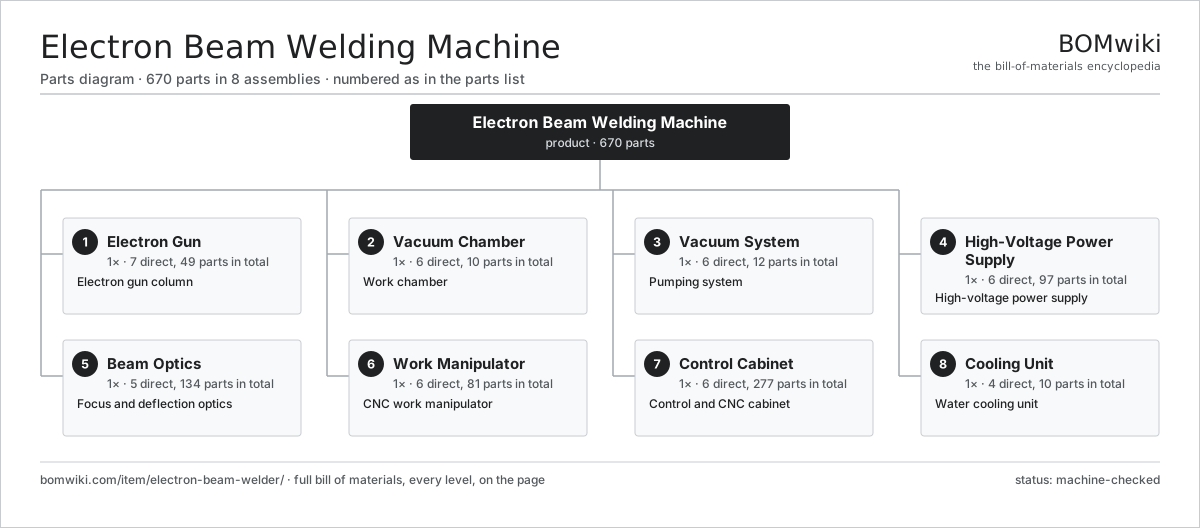
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Electron Gun 7 parts | 1× | Electron gun column |
| 2 | Vacuum Chamber 6 parts | 1× | Work chamber |
| 3 | Vacuum System 6 parts | 1× | Pumping system |
| 4 | High-Voltage Power Supply 6 parts | 1× | High-voltage power supply |
| 5 | Beam Optics 5 parts | 1× | Focus and deflection optics |
| 6 | Work Manipulator 6 parts | 1× | CNC work manipulator |
| 7 | Control Cabinet 6 parts | 1× | Control and CNC cabinet |
| 8 | Cooling Unit 4 parts | 1× | Water cooling unit |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Electron Beam Welding Machine
8 top-level lines · 78 rows shown · 670 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Electron Gun 7 parts | electron-beam-welder-gun | 1× | 1 | 49 | assembly |
| 1.1 | Tungsten Cathode | electron-beam-welder-cathode | 1× | 1 | · | part |
| 1.2 | Wehnelt Cylinder | electron-beam-welder-wehnelt | 1× | 1 | · | part |
| 1.3 | Accelerating Anode | electron-beam-welder-anode | 1× | 1 | · | part |
| 1.4 | HV Ceramic Insulator | electron-beam-welder-gun-insulator | 1× | 1 | · | part |
| 1.5 | Gun Housing | electron-beam-welder-gun-housing | 1× | 1 | · | part |
| 1.6 | Filament Supply 3 parts | electron-beam-welder-filament-supply | 1× | 1 | 42 | assembly |
| 1.6.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 1.6.2 | Filament Isolation Transformer | electron-beam-welder-filament-transformer | 1× | 1 | · | part |
| 1.6.3 | SMD Passive (R/C/L) | smd-passives | 40× | 40 | · | part |
| 1.7 | O-Ring Set | oring-set | 2× | 2 | · | part |
| 2 | Vacuum Chamber 6 parts | electron-beam-welder-vacuum-chamber | 1× | 1 | 10 | assembly |
| 2.1 | Chamber Shell | electron-beam-welder-chamber-shell | 1× | 1 | · | part |
| 2.2 | Chamber Door | electron-beam-welder-chamber-door | 1× | 1 | · | part |
| 2.3 | Door Seal | electron-beam-welder-door-seal | 1× | 1 | · | part |
| 2.4 | Leaded Viewport | electron-beam-welder-viewport | 2× | 2 | · | part |
| 2.5 | Vacuum Feedthrough | electron-beam-welder-feedthrough | 4× | 4 | · | part |
| 2.6 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 3 | Vacuum System 6 parts | electron-beam-welder-vacuum-system | 1× | 1 | 12 | assembly |
| 3.1 | Roughing Pump | electron-beam-welder-roughing-pump | 1× | 1 | · | part |
| 3.2 | Turbomolecular Pump | turbo-pump | 1× | 1 | · | part |
| 3.3 | Vacuum Valve | electron-beam-welder-vacuum-valve | 3× | 3 | · | part |
| 3.4 | Vacuum Gauge | electron-beam-welder-vacuum-gauge | 2× | 2 | · | part |
| 3.5 | Pumping Manifold | electron-beam-welder-vacuum-manifold | 1× | 1 | · | part |
| 3.6 | O-Ring Set | oring-set | 4× | 4 | · | part |
| 4 | High-Voltage Power Supply 6 parts | electron-beam-welder-hv-supply | 1× | 1 | 97 | assembly |
| 4.1 | HV Step-Up Transformer | electron-beam-welder-hv-transformer | 1× | 1 | · | part |
| 4.2 | HV Rectifier Stack | electron-beam-welder-hv-rectifier | 1× | 1 | · | part |
| 4.3 | HV Oil Tank | electron-beam-welder-hv-tank | 1× | 1 | · | part |
| 4.4 | HV Cable | electron-beam-welder-hv-cable | 1× | 1 | · | part |
| 4.5 | Bias Control Board 3 parts | electron-beam-welder-bias-board | 1× | 1 | 92 | assembly |
| 4.5.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 4.5.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 4.5.3 | SMD Passive (R/C/L) | smd-passives | 90× | 90 | · | part |
| 4.6 | Power Supply | power-supply | 1× | 1 | · | part |
| 5 | Beam Optics 5 parts | electron-beam-welder-beam-optics | 1× | 1 | 134 | assembly |
| 5.1 | Magnetic Focus Lens | electron-beam-welder-focus-coil | 1× | 1 | · | part |
| 5.2 | Deflection Coil | electron-beam-welder-deflection-coil | 1× | 1 | · | part |
| 5.3 | Stigmator Coil | electron-beam-welder-stigmator | 1× | 1 | · | part |
| 5.4 | Alignment Coil | electron-beam-welder-alignment-coil | 1× | 1 | · | part |
| 5.5 | Coil Driver 4 parts | electron-beam-welder-coil-driver | 1× | 1 | 130 | assembly |
| 5.5.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 5.5.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 5.5.3 | Power MOSFET | mosfet | 8× | 8 | · | part |
| 5.5.4 | SMD Passive (R/C/L) | smd-passives | 120× | 120 | · | part |
| 6 | Work Manipulator 6 parts | electron-beam-welder-motion-stage | 1× | 1 | 81 | assembly |
| 6.1 | XY Cross Table | electron-beam-welder-xy-table | 1× | 1 | · | part |
| 6.2 | Rotary Table | electron-beam-welder-rotary-table | 1× | 1 | · | part |
| 6.3 | Linear Guide Rail | linear-guide | 4× | 4 | · | part |
| 6.4 | Ball Screw | ball-screw | 2× | 2 | · | part |
| 6.5 | Servo Motor 4 parts | servo-motor | 3× | 3 | 24 | assembly |
| 6.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 3 | 3 | assembly |
| 6.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 3 | 19 | assembly |
| 6.5.3 | Encoder | encoder | 1× | 3 | · | part |
| 6.5.4 | Motor Housing | motor-housing | 1× | 3 | · | part |
| 6.6 | Part Fixture | electron-beam-welder-fixture | 1× | 1 | · | part |
| 7 | Control Cabinet 6 parts | electron-beam-welder-control | 1× | 1 | 277 | assembly |
| 7.1 | CNC Controller 4 parts | electron-beam-welder-cnc | 1× | 1 | 204 | assembly |
| 7.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.1.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 7.1.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.1.4 | SMD Passive (R/C/L) | smd-passives | 200× | 200 | · | part |
| 7.2 | Operator Console 3 parts | electron-beam-welder-hmi | 1× | 1 | 3 | assembly |
| 7.2.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.2.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.2.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.3 | Safety Interlock | electron-beam-welder-interlock | 1× | 1 | · | part |
| 7.4 | I/O Rack 3 parts | electron-beam-welder-io-rack | 1× | 1 | 37 | assembly |
| 7.4.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.4.2 | Relay | relay | 16× | 16 | · | part |
| 7.4.3 | Connector | connector | 20× | 20 | · | part |
| 7.5 | Wire Bundle | wire-bundle | 2× | 2 | · | part |
| 7.6 | Connector | connector | 30× | 30 | · | part |
| 8 | Cooling Unit 4 parts | electron-beam-welder-cooling | 1× | 1 | 10 | assembly |
| 8.1 | Water Chiller | electron-beam-welder-chiller | 1× | 1 | · | part |
| 8.2 | Circulation Pump | electron-beam-welder-coolant-pump | 1× | 1 | · | part |
| 8.3 | Coolant Line | electron-beam-welder-coolant-line | 6× | 6 | · | part |
| 8.4 | Flow Switch | electron-beam-welder-flow-switch | 2× | 2 | · | part |
Related products
same domain, ranked by shared parts Railway Wheel Lathe
1,201 parts · shares 6 with this page
Spring End Grinding Machine
1,048 parts · shares 6 with this page
Twin-Column Vertical Turret Lathe
1,387 parts · shares 6 with this page
Stud and Track Rollformer
517 parts · shares 5 with this page
Roller Shutter Slat Rollformer
524 parts · shares 4 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,018-word article