Washer Stamping Press
ProductOverview
A washer stamping press makes flat washers by punching them out of a strip of metal. In one stroke a compound die pierces the center hole and cuts the outer disc, so a finished washer drops out the bottom while the strip advances and the next washer is stamped. It is a high-rate, low-cost operation: a press can make several hundred washers a minute from a coil, with the only waste being the center slugs and the skeleton web left after the discs are punched out. The same press, with different tooling, stamps any flat sheet-metal part, but washer dies are among the simplest and most common, which is why the machine is often set up and named for them.
The press is a frame that drives a ram up and down through a die. The Press Frame carries the load, the Ram Slide reciprocates the upper die, the Crank Drive powers the stroke, the Die Set does the cutting, the Strip Feed indexes the strip, the Part and Scrap Handling system clears parts and waste, and the Control System runs and protects the cycle.
Frame and slide
Most washer presses use a gap or C frame, open at the front so strip can run straight through. The Press Frame is a Frame Casting carrying a Bolster Plate that mounts the lower die, with the slide riding on adjustable Slide Gib strips and a Operation Guard over the die area. The Ram Slide is a Ram Body whose closed height is set by a Shut-height Screw so the die just shears through the strip, with a Punch Holder mounting the upper tool and a Counterbalance air cylinder offsetting the slide weight so the drive sees a balanced load. A gap frame deflects slightly under load, which limits the tightest tolerances, but it is cheap and easy to feed.
Flywheel drive
Punching is a brief high-force event, so the Crank Drive stores energy in a Flywheel driven by the Main Motor through Drive Belt pairs. A Clutch and Brake couples the flywheel to the Crankshaft for each stroke, or leaves it engaged for continuous running, and the Pitman converts crank rotation into the straight ram stroke, all on Ball Bearing supports. The clutch-brake is also the main safety element: it must stop the slide mid-stroke reliably, since the press runs fast enough that a single missed stop is dangerous.
The compound die
The cut is made by the Die Set, a compound tool that does both the pierce and the blank in one stroke so the hole is always concentric with the disc. Upper and lower Die Shoe plates ride together on Guide Pillar posts for alignment. As the ram descends, the Pierce Punch cuts the center bore and the Blanking Punch cuts the outer disc, both shearing against the Die Button, while the Stripper Plate plate, backed by Coil Spring pressure, holds the strip flat and strips it off the punch on the up-stroke. Doing pierce and blank together is why a compound die makes a truer washer than two separate operations.
Strip feed
Stock comes off a Decoiler and through a Straightener that flattens the coil curve, then into a servo Roll Feed that advances the strip exactly one washer pitch each stroke. Because the feed must register precisely with the die, Pilot Pin pins enter pre-punched locating holes and pull the strip into final position just before the punches hit, correcting any small feed error. The Servo Motor feed is timed to index only while the ram is clear of the strip, so feed accuracy and timing together set how fast the press can run without the punches striking a mis-positioned strip.
Scrap, parts, and control
After punching, finished washers drop through the Part Chute to a Collection Bin, helped by Air-blow Nozzle jets that also clear center slugs from the die. The skeleton strip left behind runs into a Scrap Chopper that cuts it into short pieces for recycling, since a continuous scrap web would tangle. The Control System cabinet sets stroke rate with an Microcontroller on a Bare PCB, a Power Supply feeds the logic, and Relay safety chains tie in the guard and clutch-brake. A Die Protection sensor stops the press if a slug fails to clear or the strip misfeeds, since a stacked slug can crack a die in one stroke. The operator works from the Operator Panel.
Materials, output, and use
Washer presses run steel, stainless, brass, copper, and aluminium strip, sized to the washer thickness, and a tooling change sets the inner and outer diameters. The operation is pure shearing, fast and cheap, with material use limited by how tightly the discs can be nested across the strip width. Output reaches hundreds of washers a minute, which is why this is the standard way flat washers are made, and the same press also stamps shims, brackets, lamination blanks, and contacts. Within the fastener family it complements the cold formers: where the Bolt Heading Machine and Nut Forming Machine form parts from wire, the washer press shears flat parts from strip, and both feed the same assembled fastener sets.
Washer Stamping Press parts and their functions
7 top-level parts · 85 parts in total · full bill of materials below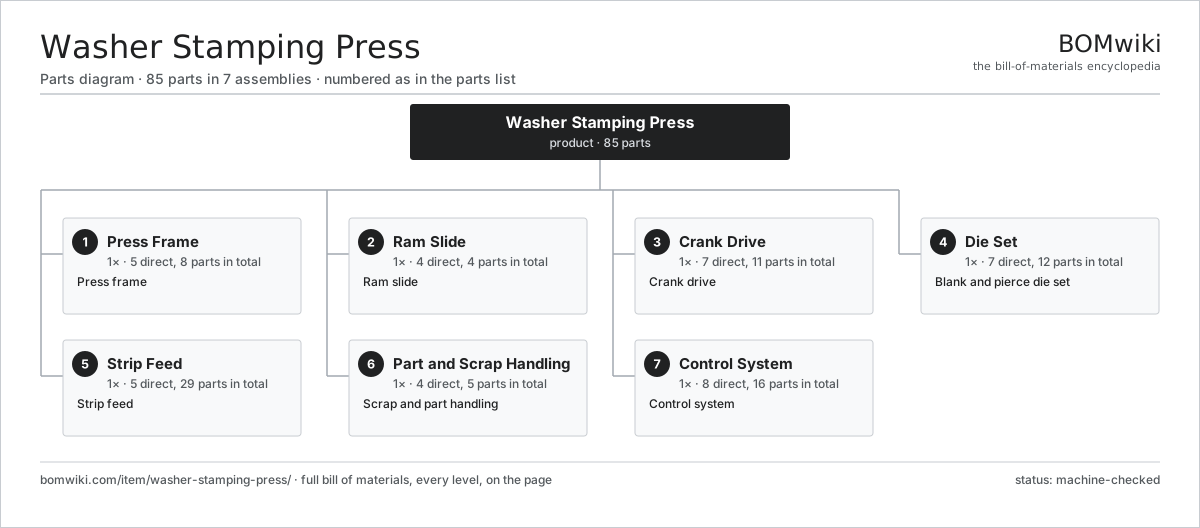
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Press Frame 5 parts | 1× | Press frame |
| 2 | Ram Slide 4 parts | 1× | Ram slide |
| 3 | Crank Drive 7 parts | 1× | Crank drive |
| 4 | Die Set 7 parts | 1× | Blank and pierce die set |
| 5 | Strip Feed 5 parts | 1× | Strip feed |
| 6 | Part and Scrap Handling 4 parts | 1× | Scrap and part handling |
| 7 | Control System 8 parts | 1× | Control system |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Washer Stamping Press
7 top-level lines · 51 rows shown · 85 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Press Frame 5 parts | washer-stamping-press-frame | 1× | 1 | 8 | assembly |
| 1.1 | Frame Casting | washer-stamping-press-frame-casting | 1× | 1 | · | part |
| 1.2 | Bolster Plate | washer-stamping-press-bolster | 1× | 1 | · | part |
| 1.3 | Slide Gib | washer-stamping-press-gib | 4× | 4 | · | part |
| 1.4 | Operation Guard | washer-stamping-press-guard | 1× | 1 | · | part |
| 1.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Ram Slide 4 parts | washer-stamping-press-slide | 1× | 1 | 4 | assembly |
| 2.1 | Ram Body | washer-stamping-press-ram | 1× | 1 | · | part |
| 2.2 | Shut-height Screw | washer-stamping-press-adjust-screw | 1× | 1 | · | part |
| 2.3 | Punch Holder | washer-stamping-press-punch-holder | 1× | 1 | · | part |
| 2.4 | Counterbalance | washer-stamping-press-counterbalance | 1× | 1 | · | part |
| 3 | Crank Drive 7 parts | washer-stamping-press-drive | 1× | 1 | 11 | assembly |
| 3.1 | Main Motor | washer-stamping-press-main-motor | 1× | 1 | · | part |
| 3.2 | Flywheel | washer-stamping-press-flywheel | 1× | 1 | · | part |
| 3.3 | Clutch and Brake | washer-stamping-press-clutch-brake | 1× | 1 | · | part |
| 3.4 | Crankshaft | washer-stamping-press-crankshaft | 1× | 1 | · | part |
| 3.5 | Pitman | washer-stamping-press-pitman | 1× | 1 | · | part |
| 3.6 | Drive Belt | drive-belt | 2× | 2 | · | part |
| 3.7 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 4 | Die Set 7 parts | washer-stamping-press-die-set | 1× | 1 | 12 | assembly |
| 4.1 | Die Shoe | washer-stamping-press-die-shoe | 2× | 2 | · | part |
| 4.2 | Guide Pillar | washer-stamping-press-guide-pillar | 2× | 2 | · | part |
| 4.3 | Blanking Punch | washer-stamping-press-blank-punch | 1× | 1 | · | part |
| 4.4 | Pierce Punch | washer-stamping-press-pierce-punch | 1× | 1 | · | part |
| 4.5 | Die Button | washer-stamping-press-die-button | 1× | 1 | · | part |
| 4.6 | Stripper Plate | washer-stamping-press-stripper | 1× | 1 | · | part |
| 4.7 | Coil Spring | coil-spring | 4× | 4 | · | part |
| 5 | Strip Feed 5 parts | washer-stamping-press-feed | 1× | 1 | 29 | assembly |
| 5.1 | Decoiler | washer-stamping-press-decoiler | 1× | 1 | · | part |
| 5.2 | Straightener | washer-stamping-press-straightener | 1× | 1 | · | part |
| 5.3 | Roll Feed | washer-stamping-press-roll-feed | 1× | 1 | · | part |
| 5.4 | Pilot Pin | washer-stamping-press-pilot | 2× | 2 | · | part |
| 5.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 5.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 5.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 5.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 5.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 6 | Part and Scrap Handling 4 parts | washer-stamping-press-scrap | 1× | 1 | 5 | assembly |
| 6.1 | Part Chute | washer-stamping-press-part-chute | 1× | 1 | · | part |
| 6.2 | Scrap Chopper | washer-stamping-press-scrap-chopper | 1× | 1 | · | part |
| 6.3 | Air-blow Nozzle | washer-stamping-press-air-blow | 2× | 2 | · | part |
| 6.4 | Collection Bin | washer-stamping-press-bin | 1× | 1 | · | part |
| 7 | Control System 8 parts | washer-stamping-press-control | 1× | 1 | 16 | assembly |
| 7.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.4 | Relay | relay | 6× | 6 | · | part |
| 7.5 | Die Protection | washer-stamping-press-die-protect | 1× | 1 | · | part |
| 7.6 | Operator Panel | washer-stamping-press-hmi | 1× | 1 | · | part |
| 7.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 7.8 | Connector | connector | 4× | 4 | · | part |
Related products
same domain, ranked by shared parts Bevel Gear Generator
201 parts · shares 3 with this page
Blanking Press Line
350 parts · shares 3 with this page
Bolt Heading Machine
102 parts · shares 3 with this page
Camshaft Grinder
489 parts · shares 3 with this page
 Crankshaft Grinder
511 parts · shares 3 with this page
 Creep-Feed Grinder
571 parts · shares 3 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
969-word article