Roll Tapping Machine
ProductOverview
A roll tapping machine produces internal threads by pressing and rolling metal into shape instead of cutting it away. A fluteless forming tap, lobed rather than grooved, is driven into a pre-drilled hole; its lobes displace the wall material and flow it up into the thread crests. No chips are made, which is the central difference from a conventional cutting tap. Because the grain of the metal is bent around the thread rather than severed, a rolled thread is stronger in shear and fatigue than a cut thread of the same size, and the finished surface is burnished smooth. The trade is that the process only works in ductile metals, needs a more precise starting hole, and demands far heavier lubrication because the tap is working the metal hard rather than slicing it.
The machine drives the tap with the Tapping Spindle Head carried on the Frame and Column. A Feed and Reversing Unit unit pushes the tap in at the thread lead and reverses it at depth, the Tap Holder floats the tap so it can pull to its own pitch, the Lubrication System system floods the forming zone, the Workholding Fixture holds the part, and the Control Cabinet sets and sequences the cycle.
Spindle and drive
The Tapping Spindle Head carries far more torque than a cutting-tap head because forming metal resists harder than shearing it. A Servo Motor drives through a Helical Gearbox into the Spindle Shaft, which runs on a stack of Ball Bearing units for radial support and Thrust Bearing pairs to take the axial push of driving the tap into the hole. The shaft rides in a Quill that slides for feed, and Oil Seal rings keep forming oil out of the bearings. The servo allows the controller to ramp speed at entry, hold a steady forming speed, and brake quickly before reversal so the thread depth is repeatable.
Feed and reversal
Forming a thread requires the tap to advance exactly one pitch per turn, the same as the lead it is creating. The Feed and Reversing Unit unit handles this with a Lead Cam Screw cut to the thread pitch and a Lead Cam that lets the tap pull itself to the true lead once it has bitten. When the Depth Stop reaches the set depth, the Reversing Clutch flips spindle direction and the tap rolls back out, backed by Coil Spring return and a Helical Gear Pair in the reversing train. On servo machines this reversal is done electronically, but the lead-tracking principle is the same: feed must follow the thread, not fight it, or the new thread tears.
Tap holder
The Tap Holder is a tension-compression float that lets the tap correct small errors between the mechanical feed rate and the lead it is forming. A Tap Collet grips the square drive of the Forming Tap, and Float Spring pairs let the holder stretch and compress by a few tenths of a millimetre so the tap is never forced ahead of or behind its own thread. A Torque Limiter slips before the tap snaps if the hole is undersized or the metal too hard, which protects the costly forming tap. The forming tap itself has no flutes; its cross section is a rounded polygon whose lobes do the burnishing, and it lasts far longer than a cutting tap because there are no cutting edges to wear.
Lubrication and workholding
Cold forming generates heat and high contact pressure, so the Lubrication System system is not optional. A Oil Pump draws heavy forming oil from the Oil Tank through a Oil Filter and floods the hole through Flood Nozzle jets, with a Pressure Sensor confirming flow before the cycle starts. Without this oil the tap galls and the thread surface tears. The part is held by the Workholding Fixture: a Pneumatic Vise driven by an Air Cylinder squeezes the part against Locator stops on the Work Table, so the pre-drilled hole sits true under the spindle and resists the forming torque.
Hole preparation and materials
The starting hole matters more for roll tapping than for cutting. Because metal is displaced rather than removed, the drill must leave more material than a cut tap would need, and the hole diameter is held to a tighter tolerance: too small and the tap overloads, too large and the thread crests come up short. Roll tapping works only in metals that flow without cracking, such as low and medium carbon steels below about 35 HRC, stainless, aluminium, brass, and copper. Cast iron and hardened steel are not candidates because they fracture rather than flow. Within the right materials the rolled thread comes out with no burr, a polished finish, and a continuous grain line that resists stripping.
Control and use
The Control Cabinet cabinet runs the cycle. A Spindle Drive commands the spindle, an Microcontroller on a Bare PCB sequences entry speed, depth, dwell, and reversal, a Power Supply feeds the logic, and Relay interlocks tie in the clamp, guard, and oil-flow checks before motion is allowed. The operator sets thread size, depth, and speed at the Operator Panel. These machines run in high-volume threading of nuts, fittings, valve bodies, and sheet-metal parts where thread strength and the absence of chips both matter. They share a forming-not- cutting philosophy with the Flat-Die Thread Roller, which rolls external threads the same way, and they replace cut tapping wherever the metal is ductile enough to be rolled.
Roll Tapping Machine parts and their functions
7 top-level parts · 82 parts in total · full bill of materials below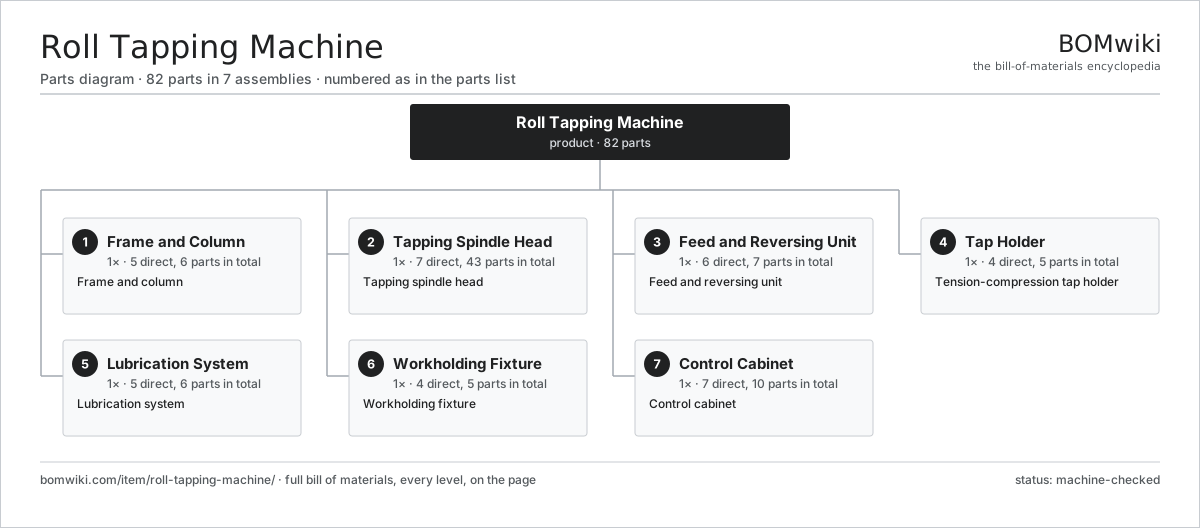
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Frame and Column 5 parts | 1× | Frame and column |
| 2 | Tapping Spindle Head 7 parts | 1× | Tapping spindle head |
| 3 | Feed and Reversing Unit 6 parts | 1× | Feed and reversing unit |
| 4 | Tap Holder 4 parts | 1× | Tension-compression tap holder |
| 5 | Lubrication System 5 parts | 1× | Lubrication system |
| 6 | Workholding Fixture 4 parts | 1× | Workholding fixture |
| 7 | Control Cabinet 7 parts | 1× | Control cabinet |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Roll Tapping Machine
7 top-level lines · 53 rows shown · 82 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Frame and Column 5 parts | roll-tapping-machine-frame | 1× | 1 | 6 | assembly |
| 1.1 | Base Casting | roll-tapping-machine-base-casting | 1× | 1 | · | part |
| 1.2 | Column | roll-tapping-machine-column | 1× | 1 | · | part |
| 1.3 | Slide Way | roll-tapping-machine-slide-ways | 2× | 2 | · | part |
| 1.4 | Counterweight | roll-tapping-machine-counterweight | 1× | 1 | · | part |
| 1.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Tapping Spindle Head 7 parts | roll-tapping-machine-spindle | 1× | 1 | 43 | assembly |
| 2.1 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 2.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 2.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 2.1.3 | Encoder | encoder | 1× | 1 | · | part |
| 2.1.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 2.2 | Helical Gearbox 4 parts | gearbox | 1× | 1 | 9 | assembly |
| 2.2.1 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 2.2.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 2.2.3 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 2.2.4 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 2.3 | Spindle Shaft | roll-tapping-machine-spindle-shaft | 1× | 1 | · | part |
| 2.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 2.5 | Thrust Bearing | roll-tapping-machine-thrust-bearing | 2× | 2 | · | part |
| 2.6 | Quill | roll-tapping-machine-quill | 1× | 1 | · | part |
| 2.7 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 3 | Feed and Reversing Unit 6 parts | roll-tapping-machine-feed | 1× | 1 | 7 | assembly |
| 3.1 | Lead Cam Screw | roll-tapping-machine-lead-screw | 1× | 1 | · | part |
| 3.2 | Reversing Clutch | roll-tapping-machine-reversing-clutch | 1× | 1 | · | part |
| 3.3 | Depth Stop | roll-tapping-machine-depth-stop | 1× | 1 | · | part |
| 3.4 | Lead Cam | roll-tapping-machine-feed-cam | 1× | 1 | · | part |
| 3.5 | Coil Spring | coil-spring | 2× | 2 | · | part |
| 3.6 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 4 | Tap Holder 4 parts | roll-tapping-machine-tap-holder | 1× | 1 | 5 | assembly |
| 4.1 | Tap Collet | roll-tapping-machine-collet | 1× | 1 | · | part |
| 4.2 | Float Spring | roll-tapping-machine-float-spring | 2× | 2 | · | part |
| 4.3 | Forming Tap | roll-tapping-machine-form-tap | 1× | 1 | · | part |
| 4.4 | Torque Limiter | roll-tapping-machine-torque-limiter | 1× | 1 | · | part |
| 5 | Lubrication System 5 parts | roll-tapping-machine-lube | 1× | 1 | 6 | assembly |
| 5.1 | Oil Pump | roll-tapping-machine-pump | 1× | 1 | · | part |
| 5.2 | Oil Tank | roll-tapping-machine-tank | 1× | 1 | · | part |
| 5.3 | Flood Nozzle | roll-tapping-machine-nozzle | 2× | 2 | · | part |
| 5.4 | Oil Filter | roll-tapping-machine-filter | 1× | 1 | · | part |
| 5.5 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 6 | Workholding Fixture 4 parts | roll-tapping-machine-clamp | 1× | 1 | 5 | assembly |
| 6.1 | Work Table | roll-tapping-machine-table | 1× | 1 | · | part |
| 6.2 | Pneumatic Vise | roll-tapping-machine-vise | 1× | 1 | · | part |
| 6.3 | Locator | roll-tapping-machine-locator | 2× | 2 | · | part |
| 6.4 | Air Cylinder | roll-tapping-machine-air-cylinder | 1× | 1 | · | part |
| 7 | Control Cabinet 7 parts | roll-tapping-machine-control | 1× | 1 | 10 | assembly |
| 7.1 | Spindle Drive | roll-tapping-machine-vfd | 1× | 1 | · | part |
| 7.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.5 | Relay | relay | 4× | 4 | · | part |
| 7.6 | Operator Panel | roll-tapping-machine-hmi | 1× | 1 | · | part |
| 7.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Rotary Draw Bender
821 parts · shares 5 with this page
 Flat-Die Thread Roller
65 parts · shares 4 with this page
Cut-to-Length Line
500 parts · shares 4 with this page
 Shaft Straightening Press
93 parts · shares 4 with this page
Strip Tension Leveler
513 parts · shares 4 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
991-word article