Wire Mesh Welding Machine
ProductOverview
A wire mesh welding machine builds flat welded mesh by resistance-welding every point where a cross wire meets a longitudinal line wire. The line wires run continuously down the length of the machine while cross wires are laid across them one at a time; at each crossing a pair of electrodes presses the wires together and passes a current that fuses them. After a row is welded the mesh steps forward by one pitch and the next cross wire is welded, so the panel grows row by row until a shear cuts it to length. The output is the welded mesh used as concrete reinforcement, fencing, cages, and grating.
The line wires come from the Line Wire Feed and the cross wires from the Cross Wire Feed. The Welding Electrode Beam welds a whole row of crossings at once, powered by the Welding Transformer Bank. The Mesh Step Advance advances the mesh by one pitch between welds, the Mesh Shear cuts finished panels, and the Control System sets the geometry and weld energy. The Electrode Cooling system keeps the rows of electrodes from overheating.
Feeding line and cross wires
The longitudinal wires define the mesh and must arrive straight and evenly spaced. The Line Wire Feed runs one Line Decoiler per line wire, and the Line Straightener Bank bank works the curl out of each with its Straightening Roller rollers. A Spacing Comb comb fixes the pitch between wires, and the Line Wire Clamp holds them still during each weld so they cannot creep.
The cross wires are made one at a time. The Cross Wire Feed pulls wire from its Cross Decoiler, straightens it through the Cross Straightener, and the Cross Wire Cutter crops it to the mesh width. The Drop Chute and Placer then lays the cut wire square across all the line wires at the next pitch position, ready for the beam to come down.
Welding a full row at once
The defining feature of a mesh welder is that it welds every crossing in a row simultaneously. The Welding Electrode Beam carries a full-width row of electrode pairs: an Upper Electrode above and a Lower Electrode below each line wire, held in cooled Electrode Holder units. Each pair has its own Electrode Cylinder so weld force is even and electrodes can be lifted out where a wire is skipped to change the pattern.
Current comes from the Welding Transformer Bank. Several Welding Transformer units each feed a group of crossings, because a single transformer cannot supply a wide mesh evenly. Each transformer has a laminated Transformer Core, a Primary Winding, and a low-turn Secondary Winding, and is switched by an SCR Contactor so the controller can phase-control the energy into each zone. The Secondary Busbar secondary connects each transformer to its electrode group.
Step advance, shearing, and cutoff
Between welds the mesh must move forward by exactly one pitch, accurately, or the mesh openings will not be square. The Mesh Step Advance does this: a Step Carriage running on a Ball Screw and Linear Guide Rail rails carries two Step Gripper jaws that grip the leading cross wire, pull the mesh one pitch, release, and return for the next bite, driven by a Servo Motor.
When the programmed number of cross wires for a panel is welded, the Mesh Shear cuts the mesh free. The Shear Cylinder drives a full-width Shear Blade through every line wire at once against the Shear Anvil, and the finished panel slides onto the Run-off Table.
Materials and construction
Line and cross wires are cold-drawn low-carbon steel, ribbed for reinforcement mesh or plain and often galvanized for fencing. Electrodes are CuCrZr alloy, which keeps conductivity and hardness at the temperature the weld zone reaches; they wear at the tip and are dressed or swapped on a schedule. The Base Weldment is a heavy steel structure because the weld beam force and step accuracy depend on a frame that does not flex. The whole work zone, where wires drop and the beam closes, sits behind interlocked Sheet Metal Panel guarding.
Variants and use
Machines are sized by mesh width and wire diameter. A reinforcement-mesh line makes wide panels of ribbed bar at standard pitches for concrete slabs, walls, and precast; a fence-mesh machine makes lighter galvanized mesh in fixed patterns at high speed. Pitch is programmable on better machines, set at the Control System, so one line can run several mesh patterns by skipping line wires through their Electrode Cylinder units and changing the step. Reinforcement mesh follows standards for bar size and spacing, and the Weld Controller logs current per zone so weld strength can be verified. The welded mesh that comes off these lines reinforces almost all modern concrete and forms a large share of industrial and security fencing.
Control and cooling
The Control System runs the line. A PLC sequences cross-wire placement, beam close, weld, step, and shear with interlocks, while the Weld Controller fires each SCR Contactor and holds weld energy per zone using feedback from Current Sensor units, since a wide mesh can need different current at the edges than the centre. Operators set wire sizes, pitch, panel length, and weld parameters at the LCD Panel. Because many electrode pairs pass high current at a steady cycle rate, the Electrode Cooling system runs continuously: the Coolant Pump feeds water to every holder and busbar and the Heat Exchanger sheds the heat, holding electrode temperature so weld quality stays even from the first row of a shift to the last.
Wire Mesh Welding Machine parts and their functions
9 top-level parts · 841 parts in total · full bill of materials below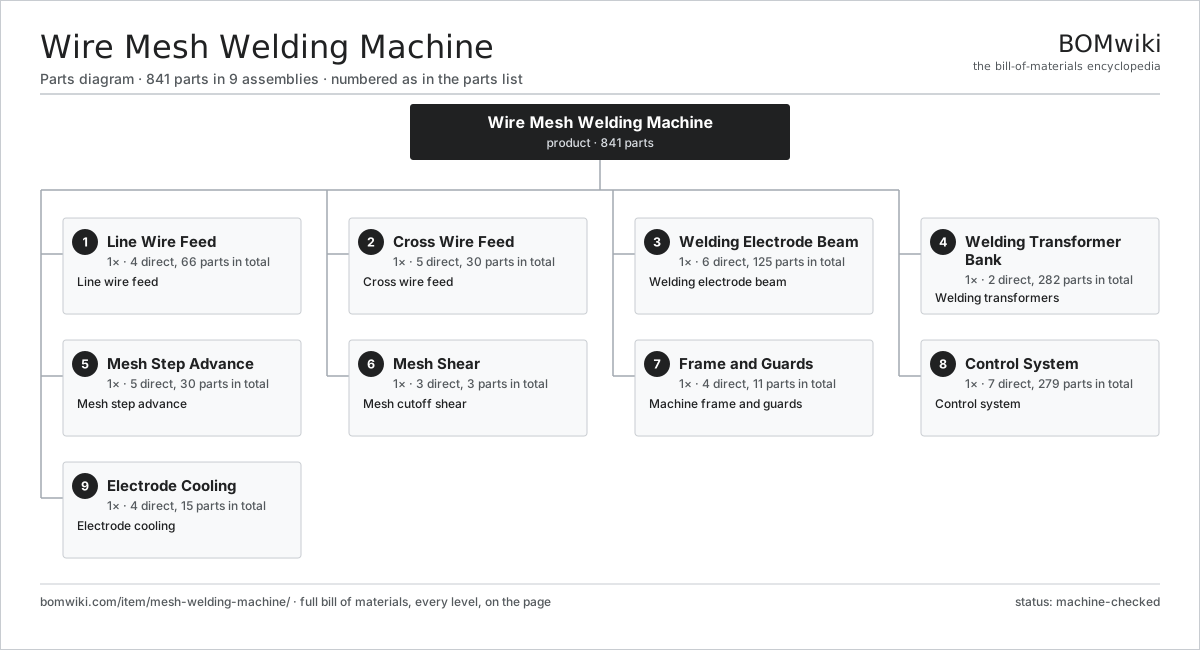
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Line Wire Feed 4 parts | 1× | Line wire feed |
| 2 | Cross Wire Feed 5 parts | 1× | Cross wire feed |
| 3 | Welding Electrode Beam 6 parts | 1× | Welding electrode beam |
| 4 | Welding Transformer Bank 2 parts | 1× | Welding transformers |
| 5 | Mesh Step Advance 5 parts | 1× | Mesh step advance |
| 6 | Mesh Shear 3 parts | 1× | Mesh cutoff shear |
| 7 | Frame and Guards 4 parts | 1× | Machine frame and guards |
| 8 | Control System 7 parts | 1× | Control system |
| 9 | Electrode Cooling 4 parts | 1× | Electrode cooling |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Wire Mesh Welding Machine
9 top-level lines · 78 rows shown · 841 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Line Wire Feed 4 parts | mesh-welding-machine-line-wire-feed | 1× | 1 | 66 | assembly |
| 1.1 | Line Decoiler 2 parts | mesh-welding-machine-line-decoiler | 8× | 8 | 3 | assembly |
| 1.1.1 | Reel Cradle | mesh-welding-machine-reel-cradle | 1× | 8 | · | part |
| 1.1.2 | Ball Bearing | ball-bearing | 2× | 16 | · | part |
| 1.2 | Line Straightener Bank 3 parts | mesh-welding-machine-line-straightener | 1× | 1 | 40 | assembly |
| 1.2.1 | Straightening Roller | mesh-welding-machine-straightener-roll | 16× | 16 | · | part |
| 1.2.2 | Roller Block | mesh-welding-machine-roll-block | 8× | 8 | · | part |
| 1.2.3 | Ball Bearing | ball-bearing | 16× | 16 | · | part |
| 1.3 | Spacing Comb | mesh-welding-machine-wire-guide | 1× | 1 | · | part |
| 1.4 | Line Wire Clamp | mesh-welding-machine-line-clamp | 1× | 1 | · | part |
| 2 | Cross Wire Feed 5 parts | mesh-welding-machine-cross-wire-feed | 1× | 1 | 30 | assembly |
| 2.1 | Cross Decoiler 2 parts | mesh-welding-machine-cross-decoiler | 1× | 1 | 3 | assembly |
| 2.1.1 | Reel Cradle | mesh-welding-machine-reel-cradle | 1× | 1 | · | part |
| 2.1.2 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 2.2 | Cross Straightener | mesh-welding-machine-cross-straightener | 1× | 1 | · | part |
| 2.3 | Cross Wire Cutter | mesh-welding-machine-cross-cutter | 1× | 1 | · | part |
| 2.4 | Drop Chute and Placer | mesh-welding-machine-drop-chute | 1× | 1 | · | part |
| 2.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 2.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 2.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 2.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 2.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 3 | Welding Electrode Beam 6 parts | mesh-welding-machine-weld-beam | 1× | 1 | 125 | assembly |
| 3.1 | Upper Electrode | mesh-welding-machine-upper-electrode | 24× | 24 | · | part |
| 3.2 | Lower Electrode | mesh-welding-machine-lower-electrode | 24× | 24 | · | part |
| 3.3 | Electrode Holder | mesh-welding-machine-electrode-holder | 48× | 48 | · | part |
| 3.4 | Electrode Cylinder | mesh-welding-machine-weld-cylinder | 24× | 24 | · | part |
| 3.5 | Beam Frame | mesh-welding-machine-beam-frame | 1× | 1 | · | part |
| 3.6 | Secondary Busbar | mesh-welding-machine-busbar | 4× | 4 | · | part |
| 4 | Welding Transformer Bank 2 parts | mesh-welding-machine-transformer-bank | 1× | 1 | 282 | assembly |
| 4.1 | Welding Transformer 3 parts | mesh-welding-machine-welding-transformer | 6× | 6 | 3 | assembly |
| 4.1.1 | Transformer Core | mesh-welding-machine-transformer-core | 1× | 6 | · | part |
| 4.1.2 | Primary Winding | mesh-welding-machine-primary-winding | 1× | 6 | · | part |
| 4.1.3 | Secondary Winding | mesh-welding-machine-secondary-winding | 1× | 6 | · | part |
| 4.2 | SCR Contactor 4 parts | mesh-welding-machine-scr-stack | 6× | 6 | 44 | assembly |
| 4.2.1 | Power Thyristor | mesh-welding-machine-thyristor | 2× | 12 | · | part |
| 4.2.2 | Heatsink | mesh-welding-machine-heatsink | 1× | 6 | · | part |
| 4.2.3 | Bare PCB | pcb-bare | 1× | 6 | · | part |
| 4.2.4 | SMD Passive (R/C/L) | smd-passives | 40× | 240 | · | part |
| 5 | Mesh Step Advance 5 parts | mesh-welding-machine-step-feed | 1× | 1 | 30 | assembly |
| 5.1 | Step Gripper | mesh-welding-machine-step-gripper | 2× | 2 | · | part |
| 5.2 | Step Carriage | mesh-welding-machine-step-carriage | 1× | 1 | · | part |
| 5.3 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 5.4 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 5.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 5.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 5.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 5.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 5.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 6 | Mesh Shear 3 parts | mesh-welding-machine-shear | 1× | 1 | 3 | assembly |
| 6.1 | Shear Blade | mesh-welding-machine-shear-blade | 1× | 1 | · | part |
| 6.2 | Shear Cylinder | mesh-welding-machine-shear-cylinder | 1× | 1 | · | part |
| 6.3 | Shear Anvil | mesh-welding-machine-shear-anvil | 1× | 1 | · | part |
| 7 | Frame and Guards 4 parts | mesh-welding-machine-frame | 1× | 1 | 11 | assembly |
| 7.1 | Base Weldment | mesh-welding-machine-base-weldment | 1× | 1 | · | part |
| 7.2 | Sheet Metal Panel | sheet-panel | 8× | 8 | · | part |
| 7.3 | Run-off Table | mesh-welding-machine-runoff-table | 1× | 1 | · | part |
| 7.4 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 8 | Control System 7 parts | mesh-welding-machine-control | 1× | 1 | 279 | assembly |
| 8.1 | PLC 3 parts | mesh-welding-machine-plc | 1× | 1 | 122 | assembly |
| 8.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.1.3 | SMD Passive (R/C/L) | smd-passives | 120× | 120 | · | part |
| 8.2 | Weld Controller 4 parts | mesh-welding-machine-weld-controller | 1× | 1 | 126 | assembly |
| 8.2.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.2.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.2.3 | Current Sensor | current-sensor | 4× | 4 | · | part |
| 8.2.4 | SMD Passive (R/C/L) | smd-passives | 120× | 120 | · | part |
| 8.3 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.5 | Relay | relay | 12× | 12 | · | part |
| 8.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8.7 | Connector | connector | 16× | 16 | · | part |
| 9 | Electrode Cooling 4 parts | mesh-welding-machine-coolant | 1× | 1 | 15 | assembly |
| 9.1 | Coolant Pump | mesh-welding-machine-coolant-pump | 1× | 1 | · | part |
| 9.2 | Heat Exchanger | mesh-welding-machine-heat-exchanger | 1× | 1 | · | part |
| 9.3 | Coolant Tank | mesh-welding-machine-coolant-tank | 1× | 1 | · | part |
| 9.4 | Coolant Hose | mesh-welding-machine-coolant-hose | 12× | 12 | · | part |
Related products
same domain, ranked by shared parts Industrial TIG Welder
492 parts · shares 3 with this page
Bar Chamfering Machine
1,148 parts · shares 5 with this page
Camshaft Grinder
489 parts · shares 5 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,062-word article