Gear Honing Machine
ProductOverview
A gear honing machine finishes the teeth of a hardened gear, after heat treatment, to a fine surface and an accurate, quiet-running shape. Hardening distorts a gear slightly and leaves a rough surface, so a finishing step is needed; honing does it by running the gear in tight mesh with an abrasive internal-gear ring that abrades a few microns off each tooth flank. Unlike grinding, honing leaves a flank texture whose lay runs along the direction of rolling contact, and that texture is what makes a honed gear notably quieter than a ground one. It is the final operation on high-grade automotive transmission and electric-drive gears, where low noise is a selling point.
The machine resembles a gear shaving machine but works on hardened steel with an abrasive tool. The hardened gear mounts on the Work Head, the abrasive ring spins on the Honing Head, and the two are crossed at an angle by the Crossed-Axis Swivel so the abrasive slides along the flanks. The Cross Feed Slide sets the contact, a Tool Dresser keeps the ring true, and the whole machine stands on a vibration-damping Bed & Column.
How honing works
The Honing Ring is shaped like an internal gear and coated with diamond or CBN abrasive. It meshes with the work gear, and because the Crossed-Axis Swivel crosses the two axes by a few degrees, the contact point slides lengthwise along each flank as the pair rolls. That sliding is what abrades the metal: where shaving uses cutting serrations, honing uses bonded abrasive grit. The Hone Spindle Drive drives the ring and the ring drives the gear, while the Work Drive Servo on the work spindle controls the relative speed so the abrasive does its work at the right rate. The Cross Feed Slide sets how hard the ring presses into the gear, and the Pressure Sensor in the Hydraulic System holds that contact force steady so removal is even from gear to gear.
Work and honing heads
The Work Head holds the gear on a low-runout Work Arbor in Angular Contact Bearing sets, because any runout copies into the finished teeth. The Honing Head carries the ring in a Ring Holder that lets a worn ring be changed, also running in angular bearings. Both heads are carried on the Bed & Column, which is mineral cast, a polymer concrete that damps vibration far better than iron; this matters because chatter at honing speeds would spoil the fine surface the process is there to produce.
Dressing the ring
An abrasive ring wears and loses its exact tooth form, so the machine trues it in place. The Tool Dresser carries a Diamond Dressing Gear, a diamond-coated master gear, that meshes with the honing ring during a dressing cycle to restore its form and expose fresh abrasive. The Dresser Slide brings the dressing gear into mesh on a schedule the control manages, often after a set number of parts, so the ring holds its accuracy across a batch without the operator removing it.
Coolant and control
Honing makes very fine swarf, a mix of steel and shed abrasive, that must be kept out of the contact. The Coolant System system floods the mesh with honing oil through a Flood Nozzle and passes the returning oil through a Fine Filter fine enough to catch the micron-size particles before the oil is pumped again. The CNC Control runs the synchronised mesh, sets the crossed-axis angle through the Swivel Drive, manages the dressing cycle, and on many machines reads an in-process gauge to stop when the gear is to size. The operator programs the part at the Operator Display.
Use and variants
Gear honing is the quiet-gear finish: it is chosen where transmission and axle gears have to be both accurate and low-noise, which is why it has grown with electric drivetrains whose gear whine is no longer masked by an engine. It removes far less metal than grinding, so it is used to clean up and quiet a gear rather than to make large corrections; gears needing big shape changes are ground first, then honed. The flank texture left by honing is the point as much as the accuracy: the abrasive lays a fine cross-hatch that runs along the rolling direction, and that lay carries oil and meshes smoothly, so a honed gear runs several decibels quieter than the same gear ground. Removal is measured in single-digit microns, so honing cannot fix a mis-cut gear, only refine a good one. Variants include power honing machines that take more stock for combined correction and finishing, twin-spindle machines that load one gear while another is honed, dry honing setups for cleaner shop conditions, and cells that gauge every part and adjust the cycle automatically on a line.
Gear Honing Machine parts and their functions
10 top-level parts · 260 parts in total · full bill of materials below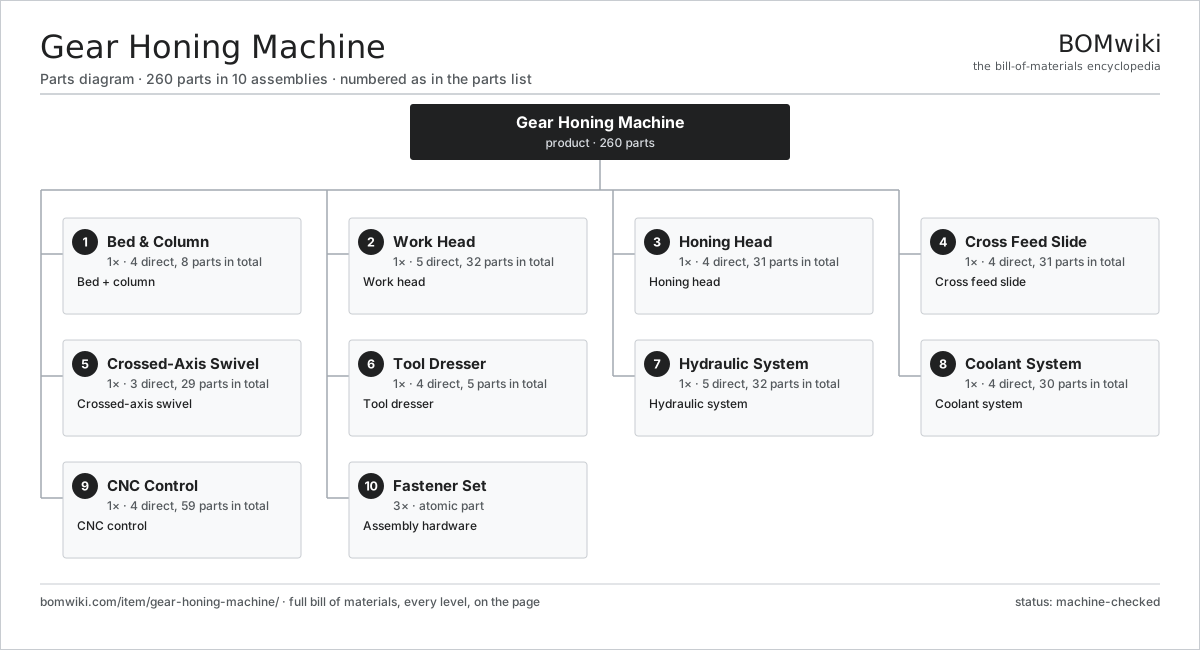
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Bed & Column 4 parts | 1× | Bed + column |
| 2 | Work Head 5 parts | 1× | Work head |
| 3 | Honing Head 4 parts | 1× | Honing head |
| 4 | Cross Feed Slide 4 parts | 1× | Cross feed slide |
| 5 | Crossed-Axis Swivel 3 parts | 1× | Crossed-axis swivel |
| 6 | Tool Dresser 4 parts | 1× | Tool dresser |
| 7 | Hydraulic System 5 parts | 1× | Hydraulic system |
| 8 | Coolant System 4 parts | 1× | Coolant system |
| 9 | CNC Control 4 parts | 1× | CNC control |
| 10 | Fastener Set | 3× | Assembly hardware |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Gear Honing Machine
10 top-level lines · 82 rows shown · 260 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Bed & Column 4 parts | gear-honing-machine-bed | 1× | 1 | 8 | assembly |
| 1.1 | Mineral-Cast Bed | gear-honing-machine-bed-casting | 1× | 1 | · | part |
| 1.2 | Column | gear-honing-machine-column | 1× | 1 | · | part |
| 1.3 | Slide Way | gear-honing-machine-way | 4× | 4 | · | part |
| 1.4 | Fastener Set | fastener-set | 2× | 2 | · | part |
| 2 | Work Head 5 parts | gear-honing-machine-work-head | 1× | 1 | 32 | assembly |
| 2.1 | Work Spindle | gear-honing-machine-work-spindle | 1× | 1 | · | part |
| 2.2 | Work Arbor | gear-honing-machine-arbor | 1× | 1 | · | part |
| 2.3 | Work Drive Servo 4 parts | gear-honing-machine-servo | 1× | 1 | 25 | assembly |
| 2.3.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 2.3.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 2.3.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 2.3.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 2.4 | Angular Contact Bearing | angular-bearing | 4× | 4 | · | part |
| 2.5 | Position Encoder | gear-honing-machine-encoder | 1× | 1 | · | part |
| 3 | Honing Head 4 parts | gear-honing-machine-hone-head | 1× | 1 | 31 | assembly |
| 3.1 | Hone Spindle Drive 4 parts | gear-honing-machine-hone-spindle | 1× | 1 | 25 | assembly |
| 3.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 3.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 3.1.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 3.1.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3.2 | Honing Ring | gear-honing-machine-hone-ring | 1× | 1 | · | part |
| 3.3 | Ring Holder | gear-honing-machine-ring-holder | 1× | 1 | · | part |
| 3.4 | Angular Contact Bearing | angular-bearing | 4× | 4 | · | part |
| 4 | Cross Feed Slide 4 parts | gear-honing-machine-cross-slide | 1× | 1 | 31 | assembly |
| 4.1 | Axis Feed Servo 5 parts | gear-honing-machine-axis-servo | 1× | 1 | 26 | assembly |
| 4.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 4.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 4.1.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 4.1.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 4.1.5 | Position Encoder | gear-honing-machine-encoder | 1× | 1 | · | part |
| 4.2 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 4.3 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 4.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 5 | Crossed-Axis Swivel 3 parts | gear-honing-machine-swivel | 1× | 1 | 29 | assembly |
| 5.1 | Swivel Table | gear-honing-machine-swivel-table | 1× | 1 | · | part |
| 5.2 | Swivel Drive 3 parts | gear-honing-machine-swivel-drive | 1× | 1 | 27 | assembly |
| 5.2.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 5.2.2 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 5.2.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 5.3 | Position Encoder | gear-honing-machine-encoder | 1× | 1 | · | part |
| 6 | Tool Dresser 4 parts | gear-honing-machine-dresser | 1× | 1 | 5 | assembly |
| 6.1 | Diamond Dressing Gear | gear-honing-machine-dress-gear | 1× | 1 | · | part |
| 6.2 | Dresser Spindle | gear-honing-machine-dress-spindle | 1× | 1 | · | part |
| 6.3 | Dresser Slide | gear-honing-machine-dress-slide | 1× | 1 | · | part |
| 6.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 7 | Hydraulic System 5 parts | gear-honing-machine-hydraulics | 1× | 1 | 32 | assembly |
| 7.1 | Hydraulic Pump 5 parts | gear-honing-machine-hyd-pump | 1× | 1 | 26 | assembly |
| 7.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 7.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 7.1.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 7.1.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 7.1.5 | Oil Seal | oil-seal | 1× | 1 | · | part |
| 7.2 | Oil Tank | gear-honing-machine-hyd-tank | 1× | 1 | · | part |
| 7.3 | Hydraulic Valve | gear-honing-machine-hyd-valve | 3× | 3 | · | part |
| 7.4 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 7.5 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 8 | Coolant System 4 parts | gear-honing-machine-coolant | 1× | 1 | 30 | assembly |
| 8.1 | Coolant Pump 5 parts | gear-honing-machine-coolant-pump | 1× | 1 | 26 | assembly |
| 8.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 8.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 8.1.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 8.1.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 8.1.5 | Oil Seal | oil-seal | 1× | 1 | · | part |
| 8.2 | Coolant Tank | coolant-tank | 1× | 1 | · | part |
| 8.3 | Fine Filter | gear-honing-machine-filter | 1× | 1 | · | part |
| 8.4 | Flood Nozzle | gear-honing-machine-nozzle | 2× | 2 | · | part |
| 9 | CNC Control 4 parts | gear-honing-machine-control | 1× | 1 | 59 | assembly |
| 9.1 | CNC Controller 5 parts | cnc-controller | 1× | 1 | 5 | assembly |
| 9.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.1.2 | Compute SoC Module | soc-module | 1× | 1 | · | part |
| 9.1.3 | I/O Board | io-board | 1× | 1 | · | part |
| 9.1.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 9.1.5 | HMI Panel | hmi-panel | 1× | 1 | · | part |
| 9.2 | Operator Display 4 parts | gear-honing-machine-display | 1× | 1 | 43 | assembly |
| 9.2.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.2.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 9.2.3 | Touch Digitizer | touch-digitizer | 1× | 1 | · | part |
| 9.2.4 | SMD Passive (R/C/L) | smd-passives | 40× | 40 | · | part |
| 9.3 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9.4 | Connector | connector | 10× | 10 | · | part |
| 10 | Fastener Set | fastener-set | 3× | 3 | · | part |
Related products
same domain, ranked by shared parts CNC Milling Machine
400 parts · shares 9 with this page
 Vertical Boring Mill
265 parts · shares 11 with this page
 CNC Lathe
511 parts · shares 7 with this page
CNC Metal Spinning Machine
768 parts · shares 8 with this page
Vertical Broaching Machine
220 parts · shares 4 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
866-word article